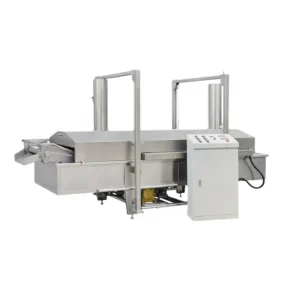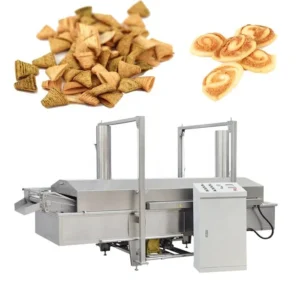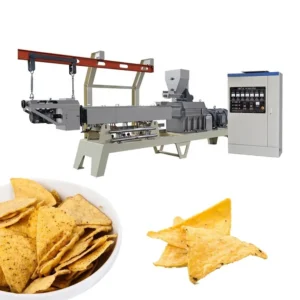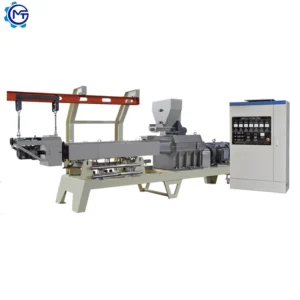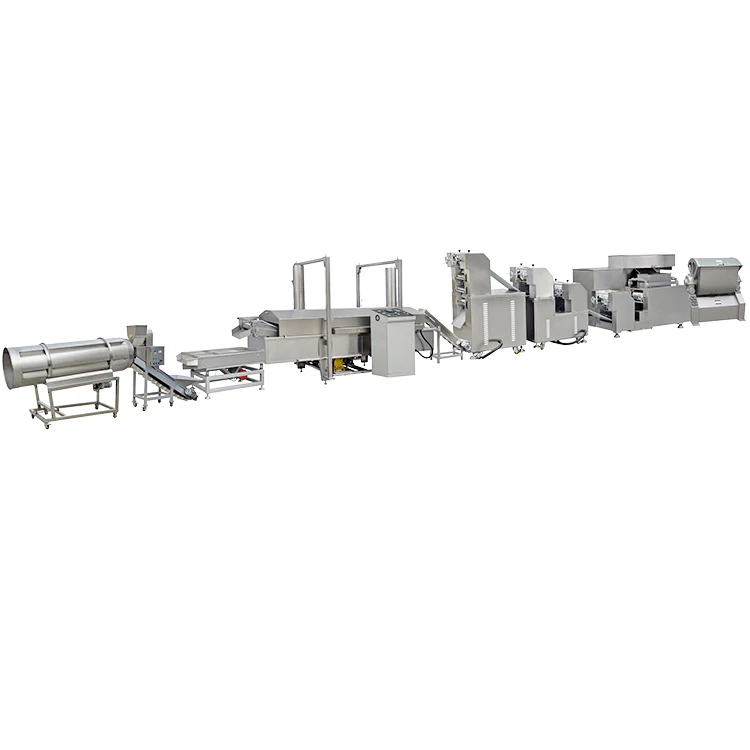
Full Equipment Range Integration — The MT100/MT120 frying chips making machine line is cataloged as a complete sequence from mixing through extrusion, frying, flavoring, and cooling, enabling buyers to survey every station before specifying a single vendor.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT100/MT120 |
| Product Type | Single Screw Extruder Snack Production Line |
| Extruder Type | Single Screw |
| Application | Snacks & pasta (golgappa / pani puri / turtle chips / four-layer crispy snacks) |
| Capacity | 120 kg/h (basis not stated in source — confirm raw material formulation, moisture, product shape and fryer parameters) |
| Total Power | 50–70 kW (electric heating approximately 100 kW; gas or diesel heating approximately 50–60 kW) |
| Voltage & Frequency | Three-phase 380 V / 50 Hz; Single-phase 220 V / 50 Hz (configurable to local supply) |
| Overall Dimensions (L×W×H) | 12,000–26,000 × 1,200 × 2,200 mm |
| Contact Material | Food-grade stainless steel 201 (304 option available) |
| Electrical Components | Motors: Siemens (China) or domestic top brand; Inverters: Delixi or Delta |
| Energy Options | Electricity / gas / diesel / steam (selectable per station) |
| Process Flow | Mixer → Screw Conveyor → Single Screw Extruder → Pulling & Cutting Machine → Automatic Fryer → Automatic Flavoring Line → Cooling |
| Assembly State | Complete line, factory-assembled modules |
| Certification | CE, ISO 9001 |
| Warranty | One year with lifetime technical guidance |
Application Suitability
| Application | Material or Output |
|---|---|
| Golgappa / pani puri shells | Potato starch, corn starch, wheat flour blends |
| Turtle chips (secondary puffing) | Starch-based pellets requiring frying expansion |
| Four-layer crispy snacks | Multi-layer dough sheets from starch and flour formulations |
| Screw shell, round tube, square tube | Corn starch and wheat flour with die adjustment |
| Ring and cartoon-shaped puffed snacks | Starch blends with custom die profiles |
| Pasta-type extruded shapes | Wheat flour and semolina formulations |
Why Nominal Capacity Figures Mislead Snack Line Buyers
A frying chips making machine manufacturer quotes 120 kg/h without stating which starch blend, moisture level, or die profile that figure was measured on.
Capacity is only meaningful when tied to your exact formulation and product shape.
I once watched a four-layer crispy snack line stall at the fryer because the buyer’s corn flour recipe carried higher moisture than the material used during the supplier’s test run. The layers fused during extrusion and collapsed after frying, turning out flat, dense chips that could not be packaged. The extruder was running at the nameplate speed the whole time, but usable output was effectively zero. [NEED_CITE: starch gelatinisation behaviour at varying moisture levels in single-screw extrusion] Sizing a snack extrusion line starts with your raw material data, not a catalog number.
Matching Every Station Across the Snack Line
The MT100/MT120 sequence is presented here as a full equipment range rather than a standalone extruder listing. That means the screw conveyor, fryer, flavoring drum, and cooler are each sized against the extruder’s throughput envelope, so no single station creates a bottleneck that leaves upstream equipment idling or downstream stations starved. Buyers surveying a frying chips making machine line for the first time can compare station footprints and utility draws before committing to a layout.
Selecting the Right Energy Source Per Station
Snack factories in different regions face different utility realities. This line allows each heating station — fryer, dryer, flavoring drum — to be specified with electricity, gas, diesel, or steam independently. A plant with abundant natural gas can route the fryer to gas burners while keeping the extruder barrel on electric heaters, reducing overall electrical load. The total installed power for the frying chips making machine shifts accordingly, dropping to the lower end of the 50–60 kW range when gas or diesel replaces electric heating across thermal stations. [NEED_CITE: industrial energy tariff comparison for gas versus electric heating in food processing]
How Screw Design and Die Geometry Shape the Final Chip
The single-screw extruder uses a configurable screw profile with adjustable compression to handle starch-based materials that vary in gelatinisation temperature and shear sensitivity. The screw geometry, combined with barrel temperature zones, controls residence time and the degree of starch cooking before the material reaches the die. Die inserts then define whether the output is a hollow tube, a flat ribbon destined for four-layer lamination, or a shaped pellet for secondary puffing in the fryer. Changing between screw shell, ring, and cartoon profiles requires a die swap rather than a full screw rebuild, keeping format changeover practical for a snack extrusion production line for sale to multi-product facilities. Moisture content at the mixer stage directly affects expansion ratio downstream — a point that matters especially for four-layer formats where layer separation depends on controlled steam release during frying.
The Cost of Skipping Configuration Verification
Specifying a frying line on price alone, without confirming which die profiles ship with the extruder, often means the buyer receives a generic set that does not cover the shapes their market demands. Commissioning then stalls while replacement dies are sourced and shipped. Similarly, choosing full-electric heating in a region where gas is a fraction of the cost locks the factory into higher per-shift energy expenses for the life of the line. [NEED_CITE: common causes of delayed commissioning in food extrusion installations] Voltage mismatches surface even later — a 380 V / 50 Hz line landed in a 440 V / 60 Hz market requires transformer upgrades or motor replacements before the first test run.
Why Source This Line Through the Full Equipment Catalog
Every station — mixer, conveyor, extruder, cutter, fryer, flavoring drum, cooler — is listed within the same equipment range, so throughput calculations are performed across matched modules rather than assembled from independent vendor quotes. The screw and die combination is specified against the buyer’s raw material sample rather than copied from a generic build. An in-house testing workshop is available for trial runs on the buyer’s actual starch formulation before the line ships. Food-grade stainless steel 201 contact surfaces are standard, with 304 available for environments requiring higher corrosion resistance. CE and ISO 9001 documentation accompanies every shipment.
Documentation & Verification
- Line layout drawing with station-by-station throughput matched to your starch recipe
- Machine specification sheet confirming voltage, frequency, and energy source per station
- Screw and die configuration record listing each die profile and its corresponding snack shape
- Factory test record including trial run results on buyer-supplied raw material when requested
- CE declaration of conformity and ISO 9001 certificate included in shipping documents
- Operation and maintenance manual with illustrated wear parts list
Installation, Commissioning & Support
- Foundation and floor space planning based on the 12,000–26,000 mm line length envelope
- Dedicated electrical circuit sizing for the 50–100 kW total load depending on heating configuration
- Factory-assembled modules arrive in sequence for staged mechanical and electrical connection
- First-run parameter setting covering barrel temperatures, screw speed, and fryer oil temperature
- Operator training on die changeover between tube, ring, and four-layer snack formats
- Wear parts list covering screws, dies, and fryer baskets with reorder lead-time guidance
What to Prepare Before Requesting a Quotation
Share your starch or flour formulation, including moisture content and any additives, along with the specific snack shapes you intend to produce and your target daily output. Confirm the voltage, frequency, and preferred energy source at your facility so the frying chips making machine manufacturer can configure each station correctly. Provide workshop dimensions and ceiling height to ensure the line layout fits your floor plan without post-delivery modifications.
Frequently Asked Questions
Q: How is the 120 kg/h capacity verified, and on which raw material and product shape does it apply?
A: The rated figure depends on the starch formulation, moisture percentage, die profile, and fryer settings used during testing. We recommend a trial run on your actual raw material in the testing workshop before final order, so the capacity is confirmed against the exact recipe and snack shape you will produce commercially.
Q: Which voltage, frequency, and control language will the line ship with for my country?
A: The standard offering covers three-phase 380 V / 50 Hz and single-phase 220 V / 50 Hz, both configurable to local supply standards. Control panel labeling and manual language are confirmed during the specification stage to match your operator team’s requirements.
Q: Can the line use gas or steam heating instead of full-electric to match my plant utility?
A: Yes. Each thermal station — fryer, dryer, flavoring drum — can be specified independently with electricity, gas, diesel, or steam. This flexibility allows the total connected electrical load to be reduced significantly when gas or steam is available on site.
Q: What die and screw configurations are available for the shapes I want to produce?
A: The single-screw extruder accepts interchangeable die inserts for screw shell, round tube, square tube, ring, cartoon profiles, and four-layer sheet formats. Screw compression is adjusted to suit your starch blend, and the configuration record shipped with the line documents each die-to-shape pairing.
Q: Which supporting stations are matched to the extruder throughput?
A: The full equipment range includes a mixer, screw conveyor, pulling and cutting machine, automatic fryer, flavoring drum, and cooler, each sized against the extruder output. This prevents bottlenecks where one station runs faster or slower than the rest of the line.