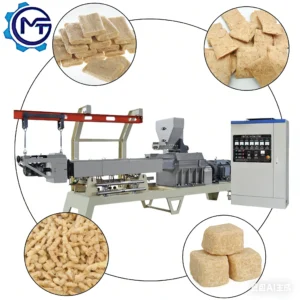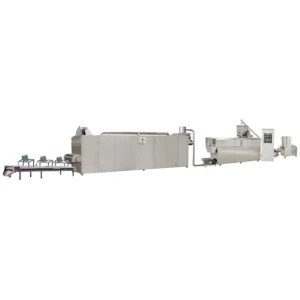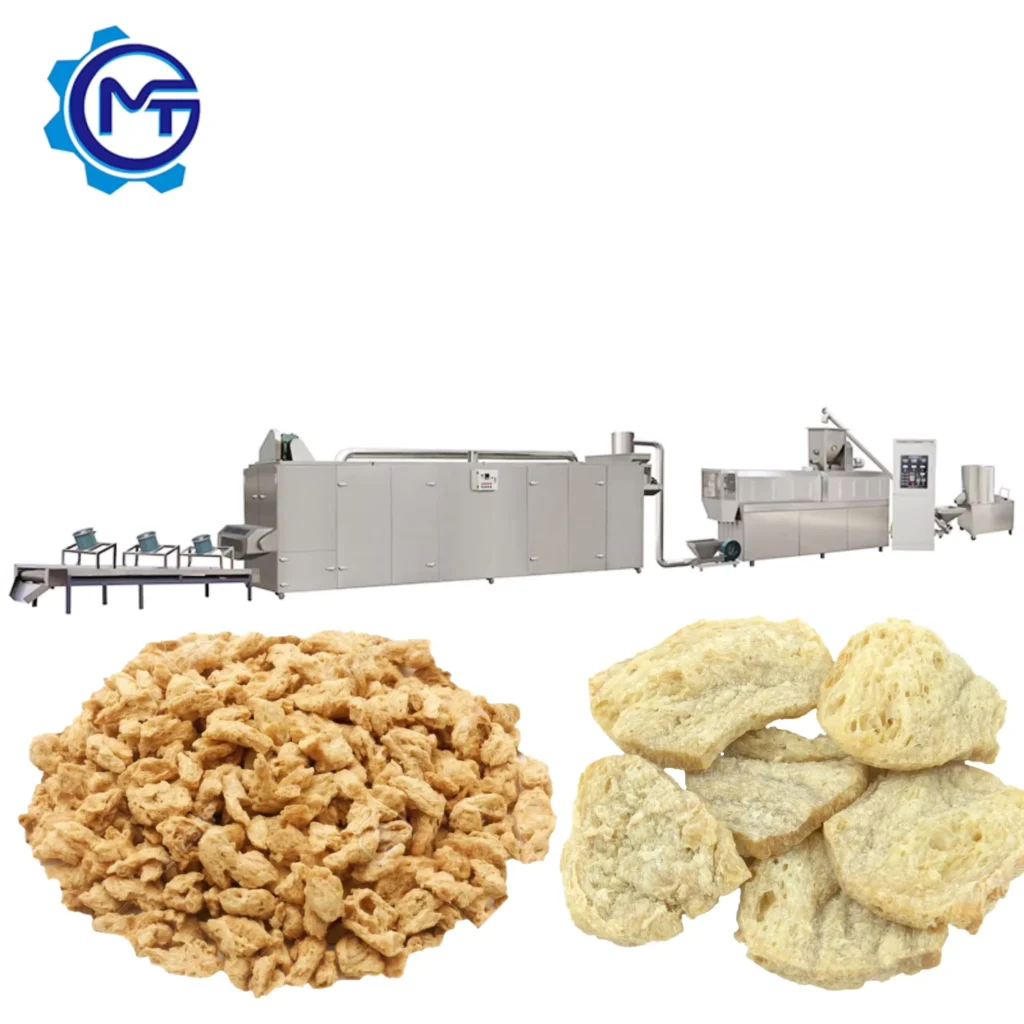
Every Station Catalogued — A complete textured soybean protein processing line where mixer batch size, extruder output, and dryer throughput are matched and listed so buyers can verify capacity balance before committing.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Textured Soybean Protein Processing Line |
| Extruder Models Available | MT65 / MT70 / MT75 / MT85 |
| Extruder Type | Twin Screw |
| Main Motor Power Options | 22 kW / 30 kW / 45 kW |
| Heating Power | 10 kW / 14 kW |
| Installed Power (MT65 / MT70 / MT75 / MT85) | 84 kW / 160 kW / 190 kW / 210 kW |
| Power Consumption (MT65 / MT70 / MT75 / MT85) | 59 kW / 120 kW / 140 kW / 140 kW |
| Output Capacity (MT65) | 100–150 kg/h (basis not stated in source — confirm raw material type, moisture content and product format) |
| Output Capacity (MT70) | 150–200 kg/h (basis not stated in source — confirm raw material type, moisture content and product format) |
| Output Capacity (MT75) | 150–200 kg/h (basis not stated in source — confirm raw material type, moisture content and product format) |
| Output Capacity (MT85) | 250–300 kg/h (basis not stated in source — confirm raw material type, moisture content and product format) |
| Mixer Type | Vertical, stainless steel 304 mixing ruler |
| Mixer Power Options | 4 kW / 7.5 kW / 15 kW |
| Mixer Batch Capacity | 20–30 kg / 70–80 kg / 170–180 kg (source value — verify against manufacturer catalog) |
| Dryer Drive | Double pitch roller chain drive, round-trip drying |
| Dryer Energy Options | Fuel / Gas / Electricity |
| Line Station Sequence | Mixer → Screw Conveyor → Twin Screw Extruder → Air Conveyor → Multi-layer Dryer → Cooling Machine |
| Overall Dimensions (MT65 / MT70 / MT75 / MT85) | 40×1.2×2.2 m / 41×1.5×2.2 m / 43×1.5×3.2 m / 45×1.5×3.5 m |
| Assembly State | Complete line, pre-shipment testing available |
| Warranty | 1 year complete guarantee, life-time maintenance service |
Application Suitability
| Application | Material or Output |
|---|---|
| Textured vegetable protein (TVP/TSP) production | Defatted soya flour, low temperature soya flakes |
| Soya nuggets and soya chunks manufacturing | Soybean dregs, peanut dregs |
| Plant-based meat analogue processing | Blended soy protein isolates with starch carriers |
| Vegetarian snack ingredient preparation | Textured protein pieces cut to specification |
| Meat extender and filler production | Rehydrated TVP for sausage and patty formulations |
Why "Nominal Output" Means Nothing Without Your Raw Material
The extruder only reaches its rated throughput when screw configuration, die design, and moisture profile match the exact protein content and particle size of your feedstock.
A textured soybean protein processing line quoted at a fixed kilogram-per-hour figure often falls short the moment the buyer switches from standard defatted soya flour to a locally sourced batch with different protein concentration. I have watched production stall because the screw combination was copied from a generic build, leaving the protein strands unable to align under shear. When the die pressure drops, the extrudate loses its fibrous structure and crumbles like wet meal instead of holding a meat-like bite. This is why every capacity figure in the table above carries a verification note — those numbers shift depending on what you actually feed into the hopper [NEED_CITE: raw material protein content and moisture impact on twin-screw extrusion throughput].
Station-by-Station Equipment Survey
This page catalogs every piece of equipment in the textured soybean protein processing line so that technical buyers can evaluate each station independently. The vertical mixer prepares raw material in batches sized to match extruder feed rate, with stainless steel 304 contact surfaces preventing contamination across product changeovers. A screw conveyor then meters the blended flour into the twin-screw extruder at a controlled rate, maintaining consistent residence time inside the barrel.
Extrusion, Drying, and Cooling as a Matched Sequence
The twin-screw extruder sits at the center of the line, where adjustable die moulds allow a single platform to produce soya nuggets, TVP granules, and larger soya chunks by swapping die plates and cutting speed. Downstream, an air conveyor lifts the hot extrudate into a multi-layer dryer that runs on a double pitch roller chain drive for round-trip drying — the buyer selects fuel, gas, or electricity based on local utility infrastructure. A cooling machine at the end of the sequence brings product temperature down before packing, preventing condensation inside sealed bags. Each station’s power rating and physical footprint appear in the specification table so that throughput matching can be checked on paper before the line ships [NEED_CITE: multi-layer dryer residence time and temperature profile for textured protein stabilization].
Reading the Power and Dimension Data
The installed power column shows the total electrical load of every motor and heating element running simultaneously, while the power consumption figure reflects typical draw under normal operating conditions — the gap between the two indicates headroom for startup surges. Main motor power steps up across the MT65 through MT85 range, with larger barrels requiring higher torque to maintain screw speed under the viscous resistance of high-protein dough. Overall line length stretches from 40 meters for the smallest configuration to 45 meters for the largest, a factor that determines workshop floor planning and utility routing. Mixer batch capacity tiers must be cross-referenced against extruder feed rate; a mixer that empties too slowly starves the screws, while one that dumps too fast causes surge feeding and inconsistent texture.
The Hidden Cost of a Mismatched Dryer
An extruder running at full output means little if the dryer cannot remove moisture fast enough to stabilize the extrudate. When dryer capacity lags behind, product piles up on the conveyor belts, surface moisture causes clumping, and the fibrous structure collapses before it sets. Buyers who specify the extruder first and treat the dryer as an afterthought frequently discover that their actual throughput is limited not by screw speed but by drying belt length and air temperature. This bottleneck is invisible in a quotation that lists only extruder output [NEED_CITE: moisture removal rate and dryer belt length correlation in protein extrusion lines].
Why Source the Full Equipment Range Here
Every station from mixer to cooling machine comes from a single supplier, so throughput is matched across the line rather than assembled from separate vendors with mismatched capacities. Screw configuration and die design are specified to the buyer’s raw material and target product format, not copied from a generic template. An in-house testing workshop allows trial runs on the customer’s actual defatted soya flour or low temperature flakes before shipment, confirming that the fibrous texture meets market expectations. The line is supported by pre-sales consultation through engineer design, on-site installation, commissioning, and ongoing maintenance. CE and ISO certifications are documented for export market compliance.
Documentation & Verification
- Line layout drawing showing station spacing and utility connection points for the chosen extruder model
- Screw and die configuration record matched to your specific soya flour protein content
- Electrical schematic with voltage and frequency confirmed for your facility’s power supply
- Trial run report on your raw material sample documenting extrudate texture and moisture level
- Factory test record verifying motor amperage and heating element function before dispatch
- Operation and maintenance manual covering daily inspection points for each station
Installation, Commissioning & Support
- Floor space of up to 45 meters in length requires level concrete footing with anchor bolt预埋 for extruder and dryer stations
- Dedicated electrical circuit sized to the installed power of the selected model, with voltage confirmed before production
- Line arrives in modular sections; extruder barrel, dryer frames, and mixer are reassembled on site by commissioning engineers
- First-run parameter setting covers barrel temperature zones, screw speed, and die gap adjusted to your raw material
- Operator training addresses daily screw inspection, mixer cleaning, and dryer belt tension checks
- Wear parts list identifies screws, dies, and cutter blades with reorder codes for the specific model purchased
What to Include in Your Inquiry
Provide the specific raw material type — defatted soya flour, low temperature flakes, or a blend — along with its protein percentage and moisture content so that screw configuration can be matched. Confirm your workshop length and ceiling height to verify that the chosen line configuration fits. State the local voltage, frequency, and preferred control language so that electrical panels and interface screens are built accordingly.
Frequently Asked Questions
Q: How is output capacity verified against my specific raw material and moisture content?
A: Before shipment, a trial run is conducted in the testing workshop using a sample of your raw material. Screw speed, barrel temperature zones, and moisture addition are adjusted until extrudate texture and throughput meet your product specification. The results are documented in a trial run report shared with you before the line is crated.
Q: Which dryer energy source fits my facility’s utility infrastructure?
A: The multi-layer dryer is available with fuel, gas, or electric heating. The selection depends on local energy costs and available utility connections at your plant. Confirming this early ensures the correct burner or element bank is installed and avoids delays during commissioning.
Q: Can individual stations be ordered separately, or is the line sold only as a complete package?
A: Each station — mixer, extruder, dryer, cooling machine — is catalogued with its own specifications and can be sourced individually to integrate with existing equipment. When ordering a single station, provide your current line’s throughput and interface dimensions so that matching is confirmed.
Q: What screw and die configurations are available for different TVP and TSP product formats?
A: Die plates are interchangeable to produce soya nuggets, granules, or chunks, and the screw combination is rearranged to control shear and residence time for each format. The configuration record is documented for your product so that future die or screw reorders match the original setup.
Q: How are mixer batch capacity and extruder feed rate matched to avoid bottlenecks?
A: Mixer batch size and cycle time are calculated against the extruder’s continuous feed rate so that the screw conveyor receives a steady supply. An undersized mixer causes intermittent starvation; an oversized one leads to surge feeding. The line layout proposal shows this calculation for your selected model.