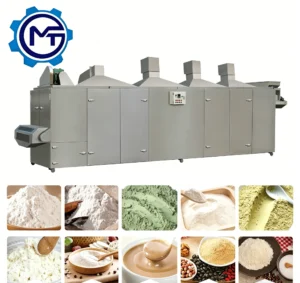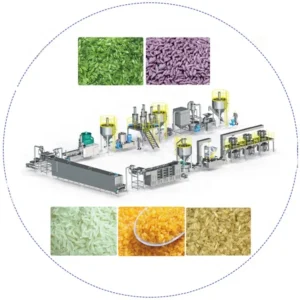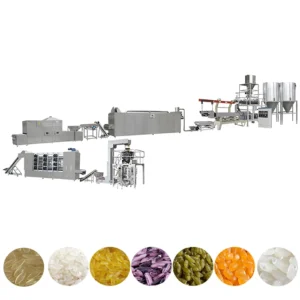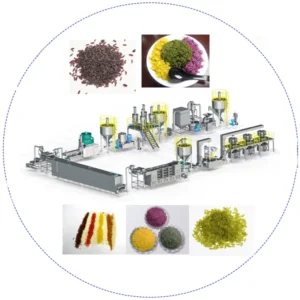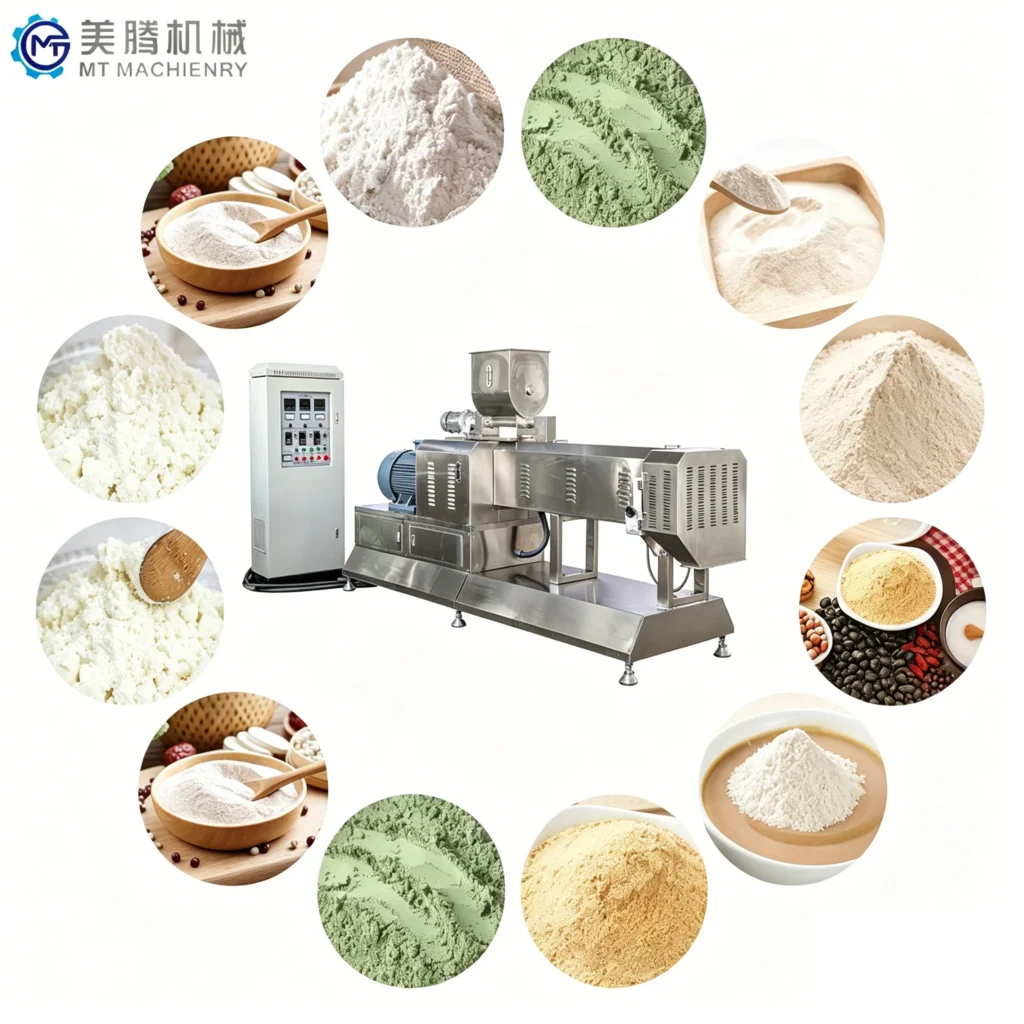
Integrated Material Handling — every station from batching to packing is matched for throughput on baby rice flour lines, preventing the dryer or cooler bottleneck that stalls extruder output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruder Baby Rice Flour Making Machine |
| Capacity | 150–500 kg/h on rice flour-based formulations (basis to be confirmed) |
| Screw Configuration | Twin-screw, segmented elements matched to starch gelatinisation profile |
| Barrel Sections | Multi-zone with independent heating and cooling channels |
| Main Motor Power | Configurable per installation requirement |
| Control System | Available with PLC or MCC control |
| Voltage | Configurable from 110V to 440V per destination market |
| Contact Materials | Food-grade stainless steel on all product-contact surfaces |
| Die Assembly | Interchangeable die plates for flour, pre-cooked flour, and instant porridge formats |
| Feeding System | Automated batching and volumetric dosing with pre-mixing |
Application Suitability
| Application | Material or Output |
|---|---|
| Instant baby rice porridge | Pre-gelatinised rice flour, single or blended with millet and oat |
| Fortified infant cereal | Rice flour base with vitamin and mineral premix addition |
| Rice-based weaning food | Blends of rice, corn, and legume flours at controlled moisture |
| Hypoallergenic infant formula carrier | Pure rice starch processed through controlled gelatinisation |
| Instant rice flour for reconstitution | Fully cooked and dried rice flour for consumer or industrial packing |
What "150–500 kg/h" Leaves Out on a Baby Rice Flour Line
Rated output holds only when raw material moisture, particle size, and barrel temperature profile are locked to the trial recipe.
I have stood in a humid workshop in West Africa watching a twin screw extruder for baby rice flour choke at the die plate because the local milled rice carried three percentage points more moisture than the factory sample. The nameplate capacity assumed a controlled 12–14% moisture feedstock. Once the barrel zones were re-tuned and screw speed adjusted downward to extend residence time, throughput stabilised — but the lesson was clear. Capacity numbers without raw material context are just marketing. Buyers sourcing nutritional powder processing lines should always confirm that the quoted figure rests on their actual flour, not a generic reference blend [NEED_CITE: raw material moisture variability in tropical milling environments].
Starch Gelatinisation as the Decisive Variable
Baby rice flour is fundamentally a starch gelatinisation product. The twin screw extruder for baby rice flour must hold the material inside the barrel long enough for complete starch conversion while avoiding excessive shear that degrades the final powder texture. Segmented screw elements let the process engineer set a gentle compression zone followed by a controlled cooking zone. This matters because under-gelatinised rice flour will not reconstitute smoothly in warm water — the exact failure a mother notices when preparing infant porridge.
Barrel Temperature Zoning for Nutrient Retention
Infant cereal formulations often carry heat-sensitive vitamin and mineral premixes added upstream or via a secondary dosing port. Multi-zone barrel heating with independent cooling channels allows the front zones to run hot enough for starch conversion while the final zones drop in temperature to protect micronutrient integrity. On nutritional powder processing lines, this zoning capability separates a compliant product from one that fails lab assay at the packing stage.
Screw Speed, Residence Time, and Powder Density
The interplay between screw RPM and barrel length determines how long the rice flour sits under heat and shear. A higher screw speed pushes material through faster, raising hourly output but risking incomplete cooking. Lower RPM extends residence time, producing fully gelatinised flour at a reduced throughput. For buyers running fortified infant cereal, finding the correct balance during the pre-shipment trial run prevents weeks of post-installation troubleshooting. The control system — whether PLC or MCC — must make this adjustment accessible to the line operator without requiring a process engineer on call [NEED_CITE: twin-screw extrusion residence time distribution models].
How Die Design Shapes the Final Flour
The die plate at the extruder discharge determines whether the output emerges as thin strands for easy milling into fine powder, or as expanded ribbons for a flaked or granulated format. Interchangeable die plates give the processor flexibility to switch between instant porridge flour and a coarser weaning food base on the same line. Die orifice diameter and land length together set the expansion ratio, and that expansion ratio controls bulk density — a parameter that directly affects packing weight accuracy and shelf appearance.
The Hidden Cost of Skipping the Pre-Shipment Trial
When a buyer accepts delivery without a trial run on their own raw material, the first weeks of production become an expensive experiment. I have seen a South Asian infant cereal producer spend days reconfiguring screw elements and re-mapping barrel temperatures because the supplier tested only with standard polished japonica rice while the buyer’s local supply was a mix of broken indica grains and cassava starch. The extruder itself was not at fault. The screw configuration simply had not been matched to the actual feedstock. On nutritional powder processing lines, this mismatch can delay market entry by weeks and erode buyer confidence before the first commercial batch ships [NEED_CITE: starch gelatinisation temperature differences between rice varieties].
Why Sourcing the Full Line from One Supplier Matters
Every station on a baby rice flour line — batching, extrusion, drying, milling, cooling, and packing — must pass the same throughput. When the dryer is undersized relative to the extruder, wet extrudate piles up and degrades before it enters the drying bed. When the mill cannot handle the dried output rate, the entire line slows to match the bottleneck. Sourcing the twin screw extruder for baby rice flour as part of a matched line from one builder eliminates the finger-pointing between separate vendors when capacity falls short.
- Screw configuration and die design are specified to the buyer’s actual rice variety, blend ratio, and target powder density, not copied from a generic build.
- In-house testing workshop runs the buyer’s raw material before shipment, producing a documented trial report with barrel temperature curves and screw speed settings.
- PLC or MCC control panels are wired and labelled in the language and voltage standard of the destination country before crating.
- Food-grade stainless steel contact surfaces are verified at the factory inspection stage, not assumed from a catalogue description.
- Throughput matching across batching, extrusion, drying, milling, and packing stations is calculated in the line layout proposal, not left to on-site guesswork.
Documentation & Verification
- Line layout drawing showing station-by-station throughput calculation for baby rice flour output
- Screw element arrangement record matched to the buyer’s rice flour formulation
- Factory trial run report on customer-supplied raw material with temperature and speed logs
- Electrical schematic confirming voltage, frequency, and control language before shipment
- CE declaration of conformity and ISO certificate copies included with shipping documents
- Wear parts list covering screw elements, die plates, and barrel liners with replacement intervals
Installation, Commissioning & Support
- Foundation plan provided based on the extruder motor weight and vibrating feeder load
- Dedicated power circuit sized to the main motor kW rating and barrel heater zones
- Modular barrel sections arrive separated for easier workshop entry and reassembly on site
- First production run supervised by a process engineer who sets barrel curves and screw speed
- Operator training covers die changeover, screw element inspection, and emergency stop sequences
- Spare screw elements and die plates shipped with the initial order to cover the first replacement cycle
- Preventive maintenance schedule tied to running hours with barrel liner and seal checkpoints
What to Include in Your Enquiry
To configure a nutritional powder processing line that matches your facility, share the rice variety or blend you plan to use, the target daily output in tonnes, and the particle size range required for the finished flour. Confirm the local voltage and frequency at your installation site, the preferred control language on the HMI, and whether an existing milling or packing station will be integrated. If your formulation includes cassava, millet, or legume additions, note the blend percentages so the screw configuration can be specified before the trial run.
Frequently Asked Questions
Q: Can the extruder handle rice flour blended with cassava or millet starch?
A: Yes. The twin-screw configuration and barrel temperature profile are adjusted to the specific blend ratio and gelatinisation temperature of each starch component. A pre-shipment trial on the buyer’s actual blend confirms screw speed, moisture addition, and zone temperatures before the line is dispatched.
Q: What happens if our local rice has higher moisture than standard specifications?
A: Higher feedstock moisture shifts the gelatinisation point and can cause die blockage or sticky extrudate. The pre-shipment trial run uses your raw material so that barrel temperature curves and screw element spacing are set for your actual moisture range, not a laboratory reference sample.
Q: Is the control system available in our local language and voltage standard?
A: Both PLC and MCC control options are available. The HMI language, electrical schematic, voltage, and frequency are confirmed during the specification stage so the panel matches your workshop standards before crating and shipment.
Q: How is throughput matched between the extruder and downstream drying and milling?
A: The line layout proposal includes a station-by-station capacity calculation. The dryer bed area, milling throughput, and cooler conveyor speed are all sized to the extruder output on your specific recipe, preventing bottlenecks that stall production.
Q: Do you supply spare screw elements and die plates with the first order?
A: A wear parts list is included in the documentation package, and spare screw segments, die plates, and barrel liners can be shipped with the initial order. This covers the first replacement cycle and avoids production downtime while waiting for international freight.