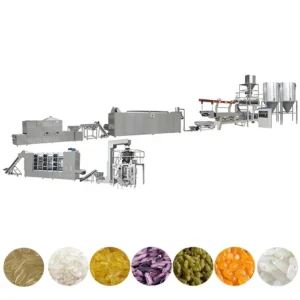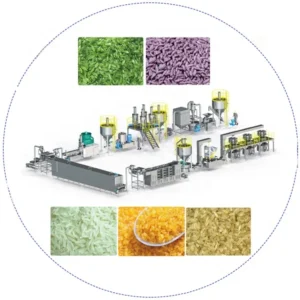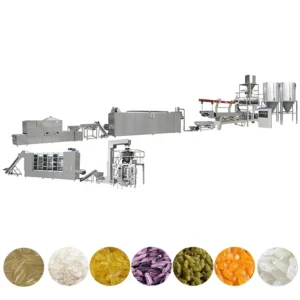
Turnkey Line Integration — every station from batching to packing is sourced under one supply contract, so the mixer, extruder, dryer, and packer are capacity-matched to your grain formulation rather than assembled from mismatched vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Nutrition Powder Processing Line |
| Output Capacity | 200–500 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Extruder Type | Twin Screw |
| Control System | Automatic PLC with touch control panel and digital interface |
| Construction Material | Food-Grade 304 Stainless Steel (contact surfaces) |
| Heat Source Options | Electric / Gas / Steam (configurable to site utilities) |
| Assembly State | Complete production line (batching through packing) |
| Standards | CE, ISO |
| Warranty | 1 year |
| After-Sales Service | Overseas engineer service available |
Application Suitability
| Application | Material or Output |
|---|---|
| Baby food nutrition powder and porridge | Rice, corn, and multi-grain blends processed into fine instant powder |
| Infant formula and fortified nutritional powder | Grain base with added micronutrients, whey, and oil fractions |
| Breakfast cereal and instant porridge production | Oats, wheat, barley, and bean formulations for hot-cereal formats |
| Fortified food and nutrition programme supply | Diverse grain and legume blends meeting institutional specification sheets |
Why Nominal Capacity Figures Mislead Nutrition Powder Buyers
A line rated at 500 kg/h on standard rice flour may deliver half that when your formulation includes high-fat or high-whey fractions.
I have spent years flying into Middle Eastern plants to watch nutrition powder processing line full equipment range installations stall at the extruder station. The buyer approved a line quoted on clean starch, but the actual recipe — loaded with milk powder, vegetable oil, and micronutrient premix — caused the twin screws to slip. Throughput dropped, the dryer ran half-empty, and the packing station sat idle. The entire line was bottlenecked by one station that was never tested on the real formulation. [NEED_CITE: raw material formulation impact on twin-screw extrusion throughput]
How Each Station Connects Across the Nutrition Powder Line
A nutrition powder processing line full equipment range is only as reliable as its weakest throughput match. The mixer must deliver a homogeneous blend at a rate the extruder can accept continuously; the extruder must gelatinise starch and condition moisture so the downstream dryer receives a consistent feed; the dryer must reduce moisture to a level the milling or flaking stage can handle without clumping. When any station is oversized or undersized relative to its neighbour, the line oscillates between starvation and surge, degrading powder quality and wasting energy.
Screw Configuration and Raw Material Behaviour
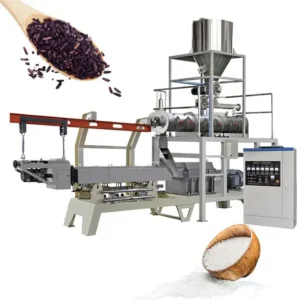
The twin-screw extruder is where the formulation either works or fails. Rice-dominant blends gelatinise predictably and expand well under standard screw profiles. Introduce higher proportions of legume flour, oil, or dairy solids and the material behaves differently inside the barrel — lubrication increases, residence time requirements shift, and die pressure changes. Matching screw element geometry, barrel temperature zones, and die aperture to the specific grain blend is the engineering work that determines whether the line runs at its intended rate or limps through commissioning. [NEED_CITE: twin-screw extrusion screw configuration for multi-grain formulations]
Reading the Specs That Actually Matter
The PLC touch-panel control system matters because nutrition powder formulations change between production runs — operators adjust barrel temperatures, screw speed, and feed rate from recipe to recipe, and a digital interface with stored parameters keeps batch consistency tight. Food-grade 304 stainless steel on all contact surfaces is not optional when producing infant and baby food powders; cleaning protocols demand smooth, corrosion-resistant surfaces that withstand caustic wash-downs. The heat source choice — electric, gas, or steam — dictates the dryer design and the utility infrastructure the buyer must prepare on-site before installation begins. Selecting the wrong option delays commissioning by weeks while ductwork or boiler connections are retrofitted.
What Happens When Line Stations Are Sourced Separately
Buyers who assemble a nutrition powder line from multiple vendors often discover during commissioning that the mixer output does not align with the extruder infeed rate, or the dryer belt width cannot handle the extrudate volume. I have seen drying sections added as afterthoughts, with conveyors jury-rigged between stations that were never designed to interface. The result is chronic downtime at transfer points, product loss, and a control architecture where each station runs on its own logic without coordinated start-stop sequencing. [NEED_CITE: throughput mismatch risks in multi-vendor food processing lines]
Why Buyers Consolidate With One Line Supplier
Every station — mixing, extrusion, drying, flavouring, cooling, packing — is engineered as a single system, so belt widths, conveyor speeds, and bin volumes are calculated against one throughput target. Screw and die configurations are specified to the buyer’s actual grain blend and target powder particle size, not copied from a generic build. An in-house testing workshop runs the buyer’s raw material before shipment, producing a trial run report that confirms capacity and texture. Electrical schematics are confirmed against the target market’s voltage and frequency before the control panel is wired. Spare wear parts — screws, dies, seals — are documented and available so the first replacement does not become an emergency.
Documentation & Verification
- Line layout and capacity calculation confirming throughput across every station
- Screw and die configuration record matched to your grain formulation
- Electrical schematic with voltage and frequency confirmed for your market
- Trial run report on your actual raw material before shipment
- CE declaration of conformity and ISO certificate
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation plan and floor-space drawing provided for your plant layout before equipment arrival
- Electrical supply specification detailing voltage, frequency, and dedicated circuit requirements for the PLC panel
- Line arrives in shipping sections with labelled connections for on-site reassembly
- Overseas engineer available for first-start parameter tuning and recipe validation
- Operator training covers PLC recipe storage, barrel temperature profiles, and screw speed adjustment
- Wear parts list with lead times for replacement screws, dies, and barrel liners
What to Include in Your Enquiry
Share your target formulation — grain types, oil and dairy fractions, micronutrient additions — along with the powder specification you need to meet, whether that is particle size, bulk density, or instant solubility. Confirm your site voltage and frequency, available heat source, and the daily or shift-based output you are planning for. If you have existing upstream or downstream equipment that the new line must integrate with, include those details so the layout accounts for the connection points.
Frequently Asked Questions
Q: What stations are included in the nutrition powder processing line, and how is throughput matched?
A: The line covers mixing, extrusion, drying, milling or flaking, cooling, and packing. Each station is sized against a single throughput target calculated from your formulation, so no section starves or surges. The layout document confirms capacity at every transfer point before production begins.
Q: Which grain formulations can the twin-screw extruder handle?
A: Rice, corn, oats, wheat, beans, and multi-grain blends are all processed. The screw configuration and barrel temperature profile are adjusted to each formulation’s starch, protein, and fat content. A trial run on your specific blend is conducted before the line ships.
Q: What heat source options are available for the dryer?
A: Electric, gas, and steam options are configurable. The choice affects utility planning — gas requires burner infrastructure and ventilation, steam needs a boiler, and electric demands sufficient transformer capacity. Your site conditions determine which option fits.
Q: Is a trial run performed on my raw material before shipment?
A: Yes. Your raw material is run through the extruder in the in-house testing workshop. The trial report documents throughput, product texture, moisture content, and screw configuration, giving you confirmed parameters before installation starts.
Q: What spare wear parts are included, and how are replacements handled?
A: Initial spare screws, dies, and seals ship with the line. The wear parts list specifies part numbers and material grades. Replacement orders are fulfilled against documented lead times so maintenance can be planned rather than reactive.