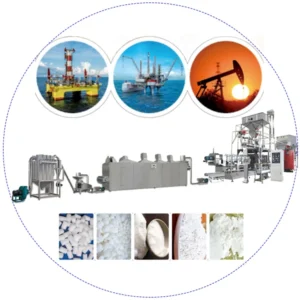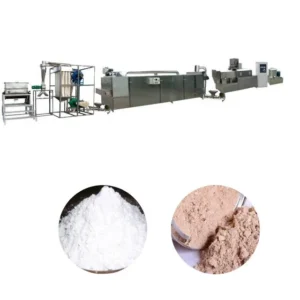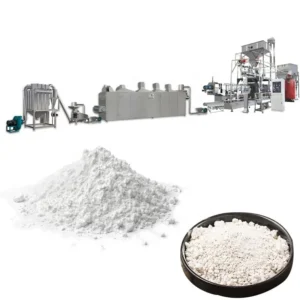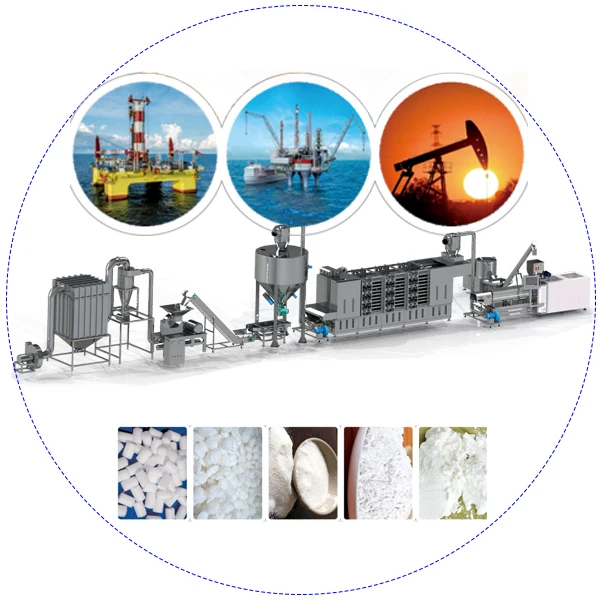
Integrated Line Stations — Every piece of equipment from batching through extrusion to grinding is sourced under one supplier, ensuring throughput alignment rather than assembling mismatched units from separate vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Modified Starch Processing Production Line (Twin Screw Extrusion) |
| Main Extruder | Twin Screw Configuration (MT70 class reference) |
| Power Range | 45–200 kW |
| Capacity | 100–1500 kg/h (basis not stated in source — confirm raw material type, moisture content, modification degree) |
| Machine Weight | 1000–5000 kg (source value — verify against manufacturer catalog) |
| Voltage | 220–440V, tri-phase (frequency to be confirmed) |
| Contact Material | Food-grade 304 stainless steel (product contact zones); PVC on select conveyors |
| Control System | PLC/MCC presence to be confirmed |
| Grinder Configuration | Pulse grinder with speed-controlled auger feeder, rotor, stator, classifier, cyclone discharge, and filter pocket dust collector |
| Cooling Conveyor | Low-power fan with wind-knife blowing mouth, ambient air temperature drying |
| Fuel Options (for dryer integration) | Gas, diesel, electricity, or steam |
| Standards | CE certified, ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Food-grade modified starch | Corn starch, wheat flour, and additive blends for sauces, bakery products, and instant foods |
| Industrial starch for oil drilling | Modified starch formulations engineered for drilling fluid viscosity and thermal stability |
| Papermaking starch | Cationic and oxidized starch variants for paper surface sizing and coating |
| Fortified nutrition powders | Blends of rice flour, soybean flour, potato starch, and grain flours with vitamin and mineral premixes |
| Pregelatinized starch | Pre-cooked starch for cold-water solubility in convenience food and industrial applications |
What "500 kg/h Modified Starch" Actually Depends On
Capacity figures mean nothing without naming the raw material and its moisture content.
I once configured a modified starch processing line full equipment range for a plant that sent us standard corn starch samples. The trial ran clean, the line shipped, and then we learned on-site they were running waxy corn — a completely different gelatinization temperature window. The screw combination had to be rearranged from scratch, and it took nearly two weeks to recover stable throughput. That is the kind of mismatch a spec sheet will never warn you about. When a supplier quotes a capacity number, the real question is always: on whose material, at what moisture, and targeting what degree of modification? [NEED_CITE: gelatinization temperature variance across starch types]
How Extruder Configuration Shapes the Starch Molecule
The twin screw extruder sits at the heart of any modified starch processing line full equipment range because the mechanical and thermal energy it delivers determines the degree of starch conversion. Screw configuration — the arrangement of conveying elements, kneading blocks, and reverse screws — controls residence time and shear intensity inside the barrel. A setup optimized for pregelatinization will differ markedly from one targeting dextrinization or cross-linking, even on the same base extruder. Barrel temperature profiling across multiple heating zones allows operators to manage the gelatinization front precisely, avoiding both under-processed starch that fails viscosity tests and over-processed material that degrades.
Why the Grinder and Cooling Conveyor Are Not Afterthoughts
After extrusion, the extrudate must be cooled before grinding to prevent moisture condensation and particle clumping downstream. The cooling conveyor on this line uses ambient-temperature wind-knife drying rather than heated air, which preserves the functional properties the extruder just created. The pulse grinder then handles particle size reduction with a speed-controlled auger feeder that meters material into the rotor-stator chamber at a consistent rate. Its integrated classifier and cyclone dust collection are not optional extras — they determine whether your final powder meets the mesh size specification your customer requires, or whether you lose product to uncontrolled dust. [NEED_CITE: particle size distribution standards for modified starch grades]
Reading the Specifications That Matter
The power range of 45–200 kW reflects the spread across different extruder sizes within this line family, and selecting the right point within that range depends on your target throughput and the specific modification reaction you need to drive. Higher modification degrees — deeper molecular restructuring — demand more mechanical energy input, which translates to higher motor load. Voltage specification at 220–440V tri-phase covers most export markets, but frequency must be locked to your local grid before production begins; running a 50 Hz motor on 60 Hz power shifts every speed-dependent parameter in the process. The food-grade 304 stainless steel contact surfaces are essential for starch lines because starch slurries are mildly corrosive and any iron contamination discolors the final product. The multi-fuel dryer compatibility — gas, diesel, electricity, steam — lets you match the heat source to whatever utility infrastructure your plant already has in place.
When Line Stations Are Sized Independently
An extruder running at its rated output means nothing if the grinder downstream can only handle a fraction of that flow. Material backs up, operators manually throttle the extruder, and the entire modified starch processing line full equipment range runs below the capacity you paid for. I have seen starch plants where the cooling conveyor was too short for the extruder’s discharge rate, meaning warm extrudate entered the grinder and produced gummy particles that clogged the classifier. These bottlenecks are invisible on a quote that lists machines individually. The only defense is a line layout that shows throughput calculations at every station, matched to your specific material characteristics. [NEED_CITE: throughput matching methodology for extrusion-based processing lines]
Why Sourcing Everything Under One Supplier Matters Here
The twin screw extruder, cooling conveyor, pulse grinder, and all intermediate conveying are designed and supplied as a coordinated system, so each station’s throughput is calculated against the next rather than pulled from a generic catalog. Screw configuration and die design are specified to your raw material — whether that is standard corn starch, waxy corn, potato starch, or a blended formulation — and documented before production begins. The in-house testing workshop runs your actual material before the line ships, catching gelatinization mismatches and particle size issues at the factory instead of on your floor. Pre-sales consultation covers line layout and utility planning, while on-site installation includes commissioning and operator training so the crew understands how screw speed, barrel temperature, and feeder rate interact. Documentation includes the trial run report on your specific formulation, not a generic test on a reference starch.
Documentation & Verification
- Line layout showing throughput matching from extruder through grinder to packing
- Screw and die configuration record matched to your specific starch type
- Electrical schematic with voltage and frequency locked to your local grid
- Trial run report on your raw material conducted before shipment
- CE declaration of conformity and ISO certificate included with delivery
- Wear parts list covering screws, dies, and grinder rotor-stator components
Installation, Commissioning & Support
- Floor plan and utility connection points mapped to the 220–440V tri-phase supply and your chosen fuel source for dryer integration
- Dedicated electrical circuit sizing based on the 45–200 kW power envelope of your selected extruder model
- Grinder classifier calibration and cyclone dust collector commissioning performed on-site during initial startup
- Screw configuration validation using your raw material during the commissioning phase to confirm target modification degree
- Operator training covering barrel temperature profiling, auger feeder speed adjustment, and grinder classifier settings
- Spare screws, dies, and grinder wear parts supplied with initial delivery and available for reorder
What We Need to Configure Your Line Accurately
To move from a general inquiry to a specific line proposal, we need your base starch type and source — corn, wheat, potato, rice, or a blend — along with the modification you are targeting. Your intended throughput in kg/h, the moisture content of your incoming material, and your final powder mesh size requirement all feed directly into extruder sizing and grinder selection. Share your plant’s available voltage and frequency, the fuel source you prefer for drying, and the floor space you have allocated so the layout can be drawn to scale.
Frequently Asked Questions
Q: What stations are included in the full modified starch line and how is throughput matched?
A: The line covers the twin screw extruder, cooling conveyor, pulse grinder with cyclone dust collection, and all intermediate conveying. Each station is sized against the next based on your raw material and target capacity so that no single unit bottlenecks the entire modified starch processing line full equipment range. Throughput calculations are documented in the line layout before production starts.
Q: What raw materials can the twin screw extruder handle for starch modification?
A: The extruder processes corn starch, wheat flour, rice flour, soybean flour, potato starch, and blended grain formulations. Screw configuration and barrel temperature profiles are adjusted for each material’s gelatinization behavior. A trial run on your specific raw material is conducted in the testing workshop before the line ships to confirm the setup.
Q: How is voltage, frequency, and fuel type confirmed for my market?
A: Voltage is configurable across the 220–440V tri-phase range, and frequency must be confirmed to match your local grid standard before electrical assembly begins. For dryer integration, fuel options include gas, diesel, electricity, or steam — selected based on your plant’s existing utility infrastructure. The electrical schematic is included in the documentation package.
Q: Can a trial run be done on my specific starch formulation before shipment?
A: Yes. The in-house testing workshop runs your actual raw material on the configured extruder and grinder setup before the line is packed. The trial run report documents throughput, product quality, screw configuration, and operating parameters so you know the line will perform on your material when it arrives.
Q: What spare wear parts are available and how are they supplied?
A: Wear parts include extruder screws, die plates, and grinder rotor-stator assemblies. A complete wear parts list is provided with the initial delivery, and replacement components are manufactured to the same specification. Keeping a first replacement set on hand avoids downtime when routine wear reaches its service limit.