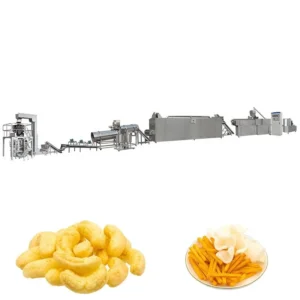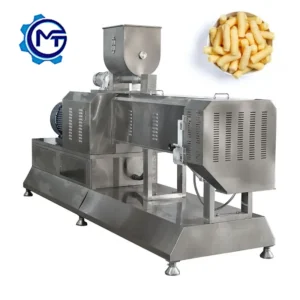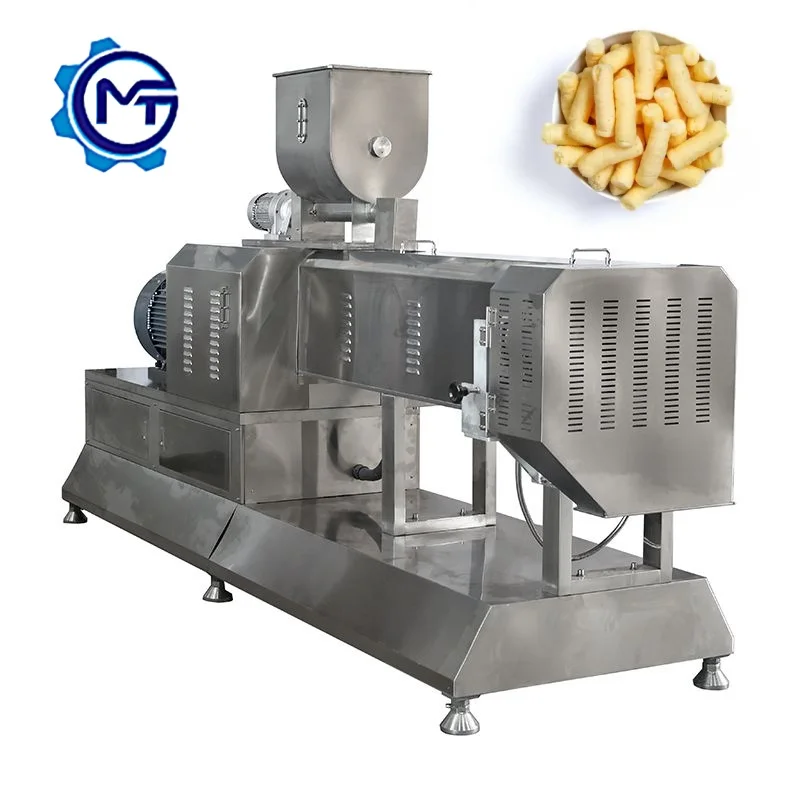
Complete Line Integration — Every station from mixing to packing is throughput-matched under one supplier, preventing bottlenecks that occur when assembling from separate vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 |
| Product Type | Twin Screw Puffed Snack Extrusion Line |
| Installed Power | 130 kW |
| Real Consumption | 95 kW |
| Capacity | 120–150 kg/h (basis not stated in source — confirm raw material, moisture, and product shape) |
| Screw Type | Twin Screw |
| Extruder Series Options | MT65 / MT70 / MT85 / MT100 |
| Control System | Frequency speed controlling system |
| Lubrication | Automatic lubricating and cooling |
| Dryer Heating Source Options | Electric / Steam / Gas |
| Flavoring System | Double drum flavoring line with sugar melting and spraying nozzle |
| Packing Machine | Automatic weighing, sealing, marking, coding |
| Raw Materials | Corn, rice, wheat, oat, barley flour |
| Product Shapes | Cheese ball, ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Core Filling Option | Available with core filling machine and cutting machine addition |
| Assembly State | Complete line from batching to packing |
| Warranty | 1 year free warranty |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Puffed snack production | Corn flour, rice flour, wheat flour extruded into balls, rings, sticks, loops |
| Core-filled snack production | Filled extrudates with cream or jam centers using dedicated cutting station |
| Breakfast cereal formats | Oat and barley flour shaped into stars, wheels, and flower shapes |
| Snack format expansion | Die changes on the same extruder to switch between cheese ball, tube, and fruit loop profiles |
| Multi-grain snack lines | Blended grain flours processed through twin screw extruder with matched downstream drying |
Why Matching Dryer Capacity to Extruder Output Matters More Than You Think
A Puffed Snack Extrusion Line Full Equipment Range that is not balanced across every station will never hold its nameplate output in real production.
I learned this the hard way on a line installation in South America. The extruder was running smoothly at its rated capacity, but the dryer could only handle part of that volume. Product piled up on the cooling conveyor, moisture readings were all over the place, and the flavoring drum received unevenly dried pieces that rejected seasoning coating. The buyer had purchased each station from a different vendor, and nobody had done the math on throughput matching. [NEED_CITE: consequences of throughput mismatch in multi-station food processing lines]
When you survey equipment for a puffed snack line, the extruder gets most of the attention. But the dryer, flavoring drum, and packing station each have their own cycle times and capacity ceilings. If any one of them falls short, the entire line slows down to match the weakest link.
How Station-to-Station Throughput Matching Works
The Puffed Snack Extrusion Line Full Equipment Range approach treats every station as a connected system rather than isolated machines. The mixer must deliver batched material at a rate that keeps the extruder hopper consistently fed without overflow. The extruder pushes product into the dryer at a moisture level and volume that the dryer’s residence time can handle. Each station’s nominal capacity is calculated against the actual product profile, not a generic benchmark.
Why Twin Screw Configuration Affects Every Downstream Station
The twin screw design generates higher shear and more uniform gelatinisation than single screw alternatives, which directly influences the moisture content and density of the extrudate entering the dryer. If the dryer was specified for single screw output characteristics, it will struggle with the different moisture profile. This is why the Puffed Snack Extrusion Line Full Equipment Range must be configured as a complete system, with screw speed, barrel temperature, and die selection all factored into downstream station sizing. [NEED_CITE: twin screw extrusion shear and gelatinisation effects on downstream drying requirements]
Reading the Specs That Actually Matter for Snack Production
The MT65 carries 130 kW installed power with 95 kW real consumption, which reflects the actual thermal and mechanical load during continuous extrusion rather than peak startup draw. The frequency speed controlling system allows operators to adjust screw RPM in response to raw material variation — critical when switching between corn flour and rice flour, which demand different shear profiles. The automatic lubricating and cooling system maintains barrel temperature consistency across long production runs, preventing the gradual thermal drift that causes expansion inconsistency. The double drum flavoring line with sugar melting and spraying nozzle ensures coating uniformity even on complex shapes like fruit loops and stars, where a single drum would leave uncoated surfaces in the recesses.
What Happens When You Ignore the Utility Planning Stage
Buyers often finalize equipment selection before confirming local utility conditions. The dryer on this line offers electric, steam, or gas heating options, and choosing the wrong one for your facility’s available infrastructure causes delays that ripple through the entire commissioning schedule. A gas-heated dryer connected to an undersupply line will never reach temperature setpoint, producing under-dried snacks that fail shelf life tests. Electrical frequency mismatches between the motor ratings and local grid supply can cause overheating and premature bearing failure within the first production week. [NEED_CITE: industrial equipment commissioning failures caused by utility mismatches]
Why Buyers Choose This Configuration for Snack Line Projects
The complete line from batching through packing is supplied under one responsibility, so throughput calculations are done across every station rather than leaving gaps between vendor scopes. Screw configuration and die design are specified to the buyer’s actual raw material and target product shape, not copied from a generic build. An in-house testing workshop allows trial runs on customer-supplied raw material before shipment, catching starch content and moisture issues that would otherwise surface during on-site commissioning. The frequency speed controlling system and automatic lubrication are standard across the MT65 series, reducing the number of variables operators must manage during production changeovers. Documentation includes line layout and capacity calculation showing how each station’s throughput was matched, giving buyers a verifiable reference before the equipment leaves the factory.
Documentation & Verification
- Line layout showing throughput matching across mixing, extrusion, drying, flavoring, and packing stations
- Machine specification sheet for each station with utility and footprint requirements
- Screw and die configuration record matched to your target snack shape and raw material
- Electrical schematic with voltage and frequency confirmation for your local grid supply
- Trial run report produced on your raw material in the testing workshop before shipment
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
Installation, Commissioning & Support
- Foundation and floor space plan based on the full line footprint including dryer and flavoring drum clearance
- Electrical supply verification against the 130 kW installed power requirement and local voltage standard
- Assembly sequence for the twin screw extruder, dryer, and double drum flavoring line on site
- First-run parameter setting for screw speed, barrel zones, and dryer temperature on your specific flour blend
- Operator training covering the frequency speed controlling system and automatic lubrication monitoring
- Wear parts list for screws, dies, and dryer screens with recommended replacement intervals
What We Need to Configure Your Line Accurately
To prepare a line layout and capacity calculation that reflects your actual production conditions, we need your target product shapes, the specific flour or blend you plan to run, and your daily output target. Please also share your facility’s available voltage and frequency, preferred dryer heating source, and whether core filling capability is required. If you can send a sample of your raw material, we can run a trial in the testing workshop and include the results with the proposal.
Frequently Asked Questions
Q: How is throughput matched across every station in the full line?
A: Each station’s capacity is calculated based on the extruder’s actual output on your raw material, not a generic rating. The dryer residence time, flavoring drum volume, and packing speed are all sized to handle the extrudate flow without accumulation or starvation at any transfer point.
Q: What supporting stations are included beyond the extruder?
A: The line includes a mixing and batching system, conveying equipment, dryer with selectable heating source, double drum flavoring line with sugar melting and spraying nozzle, cooling conveyor, and automatic packing machine with weighing, sealing, and coding functions.
Q: How do I select the right dryer heating source for my facility?
A: The choice between electric, steam, or gas depends on your local utility availability and cost structure. Gas heating suits facilities with existing gas infrastructure, steam works where boiler capacity is available, and electric is practical for smaller installations or regions with stable grid supply.
Q: What product shapes can I produce with die changes on the same extruder?
A: The MT65 twin screw extruder supports cheese ball, tube, stick, ring, fruit loop, star, wheel, flower, and heart shapes through die changes. Each shape requires a matched screw configuration and specific barrel temperature profile to achieve correct expansion and density.
Q: How does core filling capability integrate into the base line?
A: Core filling is added by integrating a filling machine and dedicated cutting station into the extrusion and drying sequence. The base line configuration remains unchanged, and the filling module can be activated or bypassed depending on whether the current production run requires filled or solid snack formats.