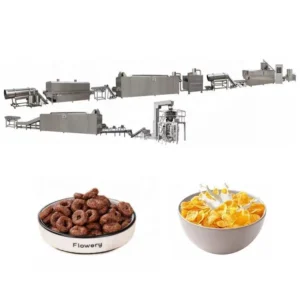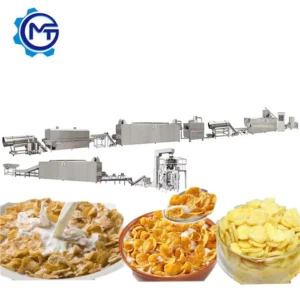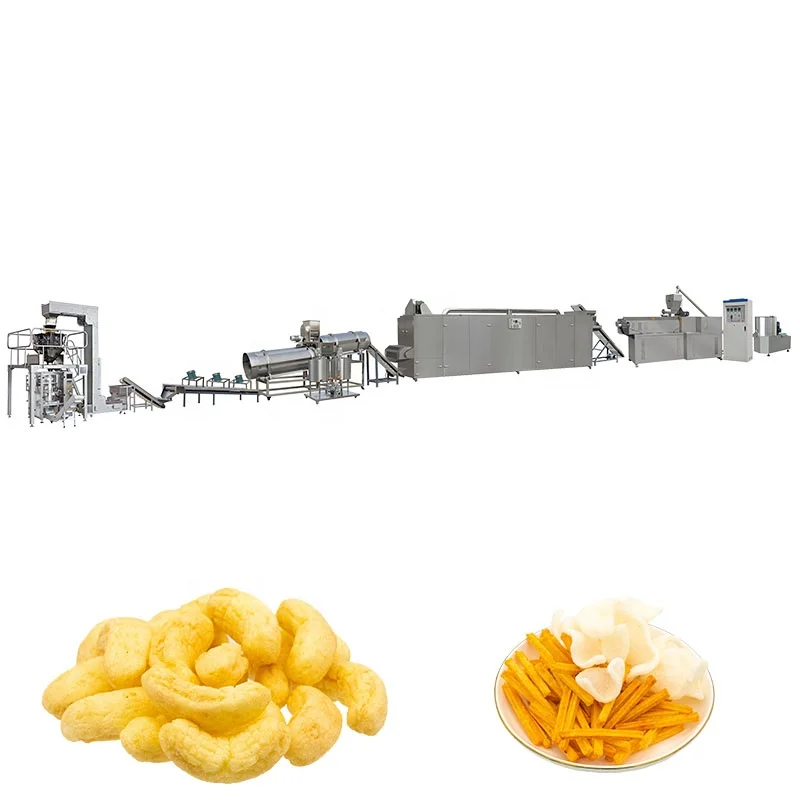
Throughput-Matched Stations — Every mixer, extruder, flaker, dryer, roaster and coater in this corn flakes line is sized to the same throughput target so no single unit bottlenecks the rest of the system.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Making Machine and Production Line |
| Extruder Models Available | MT70 / MT85 / MT75 |
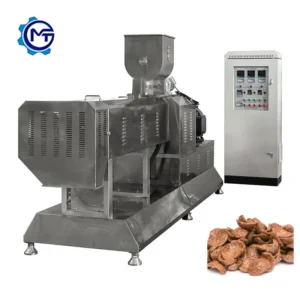
| Extruder Type | Twin Screw |
| Installed Power | MT70 — 160 kW; MT85 — 190 kW; MT75 — 210 kW |
| Power Consumption | MT70 — 120 kW; MT85 — 140 kW; MT75 — 150 kW |
| Output Capacity | MT70 — 150–200 kg/h (basis to be confirmed); MT85 — 300–400 kg/h (basis to be confirmed); MT75 — 300–500 kg/h (basis to be confirmed) |
| Overall Dimensions (L × W × H) | MT70 — 41 × 1.5 × 2.2 m; MT85 — 43 × 1.5 × 3.2 m; MT75 — 45 × 1.5 × 3.5 m |
| Control System | PLC control system with MCC integration |
| Flaking Machinery | Hydraulic double-roller system, independent dual motors, infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air roasting with vibrating pan, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melter, elevator, coating drum, spraying nozzle |
| Screw Material | Wear-resistant alloy, special processing technology |
| Lubrication | Automatic lubricating and cooling function |
| Line Stations | Mixing, Extruding, Flaking, Drying, Hot Air Roasting, Sugar Spraying/Coating, Cooling, Packing |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Final Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (by adjusting extruder mould) |
| Voltage & Frequency | Customizable to local requirements |
| Layout | Customizable to factory size |
| Standards | CE (since 2014); ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Degerminated corn grits |
| Sugar-coated corn flakes | Corn base with sugar or honey glaze |
| Multi-grain breakfast cereals | Rice, wheat, oat, and barley blends |
| Shaped cereal variants | Ball, ring, fruit loop, star, and wheel profiles via die change |
| Fortified breakfast cereal lines | Grain blends with added nutritional premix |
Why Nameplate Capacity Figures Can Mislead Your Corn Flakes Line
A quoted output number means nothing unless the dryer, roaster and coater downstream can keep pace with the extruder.
When I worked with a processor setting up a breakfast cereal line a couple of years back, they spec’d their twin-screw extruder to a comfortable hourly figure but sized the dryer for a lower throughput. The extruder ran fine during the first week of trials, then wet flakes piled up ahead of the dryer entry and the whole breakfast cereal corn flakes machine full equipment range had to be throttled back. The line’s real output dropped to roughly two-thirds of what the purchase order promised. [NEED_CITE: throughput matching between extrusion and drying stations in cereal production]
These mismatches happen because buyers compare extruder models on motor power and screw diameter while assuming the rest of the line will simply "fit." The flaking rollers, drying belt length, roasting oven volume and coating drum diameter each have their own throughput ceiling, and the lowest ceiling in the chain is what you actually produce at.
Station-by-Station Sizing Across the Complete Corn Flakes Line
Every unit in the breakfast cereal corn flakes machine full equipment range is calculated against the same target throughput before the layout is finalized. The mixer batch size aligns with extruder feed rate, the flaking roller width matches the dough sheet volume, and the dryer belt area is chosen so that residence time delivers the correct moisture reduction without slowing the line.
This approach eliminates the silent capacity ceiling that appears when stations are sourced from separate vendors who each rate their equipment independently. One supplier’s dryer may be rated for a given moisture removal at a specific air temperature, but if the incoming flake load is heavier than expected, the actual drying time extends and throughput suffers.
How Flaking and Roasting Hardware Affects Final Flake Quality
The flaking machinery uses a hydraulic double-roller system with independent dual motors and infrared sensor temperature control. Hydraulic pressure keeps roller gap consistent across the full width, which is what gives you uniform flake thickness rather than thick edges and thin centers. Independent motor drives on each roller let the operator fine-tune surface speed differential, a factor that influences how cleanly the dough sheet releases. [NEED_CITE: hydraulic roller pressure and flake thickness uniformity in cereal processing]
Downstream, the hot air roasting oven relies on a conciliation burner and two separate circulating fans to maintain even temperature zones inside the chamber. Cyclone dust removal captures fine particles before they can settle on the flakes or accumulate in the ductwork, which matters for both product appearance and sanitation compliance.
Reading the Specs That Actually Matter for Flake Output
The twin-screw extruder’s installed power and screw configuration together determine how much shear energy goes into the dough, which directly controls starch gelatinization. Under-gelatinized dough will not flake properly and produces a dense, hard finished flake. The MT75 model’s higher installed power suits coarser corn grits that need longer residence time and more mechanical work to reach full cook.
Flaking roller diameter and hydraulic pressure range define the minimum achievable flake thickness. Thinner flakes toast faster in the roasting oven and deliver a crisper bite, but if the dough is under-cooked coming out of the extruder, thin flakes shatter during conveying. The automatic lubricating and cooling system on the extruder gearbox matters here because continuous operation at high torque generates significant heat, and oil temperature stability keeps screw speed and output consistent over a full shift.
Coating drum volume and spray nozzle arrangement must match the roasted flake flow rate. If the drum is too small, flakes spend insufficient time tumbling and the sugar or honey coating ends up uneven, which customers notice immediately in the bowl.
The Hidden Cost of Undersized Downstream Stations
Processors who focus their budget on a large extruder but accept a smaller dryer or roaster often discover the imbalance only after installation. The extruder reaches its nameplate output during short runs, but once the dryer belt is fully loaded, moisture levels at the exit climb and flakes go into the roaster too wet. The roaster then has to run slower, and the coating drum receives flakes at an inconsistent temperature. [NEED_CITE: downstream bottleneck effects on cereal line actual output]
The result is a line that technically works but never reaches the throughput figure the buyer used to calculate payback. Spare parts wear faster because operators push individual stations beyond their intended duty cycle, and unplanned stoppages for cleaning or adjustment eat into available production hours.
Why Sourcing the Full Equipment Range from One Manufacturer Matters
Every station in this breakfast cereal corn flakes machine full equipment range is engineered, manufactured, and tested under one roof, which means throughput calculations use real data from adjacent units rather than generic catalog figures. Screw configuration and die design are specified to your raw material blend and target flake density before the extruder enters production.
An in-house machine testing workshop runs trial production on your actual corn, rice, or barley blend before shipment, so product development begins at the factory rather than on your floor after installation. The PLC and MCC control system is programmed with the correct voltage, frequency, and operator language for your facility, reducing commissioning delays. Pre-sales consultation covers line layout and utility planning, and on-site installation through operator training and ongoing maintenance support are handled by the same engineering team.
Documentation & Verification
- Line layout and capacity calculation showing matched throughput at every station
- Screw and die configuration record specific to your grain blend and flake target
- Electrical schematic with confirmed voltage and frequency for your plant supply
- Trial run report on your raw material produced in the in-house testing workshop
- CE declaration of conformity and ISO certificate for export compliance
- Operation and maintenance manual with wear parts list for screws, dies, and rollers
Installation, Commissioning & Support
- Foundation layout provided per overall dimensions up to 45 m line length, including anchor bolt plan
- Dedicated electrical circuits sized to installed power up to 210 kW per extruder model
- Line arrives in modular sections for staged assembly inside your existing building footprint
- PLC and MCC control system calibrated on-site with confirmed voltage and language settings
- Operator training covers screw configuration changes for switching between corn, rice, and oat recipes
- Wear parts list supplied at delivery covering screws, dies, flaking rollers, and spray nozzles
- Scheduled maintenance intervals documented for automatic lubrication system and dryer burner
What to Prepare Before Requesting a Quotation
Send your raw material specification including grain type, particle size distribution, and typical moisture content so the screw configuration can be matched before the proposal stage. Share your daily production target and available factory floor dimensions including ceiling height, because the roasting oven and dryer footprint vary with capacity. Confirm your local voltage, frequency, and preferred control language to avoid rewiring or reprogramming after delivery. If you are integrating this line with existing upstream storage or downstream packing equipment, provide the interface points so the layout accounts for conveyors and transfer chutes.
Frequently Asked Questions
Q: How is each station’s capacity matched so the extruder output is not bottlenecked downstream?
A: The line layout and capacity calculation document shows the throughput target at every station, from mixer batch size through extruder feed rate, flaker roller width, dryer belt area, roaster chamber volume, and coating drum diameter. Each unit is sized against the same figure using actual performance data from adjacent stations rather than generic catalog ratings.
Q: What raw materials beyond corn can this line process?
A: The twin-screw extruder handles rice, wheat, oat, and barley powder in addition to corn grits. Screw configuration and die design are adjusted for each material’s starch content, particle size, and gelatinization temperature. The testing workshop runs trials on your specific blend before the line ships.
Q: Which heating source is recommended for the dryer and roaster?
A: The dryer supports both gas and electric heating, and the choice depends on your local utility cost and available infrastructure. Gas heating typically suits larger lines where operating cost per kilogram matters more, while electric heating offers simpler installation in facilities without gas supply. The roaster uses hot air circulation with a conciliation burner.
Q: How does the PLC and MCC control system integrate across all stations?
A: The PLC and MCC system covers extruder speed, flaker pressure, dryer temperature, roaster airflow, and coating drum rotation from a single interface. Operator language is configured to your requirement before shipment, and the electrical schematic is matched to your plant voltage and frequency to prevent commissioning delays.
Q: What spare wear parts should be ordered with the initial line?
A: The recommended first-order spares include twin-screw elements, extrusion dies, flaking roller surfaces, and coating spray nozzles. A wear parts list is provided with the operation manual so you can plan replacements before the first scheduled changeover, avoiding unplanned downtime when consumables reach end of life.