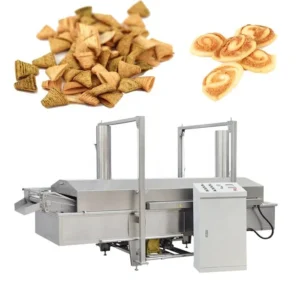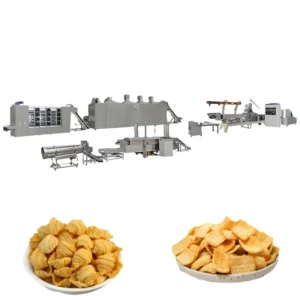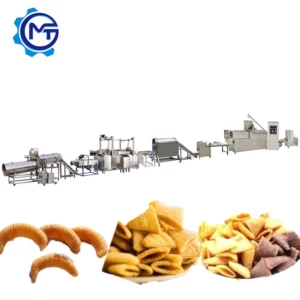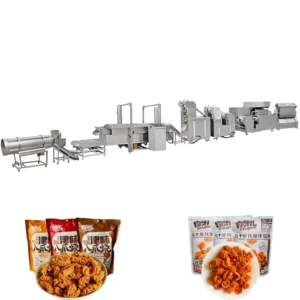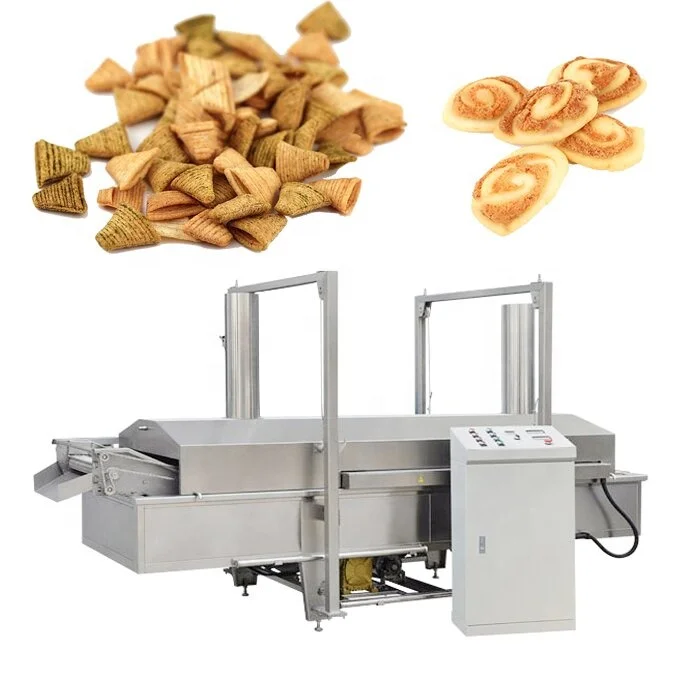
Matched Throughput Across All Stations — every component from the twin-screw extruder through the fryer and double-drum flavoring system is sized to the same capacity target, preventing mid-line bottlenecks that stall output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruder for Puffed Snack & Nacho Chips Production Line |
| Model Options | MT65 / MT70 / MT70c / MT75 |
| Screw Type | Twin Screw |
| Screw Material | Alloy 38CrMoAl, nitriding process |
| Main Motor Brand | Siemens |
| Rated Power (Main Motor) | 22 kW (MT65) / 30 kW (MT70) / 45 kW (MT70c) / 55 kW (MT75) |
| Real Power Consumption | 22 kW (MT65) / 30 kW (MT70) / 55 kW (MT70c) / 55 kW (MT75) |
| Output Capacity | 100–150 kg/h (MT65) / 150–200 kg/h (MT70) / 200–250 kg/h (MT70c) / 200–300 kg/h (MT75) (basis not stated in source — confirm raw material formulation, moisture content, target product density) |
| Feeding System | Food-grade stainless steel twin screw feeder with speed-adjusted converter |
| Control System | Speed-adjusted converter on feeding, extrusion, and cutting systems |
| Gearbox | Automatic lubrication function |
| Cutting System | Rotary cutting knife fixed in die head seat, V-belt drive |
| Cooling | Increased radiator on driving part for forced cooling |
| Die Mechanism | High pressure double crank mechanism for opening/closing |
| Line Stations | Extruder → Shaper → Hot air texture forming → Fryer (electric / diesel / gas) → Double drums flavoring system |
| Overall Dimensions (L×W×H) | 22000×1200×2200 mm (MT65) / 25000×1500×2200 mm (MT70) / 30000×3500×4300 mm (MT70c) / 33000×3500×4300 mm (MT75) |
| Certification | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Nacho chips production | Corn flour blend, extruded and shaped before frying |
| Tortilla chips line | Corn-based dough, hot-air texture formed then fried |
| Corn puff snacks | Corn flour or corn grits, puffed via twin-screw extrusion |
| Doritos-style savory snacks | Multi-grain flour blends, shaped, fried, and seasoned |
| Fried pellet snacks | Starch-based pellets, fried to target expansion and crispness |
What Happens When Frying Line Stations Are Sourced Separately
A mismatched fryer or flavoring drum turns a rated extruder into an expensive bottleneck.
I have watched snack producers invest heavily in a high-capacity extruder, only to discover that the downstream fryer cannot keep pace with the dough output. The extruder slows, product sits in the hot-air texture former too long, moisture drops below spec, and the final chip density shifts outside what the market expects. The frying chips making machine full equipment range is only as strong as its weakest station [NEED_CITE: throughput matching principles in continuous food processing lines].
This is not a theoretical problem. When stations come from separate vendors, each supplier optimizes for their own machine, and no one owns the line-wide throughput calculation. The result is a production floor where operators constantly adjust feed rates to compensate for equipment that was never designed to run together.
Station Synchronization Across the Extrusion-to-Frying Sequence
The frying chips making machine line covered here runs from the twin-screw extruder through a shaper, hot-air texture forming unit, continuous fryer, and into a double-drum flavoring system. Each station carries a speed-adjusted converter, which means the operator can fine-tune the feed rate at every transition point rather than relying on fixed-speed transfers that force product accumulation or starvation.
Energy Source Flexibility in the Frying Stage
The fryer stage supports electric, diesel, or gas heating. This matters because buyers in different export markets face different utility costs and availability. A gas-fired fryer may suit a facility with existing natural gas infrastructure, while an electric option fits smaller operations where installing fuel storage is impractical. Selecting the right energy source before ordering avoids costly retrofitting after the line is on the floor [NEED_CITE: industrial fryer energy source selection criteria].
How Screw and Die Decisions Shape the Final Chip
The twin-screw design with alloy 38CrMoAl nitriding-treated screws handles corn flour blends at varying moisture levels while providing self-cleaning capability between batches. The screw configuration and die opening are matched to the target chip geometry — a triangular nacho shape demands a different die profile and cutting speed than a round tortilla chip. Getting this right at the design stage, rather than adjusting through trial and error on the production floor, is what keeps product density and crunch consistent across long runs.
The Role of the High-Pressure Die Mechanism and Forced Cooling
The double crank mechanism for die opening and closing maintains consistent pressure during continuous operation, which directly affects how uniformly the dough exits the barrel. Meanwhile, the increased radiator on the driving section provides forced cooling to the gearbox and motor assembly. In a snack line running extended shifts, thermal management of the drive train determines whether the extruder holds its RPM and torque output or begins to drift, changing shear conditions inside the barrel and altering product texture.
The Hidden Cost of Ignoring Line-Wide Throughput Calculations
When the extruder output exceeds what the fryer can handle, product queues in the hot-air texture former. Residence time increases, moisture content drops further than intended, and the chips entering the fryer absorb oil differently. The seasoning applied in the double-drum flavoring system then adheres unevenly because the surface oil film is inconsistent. These are not equipment failures — they are integration failures, and they show up as product quality complaints from distributors rather than alarm lights on the control panel [NEED_CITE: snack food quality deviation caused by line imbalance].
Why Sourcing the Full Range Under One Supplier Matters
Throughput matching between the extruder, fryer, and flavoring drums is calculated before the line is built, not guessed after installation. The screw configuration and die design are specified to the buyer’s actual corn flour formulation and target chip density, rather than copied from a generic build. An in-house testing workshop runs trial production on the buyer’s raw material before shipment, so product development is not delayed until the line is assembled on-site. Electrical schematics are confirmed against the destination market’s voltage and frequency standards. And wear parts — screws, dies, cutting blades — are documented and available so the first replacement does not trigger a sourcing crisis.
Documentation & Verification
- Line layout and capacity calculation showing matched throughput from extruder through fryer to flavoring
- Screw and die configuration record matched to your corn flour blend and target chip geometry
- Trial run report on your actual raw material from the in-house testing workshop
- Electrical schematic with voltage, frequency, and control language confirmed for your market
- CE declaration of conformity and ISO certificate for customs and regulatory submission
- Wear parts list with part numbers for screws, dies, and cutting blades
Installation, Commissioning & Support
- Foundation layout provided based on the selected model footprint, up to 33000×3500×4300 mm for the MT75
- Power supply confirmation covering the 22–55 kW main motor range and fryer heating load
- Line arrives in station modules for sequenced assembly and belt alignment on-site
- First-run commissioning includes screw speed, barrel temperature, and fryer set-point calibration
- Operator training covers speed-adjusted converter synchronization across feeding, extrusion, and cutting
- Spare screw segments and die inserts supplied with replacement schedule documentation
What to Include in Your Inquiry
Send your corn flour formulation details, including any secondary grains or starches in the blend, along with your target chip shape and thickness. Specify your local voltage and frequency, and whether your facility has gas, diesel, or electric supply available for the fryer stage. If you have an existing mixing or packing system upstream or downstream, share the model and throughput so the line can be matched at the boundaries.
Frequently Asked Questions
Q: How is throughput matched between the extruder, fryer, and flavoring stations?
A: Each station’s capacity is calculated from the same raw material formulation and target product density. The speed-adjusted converters on feeding, extrusion, and cutting allow fine-tuning so that product flow stays balanced without manual intervention or accumulation buffers between stages.
Q: What screw and die configuration is used for nacho and tortilla chips?
A: The screw profile and die geometry are specified after reviewing the buyer’s corn flour blend and target chip shape. The alloy 38CrMoAl nitriding-treated screws are configured for the moisture level and starch gelatinization requirements of the specific formulation being run.
Q: Is a trial run performed before the line ships?
A: Yes. The buyer’s raw material is tested in the in-house workshop. The trial run report covers extrusion behavior, product shape, fryer response, and final chip density, so adjustments are made before the equipment leaves the factory rather than during on-site commissioning.
Q: What voltage and control options are confirmed before shipment?
A: The electrical schematic is prepared with the buyer’s destination voltage and frequency confirmed in advance. Control language on the speed-adjusted converter interfaces is set to the operator’s preference so the line is ready for immediate commissioning upon arrival.
Q: What spare wear parts come with the line?
A: The delivery includes a documented wear parts list covering screws, dies, and rotary cutting blades. The replacement schedule is based on typical corn flour processing conditions, and part numbers are recorded so reorders match the original specification.