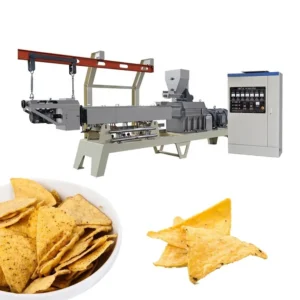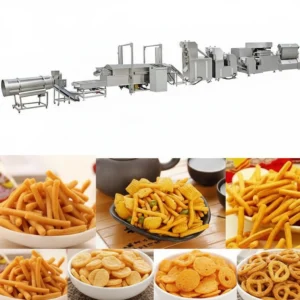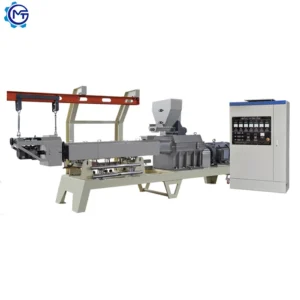
Line-Matched Frying Station — Every throughput figure is calculated against your upstream extruder and downstream coating drum, not pulled from a generic nameplate.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Continuous Deep Fryer for Snack Food Production Line |
| Power Source | Electric / Gas (dual heating method options) |
| Voltage | 380V/50HZ |
| Rated Power | 60 kW heating tube power; 2.6 kW auxiliary power (source value — verify against manufacturer catalog) |
| Oil Capacity | 320 L |
| Output Capacity | 100–1000 kg/h (basis not stated in source — confirm product type, moisture content, frying time) |
| Overall Dimensions (L×W×H) | 6700 × 2200 × 1200 mm |
| Net Weight | 2000 kg |
| Control System | PLC |
| Conveyor | Automatic belt conveying with frequency conversion stepless speed regulation |
| Lifting System | Automatic lifting for upper hood and mesh belt |
| Mesh Belt | Upper and lower double-layer mesh belt (prevents product floating) |
| Oil Filtration | Continuous oil circulation filtration system |
| Slag Discharge | Bottom slag discharge system |
| Material | Food-grade 304 stainless steel |
| Warranty | 1 Year (core components: 1 Year) |
| Assembly State | Fully assembled continuous line unit |
| Machinery Test Report | Provided |
| Video Outgoing-Inspection | Provided |
| Standards | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Extruded corn snack frying | Corn-based pellets and direct-expanded shapes requiring post-extrusion oil finishing |
| Pellet chip production lines | 2D and 3D pellet snacks fried to target moisture and crispness |
| Flavored fried chip lines | Formed potato or composite starch chips entering seasoning drums after frying |
| Food & beverage factory integration | Continuous frying station replacing batch fryers for higher daily throughput |
What "100–1000 kg/h" Leaves Out About Your Continuous Frying Machine for Snack Production Line
A fryer’s real output depends entirely on what enters the belt and how long it stays submerged.
I have seen overseas snack producers buy a continuous fryer based on a nameplate number, then discover that their corn pellet recipe needs a frying dwell time that cuts the rated throughput in half. The oil volume, belt speed, and heating recovery rate all interact with your specific product geometry and moisture content. When the upstream extruder pushes more volume than the fryer can handle at the required dwell time, product backs up, oil temperature drops, and you end up with unevenly fried chips that fail the texture spec your market expects [NEED_CITE: oil temperature recovery rates in continuous deep frying of snack foods]. That mismatch is why every continuous frying machine for snack production line we configure starts with your actual raw material and target frying time, not a catalog figure.
How Belt Width and Oil Volume Define Your Real Throughput
The 6700 mm overall length houses a frying zone where the double-layer mesh belt keeps lightweight snack pieces submerged for uniform oil contact. The 320 L oil capacity provides thermal mass that absorbs the temperature drop when cold product enters, maintaining a stable frying profile across the belt width. When you specify a continuous frying machine for snack production line, the belt width must cover the full output spread from your extruder and cooler upstream, so pieces arrive in a single layer without overlapping.
Matching the Fryer to Upstream Extrusion and Downstream Coating
A continuous deep fryer sits between the extrusion-forming stage and the seasoning drum. If the extruder delivers product faster than the fryer can process it at the correct dwell time, the buffer conveyor overflows. If the fryer outpaces the coating drum, fried chips cool down and reject seasoning powder. The frequency conversion stepless speed regulation on this unit lets you tune belt speed to balance both directions, but only if the line layout accounts for every station’s real cycle time [NEED_CITE: throughput balancing in snack food processing lines].
Reading the Specs That Actually Matter on the Factory Floor
The 60 kW heating tube power determines how fast the oil recovers after each batch of product enters the tank — a critical factor when running high-moisture items that pull heat from the oil. The 304 stainless steel construction across all contact surfaces resists the acidic degradation that frying oils cause over thousands of operating hours. The PLC control system stores frying profiles by product recipe, so operators switching from corn chips to pellet snacks can recall the exact belt speed and temperature without manual guesswork. The 380V/50HZ electrical supply is standard for most industrial markets, but voltage confirmation must happen before production starts to avoid motor and heating element failures on site.
The Hidden Cost of Specifying a Fryer in Isolation
I once worked on a line where the buyer sourced a standalone continuous fryer without mapping it to the slicer upstream. The fryer sat idling for half of every shift because the slicer could not feed it fast enough, and the oil burned off during idle periods, driving up consumable costs and darkening the oil beyond acceptable acid value limits. The buyer ended up replacing oil more often than budgeted, and the seasoning drum downstream ran empty waiting for product. That idle-burn cycle is the most expensive mistake in frying line design, and it happens because the fryer was quoted as a standalone unit rather than a station in a balanced line [NEED_CITE: oil degradation rates during idle periods in continuous fryers].
Why Sourcing the Fryer from Your Line Builder Changes the Outcome
The fryer throughput is calculated against your extruder’s real output on your recipe, not a generic capacity chart. Screw configuration and die design on the upstream extruder determine product geometry, which in turn sets the frying dwell time this unit must deliver. An in-house testing workshop runs your raw material through the extrusion and frying stages before shipment, so the belt speed and temperature profile are documented in a trial run report. The electrical schematic and voltage confirmation match your facility’s supply before the machine leaves the factory. And because the entire line from batching through extrusion, frying, and coating comes from one supplier, every station’s throughput is matched at the design stage rather than reconciled on your floor.
Documentation & Verification
- Line layout and capacity calculation showing fryer matched to extruder and coating drum throughput
- Machine specification sheet with confirmed heating method and voltage for your facility
- Electrical schematic and voltage confirmation matched to your local power supply standard
- Factory test record on your actual snack product geometry and moisture content before dispatch
- CE declaration of conformity for industrial frying equipment
- Wear parts list covering mesh belt segments, heating elements, and oil filter cartridges
Installation, Commissioning & Support
- Floor space allocation based on 6700 × 2200 mm footprint with clearance for hood lifting and maintenance access
- Dedicated 380V circuit sized for 60 kW heating load plus auxiliary motor draw
- Fully assembled unit arrives requiring utility hookup, oil fill, and PLC parameter loading
- First-run commissioning includes belt speed calibration against your product’s target frying dwell time
- Operator training covers PLC recipe storage, oil filtration cycle timing, and slag discharge procedures
- Spare wear parts inventory covers mesh belt sections, heating tubes, and filtration media for first-year operation
What We Need to Size Your Frying Station Correctly
Share the product type you intend to fry — whether extruded corn pellets, 3D pellet chips, or formed composite chips — along with the target moisture content after frying. Provide your upstream extruder model or its confirmed output so we can match belt speed and oil volume. Confirm your facility voltage and frequency, and let us know whether electric or gas heating fits your local utility cost structure. If you already have a seasoning drum or coating line downstream, send its capacity so we can balance the full line before building your continuous frying machine for snack production line.
Frequently Asked Questions
Q: How is fryer capacity matched to extruder output and downstream coating line speed?
A: We calculate the frying dwell time your product geometry requires, then set belt speed so the fryer neither starves the coating drum nor overflows from extruder output. The line layout document shows every station’s real throughput on your recipe, so no single machine becomes a bottleneck.
Q: Electric heating vs. gas heating — which is recommended for my production volume and local utility cost?
A: Electric heating offers precise PLC temperature control and simpler installation, while gas heating suits markets with lower gas tariffs and higher power costs. We confirm your local utility rates during consultation and specify the heating method that minimizes your per-kilogram frying cost.
Q: What voltage and frequency configurations are available for different export markets?
A: The standard configuration is 380V/50HZ, but we confirm your facility’s actual supply during the electrical schematic stage and adjust heating elements and motor ratings accordingly. Voltage mismatch is a leading cause of commissioning delays, so we lock this before production begins.
Q: How does the oil filtration system affect oil replacement intervals and operating cost?
A: The continuous oil circulation filtration system removes particulate matter that accelerates oil degradation, maintaining a lower acid value over extended runs. This extends the interval between full oil changes compared to static tank fryers, reducing your consumable oil expenditure over each production cycle.
Q: What upstream and downstream equipment is needed to form a complete frying and seasoning line?
A: A typical line includes an extruder or forming station, a cooling conveyor, this continuous fryer, a de-oiling belt, and a seasoning drum with powder or liquid coating capability. We configure every station under one line layout so throughput is balanced from raw material input to finished packaging.