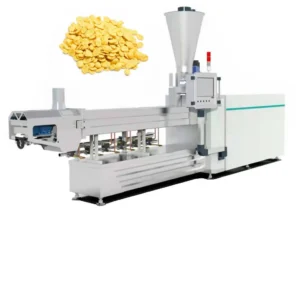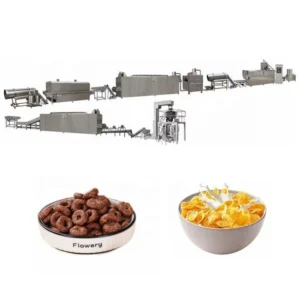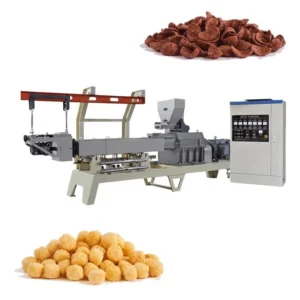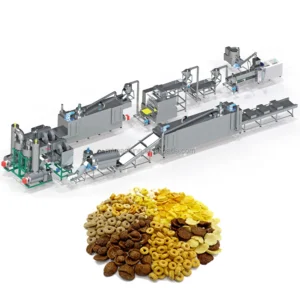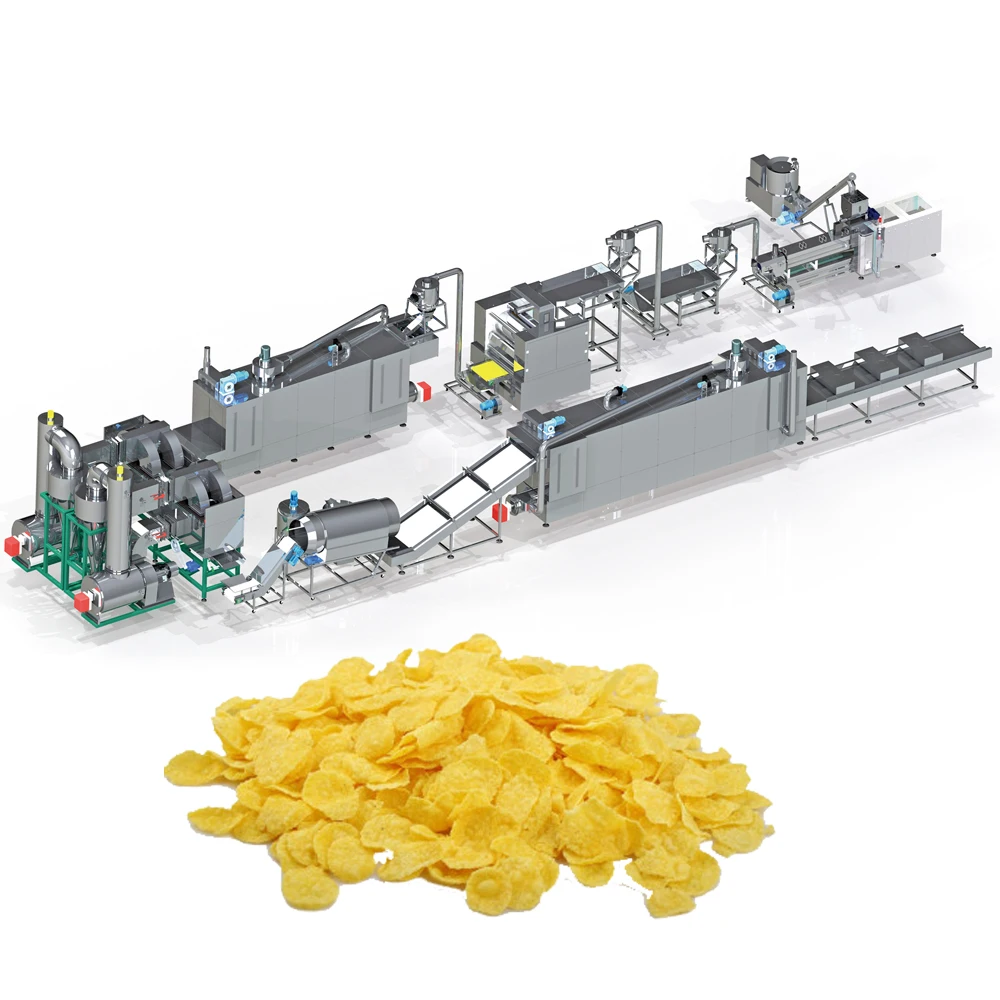
Throughput-matched line design — every station from the mixer through the packing conveyor is specified together so no single unit bottlenecks the corn flakes production flow.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Corn Flakes Extrusion Line |
| Available Extruder Models | MT70 / MT75 / MT85 |
| Screw Configuration | Twin-screw assembly |
| Installed Power | MT70: 160 kW; MT75: 210 kW; MT85: 190 kW |
| Power Consumption | MT70: 120 kW; MT75: 150 kW; MT85: 140 kW |
| Output Capacity | MT70: 150–200 kg/h (basis to be confirmed); MT75: 300–500 kg/h (basis to be confirmed); MT85: 300–400 kg/h (basis to be confirmed) |
| Overall Dimensions (L×W×H) | MT70: 41 × 1.5 × 2.2 m; MT75: 45 × 1.5 × 3.5 m; MT85: 43 × 1.5 × 3.2 m |
| Control System | PLC with optional MCC integration |
| Basic Raw Materials | Corn, rice, wheat, oat, barley powder |
| Production Procedure | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Coating → Cooling → Packing |
| Die Options | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Flaking Machine Features | Hydraulic double rollers, dual independent motors, infrared sensor temperature control |
| Hot Air Roasting Oven | Vibrating pan, conciliation burner, dual circulating fans, cyclone dust removal |
| Dryer Heating Source | Gas or electric |
| Certification | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes manufacturing | Corn grits and maize flour blends |
| Sugar-coated breakfast cereals | Extruded corn pellets with sugar or honey syrup |
| Multi-grain extruded cereal formats | Rice, wheat, oat, and barley powder mixtures |
| Shaped breakfast cereal production | Interchangeable die shapes including rings, stars, and balls |
What "Nominal Capacity" Leaves Out on a Corn Flakes Line
Output numbers mean nothing unless they reflect your actual grain blend, moisture level, and target flake density.
When a buyer asks what a corn flakes machine full equipment range can produce per hour, the real answer depends on the maize particle size entering the extruder, the barrel temperature profile, and whether the flaking rollers can keep pace. I once watched a line stall because the roasting oven was undersized for the extruder’s actual throughput — the cereal piled up, moisture crept back in, and the final product lost its crunch. That kind of mismatch doesn’t show up in a brochure [NEED_CITE: throughput balancing across extrusion line stations].
Matching Every Station from Mixer to Packing
A corn flakes line is only as fast as its slowest station. The twin-screw extruder may be rated for a given output, but the flaking machine must compress each pellet at the right thickness, the dryer must reduce moisture evenly, and the hot air roasting oven must blister the surface without scorching. Each unit in this range is sized relative to the extruder model chosen, so throughput stays balanced across the entire production sequence rather than breaking down at a single choke point.
Extruder Screw and Die Configuration to Your Grain
Corn behaves differently from oat or barley under shear and heat. The screw configuration and die gap must match the specific starch content, moisture, and particle size of the buyer’s raw material. A generic build copied from another product category often produces flakes that are too thick, too dense, or unevenly expanded. Before we lock in the die configuration, we ask for a sample of the actual flour — because maize from different regions gelatinises at different barrel temperatures [NEED_CITE: starch gelatinisation behaviour across grain varieties].
Reading the Specs That Matter for Flake Quality
The hydraulic double-roller flaking system uses dual independent motors so each roller can be driven separately, preventing uneven compression that causes cracked or inconsistent flakes. Infrared sensors monitor roller temperature in real time, keeping the surface heat even across the full roller width — critical when running at higher throughput where thermal drift can alter flake thickness mid-shift. The hot air roasting oven pairs a vibrating pan with a conciliation burner and dual circulating fans, creating uniform surface blistering that gives corn flakes their signature crispy texture. Die options span nine interchangeable mould shapes, allowing a single extrusion station to produce rings, balls, stars, and other formats without changing the core line layout.
The Cost of Overlooking Downstream Equipment
Buyers often focus on extruder power and output while treating the dryer and coating drum as afterthoughts. When the roasting oven cannot handle the extruder’s volume, partially roasted cereal moves downstream with residual moisture, leading to soggy flakes that fail shelf-life tests. An undersized sugar coating drum means uneven syrup distribution and rejected batches. These downstream failures cost more than the equipment upgrade would have [NEED_CITE: common causes of breakfast cereal product rejection at quality inspection].
Why Source the Full Range from One Equipment Supplier
Every station in this corn flakes line is specified under one engineering scope, so throughput calculations account for actual material flow between units. The screw and die configuration is documented against the buyer’s raw material sample, not pulled from a generic template. In-house trial runs on the buyer’s actual grain blend are completed before shipment, reducing on-site commissioning surprises. PLC control runs across the flaking machine and key stations, giving operators one interface to monitor and adjust. CE and ISO certifications are held at the company level, covering the full equipment range rather than individual components.
Documentation & Verification
- Line layout and capacity calculation showing station-by-station throughput matching
- Screw and die configuration record tied to your specific grain blend and moisture
- Trial run report on your raw material from the in-house testing workshop
- Electrical schematic with confirmed voltage, frequency, and control language
- Operation and maintenance manual covering all line stations
- Wear parts list with replacement intervals for screws, dies, and roller surfaces
Installation, Commissioning & Support
- Foundation planning based on the chosen extruder model’s overall dimensions and weight distribution
- Dedicated power circuit matching the line’s installed power requirement up to 210 kW
- On-site assembly sequencing from mixer through packing station with utility connections
- First-run parameter tuning including screw speed, barrel temperatures, and die gap adjustment
- Operator training on PLC interface covering extrusion, flaking, and roasting controls
- Spare screw elements, die plates, and flaking roller covers stocked for first replacement cycle
What We Need to Size Your Line
To configure the right extruder model and match every downstream station, share your primary grain type and its typical moisture content, your target daily output in finished product weight, and the available floor space and ceiling height in your facility. We also need your local voltage and frequency, preferred control language, and whether you plan to run sugar-coated variants alongside natural flakes. If you can send a raw material sample, we will run a trial in the testing workshop before finalising the quotation.
Frequently Asked Questions
Q: How is output capacity verified before the line ships?
A: We run trial batches on your actual raw material in the in-house testing workshop. The trial run report documents throughput, flake thickness, moisture reduction, and surface blistering quality at the tested conditions. This data — not a generic brochure figure — forms the basis of the capacity statement in your quotation.
Q: How are screw and die settings matched to my grain blend?
A: We request a sample of your maize flour or multi-grain mix and record its moisture, particle size, and starch behaviour under heat. The screw element sequence and die gap are then configured specifically for that material. The configuration record ships with your documentation package for future reference.
Q: Could the dryer or roasting oven bottleneck the extruder?
A: Each downstream station is sized relative to the extruder model selected. The capacity calculation in your line layout shows material flow through every unit, so the dryer, roasting oven, and coating drum are matched to the extruder’s verified throughput rather than chosen independently.
Q: What electrical and control details are confirmed before production?
A: We confirm your facility voltage, frequency, and preferred PLC display language before the line enters production. The electrical schematic in your documentation package reflects these specifications, so there are no surprises when the line arrives on site.
Q: Can I test my raw material before committing to the order?
A: Yes. Send your grain sample to the testing workshop and we run it through the extruder, flaking machine, and roasting oven at production-relevant settings. You receive the trial report with product samples before the quotation is finalised and production begins.