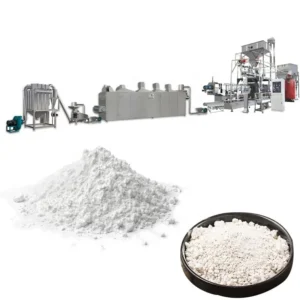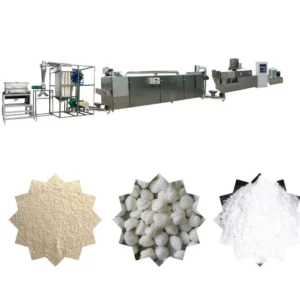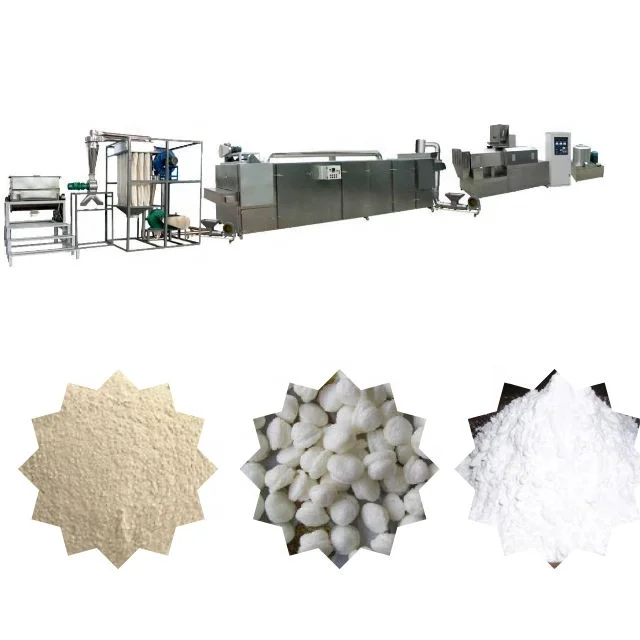
Matched Throughput Across Every Station — A single-source modified starch extrusion line where the mixer batch output, screw conveyor feed rate, twin-screw extruder throughput, dryer capacity and grinder rating are all sized together against your specific starch type and moisture profile.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Modified Starch Twin-Screw Extrusion Processing Line |
| Equipment Type | Twin screw extruder machine |
| Capacity Range | 80–500 kg/h (basis not stated in source — confirm raw material type, moisture content and target starch modification degree) |
| Raw Materials | Wheat flour, corn starch, potato starch |
| Mixer Motor Power | 4.0 kW |
| Mixer Dimensions | 1.2 × 0.9 × 1.4 m |
| Mixer Batch Output | 3.0–4.0 kg per batch |
| Screw Conveyor Motor Power | 1.1 kW |
| Screw Conveyor Dimensions | 2.5 × 0.6 × 2.3 m |
| Screw Conveyor Output | 0–150 kg/h |
| Barrel & Screw Material | 45 steel |
| Key Contact Material | Food grade stainless steel 304 |
| Frame Material | Stainless steel 201 |
| Motor Brand | Siemens (China) or domestic top brand |
| Inverter Brand | Delixi or Delta |
| Voltage & Frequency | Three-phase 380V/50Hz; Single-phase 220V/50Hz (customizable to local standards) |
| Energy Options | Electricity, gas, diesel, or steam |
| Total Electrical Power (electric heating) | Approximately 100 kW |
| Total Electrical Power (gas/diesel heating) | Approximately 50–60 kW |
| Process Flow | Mixer → Screw Conveyor → Twin Screw Extruder → Shift → Air Conveyor → Dryer → Air Conveyor → Conditioning → Conveyor → Grinder |
| Warranty | One year |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Pregelatinized starch for instant food and bakery blends | Corn starch, wheat flour at controlled moisture |
| Modified starch for paper manufacturing and adhesives | Potato starch, corn starch with target viscosity modification |
| Specialty food ingredient starches | Blends of wheat flour and corn starch for nutritional applications |
| Industrial textile and sizing starches | Potato and corn starch processed to defined gelatinisation degree |
What "80–500 kg/h" Leaves Out About Modified Starch Output
Capacity figures are meaningless unless they name the raw material, moisture content and target modification degree.
A modified starch processing line quoted at a single number across corn, potato and wheat starch hides a problem that only surfaces during commissioning. Corn starch gelatinises at a different temperature profile and shear requirement than potato starch. A screw configuration tuned for one material will under-process or over-heat another, producing starch that fails the buyer’s viscosity or solubility specification. I have seen plants where the extruder nameplate promised a certain throughput, but on the buyer’s actual potato starch formulation the output was noticeably lower — and the dryer downstream was already oversized for that real throughput, wasting energy on empty belt area [NEED_CITE: twin-screw extrusion gelatinisation parameters by starch type].
The modified starch processing line full equipment range addresses this by requiring the raw material type and target degree of modification before the capacity figure is confirmed. Each station — mixer, screw conveyor, extruder, dryer and grinder — is then sized to the real output that the buyer’s formulation will produce, not a generic benchmark.
How Each Station on the Line Connects to the Next
The process flow for this modified starch processing line full equipment range follows a deliberate sequence: batching and mixing, controlled feeding, twin-screw extrusion, drying, conditioning and grinding. The mixer delivers 3.0–4.0 kg batches that feed the screw conveyor, which meters material into the extruder at a controlled rate up to 150 kg/h. The twin-screw extruder performs the actual starch modification through shear, heat and moisture control inside the 45 steel barrel.
After extrusion, the air conveyor moves the extrudate to the dryer, where residual moisture is reduced to a level suitable for grinding. The conditioning unit stabilises the material before it reaches the grinder, which reduces it to the target particle size. If any one of these stations is undersized relative to the others, the entire line backs up. The modified starch processing line full equipment range is configured so that each station’s throughput aligns with the confirmed capacity of the extruder on the buyer’s specific formulation.
Starch Type Determines the Screw and Die Configuration
Corn starch, potato starch and wheat flour behave differently inside the extruder barrel. Potato starch granules are larger and gelatinise at a lower temperature than corn starch, meaning the barrel temperature profile and screw element arrangement must be adjusted to avoid excessive shear that degrades the starch polymer. Wheat flour contains protein alongside starch, introducing a different rheological behaviour that affects how the material flows through the die.
The screw configuration and die design on this line are specified after the buyer confirms their raw material and target modification degree [NEED_CITE: starch granule morphology and gelatinisation temperature differences]. A generic screw build copied from a standard extruder catalogue will produce inconsistent gelatinisation, leading to modified starch that does not meet the buyer’s viscosity or water-binding specification. The in-house testing workshop allows trial runs on the buyer’s actual raw material before the configuration is locked in for production.
Reading the Specifications That Actually Matter
The total connected load varies significantly depending on the energy source chosen. Electric heating draws approximately 100 kW, while gas or diesel heating reduces the electrical demand to approximately 50–60 kW — a difference that affects the transformer size and dedicated circuit requirements at the installation site. Buyers must confirm the local voltage and frequency before production begins, as the control panel and motor wiring are configured to match.
Food grade stainless steel 304 on all product contact surfaces ensures compliance with food safety requirements for starch destined for human consumption, while the stainless steel 201 frame provides structural rigidity in humid processing environments. The motor and inverter specification — Siemens (China) or domestic top brand motors paired with Delixi or Delta inverters — determines the precision of screw speed control, which directly affects the consistency of starch modification from batch to batch. The control system configuration should be confirmed as PLC or MCC depending on the level of automation the buyer requires for their modified starch processing line full equipment range.
The Hidden Cost of Mismatched Supporting Stations
When the extruder pushes material faster than the dryer can handle, the mesh belt loads up, moisture levels stay too high, and the grinder downstream produces clumped output that fails particle size specification. I have walked into plants where the extruder was rated for a certain capacity but the dryer was selected from a generic catalogue without reference to the actual extrudate moisture content. The result was a bottleneck that forced the operator to slow the extruder down, running the line well below the capacity the buyer had paid for [NEED_CITE: dryer capacity matching in starch extrusion lines].
Conversely, an oversized dryer wastes thermal energy and floor space. The screw conveyor output range of 0–150 kg/h must be matched to the extruder’s confirmed throughput on the buyer’s starch formulation, and the air conveyor must move material between stations without accumulation or degradation. These matching decisions are where lines built from separate vendor purchases most commonly fail.
Why Source the Full Equipment Range from One Supplier
Complete line configuration under one supplier means the mixer batch output, screw conveyor feed rate, dryer belt length and grinder motor power are all calculated against the same confirmed extruder throughput — eliminating the throughput gaps that appear when stations are sourced separately.
Screw and die configuration is specified to the buyer’s exact starch type and target modification degree rather than copied from a generic build, ensuring the gelatinisation profile matches the product specification from the first production run.
In-house testing workshop trial runs on the buyer’s own raw material verify that the line produces starch meeting the required viscosity and solubility targets before shipment, reducing commissioning surprises.
Multiple energy source options — electricity, gas, diesel or steam — allow the line to be configured for the utility infrastructure and running cost targets at the buyer’s installation site.
Food grade stainless steel 304 contact materials and stainless steel 201 frame construction are standard across every station, maintaining hygienic consistency throughout the modified starch processing line full equipment range.
Documentation & Verification
- Line layout showing matched throughput across mixer, extruder, dryer and grinder
- Screw and die configuration record tied to your specific starch formulation
- Electrical schematic confirming voltage, frequency and control language before build
- Trial run report on your raw material from the in-house testing workshop
- CE declaration of conformity for the complete processing line
- Operation and maintenance manual with wear parts list for barrel and screw
Installation, Commissioning & Support
- Confirm three-phase 380V/50Hz supply and dedicated circuit for the approximately 100 kW electric heating load before delivery
- Verify floor space accommodates the full process flow from 1.2 m mixer through 2.5 m screw conveyor to dryer and grinder footprint
- Barrel and screw configuration validated during on-site commissioning against your starch modification targets
- Operator training covers screw speed adjustment via inverter and barrel temperature zone management
- Wear parts supply includes replacement 45 steel screw elements and die plates for ongoing production
- Annual maintenance schedule aligned with one-year warranty covering all stations on the line
What to Share When Requesting a Quotation
To configure the modified starch processing line full equipment range accurately, provide the specific starch type you will process — corn, potato or wheat — along with the target modification degree and any viscosity or solubility specification your end product must meet. Share the local voltage, frequency and preferred energy source at your facility so the electrical design and heating system are configured correctly from the start. If you have existing upstream batching or downstream packing equipment, describe its throughput so the new line integrates without capacity gaps.
Frequently Asked Questions
Q: How is the 80–500 kg/h capacity range verified for a specific starch type?
A: The capacity figure depends on the raw material — corn starch, potato starch or wheat flour — the incoming moisture content and the target modification degree. Before the capacity is confirmed, a trial run in the testing workshop processes your actual formulation through the twin-screw extruder. The measured output from that trial becomes the basis for sizing every downstream station on the line.
Q: Which supporting stations are matched to the extruder to prevent bottlenecks?
A: The screw conveyor output, dryer belt capacity, air conveyor throughput and grinder motor rating are all calculated against the extruder’s confirmed throughput on your starch formulation. The mixer batch output of 3.0–4.0 kg is timed to match the screw conveyor feed rate so material flows continuously without accumulation or starvation at any station.
Q: How does the energy source choice affect the total connected load?
A: Electric heating requires approximately 100 kW total connected load, while gas or diesel heating reduces the electrical demand to approximately 50–60 kW because only the motors and controls draw electricity. Steam heating shifts the thermal load entirely to the site boiler. The choice affects transformer sizing, circuit design and ongoing running costs at your facility.
Q: How is screw and die configuration selected for different starch types?
A: Potato starch granules gelatinise at a lower temperature than corn starch, so the barrel heating profile and screw element spacing must be adjusted to prevent polymer degradation. Wheat flour introduces protein that changes material flow behaviour through the die. The configuration is determined during the trial run on your raw material and documented in the screw and die configuration record.
Q: Can PLC or MCC control be specified for the complete line?
A: The control system configuration is confirmed during the pre-sales consultation. Motors from Siemens (China) or domestic top brands and inverters from Delixi or Delta are standard across the line. The PLC or MCC selection determines the level of automated coordination between the mixer, extruder, dryer and grinder, and the control language is confirmed before the panel is wired.