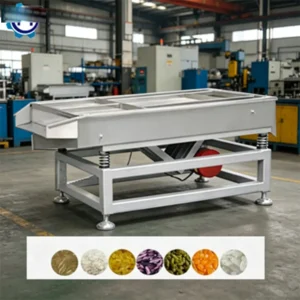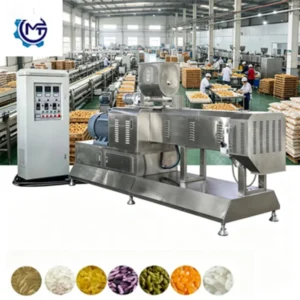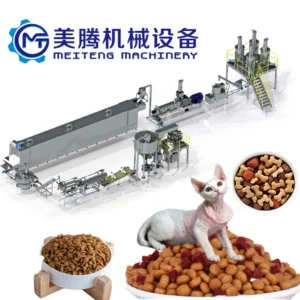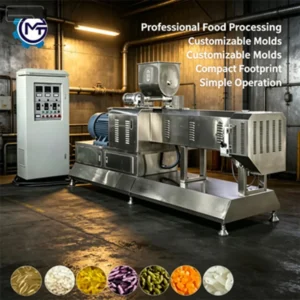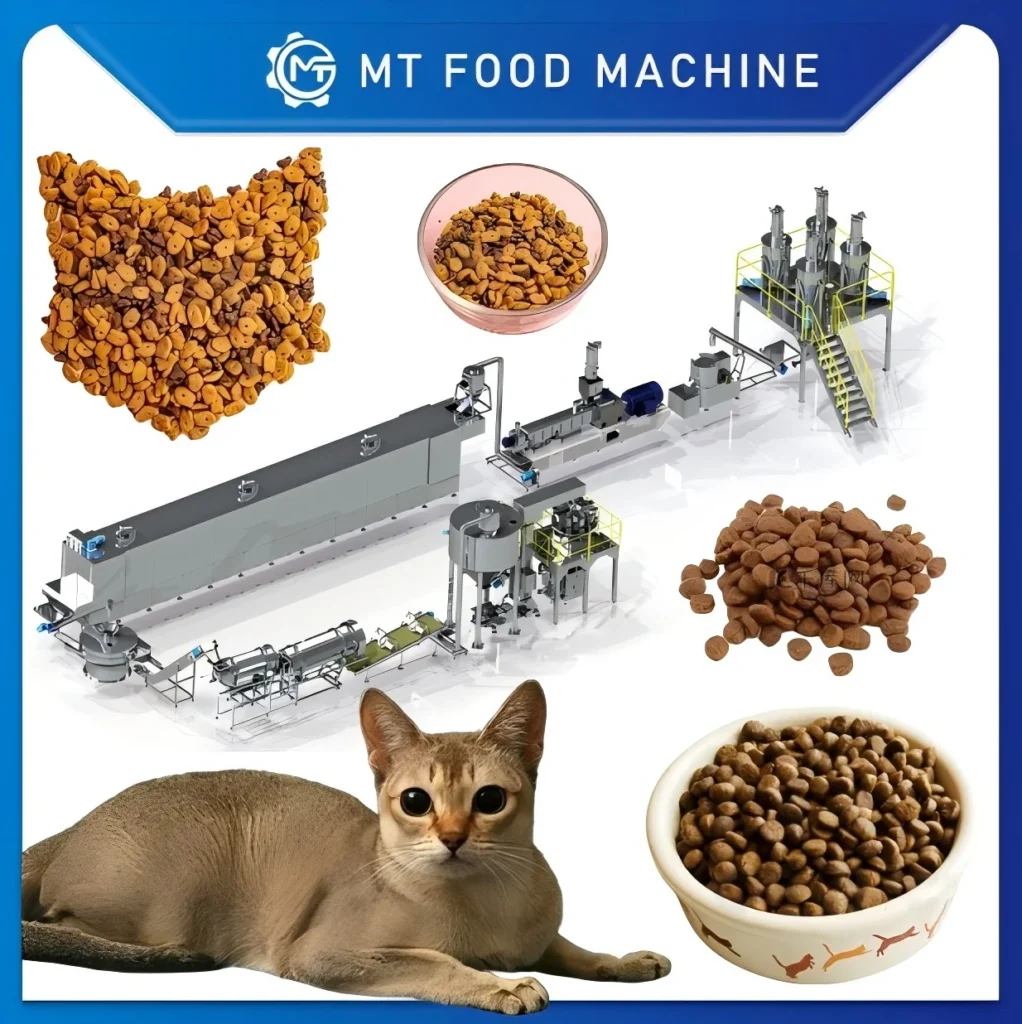
Matching Every Station to Your Recipe — throughput only holds when the dryer, coating drum, and cooler are sized against the extruder’s actual output on your raw material, not its brochure rating.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | PLC Controlled Multi-Species Cat Food Processing Line |
| Output Capacity | 100-200 kg/h (basis not stated in source — confirm raw material / moisture content) |
| Control System | PLC |
| Automation Level | Full Automation |
| Target Product Formats | Dry kibble, semi-moist, treats |
| Interface | User-friendly, intuitive controls |
| Quality Control Feature | Consistent product quality and stable nutritional content |
| Design Characteristic | Energy saving & eco-friendly design |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Dry kibble production for feline and canine species | Meat meal, corn, wheat, rice flour blends |
| Semi-moist pet food manufacturing | High-moisture formulations with humectants and palatants |
| Pet treats and snack formats | Starch and protein bases with varied inclusion rates |
Why "Nominal Capacity" Can Collapse the Moment You Switch Recipes
A pet food making machine for sale that prints 200 kg/h on paper rarely delivers that figure across every recipe you intend to run.
I remember a plant in Karachi that ordered a line rated at a specific throughput, only to find that when they shifted from a standard corn-heavy kibble recipe to a high-fibre weight-management formula, the actual output dropped sharply. The extruder was struggling with the different shear requirements, and the downstream dryer — sized to the original nominal figure — sat half-empty, burning energy on air. The entire line rhythm fell apart because one station was spec’d to a number that did not account for the recipe range [NEED_CITE: typical throughput variation across pet food formulations with different fibre and protein levels].
The Full Equipment Range Behind a Stable Kibble Line
A complete pet food processing line extends far beyond the extruder itself. The mixing and batching system must deliver a uniform blend before material ever enters the barrel, because inconsistent feed stock creates density variation that no downstream station can correct. Conveying equipment links every stage, and its speed must be synchronised with both the extruder output and the dryer residence time. When buyers survey the full equipment range before specifying a line, they avoid the trap of sourcing stations from separate vendors whose throughput ratings do not align.
Where Mismatched Stations Create Invisible Bottlenecks
The flavouring drum and coating line sit near the end of the chain, yet they dictate the final product weight and palatability. If the drum is undersized relative to the extruder, kibble queues up in the conveyor, absorbing ambient moisture and losing the crispness the market expects. I have walked through facilities where the packing station was the real choke point — bags were being sealed slower than the cooler could deliver, forcing operators to shut down upstream stations repeatedly [NEED_CITE: impact of downstream station mismatch on overall line effectiveness in extruded food production]. Sizing each machine against the extruder’s verified output on your specific formulation eliminates this cascade.
Reading the Specs That Actually Matter
The PLC control system governs barrel temperature profiles, screw speed, and feeder rates across the full line, which directly influences starch gelatinisation and the expansion ratio of the final kibble. Inconsistent gelatinisation leads to variation in digestibility — something pet owners and veterinarians notice. The automation level allows recipe parameters to be stored and recalled, reducing the batch-to-batch drift that manual adjustment inevitably introduces. Output capacity in the 100-200 kg/h range covers small-to-medium production runs, but this figure must be validated against your actual raw material blend and target moisture content before the line is built. Energy-efficient design in the dryer and cooler sections matters because those stations run continuously and account for a large share of total utility consumption in any extruded pet food making machine for sale.
The Cost of Skipping the Layout Stage
When buyers skip the line layout and capacity calculation stage, they often discover during commissioning that the dryer is too short for the moisture reduction the recipe demands, or that the cooler cannot bring kibble temperature down before packing, causing condensation inside the bag. These problems are not solved by turning a dial — they require physical station replacement, weeks of downtime, and capital that was not budgeted. A layout that maps every station’s throughput to the extruder’s verified output prevents these discoveries from happening on your factory floor instead of on the engineer’s screen [NEED_CITE: common post-installation line modification costs in extruded food manufacturing].
What Sourcing From One Supplier Actually Changes
Sourcing the entire line from a single supplier means the extruder, dryer, flavouring drum, cooler, and packing station are designed around the same throughput target rather than assembled from independent catalogues. Screw and die configurations are matched to the buyer’s raw material and target product before the machine leaves the factory. An in-house testing workshop allows trial runs on customer-supplied raw material, so you see the actual kibble density and texture before shipment. Pre-sales consultation extends through engineer-led layout design, on-site installation, commissioning, and operator training — ensuring the line performs as specified from the first production day. Documentation covers everything from electrical schematics to wear parts lists, so maintenance planning starts before the container arrives.
Documentation & Verification
- Line layout and capacity calculation showing throughput at every station for your pet food formulation
- Screw and die configuration record matched to your raw material blend and target kibble density
- Electrical schematic with voltage and frequency confirmed against your facility supply before production
- Trial run report generated on your actual raw material in the testing workshop prior to dispatch
- Factory test record documenting output, product quality, and control system response before packing
Installation, Commissioning & Support
- Foundation and floor space planning based on the full line footprint from mixer to packing station
- Dedicated power circuit sizing aligned with the PLC-controlled extruder and dryer combined load
- Modular station delivery allowing phased assembly in facilities with limited overhead clearance
- First-run parameter setting by on-site engineers covering barrel temperature, screw speed, and feeder calibration
- Operator training on recipe recall, alarm response, and daily inspection points across every station
- Wear parts inventory — screws, dies, seals — stocked and listed for each machine in the line
Planning Your Line Specification
To move forward with a configuration that fits your production goals, share your target pet species and kibble format, the primary raw materials in your formulation, and your intended daily output volume. Include your facility voltage and frequency, preferred control language, and any existing upstream or downstream equipment that the new line must integrate with. A sample of your raw material blend enables a trial run that verifies actual throughput before the engineering drawing stage begins.
Frequently Asked Questions
Q: How do I ensure the dryer and coating drum match the extruder so the line holds its rated throughput?
A: Request a capacity calculation that lists every station’s throughput based on your specific raw material and target moisture reduction. Each station — dryer, flavouring drum, cooler, packer — should be sized to the extruder’s verified output, not its nominal rating. Trial runs in the testing workshop confirm the match before the equipment ships.
Q: What supporting stations are included in the full equipment range, and what role does each play?
A: The range covers mixing and batching systems, conveying equipment, dryers, flavouring drums, coating and seasoning lines, coolers, and packing machines. Each station addresses a distinct stage: blending raw material, transporting product between processes, reducing moisture, applying palatants, stabilising temperature, and sealing finished kibble into bags.
Q: Can I order individual stations separately, or only as a complete line?
A: Individual machines such as dryers, flavouring drums, or packing stations can be sourced separately. However, throughput matching is most reliable when all stations are configured together, since each unit’s capacity must align with the extruder’s actual output on your formulation to avoid bottlenecks.
Q: What voltage and control language options are available for each station?
A: Voltage and frequency are confirmed during the specification stage to match your facility’s power supply. The PLC interface supports configurable control languages. Electrical schematics and a voltage confirmation document are provided before production begins, preventing commissioning delays caused by mismatched supply or unreadable screens.
Q: How are spare wear parts stocked for the different machines in the line?
A: A wear parts list covers screws, dies, seals, and other consumables for every station. Parts are identified by machine and position so replacements can be ordered before the first change-out is due, avoiding unplanned downtime while waiting for shipments.