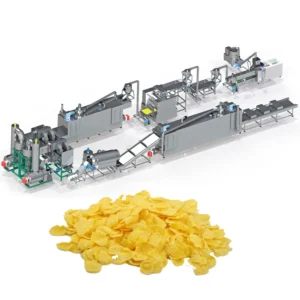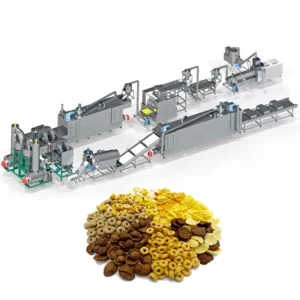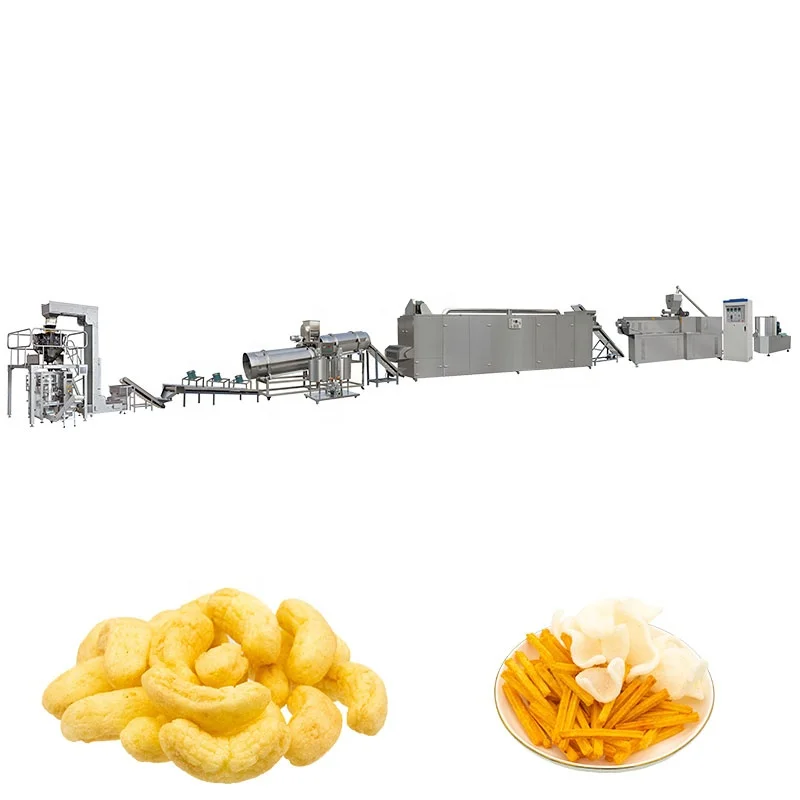
Throughput-Matched Stations — Every station from the mixer to the packing scale is sized to the MT-75’s actual output on your grain recipe, preventing silent bottlenecks that plague lines assembled from separate vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-75 Twin Screw Extruder |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin Screw |
| Production Capacity | 200-300 kg/h (basis not stated in source — confirm raw material formulation / moisture content) |
| Control System | PLC and MCC control |
| Voltage | 220V / 380V (frequency to be confirmed) |
| Heating Source (Dryer) | Gas / Electric |
| Flaking System | Hydraulic double rollers, separate motor drives, infrared temperature control |
| Roasting Oven | Vibrating pan, dual circulating fans, cyclone dust removal, reconciliation burner |
| Coating System | Double tumble melter, elevator, coating drum, spraying nozzle |
| Line Configuration (Natural) | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Cooling → Packing |
| Line Configuration (Sugar-Coated) | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Spraying → Sugar Coating → Drying → Cooling → Packing |
| Core Components | Gearbox |
| Warranty | 1 Year; 1 Year on core components |
| Machinery Test Report | Provided |
| Video Outgoing Inspection | Provided |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal market | De-germed corn grits, maize flour |
| Sugar-coated cereal flakes | Corn, rice, or wheat-based extrudate with sugar or honey glaze |
| Multi-grain breakfast flakes | Blends of oat, barley, rice, and wheat |
| Puffed and flaked snack formats | Corn meal, rice flour, or composite grain recipes |
| Fortified cereal production | Grain base with added vitamin and mineral premix |
What a Nameplate Capacity Rating Leaves Out on a Corn Flakes Line
A line quoted at a nominal throughput will only hold that number if every downstream station is sized to the extruder’s real output on your specific grain formulation — not its catalog rating.
I once stood in a workshop outside Lagos watching an entire corn flakes line sit idle for five days. The extruder ran fine on our standard corn grits during the factory test, but the locally sourced de-germed maize the buyer used had a higher residual fat content. The flakes collapsed coming out of the die, and the dryer could not keep up with the adjusted feed rate we eventually dialed in. The corn flakes production line equipment for sale had been spec’d on paper, not on the buyer’s actual material. Sizing a line demands more than matching nameplate numbers across stations; it demands a trial run on the grain you will actually feed into the hopper [NEED_CITE: grain composition variability in Sub-Saharan maize supply chains]. When the flaking rollers, dryer belt length, and roaster residence time are all calculated from the extruder’s verified output on your recipe, the line holds its rate shift after shift.
How Twin-Screw Shear Controls Flake Integrity
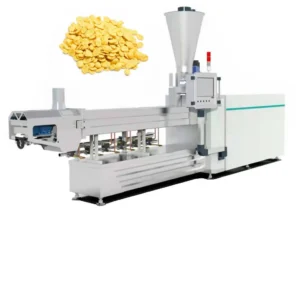
The MT-75 uses a twin-screw configuration to generate the mechanical shear and thermal profile needed for thorough starch gelatinisation across a range of grain recipes. Barrel sections are heated independently, letting the operator build a temperature gradient that matches the specific gelatinisation window of corn, wheat, or multi-grain blends. Consistent gelatinisation is what gives the extrudate enough structural strength to survive the flaking rollers without crumbling, which directly determines the final flake appearance and bowl crispness. The screw elements and die aperture are specified together so that the corn flakes production line equipment for sale produces a rope of the correct diameter and moisture for downstream processing.
Matching the Dryer and Roaster to Real Extruder Output
A common failure in assembled cereal lines is an undersized dryer that forces the extruder to run below its capable rate. The hot-air roasting oven on this line uses two independent circulating fans and a cyclone dust removal device to maintain even heat distribution across the vibrating pan. This matters because uneven roasting produces flakes with soft centres that go soggy within seconds of hitting milk. The reconciliation burner in the combustion chamber allows fine temperature adjustment so that surface blistering — the visual cue buyers expect on premium natural corn flakes — is achieved without scorching [NEED_CITE: blister formation and moisture equilibrium in flaked cereal roasting]. Gas or electric heating options let the line adapt to local utility costs and availability.
Reading the Specs That Actually Determine Flake Quality
The hydraulic double-roller flaking station uses separate motors for each roller, which prevents the speed differential that causes flake tearing on single-drive units. Infrared sensors monitor roller surface temperature continuously, because even a few degrees of drift will change flake thickness and alter the roasting time required downstream. The PLC and MCC control architecture logs these parameters per batch, so an operator can reproduce a successful run weeks later by recalling the stored recipe. Voltage is configurable between 220V and 380V, but the frequency — 50 Hz or 60 Hz — must be confirmed against the destination market before the motors and heaters are wired, since running a 50 Hz motor on 60 Hz supply shifts every driven component to a different operating point. The gearbox is listed as the core component under warranty, reflecting its role in translating motor torque to the screw shafts under continuous high-load extrusion.
The Hidden Cost of Skipping the Trial Run
Lines shipped without a factory test on the buyer’s real grain formulation routinely stall during commissioning. Screw combinations that work on one corn variety may produce under-expanded extrudate on another, forcing days of trial-and-error on the factory floor while installation crews wait and production schedules slip. The flaking rollers then receive material outside their designed thickness range, accelerating wear on the roller surfaces. Downstream, a roaster calibrated for the expected moisture profile will either over-dry or under-dry the flakes, creating a batch rejection problem that looks like a machine fault but is actually a process mismatch [NEED_CITE: extrusion process validation before equipment shipment]. These cascading issues cost far more in lost production time than a pre-shipment trial run ever would.
Why Source This Line from One Supplier
Every station on this corn flakes production line is configured under a single supplier, which means throughput calculations are reconciled across the mixer, extruder, flaker, dryer, roaster, coater, and cooler before the layout is finalized. The screw configuration and die design are specified against the buyer’s raw material and target flake format rather than copied from a generic build. An in-house testing workshop allows trial runs on customer-supplied grain before the line ships, catching formulation issues early. Twin-screw expertise extends across pet food, aquatic feed, snacks, and cereal applications, so process knowledge transfers between product categories when a buyer wants to run multiple formats on related equipment. Pre-sales engineering covers line layout, utility planning, and phased installation scheduling rather than ending at machine delivery.
Documentation & Verification
- Line layout with capacity calculation matching every station to verified extruder output
- Screw and die configuration record specific to your corn, rice, or multi-grain recipe
- Factory trial run report produced on your supplied raw material before dispatch
- Electrical schematic with confirmed voltage, frequency, and control language for your market
- CE declaration of conformity and ISO certificate included with shipment documentation
- Operation and maintenance manual with wear parts list and reorder codes
Installation, Commissioning & Support
- Foundation plan accounts for the MT-75 gearbox weight and vibrating roaster pan loads
- Dedicated electrical circuits sized for PLC and MCC control panel plus heater banks
- Stations arrive modular and are aligned on-site to the approved line layout drawing
- First-run commissioning includes screw speed, barrel temperature, and roller gap calibration
- Operator training covers recipe recall, roller temperature monitoring, and roaster fan balance
- Wear parts list covers screws, dies, and flaking roller surfaces with reorder lead times noted
- Scheduled maintenance intervals set around gearbox oil checks and infrared sensor calibration
What to Include in Your Inquiry
To configure a corn flakes production line equipment for sale that matches your operation, share the grain varieties and formulations you plan to run, including moisture content and any fat or fibre specifications from your supplier. Confirm your target daily output in finished flake weight, your workshop dimensions including ceiling height for the dryer and roaster exhaust routing, and the local voltage and frequency standard. If you already operate upstream milling or downstream packing equipment, provide the interface details so the line can be integrated without gap conveyors or buffer hoppers.
Frequently Asked Questions
Q: How is line capacity verified against my specific grain formulation and moisture content?
A: Before shipment, your raw material is run through the MT-75 in the testing workshop. Output rate, extrudate expansion, and moisture profile are measured at each station. The dryer belt speed and roaster residence time are then adjusted so that every station handles the verified throughput without bottlenecking, and a trial run report is provided with the shipment.
Q: What voltage, frequency, and control language options are confirmed before shipment?
A: The line is configurable for 220V or 380V supply. Frequency — 50 Hz or 60 Hz — must be confirmed for your market because it affects motor speed across every driven station. The PLC interface language is set to your operator preference before the control panel is wired, so the HMI is readable from day one of commissioning.
Q: How is the screw and die configuration matched to different grain recipes?
A: Screw element arrangement and die aperture are selected based on the starch content, particle size, and fat level of your grain blend. Corn, rice, wheat, and oat each gelatinise at different temperatures and shear levels, so the configuration that produces clean rope extrudate for corn flakes may not suit an oat-heavy recipe. The testing workshop validates the setup before the line ships.
Q: How is dryer and roaster capacity sized so no station becomes a bottleneck?
A: Each station’s capacity is calculated from the extruder’s verified output on your material, not from a generic nameplate figure. The dryer belt length, roaster pan area, and circulating fan volume are all proportioned to handle the moisture load that the specific extrusion rate delivers, ensuring continuous flow through the corn flakes production line equipment for sale without accumulation or starvation at any point.
Q: What spare wear parts are included and available for reorder?
A: The initial shipment includes a wear parts set covering screws, die plates, and flaking roller surface inserts. The documentation pack lists each part with its reorder code and typical replacement interval based on the trial run data. Gearbox components carry a one-year warranty, and replacement parts are stocked for ongoing supply.