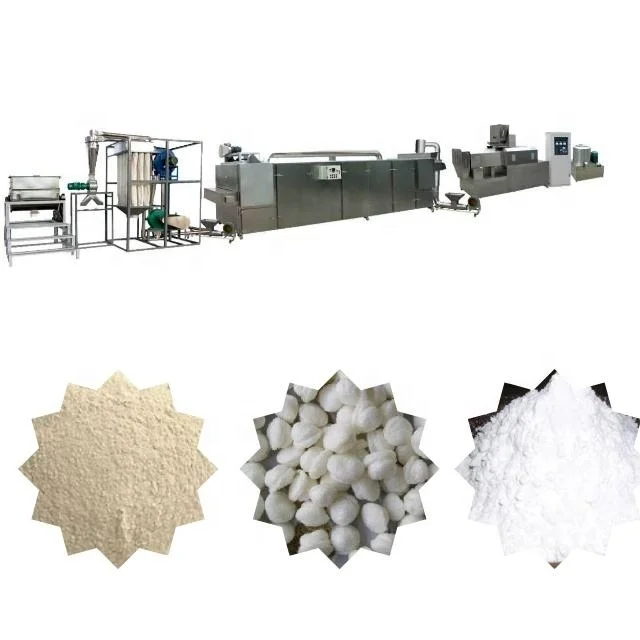
Screw Configuration Matched to Starch Source — we specify screw profile and die geometry against your exact corn, cassava, or potato starch batch rather than copying a generic build, so gelatinisation holds steady across every production run.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin-Screw Pre-Gelatinized Modified Starch Extrusion Line |
| Model Options | MT70 / MT85 / MT75 |
| Screw Type | Twin-screw |
| Screw Diameter (MT70) | 70 mm |
| Screw Length (MT70) | 1510 mm |
| Screw Material | 38CrMoAl |
| Main Motor Power (MT70) | 30 kW |
| Heating Zones (MT70) | 7 × 2 kW = 14 kW |
| Installed Power (MT70 / MT85 / MT75) | 160 kW / 190 kW / 210 kW |
| Operating Power (MT70 / MT85 / MT75) | 120 kW / 140 kW / 150 kW |
| Output Capacity (MT70 / MT85 / MT75) | 150–200 kg/h / 300–400 kg/h / 300–500 kg/h (basis to be confirmed on raw material type and moisture) |
| Mixer Batch Capacity (MT70 / MT85 / MT75) | 20–30 kg / 70–80 kg / 170–180 kg per cycle |
| Mixer Power (MT70 / MT85 / MT75) | 4 kW / 7.5 kW / 15 kW |
| Dryer Type | 5-layer baking oven |
| Dryer Fuel Options | Gas / Diesel / Electricity / Steam |
| Dryer Speed Control | Inverter |
| Grinder Type | Pulse grinder with cyclone discharge and dust collector |
| Contact Material | Stainless steel (201SS / 304SS food-grade parts) |
| Voltage & Frequency | 380V 50Hz 3-Phase (configurable to 415V 60Hz, 220V 60Hz, etc.) |
| Overall Line Dimensions (MT70 / MT85 / MT75) | 41000×1500×2200 mm / 43000×1500×3200 mm / 45000×1500×3500 mm |
| Key Features | Integrated barrel cooling, PLC/MCC control available, pre-assembled modules |
Application Suitability
| Application | Material or Output |
|---|---|
| Oil drilling fluid starch | Modified corn and cassava starch for viscosity control in drilling mud |
| Textile sizing and finishing | Pre-gelatinized starch from corn and potato for warp sizing and fabric coating |
| Paper coating and corrugation | Modified starch from cassava and corn for surface sizing and adhesive layers |
| Building material additives | Pre-gelatinized starch for gypsum board, drywall joint compound, and tile adhesive |
| Food-grade thickener and binder | Modified starch for instant food, soups, sauces, and bakery applications |
| Casting and foundry binders | Pre-gelatinized starch from corn and potato for sand core binding |
Why the Dryer and Grinder Matter as Much as the Extruder
A modified starch processing line equipment setup only reaches its stated output when every station holds the same throughput on your actual starch source.
I spent four days on a cassava starch line last winter because the dryer could not keep up with the extruder. The extruder was pushing pre-gelatinized starch out steadily, but the oven residence time was too short, so moisture stayed high and the grinder choked on tacky material. The buyer had chosen the extruder on capacity alone, without checking whether the downstream stations matched. When you specify modified starch processing line equipment, the conversation needs to cover mixer batch rate, extruder output, dryer belt speed and fuel type, and grinder throughput as one connected chain. A bottleneck at any station drags the entire line below the number on the nameplate. [NEED_CITE: throughput matching across extrusion line stations]
How Barrel Temperature Profiles Shape Gelatinisation
Starch gelatinisation happens in a narrow temperature window that shifts depending on whether you run corn, cassava, or potato starch. The twin-screw extruder in this modified starch processing line equipment range uses seven independently controlled heating zones with integrated barrel cooling to hold each section within that window. Cassava starch, for example, gelatinises at a lower temperature than corn starch, so the profile must ramp more gently in the feed section and level off before the die. Without zone-level cooling, residual shear heat pushes the material past the target and you get burnt spots or uneven expansion.
Matching Dryer Residence Time to Starch Moisture
The five-layer dryer uses inverter speed control so you can adjust belt travel to the moisture level leaving the extruder. Pre-gelatinized cassava starch typically exits the die at a higher moisture content than corn starch, meaning it needs a longer dwell in the oven. Switching fuel sources — gas, diesel, electricity, or steam — lets you match the thermal input to your facility’s utility setup without changing the dryer footprint. The multi-pass design gives the material five layers of exposure, which is important for modified starch processing line equipment where consistent final moisture directly affects grindability and shelf life.
What Screw Diameter and Length Mean for Starch
The MT70 runs a 70 mm screw diameter over 1510 mm length, giving a specific L/D ratio that determines how long the starch stays in the barrel. Longer residence allows more complete gelatinisation at lower shear, which matters when you process heat-sensitive potato starch. The 38CrMoAl screw material resists the abrasive wear that raw starch causes over extended runs. Main motor power at 30 kW on the MT70 provides enough torque to maintain screw speed even when feed viscosity spikes during cassava starch batches. The pulse grinder downstream uses cyclone discharge to pull ground starch away from the mill chamber quickly, reducing heat buildup that could damage the pre-gelatinized structure. [NEED_CITE: twin-screw extrusion parameters for starch gelatinisation]
The Hidden Cost of Skipping a Pre-Shipment Trial
I watched a buyer commission a line that had never seen their specific cassava starch variety. The screw combination was configured for a generic corn starch recipe, and the gelatinisation degree came out far below specification. Adjusting the screw elements and temperature curve on-site took the better part of a week, with production downtime the buyer had not budgeted for. A trial run in the testing workshop before shipment would have flagged the mismatch and let us adjust the configuration in days instead of weeks. Skipping that step means the first real production run becomes your development run. [NEED_CITE: importance of pre-shipment trial runs on buyer raw material]
Why Buyers Specify Equipment Here
Screw and die configurations are documented for each starch source you plan to run, so the build is not a copy of someone else’s line. Every station — mixer, extruder, dryer, grinder — is sized to hold matched throughput rather than assembled from leftover inventory. Voltage, frequency, and control language are confirmed against your facility’s electrical standard before production begins. The testing workshop runs your actual starch batch before the line ships, producing a trial report that becomes your commissioning baseline. Stainless steel contact materials across all stations mean food-grade compliance does not require a separate upgrade package.
Documentation & Verification
- Line layout drawing with matched capacity calculation for each station from mixer to packing
- Machine specification sheet recording screw and die configuration for your starch source
- Electrical schematic with confirmed voltage, frequency, and control panel language
- Trial run report on your raw material from the in-house testing workshop
- CE declaration of conformity covering the complete modified starch processing line equipment
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation plan reflecting the 41 m to 45 m line length and station-by-station load distribution
- Dedicated electrical circuit sized for 160 kW to 210 kW installed power depending on model
- Pre-assembled modules reduce on-site assembly time and alignment adjustments
- First-run parameter setting covering barrel zones, screw speed, and dryer belt speed
- Operator training on screw element changes and die swaps for different starch types
- Wear parts list for 38CrMoAl screws and dies with recommended stock levels
- Scheduled maintenance calendar tied to running hours and starch abrasion rates
What to Include in Your Inquiry
Send us the starch source you intend to process — corn, cassava, or potato — along with the moisture content of your raw feed and the target gelatinisation degree. Let us know your facility voltage and frequency, and whether your site uses gas, diesel, electricity, or steam for thermal processes. If you have a daily output target, include that along with available workshop length and ceiling height so the line layout fits your floor plan from the start.
Frequently Asked Questions
Q: How is the output capacity of each model verified, and on which starch source?
A: Capacity figures shown in the specification table are reference ranges. Actual output is verified during a trial run on your specific starch source at a defined moisture level, and the result is recorded in the trial report. We do not quote a firm capacity number without knowing your raw material and target product specification.
Q: Can the line voltage and frequency be matched to non-standard supplies?
A: Yes. The standard configuration is 380V 50Hz three-phase, but the electrical system can be built for 415V 60Hz, 220V 60Hz, or other supplies. Voltage and frequency are confirmed during the specification stage before production starts, and the electrical schematic reflects your exact requirement.
Q: How are extruder, dryer, and grinder capacities balanced?
A: Each station is selected so its maximum throughput matches the extruder output on your starch source. Dryer belt speed and layer count are sized to the moisture content leaving the die, and the pulse grinder is rated to handle the dried output without bottlenecking the line.
Q: What screw configurations are available for different starch sources?
A: Screw element arrangement and die geometry change depending on whether you run corn, cassava, or potato starch. Each starch type has a different gelatinisation temperature and shear sensitivity, so the screw profile is specified after reviewing your raw material data and target product.
Q: Is a trial run on the buyer’s raw material possible before shipment?
A: Yes. The in-house testing workshop runs your starch through the extruder, dryer, and grinder before the line ships. The trial report documents screw configuration, temperature profile, output rate, and product quality so commissioning on-site starts from a proven baseline.