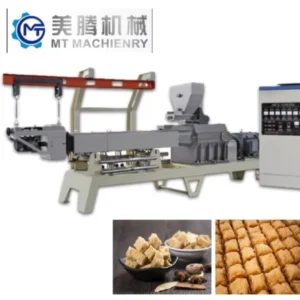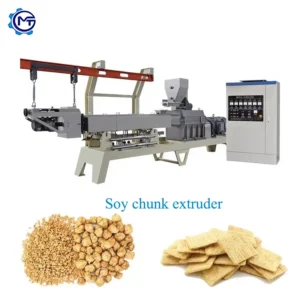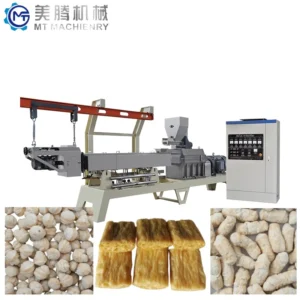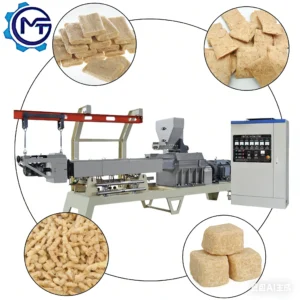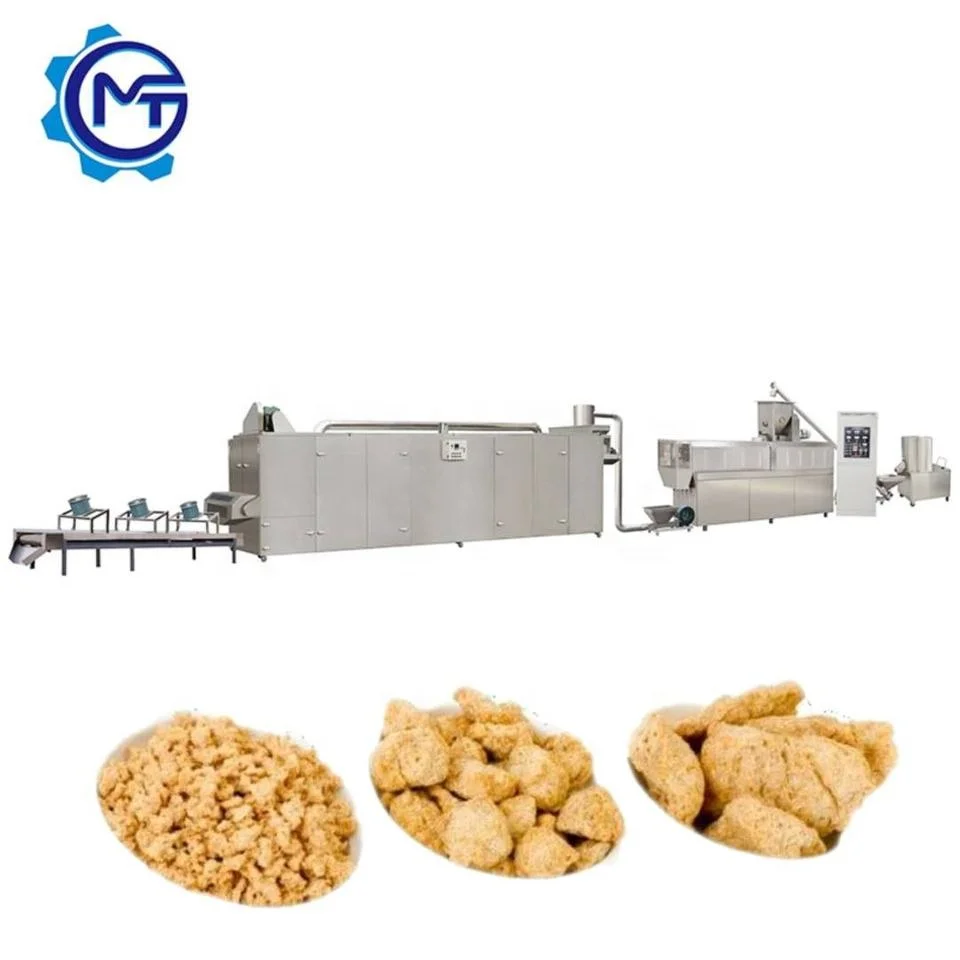
Throughput-Matched Integration — Every station from mixing to packing is engineered around your soybean meal characteristics, so rated capacity holds across the full line rather than collapsing at the dryer.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Textured Vegetable Protein (TVP) Production Line |
| Extruder Type | Double Screw (Twin Screw) |
| Available Models | MT65 / MT70 / MT85 |
| Installed Power | 85 kW (MT65) / 120 kW (MT70) / 195 kW (MT85) |
| Real Power Consumption | 65 kW (MT65) / 90 kW (MT70) / 165 kW (MT85) |
| Output Capacity | 150–200 kg/h (MT65), 200–300 kg/h (MT70), 600–800 kg/h (MT85) (basis not stated in source — confirm raw material, moisture, and product format) |
| Overall Dimensions | 18000×1300×2300 mm (MT65) / 20000×1500×2400 mm (MT70) / 24000×3500×4300 mm (MT85) |
| Construction Material | Stainless steel |
| Line Stations | Raw material preparation → mixing → conveying → extrusion → conveying → drying → cooling → packing |
| Warranty | 1 year complete warranty |
| Certification | CE compliant |
Application Suitability
| Application | Material or Output |
|---|---|
| Textured soy protein for ham and sausage analogues | Low-temperature soybean meal |
| Plant-based meat alternatives for canned food | Peanut meal and soy blends |
| Quick-frozen food protein ingredients | Textured vegetable protein chunks and strips |
| Fast food patty and nugget bases | Defatted soy flour and peanut protein |
| Cholesterol-free protein products for nutrition programmes | Soy and legume meal blends |
Why Nominal Capacity Rarely Survives Contact with Your Raw Material
A line rated on generic soy flour will underperform the moment your actual soybean meal has different protein content or moisture.
I saw this firsthand when a buyer ordered a twin-screw extrusion line based on brochure capacity. Their soybean meal had lower protein concentration than the test standard, and actual throughput dropped to roughly sixty percent of what was quoted. The extruder was not the bottleneck — the mismatch between screw configuration and their specific material was. When sourcing a plant based meat processing line manufacturer, the capacity number means nothing unless it is tied to your exact raw material, moisture level, and target product format [NEED_CITE: twin-screw extrusion throughput dependency on raw material protein content].
How Screw Configuration Changes Everything for Soy and Peanut Protein
The twin-screw extruder at the heart of this textured soy protein extrusion line for sale uses screw elements arranged specifically for the fibre-forming behaviour of soybean meal and peanut meal. Different protein concentrations demand different compression ratios and residence times inside the barrel. A screw profile designed for high-pro isolate will over-shear a lower-protein meal, destroying the fibrous texture that makes plant-based meat convincing.
We configure the screw sequence and die geometry after reviewing your material spec sheet, adjusting the shear profile so the protein molecules align into the layered, meat-like structure your end product requires.
Matching Every Station So the Line Actually Runs at Rate
A frequent failure in assembled lines is that one station cannot keep pace with the others. The extruder pushes product faster than the dryer can handle, or the cooling conveyor backs up before packing. Each station on this plant based meat processing line is sized against the extruder output so material flows continuously without accumulation or starvation. The mixing system feeds at a rate calculated for your batch cycle, the dryer length and airflow match the moisture removal requirement, and the cooling belt provides adequate dwell time before product reaches the packing station.
This throughput matching is documented in the line layout and capacity calculation before production begins [NEED_CITE: importance of throughput balancing in continuous food processing lines].
Reading the Specs That Actually Matter
Three parameters define whether this line will work in your facility. The installed power versus real power gap — for example, 120 kW installed against 90 kW real consumption on the MT70 — reflects motor starting overhead and heater cycling, which determines your transformer sizing and running cost. The overall dimensions, reaching 24 metres in length for the MT85 configuration, dictate your floor plan and utility routing before the equipment arrives. The stainless steel construction across all contact surfaces ensures compliance with food-grade requirements in most export markets, avoiding costly retrofits for hygiene audits.
The twin-screw design itself matters because single-screw extruders cannot generate the controlled shear and mixing intensity needed to restructure soy protein into fibrous textures — they produce a more uniform, less layered output unsuitable for meat analogue applications.
What Happens When the Dryer Is Undersized
Buyers often focus negotiation energy on the extruder and treat downstream equipment as secondary. An undersized dryer forces you to either slow the entire line or ship product with residual moisture that causes mould during storage. The extruder may be capable of running at a higher rate, but if the dryer cannot remove water fast enough, your actual output is dictated by the weakest station. This is the most common reason buyers report that their line "cannot reach the quoted capacity" — the bottleneck was never the extruder, and it could have been caught during the layout stage [NEED_CITE: dryer capacity matching in extrusion-based food lines].
Why Buyers Source This Line Here
Every station is specified under one supplier, so throughput responsibility does not fragment across multiple vendors pointing blame at each other. The screw configuration and die design are documented against your soybean meal or peanut meal sample, not copied from a generic build. An in-house testing workshop runs your actual raw material before shipment, so you see product texture and output data before the line leaves the factory. Multiple capacity tiers from the MT65 through the MT85 allow scaling from pilot production to full industrial volume within the same equipment family. Pre-sales engineering covers layout, utility planning, and voltage confirmation, so the installation phase addresses physical fit rather than discovering specification gaps.
Documentation & Verification
- Line layout drawing showing throughput calculation for each station against your target output
- Screw and die configuration record matched to your soybean meal protein content and moisture
- Trial run report on your raw material documenting product texture, density, and measured throughput
- Electrical schematic with confirmed voltage, frequency, and control language for your facility
- CE declaration of conformity and ISO certificate for import clearance
- Operation and maintenance manual with wear parts list for screws, dies, and seals
Installation, Commissioning & Support
- Floor plan review against the line dimensions — up to 24 metres length for the MT85 — before foundation work
- Dedicated power circuit sized to the real power draw, such as 90 kW for the MT70 configuration
- Equipment shipped in modular sections for site assembly matching your facility access constraints
- On-site commissioning with barrel temperature profile and screw speed tuned to your material
- Operator training covering die changes, screw element replacement, and dryer airflow adjustment
- Wear parts list identifying screw segments, die inserts, and seals with recommended replacement intervals
What We Need to Specify Your Line
To move from a general inquiry to a confirmed plant based meat processing line configuration, share your raw material specification including protein content and moisture percentage, your target product format such as chunks, strips, or granules, and your required hourly output. We also need your facility voltage and frequency, available floor space with ceiling height, and whether you plan to run soy and peanut protein on the same equipment. This information determines screw configuration, dryer length, and control system language before quotation.
Frequently Asked Questions
Q: How is throughput verified across mixing, extrusion, drying, and packing stations?
A: Each station is sized against the extruder output using your specific raw material data. The line layout document shows calculated throughput at every point — mixing batch cycle, extruder kg/h, dryer moisture removal rate, and packing speed — so bottlenecks are identified and resolved on paper before any equipment is built.
Q: What screw configuration is specified for soybean meal versus peanut meal?
A: Soybean meal and peanut meal differ in protein structure, fat residue, and fibre content, each requiring distinct compression ratios and shear profiles. We document the screw element sequence and die geometry against your material sample, adjusting kneading block arrangement and pitch to produce the correct fibrous texture for your target product.
Q: Can the line handle both soy and peanut protein in the same equipment?
A: Yes, the twin-screw extruder can process both materials. However, switching between soy and peanut protein typically requires screw configuration adjustment and die changes to maintain product texture. We provide the changeover procedure and any additional screw elements needed during commissioning.
Q: What is included in the pre-shipment trial run on customer raw material?
A: We run your actual soybean meal or peanut meal through the extruder in our testing workshop, documenting product texture, expansion ratio, moisture content after drying, and measured throughput. The trial run report is shared before shipment so you can verify the line meets your product specification before it leaves the factory.
Q: How are voltage, frequency, and control language confirmed before production?
A: These are locked in during the specification confirmation stage after quotation. The electrical schematic is reviewed with your facility engineer to verify transformer capacity, motor voltage, and control panel language. Any mismatch is corrected before the electrical cabinet is wired, preventing commissioning delays on site.