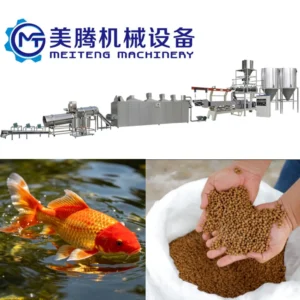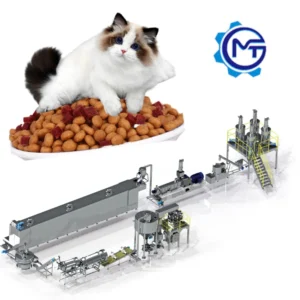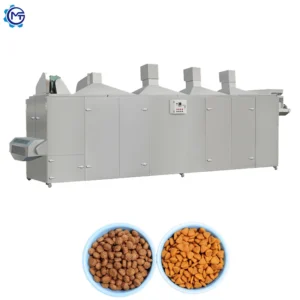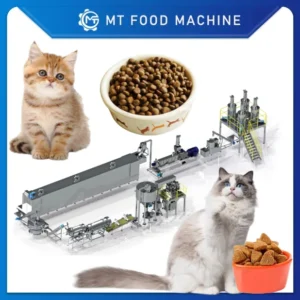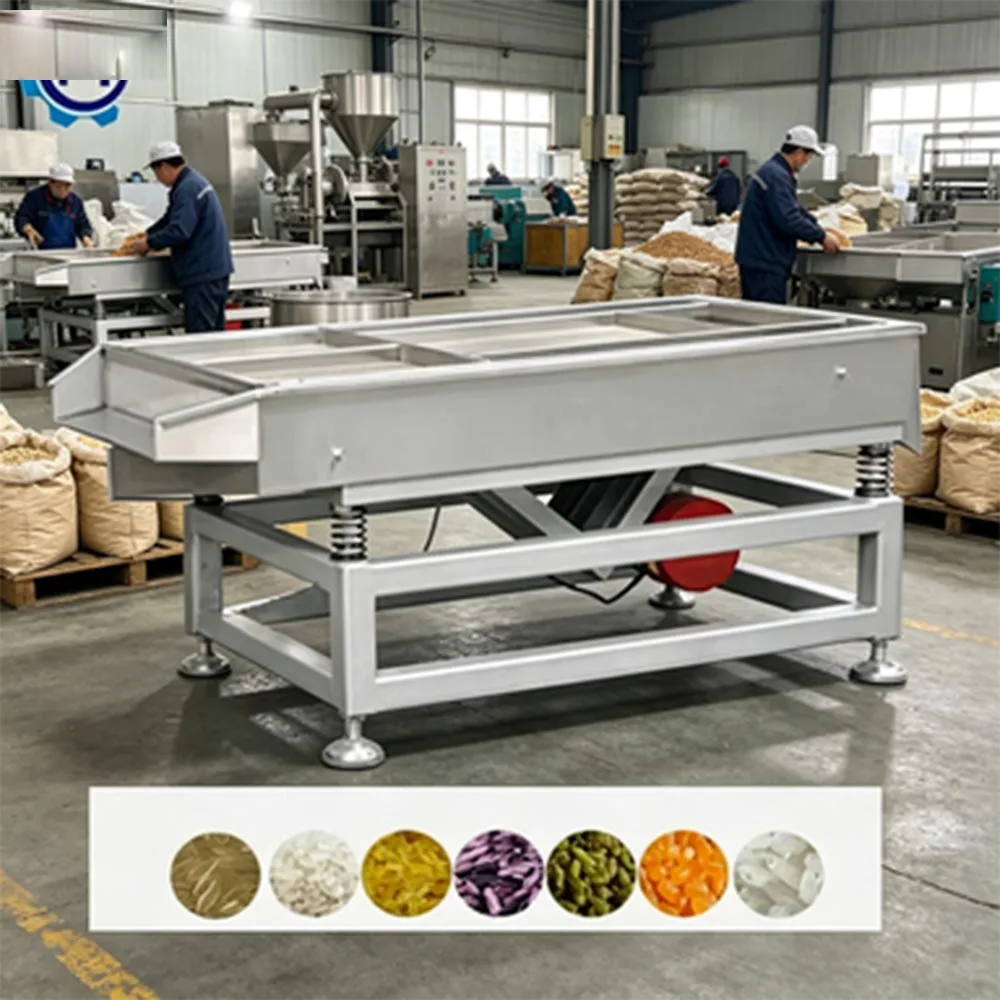
Station-by-station equipment matching — Every component from the raw material mixer through the twin-screw extruder to the vibrating sieve is specified as a coordinated set, preventing the hidden bottlenecks that occur when supporting stations are sourced separately.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruder Production Line for Aquatic and Pet Feed |
| Screw Type | Twin screw |
| Control System | PLC automatic control |
| Contact Material | Food-grade 304 stainless steel |
| Line Stations | Raw material mixer, extruder, dryer, seasoning/coating machine, vibrating sieve, conveyor equipment |
| Output Capacity | Large stable processing capacity for medium-to-large scale production (basis to be confirmed — depends on raw material formulation, moisture content, pellet size) |
| Pellet Adjustability | Size, hardness, buoyancy adjustable per breeding requirements |
| Feed Type Produced | Floating and sinking pellets |
| Operation Mode | Continuous automatic production with minimized manual intervention |
| Maintenance Design | Humanized operation interface, quick replacement of vulnerable parts |
Application Suitability
| Application | Material or Output |
|---|---|
| Aquatic feed production | Floating and sinking pellets for koi, goldfish, tropical fish, and freshwater species |
| Pet feed processing | Dry kibble from fish meal, soybean meal, corn powder, and compound additives |
| Dual-purpose commercial feed line | Medium-to-large scale mass production covering both aquatic and pet feed on one configuration |
| High-protein formulation extrusion | Aquatic feed using animal protein blends with variable fat content |
Why Nominal Capacity Figures Can Mislead Your Entire Line Plan
A twin screw fish feed pet feed extruder full equipment range is only as productive as its weakest matched station.
I once worked with a pet food manufacturer who ordered an extruder rated for a certain throughput on paper. The problem surfaced on day one of production: his raw material had a high protein content, and the actual output fell well below the quoted figure. The screw configuration had to be completely reworked. When you evaluate a twin screw fish feed pet feed extruder full equipment range, the capacity number means little without knowing the exact formulation, moisture level, and pellet diameter it was measured against. [NEED_CITE: extrusion throughput dependency on raw material composition]
How Each Station Connects Across the Extrusion Line
This twin screw fish feed pet feed extruder full equipment range begins with a raw material mixer that blends corn powder, fish meal, soybean meal, and additives into a uniform batch before feeding the extruder. The twin-screw mechanism subjects the mixture to high-temperature and high-pressure ripening inside the barrel, gelatinising starches and denaturing proteins so the pellet achieves uniform density and a smooth surface finish. From the die face, the extruded strands are cut and conveyed into the dryer, where residual moisture is reduced to a level suitable for storage and packaging.
Matching Dryer and Coating Capacity to Extruder Output
The dryer and seasoning drum are sized to handle the volume the extruder delivers at continuous operation, not just at startup. If the dryer cannot remove moisture fast enough, pellets queue up and the entire line slows to the dryer’s pace. The coating machine downstream must apply fat or flavouring evenly at the same rate pellets exit the dryer. When every station in this twin screw fish feed pet feed extruder full equipment range is specified together, the throughput at each point is calculated against the others rather than assumed. [NEED_CITE: industrial extrusion line bottleneck analysis]
Reading the Specs That Actually Matter for Pellet Quality
The twin-screw design allows operators to adjust screw segment arrangement and die geometry, which directly controls pellet expansion, density, and whether the final product floats or sinks. Floating pellets require a specific degree of expansion achieved through precise moisture content and barrel temperature profiling. The PLC control system manages barrel zone temperatures, screw speed, and feed rate simultaneously, maintaining batch-to-batch consistency that manual adjustment cannot hold over long production runs. Food-grade 304 stainless steel contact surfaces prevent corrosion from the acidic and saline components common in aquatic feed formulations, extending the service life of screws and barrels under continuous operation.
The Cost of Underspecifying Supporting Equipment
When a line is assembled from separate vendors, the extruder may perform as expected while the dryer or coater falls short, capping real throughput below the quoted nominal figure. I have seen situations where buyers discovered the mismatch only after installation, when the coating drum could not keep pace and pellets sat unseasoned for extended periods, absorbing moisture from the air. [NEED_CITE: post-installation throughput shortfall in mismatched extrusion lines]
Why Sourcing the Full Range From One Supplier Changes the Outcome
Every station in this line — mixer, extruder, dryer, seasoning drum, vibrating sieve, and conveyors — is specified against the others so that throughput is balanced from raw material intake to finished pellet discharge. Screw configuration and die design are matched to your specific raw material formulation and target pellet characteristics, not copied from a generic build. Before shipment, your actual raw material runs through the in-house testing workshop so parameters are verified and adjustments are made on the bench, not on your factory floor. Electrical schematics, voltage, frequency, and PLC language are confirmed for your target market before production begins, avoiding commissioning delays caused by incompatible control systems.
Documentation & Verification
- Line layout and capacity calculation showing throughput matching across every station
- Machine specification sheet with screw and die configuration matched to your formulation
- Trial run report on your actual raw material from the testing workshop
- Electrical schematic with voltage, frequency, and PLC language confirmed for your market
- CE declaration of conformity and ISO certificate documentation
Installation, Commissioning & Support
- Foundation and floor space planning based on the full line footprint including dryer and conveyor runs
- Dedicated power circuit specification matching PLC-controlled motor loads across all stations
- Assembly sequence from extruder placement through dryer alignment and conveyor integration
- First-run parameter setting for barrel temperature, screw speed, and feed rate on your formulation
- Operator training covering pellet buoyancy and hardness adjustment via screw and die changes
- Wear parts list identifying screws, die plates, and cutter blades with replacement intervals
What to Include in Your Initial Inquiry
Provide the specific raw materials you plan to process, including typical protein and fat percentages, along with the pellet diameter and buoyancy type your market requires. Include your facility’s available floor space, ceiling height, and local voltage and frequency standards so the line layout and electrical system are configured correctly before quotation.
Frequently Asked Questions
Q: What supporting stations are included and how is throughput matched between them?
A: The line includes a raw material mixer, twin-screw extruder, dryer, seasoning or coating machine, vibrating sieve, and conveyor equipment. Each station is sized against the extruder’s verified output on your specific formulation so that no single unit creates a bottleneck during continuous production.
Q: Can the same line produce both floating and sinking pellets, and what configuration changes are needed?
A: Yes. Floating and sinking pellets differ in expansion density, which is controlled by adjusting screw segment arrangement, die geometry, barrel temperature profile, and moisture content. The PLC system stores parameter sets for each pellet type so changeovers remain consistent.
Q: Which raw materials and formulations has the line been trialled on before shipment?
A: Before dispatch, your actual raw material — including fish meal, soybean meal, corn powder, and any compound additives you specify — runs through the testing workshop. The trial run report documents screw configuration, barrel settings, and pellet quality results for your review.
Q: What voltage, frequency and control language options are available for the PLC system?
A: The PLC system is configurable to match your facility’s voltage and frequency standards. The control interface language is confirmed during the specification phase before production begins, ensuring operators can navigate menus and alarms without translation delays during commissioning.