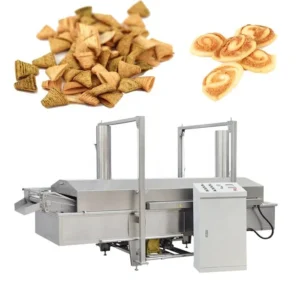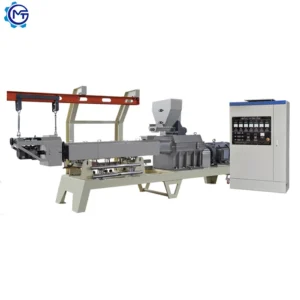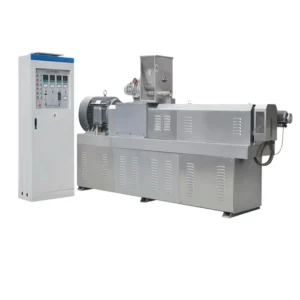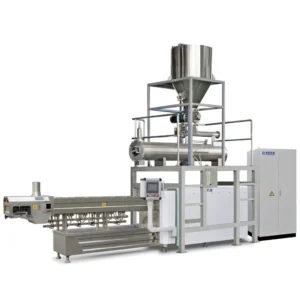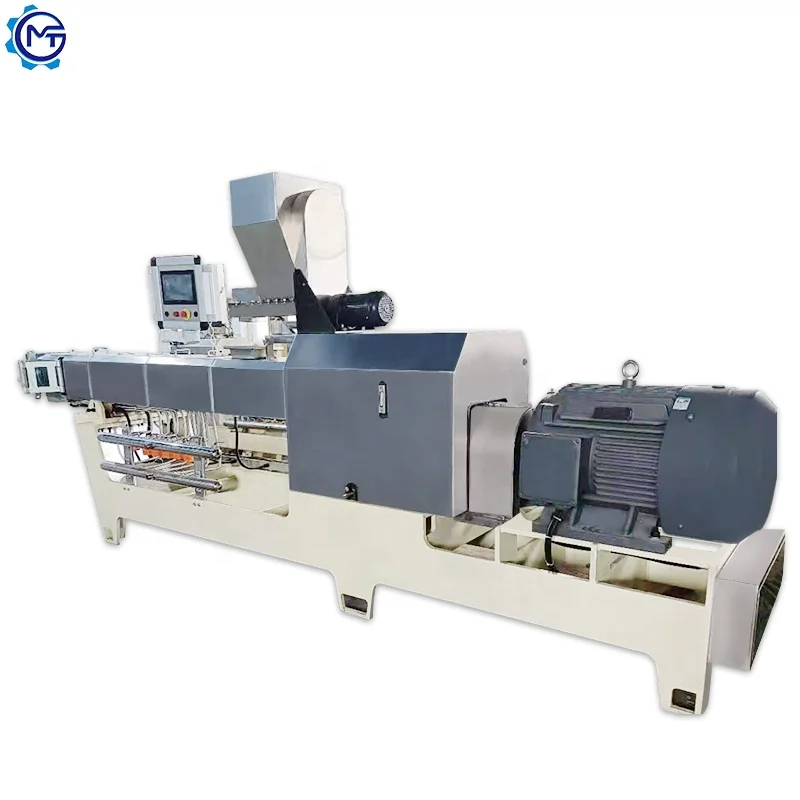
Throughput-Matched Stations — The MT65 frying chips making machine line aligns mixing, extrusion, frying, and flavoring capacity so no single station starves or floods the next.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 |
| Product Type | Twin Screw Extruder for Fried Snack Production Line |
| Screw Type | Twin screw |
| Main Power | 22 kW |
| Output Capacity | 100–150 kg/h (basis not stated in source — confirm raw material / moisture / product format) |
| Overall Dimensions | 22000 × 1200 × 2200 mm |
| Screw Material | Alloy 38CrMoAl, nitriding process |
| Feeding System | Food-grade stainless steel twin screw feeder with speed-adjusted converter |
| Cutting System | Rotary cutting knife on die head seat, V-belt drive, speed-adjusted converter |
| Main Motor | Siemens brand |
| Gearbox | Automatic lubrication function |
| Cooling | Increased radiator on driving part for forced cooling |
| Fryer Energy Options | Electric / diesel / gas |
| Flavoring System | Double drums with automatic flavoring function, powder hopper, conveyor, sprayer |
| Control System | PLC and MCC |
| Assembly State | Complete production line |
| Standards | CE, ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Nacho chips and tortilla chips | Corn flour formulations, sheeted and fried |
| Doritos-style triangular snacks | Corn-based dough, extruded, shaped, fried |
| Bugles and cone-shaped puffed snacks | Corn grits or corn flour, extruded through specialized die |
| Savory fried corn pellets | Corn starch blends, extruded and fried for crisp texture |
Why "Nominal Capacity" Means Nothing Without Your Raw Material
A frying chips making machine manufacturer must verify output against your actual corn flour blend, not a catalog figure.
I have seen lines quoted at a clean capacity number that collapses once the buyer’s local corn flour — often higher in fiber or varying in starch content — hits the barrel. The extruder struggles to maintain pressure, the fryer runs half-empty, and the flavoring drums receive an inconsistent feed. The entire line stalls at the bottleneck [NEED_CITE: twin-screw extrusion behavior on varying starch formulations]. That nominal number on the quotation was never a lie; it was simply measured on a different material than yours.
How Barrel Sections Shape Your Chip Texture
The twin-screw configuration on the MT65 allows operators to rearrange screw elements along the barrel to control shear, residence time, and gelatinisation. For a nacho chip that must hold a rigid, flat shape through frying, the screw profile needs to fully gelatinise the corn starch without over-expanding the dough at the die. This is not a fixed setting. A frying chips making machine manufacturer that ships a generic screw build will produce chips that curl, blister, or crack during frying because the starch matrix was not properly developed inside the barrel.
Die Geometry and the Density Question
The die plate determines not only the cross-section of the extruded rope — triangle for Doritos-style, cone for Bugles, flat ribbon for tortilla — but also the dough density as it exits. A die with insufficient land length lets the dough expand too quickly, resulting in a low-density piece that absorbs excessive oil in the fryer. The cutting system, driven by a speed-adjusted converter on a V-belt, must then slice at a rate synchronized with both extrusion speed and fryer belt velocity. If these three speeds drift apart, pieces pile up or the fryer runs gaps [NEED_CITE: extrusion die land length and expansion control in snack production].
Reading the Specs That Actually Matter
The 22 kW main motor, paired with a Siemens drive and forced-cooling radiator on the driving section, is sized for continuous operation under the high-torque conditions of corn flour extrusion. Corn dough is viscous; it loads the screws heavily, and without adequate cooling on the gearbox and motor housing, thermal stress shortens bearing life. The alloy 38CrMoAl nitrided screws resist abrasive wear from corn grits, which contain silica traces that erode untreated steel over production cycles. The food-grade stainless steel twin-screw feeder with its own speed-adjusted converter ensures that feed rate remains independent of screw speed, giving operators a second variable to control dough density before it even enters the barrel.
What Happens When Stations Are Mismatched
A fryer that cannot keep pace with the extruder forces operators to slow the entire line, running the twin-screw extruder below its stable operating window. At reduced throughput, residence time in the barrel increases, over-cooking the dough and altering chip color and taste. Conversely, an oversized flavoring drum tumbles chips too long, breaking fragile fried pieces and generating excess fines. These are not defects in individual machines; they are consequences of assembling a line from separate vendors who each quoted their station in isolation [NEED_CITE: throughput matching across extrusion and frying stations].
Why Source the Full Line Here
Every station on the MT65 line — from the batching mixer through the twin-screw extruder, fryer, and double-drum flavoring system — is configured under one supplier, meaning throughput is calculated across the full chain rather than per machine. Screw and die configurations are specified to the buyer’s corn flour sample and target chip shape before production begins. An in-house testing workshop runs trial extrusions on the buyer’s actual raw material, generating a test report before the line ships. Electrical schematics confirm voltage, frequency, and PLC language for the destination market. Post-installation, operator training covers screw element rearrangement for new product formats, and a wear parts list with screw and die replacement intervals is provided.
Documentation & Verification
- Line layout drawing showing throughput calculation across mixer, MT65 extruder, fryer, and flavoring drums
- Screw and die configuration record matched to your corn flour sample and target chip geometry
- Trial run report from in-house testing workshop using your raw material before dispatch
- Electrical schematic confirming voltage, frequency, and PLC control language for your market
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Wear parts list with screw element, die plate, and cutting blade replacement specifications
Installation, Commissioning & Support
- Floor plan with utility drop points for the 22000 mm line footprint, including fryer exhaust ducting
- Dedicated electrical circuit sizing for the 22 kW main motor plus fryer heating load
- Assembled extruder barrel and pre-wired MCC panel reduce on-site electrical work
- First-run commissioning includes screw speed, feed rate, and cutting speed synchronization
- Operator training covers die changes for switching between nacho, tortilla, and cone formats
- Spare screw elements, die plates, and cutting blades shipped with initial order
What We Need to Configure Your Line
Send a sample of your corn flour or corn grits along with your target chip format — nacho, tortilla triangle, or cone — so we can run a trial in the testing workshop. Confirm your local voltage and frequency, and whether your facility has gas, diesel, or electric supply available for the fryer. Let us know your available floor length and ceiling height so the line layout accounts for the fryer exhaust hood and flavoring drum clearance.
Frequently Asked Questions
Q: How is output capacity verified against my specific corn flour formulation and moisture level?
A: We run your raw material through the MT65 in our in-house testing workshop before shipment. The trial records extrusion pressure, dough temperature at the die, and piece density after frying. You receive a trial run report showing actual throughput on your formulation, not a catalog estimate.
Q: What screw and die configuration is selected for my target chip shape and density?
A: Screw elements are arranged along the barrel to match the gelatinisation profile your corn flour requires. The die plate is machined to your chip cross-section — triangle, cone, or flat ribbon — with land length calculated to control expansion. Both are documented in the configuration record shipped with the line.
Q: Are voltage, frequency, and PLC control language confirmed before shipment for my market?
A: Yes. The electrical schematic is reviewed with you during the specification stage. The PLC interface is set to your preferred language, and the MCC panel is wired for your local voltage and frequency. This is confirmed in writing before production begins.
Q: Is a trial run on my raw material conducted before the line ships?
A: Every MT65 line undergoes a trial run using the buyer’s corn flour sample in our testing workshop. The trial verifies screw configuration, die performance, and cutting synchronization. A full report is shared with the buyer before the line is cleared for packing.
Q: What wear parts are included and how are replacements supplied?
A: The initial shipment includes spare screw elements, die plates, and rotary cutting blades sized to your configuration. A wear parts list documents part numbers and replacement intervals. Replacements are manufactured to the same 38CrMoAl nitrided specification and shipped on request.