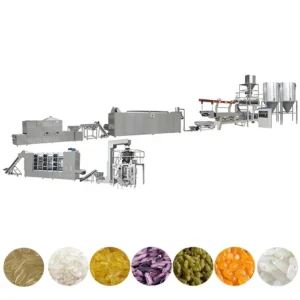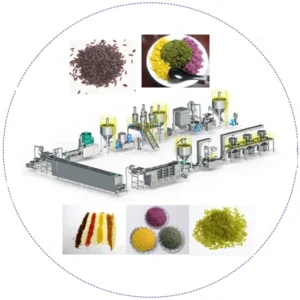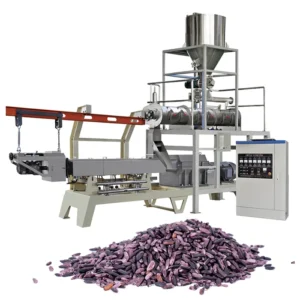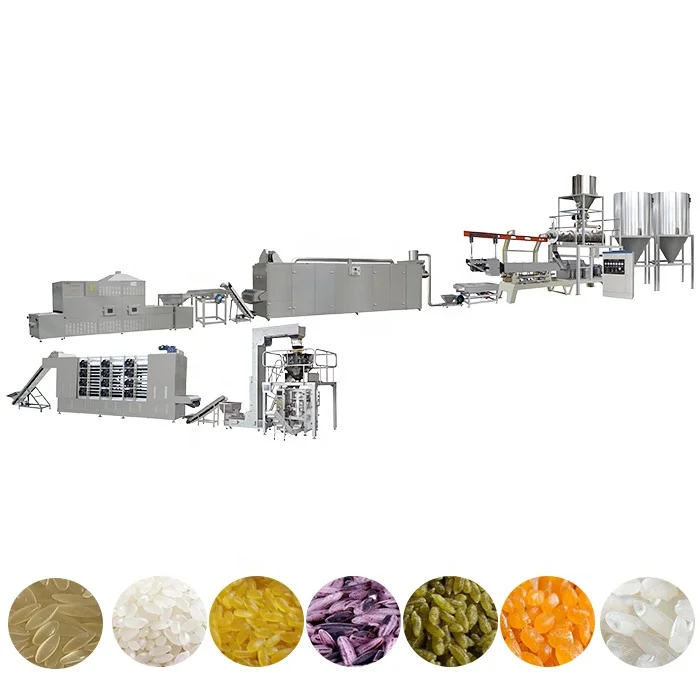
Integrated Line Engineering — every station from mixing through drying is throughput-matched on paper and verified during the pre-shipment trial run, eliminating the bottleneck risk that plagues pieced-together fortified rice lines.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 |
| Product Type | Fortified Rice & Couscous Production Line |
| Output Capacity | 100–500 kg/h (basis not stated in source — confirm raw material, moisture and product format) |
| Voltage & Frequency | 380V / 50Hz (configurable for destination market) |
| Control System | Fully automatic production control |
| Construction Material | Food-grade stainless steel on product contact surfaces |
| Line Assembly State | Complete production line |
| Standards Compliance | CE, ISO |
| Customization | Logo, packaging, graphic design, drawing-based and sample-based adjustments |
Application Suitability
| Application | Material or Output |
|---|---|
| FRK Fortified Artificial Rice | Rice flour, broken rice grits, vitamin and mineral premix blends |
| Couscous Production | Semolina, durum wheat flour with controlled hydration |
| Nutrition-Enhanced Grain Products | Cereal base flours combined with adjustable fortification premix ratios |
| Small to Medium Processing Plants | Batch or continuous runs targeting institutional and retail packed formats |
What the Rated Capacity Figure Hides on a full equipment range fortified rice production line manufacturer Quotation
Capacity is only meaningful once the raw material moisture, premix ratio, and downstream dryer residence time are all confirmed against the buyer’s actual formulation.
When an extruder is specified at a nominal output but the dryer or cooler cannot hold that throughput, the entire line stalls at the weakest station. I watched this happen on a North African FRK project where the dryer could not keep pace with the extruder output, forcing the operator to throttle feed rates down to roughly sixty percent of nameplate capacity. That lost production was not a mechanical failure — it was a specification gap that surfaced only after installation [NEED_CITE: throughput matching across extrusion line stations]. A responsible full equipment range fortified rice production line manufacturer will model every station’s throughput against the specific flour blend and moisture target before the line is built.
Station Sequencing for Fortified Rice and Couscous Formats
The MT65 line arranges raw material mixing, extrusion, shaping, drying and downstream handling in a single continuous flow. Each station is sized so that material neither queues nor starves at transfer points. This sequencing is what the full equipment range fortified rice production line manufacturer angle demands — buyers need to see where every machine sits before they commit to a layout.
Moisture Control Across the Drying Stage
Fortified rice kernels exit the die at a moisture level that must be brought down carefully to prevent cracking or case-hardening. The dryer section is specified with enough residence time and airflow volume to match the extruder’s output rate. When the premix includes heat-sensitive micronutrients, temperature profiling inside the dryer becomes critical to preserve nutritional integrity [NEED_CITE: drying temperature impact on vitamin retention in fortified rice].
Reading the Specs That Actually Matter
The 380V / 50Hz power configuration is standard for many Asian and African grid environments, but factories operating on 60Hz or different voltage levels need the motor and heating elements re-rated before build — a change that affects control panel components and transformer sizing. The food-grade stainless steel contact surfaces are necessary for lines running vitamin and mineral premixes, where iron or zinc residues can oxidize on mild steel and contaminate subsequent batches. The fully automatic production control system maintains consistent feed rate, barrel temperature and screw speed across shifts, which directly influences kernel density and cooking behavior of the finished rice. Capacity figures listed as 100–500 kg/h span a wide range; the achievable point within that band depends on flour particle size, premix loading percentage, and target moisture at the dryer outlet.
The Hidden Cost of an Unmatched Line Configuration
When the shaping die is selected for one product format but the buyer later switches to a different kernel size or couscous granule dimension, the downstream cooler and packing station may not handle the changed bulk density. Operators then face frequent line stops to recalibrate weighers and conveyors. These changeover losses compound over a production week [NEED_CITE: bulk density variation effects on downstream packing accuracy]. Specifying the die and screw profile against both current and planned future SKUs at the quotation stage prevents this downstream mismatch.
Why Source the Complete Line from One Equipment Supplier
Throughput calculations cover every station from batching to packing, so the dryer and cooler are never undersized relative to the extruder. Screw configuration and die design are matched to the buyer’s specific flour blend and premix ratio rather than copied from a generic build. An in-house testing workshop allows trial runs on the customer’s actual raw material before shipment, catching formulation issues early. Twin-screw expertise spans fortified rice, couscous, and adjacent nutritional grain applications, informing barrel temperature profiles and moisture targets. Pre-sales engineering through installation, commissioning and ongoing maintenance keeps a single technical team accountable across the project lifecycle.
Documentation & Verification
- Line layout and capacity calculation showing each station’s matched throughput for your premix formula
- Machine specification sheet recording screw and die configuration for FRK or couscous format
- Electrical schematic with voltage and frequency confirmed against your factory supply
- Trial run report produced on your actual raw material and fortification blend before dispatch
- CE declaration of conformity and ISO certificate for import clearance
- Operation and maintenance manual with wear parts list specific to your line configuration
Installation, Commissioning & Support
- Foundation plan based on the MT65 line footprint, covering mixer, extruder, dryer and cooler placement
- Dedicated power circuit sized for 380V / 50Hz supply with voltage stabilizer recommendation where grid fluctuation is common
- Modular station delivery allowing phased installation if workshop access limits full-line rigging
- First-run parameter setting covering barrel zones, screw speed and dryer temperature for your specific premix
- Operator training on the fully automatic control interface, including recipe storage for multiple fortification formulas
- Wear parts inventory list covering screws, die inserts and dryer belt segments for the first replacement cycle
Before You Send an Inquiry
Share your base flour type, premix composition and target moisture content so the line can be configured around your actual formulation rather than a generic template. Confirm your workshop voltage and frequency, along with available floor space and ceiling height, so the layout proposal accounts for dryer length and conveyor runs. If you plan to produce both fortified rice and couscous on the same line, note both formats upfront so the die and downstream stations accommodate the full SKU range.
Frequently Asked Questions
Q: What is the complete station list from mixing to packing, and where does each machine fit?
A: The MT65 line includes raw material mixing, extrusion, shaping, drying, cooling and packing stations in sequence. Each station is throughput-matched to the extruder output based on your specific formulation. A detailed layout drawing is provided at the proposal stage so you can see exact positioning and material flow direction before the build begins.
Q: How is the output capacity verified against our raw material and moisture content?
A: We run a trial in the testing workshop using your actual flour blend and premix ratio. The trial records extruder throughput, dryer residence time and finished product moisture, producing a report that confirms realistic output before shipment. This removes the gap between nameplate figures and actual production conditions.
Q: Which supporting equipment options match the extruder throughput?
A: Dryers, coolers, conveyors and packing stations are each sized to handle the extruder’s confirmed output on your material. Dryer length and airflow volume are calculated from the moisture reduction required. Cooler capacity is matched to the product temperature target before packing to prevent condensation inside sealed bags.
Q: How does the voltage configuration adapt to different country standards?
A: The standard 380V / 50Hz configuration can be adjusted for 60Hz markets or alternative voltage levels. Motor ratings, heating elements, control panel transformers and PLC power supplies are all re-specified during the design phase. Electrical schematics are confirmed with the buyer before production begins [NEED_CITE: industrial voltage and frequency standards by region].
Q: What customization is available for line configuration and footprint?
A: Layout adjustments accommodate existing workshop columns, ceiling height limits and utility connection points. Die and screw profiles are selected for your target kernel shape or couscous granule size. Control interface language and packing station format can be matched to your operator team and downstream logistics requirements.