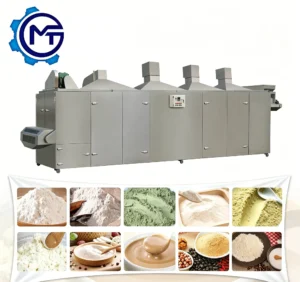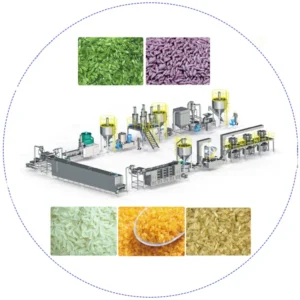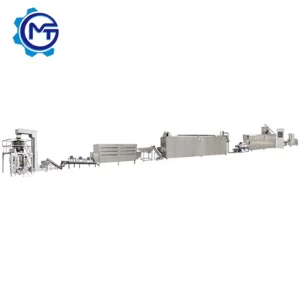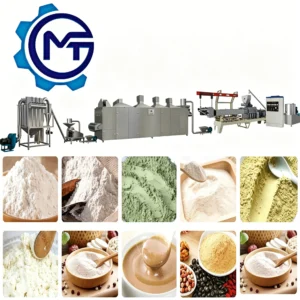
Complete Line Throughput Matching — every station from mixing to packing is sized against the chosen extruder model so the fortified rice line runs at its rated rhythm without intermediate buffers piling up.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fortified Rice Processing Line |
| Extruder Models Available | MT65 / MT70 / MT85 / MT75 / MT95 |
| Screw Type | Twin-screw |
| Installed Power Range | 85 kW (MT65) to 260 kW (MT95) |
| Power Consumption Range | 60 kW (MT65) to 195 kW (MT95) |
| Output Capacity | 80–1000 kg/h depending on model (basis not stated in source — confirm raw material formulation and moisture content) |
| Overall Line Dimensions | 28–36 m length × 1.2–3.5 m width × 2.2–4.3 m height depending on model |
| Control System | Frequency speed controlling |
| Drying Oven Heating Source | Electric or gas |
| Line Stations | Mixing → Extruding → Vibrating → Low-temperature drying → Cooling → High-temperature roasting → Cooling → Packing |
| Material Compatibility | Broken rice, rice, corn, millet, wheat, oats, buckwheat, bean, starch with vitamin and mineral additives |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice kernel production for nutrition programmes | Broken rice and rice bran blended with micro-nutrients, vitamins, and minerals |
| Artificial rice manufacturing for food relief and institutional supply | Rice flour and starch base with added iron, zinc, folic acid, and vitamin A |
| Instant rice porridge and breakfast cereal expansion | Corn, millet, oats, and buckwheat with nutrient fortification |
| Value-added grain processing from milling by-products | Rice bran and broken rice converted into uniform, reconstitutable kernels |
Why a Matching Dryer Matters More Than Extruder Horsepower
An extruder that outpaces its dryer creates a bottleneck that no motor upgrade can fix.
When a buyer specifies a high-output twin-screw extruder for a fortified rice processing line but pairs it with an undersized drying oven, the wet extrudate piles up on the cooling belt faster than moisture can be removed. I have watched lines in Southeast Asia stall every forty minutes because the downstream drying capacity was quoted on a different product with lower moisture content. The extruder sits idle while operators clear the backlog, and the actual daily output ends up far below what the motor plate suggests [NEED_CITE: line throughput matching principles in extrusion processing]. Voltage and frequency confirmation matter, but dryer-extruder mismatch is the silent killer of rated capacity.
Station-by-Station Equipment Coverage
The fortified rice processing line catalogue covers every stage from the batching and mixing system through the twin-screw extruder, vibrating cooler, low-temperature drying oven, high-temperature roaster, second cooling conveyor, and final packing station. Each piece of supporting equipment is selected to handle the volume the extruder produces at its working capacity. Frequency-controlled drives run across feeding, extruding, cutting, and mesh-belt systems so that speed adjustments at one station propagate smoothly to the next without manual recalibration.
Moisture Removal Across Two Drying Phases
Low-temperature drying removes surface moisture from freshly extruded rice kernels without case-hardening the exterior, while high-temperature roasting develops the final texture and shelf-stable moisture level. The drying oven uses a circulation drying process with mesh-belt speed controlled by a frequency motor, allowing operators to tune residence time to the specific grain formulation. Gas or electric heating sources are available depending on the destination market’s utility infrastructure. This two-phase approach prevents the cracking and uneven density that a single-pass dryer often introduces [NEED_CITE: two-stage drying for extruded grain products].
Reading the Spec Sheet Against Your Raw Material
The twin-screw extruder series spans five models with installed power from 85 kW to 260 kW, but the motor plate alone does not tell you which model fits your formulation. Broken rice behaves differently from a corn-millet blend in the barrel: gelatinisation temperature, starch damage, and fibre content all shift the residence time and shear profile needed inside the screw. The die design determines kernel shape and density, which affects how the kernels rehydrate when the end consumer cooks them. Frequency speed controlling keeps feed rate and screw speed synchronised, reducing batch-to-batch variation when operators switch between vitamin premix recipes. The overall line footprint ranges from 28 metres for the MT65 configuration to 36 metres for the MT95, so workshop length and ceiling height must be confirmed before layout finalisation.
What Happens When Line Stations Are Sourced Separately
Buying the extruder from one vendor and the dryer from another often results in incompatible control signals and mismatched throughput ratings. The extruder operator cannot communicate belt speed changes to a dryer that speaks a different PLC language, and spare parts sourcing splits across multiple suppliers with different lead times. When the first set of screws and dies wears out, the buyer discovers that the original vendor did not document the configuration, leaving the replacement order guesswork [NEED_CITE: equipment integration risks in multi-vendor processing lines].
Why Buyers Source the Full Range Here
Every station in the line is sized against the extruder model you select, so throughput figures are calculated end to end rather than quoted per isolated machine. Screw configuration and die design are specified to your raw material blend and the kernel density your market expects, not copied from a generic build. The in-house testing workshop runs your actual grain formulation before shipment, producing a trial run report that confirms capacity and texture. Electrical schematics are confirmed for your destination voltage and frequency before production starts, avoiding commissioning delays on site. Pre-sales consultation carries through to on-site installation, operator training, and wear parts supply.
Documentation & Verification
- Line layout and capacity calculation matched to your grain formulation and target output
- Machine specification sheet per selected extruder model with screw and die configuration record
- Trial run report on your actual raw material conducted in the testing workshop before dispatch
- Electrical schematic with voltage, frequency, and control language confirmed for your destination market
- CE declaration of conformity and ISO certificate included with customs documentation support
- Operation and maintenance manual with wear parts list and packing photographs
Installation, Commissioning & Support
- Foundation requirements scale with line footprint from 28 to 36 metres, confirmed during layout design
- Power supply must match installed power up to 260 kW with dedicated circuit breaker sizing per station
- Equipment ships in modular sections for container loading and reassembly at your workshop
- First-run commissioning includes screw speed, barrel temperature, and dryer belt calibration on your material
- Operator training covers frequency speed controlling interface and recipe changeover procedures
- Wear parts list covers screws, dies, and barrel sleeves with initial spare set included
- Maintenance schedule tied to drying oven heating elements and extruder screw inspection intervals
What We Need to Configure Your Line
To size each station correctly, share the grain or starch base you will run, the vitamin and mineral premix ratios, and the daily output target for your market. Workshop length, ceiling height, and local voltage and frequency standards determine the layout and electrical build. If you need the trial run conducted on your exact formulation before shipment, send a representative sample batch to the testing workshop.
Frequently Asked Questions
Q: How is output capacity verified against the buyer’s actual raw material formulation?
A: The testing workshop runs your specific grain blend and premix through the selected twin-screw extruder model before shipment. A trial run report documents the achievable throughput, kernel density, and moisture profile at each station, so the quoted capacity reflects your material rather than a generic benchmark.
Q: What voltage, frequency, and control language options are available for each model?
A: Electrical schematics are built to your destination market’s standards, with voltage and frequency confirmed before production. Control panel labelling and frequency speed controlling interface language are specified during the quotation stage to match your operators’ requirements.
Q: How are dryer and roaster capacities matched to the chosen extruder to avoid line bottlenecks?
A: Each drying and roasting station is selected based on the moisture removal load the extruder produces at its working output. Mesh-belt speed and residence time are calculated so that wet extrudate does not accumulate between stations, keeping the full line at a steady rhythm.
Q: Which screw and die configurations are specified for fortified rice versus plain artificial rice?
A: Fortified rice with vitamin and mineral additives requires screw profiles that manage different gelatinisation behaviour and die designs that produce uniform kernel density for consistent rehydration. Configuration records are documented per project so replacements match the original specification.
Q: What spare wear parts are supplied with the initial shipment?
A: The wear parts list covers screws, dies, and barrel sleeves relevant to the selected model. An initial spare set ships with the line so that the first replacement cycle does not interrupt production while waiting for international freight.