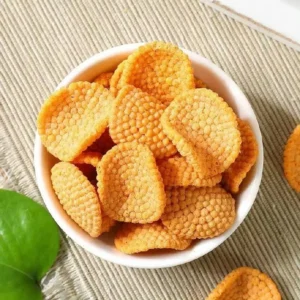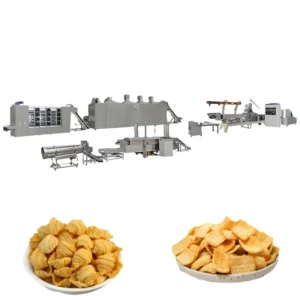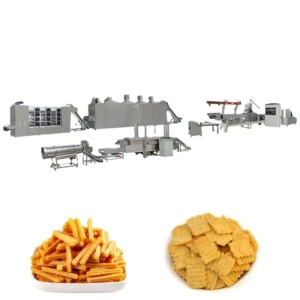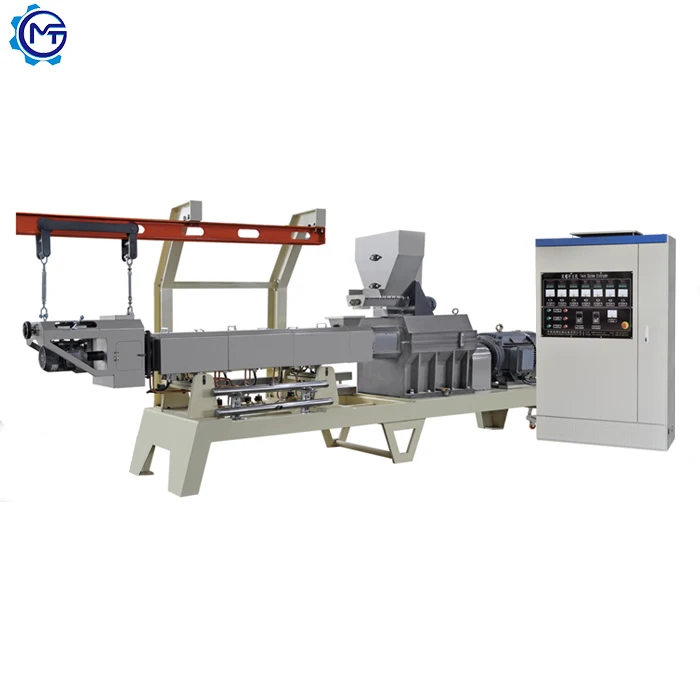
Integrated Line Throughput Matching — Every station from the mixer to the packing conveyor is sized against your actual raw material and target shape, not quoted on a nominal extruder rating alone.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fried Puffed Snack Production Line |
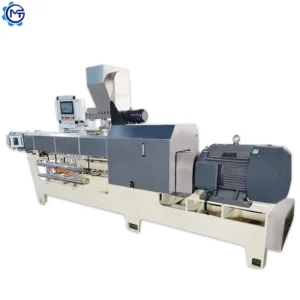
| Extruder Type | Single screw extruder |
| Model Options | MT100 / MT120 |
| Rated Power | 50–70 kW (electric heating); 50–60 kW (gas/diesel heating) |
| Voltage & Frequency | 380V/50Hz (3-phase) / 220V/50Hz (1-phase); customizable to local voltage |
| Control System | PLC-based with inverter (Delta or Delixi brand) |
| Motor Brand | Siemens (China-made) or equivalent top Chinese brand |
| Overall Dimensions (L×W×H) | 12,000–26,000 × 1,200 × 2,200 mm |
| Output Capacity | 120 kg/h (basis not stated in source — confirm raw material type, moisture content, and product shape) |
| Raw Materials | Wheat flour, corn starch, potato starch |
| Energy Options | Electricity / Gas / Diesel / Steam |
| Contact Material | Food-grade stainless steel 201/304 |
| Screw Configuration | High and low pressure screw (expands raw material range) |
| Product Shapes | Screw shell, round tube, square tube, ring, cartoon shapes (adjustable via die change) |
| Certification | CE / ISO 9001 |
| Warranty | 1 year with lifetime technical guidance |
Application Suitability
| Application | Material or Output |
|---|---|
| Secondary puffing fried snacks | Wheat flour and corn starch blends for vegetable rolls and salad strips |
| Golgappa / pani puri production | Potato starch and wheat flour mixtures requiring precise expansion control |
| Pasta-style fried shapes | Corn starch-based dough formed into rings, tubes, and cartoon shapes via die |
| Snack food line expansion | Existing producers adding a fried puffed format to their current portfolio |
What "120 kg/h Output" Means When Stations Are Mismatched
A line is only as fast as its slowest station, and nominal extruder ratings rarely reflect downstream reality.
I once helped a buyer who purchased an automatic fryer separately after their extruder vendor quoted a throughput number without considering the frying dwell time required for thicker dough shapes. The result was a conveyor pile-up between the cutting machine and the fryer infeed, with half-expanded半成品 cooling down and losing texture before they ever reached hot oil. The fried puffed snack production line equipment range you evaluate should show matched capacity at every transfer point, not just a headline figure at the extruder discharge. [NEED_CITE: Typical throughput bottleneck causes in multi-station snack lines]
How Screw Configuration Shapes Your Product Texture
The single-screw extruder in this fried puffed snack production line equipment range uses a high and low pressure screw arrangement that directly affects how starch gelatinises inside the barrel. Wheat flour and potato starch respond differently to shear and residence time, so the screw pitch and compression ratio must match the specific blend you intend to run. A configuration tuned for corn starch may leave wheat flour under-cooked at the die face, producing dense pieces that fail to expand during frying.
Die Selection and Shape Changeover on the Production Floor
The die-adjustable shaping system supports screw shells, round tubes, square tubes, rings, and custom cartoon shapes on one extruder. Changeover involves swapping the die plate and adjusting the pulling and cutting machine speed to match the new cross-section. The line layout should allocate space beside the extruder for die storage and a quick-access tool bench, so operators can complete a shape change without walking to a distant maintenance room. [NEED_CITE: Die changeover procedures for single-screw snack extruders]
Reading the Specs That Actually Determine Line Performance
The 50–70 kW rated power for electric heating and 50–60 kW for gas or diesel heating tells you how much thermal energy the extruder barrel can deliver per hour. Higher kW ratings matter when you run high-moisture doughs that need more energy to reach gelatinisation temperature before the die. The PLC-based control system with inverter drive allows operators to set and lock barrel zone temperatures, screw speed, and cutter timing as named recipes, reducing batch-to-batch variation when you switch between potato starch and wheat flour blends. Food-grade stainless steel 201 or 304 contact surfaces meet hygiene requirements for snack production, and the choice between grades typically depends on local food safety audit expectations and the chloride content of your seasoning blends. Overall dimensions spanning 12,000 to 26,000 mm in length mean the line footprint varies significantly depending on whether the cooling conveyor and packing station are included in the layout.
When the Fryer Becomes the Bottleneck You Didn’t Plan For
An automatic fryer sized only to the extruder’s nominal output will fall behind the moment you run a shape that requires a longer oil immersion time. Denser dough pieces like thick-walled tubes need more seconds in the oil than thin salad strips, and if the fryer belt cannot slow down independently of the extruder feed rate, product accumulates at the fryer infeed. The result is inconsistent oil pickup, uneven colour, and pieces that either absorb too much oil or emerge under-fried. [NEED_CITE: Fryer dwell time requirements for secondary puffing snack formats]
Why Sourcing the Full Line From One Supplier Matters
Every station — mixer, screw conveyor, single screw extruder, pulling and cutting machine, automatic fryer, automatic flavoring line, cooling, and packing — is specified together so that transfer conveyors match the discharge rate of the upstream unit. The screw configuration and die design are documented against your raw material before production begins, not copied from a generic build. An in-house testing workshop runs trial batches on your supplied flour or starch blend so you can evaluate product density, shape, and frying behaviour before the line ships. Multiple energy options for the fryer and dryer stages allow the line to match local utility costs, whether your facility has access to natural gas, diesel, steam, or relies on electric heating. The PLC control system can be configured with your local voltage, frequency, and operator interface language before dispatch, eliminating commissioning delays on your factory floor.
Documentation & Verification
- Line layout drawing showing station-by-station throughput matching for your target shape
- Screw and die configuration record specifying pitch and compression ratio for your flour blend
- Electrical schematic confirming voltage, frequency, and PLC interface language for your market
- Trial run report on your supplied raw material conducted in the testing workshop before shipment
- CE declaration of conformity and ISO 9001 certificate for the complete line
Installation, Commissioning & Support
- Floor plan requires 12,000–26,000 mm length with clear access on both sides for maintenance
- Dedicated electrical circuit sized for 50–70 kW extruder plus fryer and flavoring station loads
- Line arrives in modular sections; extruder barrel and conveyor frames bolt together on site
- First-run commissioning includes barrel temperature profiling and cutter timing calibration
- Operator training covers die changeover, PLC recipe storage, and fryer belt speed adjustment
- Wear parts list includes screw segments, die plates, and fryer mesh belt sections
What We Need From You Before Quoting
Send us the specific flour or starch blend you intend to run, including supplier data sheets if available, along with the target product shape and desired piece dimensions. Confirm your facility voltage, frequency, and whether your control operators need a specific interface language. Let us know your available energy sources so we can configure the fryer and any drying stages accordingly, and provide a rough workshop length so the layout can be drawn to your actual floor space.
Frequently Asked Questions
Q: How is the 120 kg/h capacity verified, and what raw material and product shape is it based on?
A: That figure is listed in the source without a stated raw material, moisture content, or product shape. We confirm actual throughput by running a trial on your supplied flour or starch blend in our testing workshop, measuring output at the packing station for your target shape before the quotation is finalised.
Q: How do I confirm voltage, frequency, and control panel language for my target market?
A: During the specification phase we collect your site electrical data and operator language preference. The PLC and inverter are then configured and tested at those settings before shipment, and the electrical schematic documents every confirmed parameter for your local electrician.
Q: Can the fryer and flavoring stations be matched to a different extruder output if I scale up later?
A: Each station is specified based on the extruder’s verified throughput at your target shape. If you plan a future capacity increase, we can design the fryer, seasoning drum, and cooling conveyor with headroom, or quote them as standalone units sized to a higher extruder model.
Q: What die configurations are available, and how quickly can shapes be changed on the production floor?
A: The extruder supports screw shell, round tube, square tube, ring, and cartoon shape dies. Operators swap the die plate and adjust the pulling and cutting machine parameters; a trained team typically completes a changeover within a planned production break.
Q: Is a trial run on my specific raw material possible before shipment, and what does the report include?
A: Yes, our in-house testing workshop runs your supplied material through the extruder, fryer, and flavoring stages. The trial report records extrusion temperatures, screw speed, frying time, final product density, and shape dimensions so you can evaluate results before the line leaves the factory.