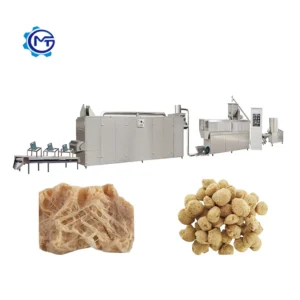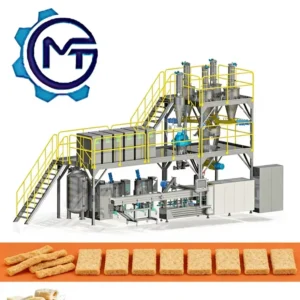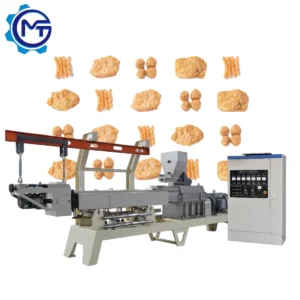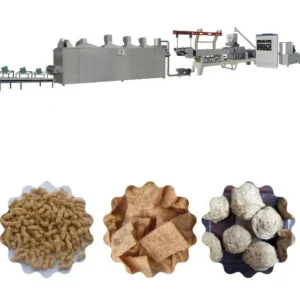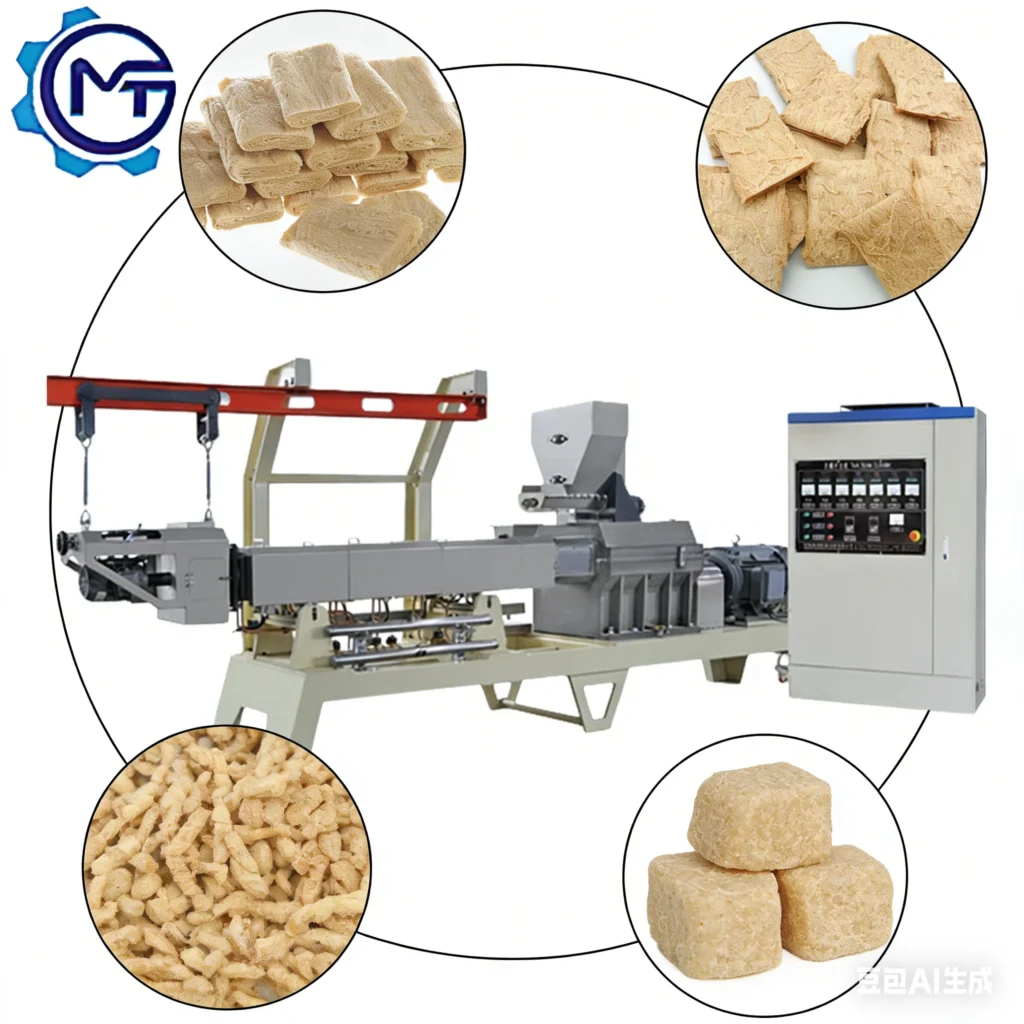
Station-by-Station Throughput Alignment — every unit on this twin screw extruder line, from mixer intake to dryer discharge, is configured to the same capacity target so no single node bottlenecks your TVP output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruder Production Line for Texturized Vegetable Protein (Plant-Based Meat) |
| Model Options | MT65 / MT70 / MT75 / MT85 |
| Screw Type | Twin Screw |
| Screw Length Options | 1050 mm / 1520 mm |
| Main Motor Power Options | 22 kW / 30 kW / 45 kW |
| Installed Power | 84 kW (MT65) / 160 kW (MT70) / 190 kW (MT75) / 210 kW (MT85) |
| Power Consumption | 59 kW (MT65) / 120 kW (MT70) / 140 kW (MT75) / 140 kW (MT85) |
| Output Capacity | 100–150 kg/h (MT65) / 150–200 kg/h (MT70) / 150–200 kg/h (MT75) / 250–300 kg/h (MT85) (basis to be confirmed — raw material, moisture and product format dependent) |
| Overall Dimensions (L×W×H) | 40000×1200×2200 mm (MT65) / 41000×1500×2200 mm (MT70) / 43000×1500×3200 mm (MT75) / 45000×1500×3500 mm (MT85) |
| Line Stations | Mixer → Screw Conveyor → Twin Screw Extruder → Air Conveyor → Multi-layer Dryer → Cooling Machine |
| Mixer Type | Vertical, stainless steel 304 mixing ruler, carbon steel shelf |
| Mixer Power Options | 4 kW / 7.5 kW / 15 kW |
| Mixer Capacity Options | 20–30 kg / 70–80 kg / 170–180 kg |
| Rotary Cutting Motor | 0.75 kW |
| Feeding Motor | 0.75 kW |
| Pump Motor | 0.37 kW |
| Heating Power Options | 10 kW / 14 kW |
| Dryer Drive | Double pitch roller chain drive, round-trip drying |
| Dryer Energy Options | Fuel / Gas / Electricity |
| Die Configuration | Interchangeable moulds for soya nuggets, TVP/TSP, soya chunks |
| Raw Materials | Defatted soya flour, low temperature soya flakes |
| Certification | CE (since 2014); ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Texturized vegetable protein (TVP/TSP) production | Defatted soya flour processed into fibrous protein structures |
| Soya nuggets and soya chunks | Low temperature soya flakes formed through interchangeable die plates |
| Plant-based meat analogues for industrial food manufacturing | TVP output sized and textured for meat product blending and fast food prep |
| Deep-freeze food production inputs | Extruded protein pieces dried and cooled to moisture levels suitable for frozen storage |
| Vegetarian and maigre snack bases | Shaped and textured protein formats for direct seasoning and packaging |
Why the Dryer Sizing Decides Whether Your Plant Based Meat Processing Line Actually Ships Product
An undersized dryer turns a rated extruder into a parking lot for wet, half-finished protein pieces.
I watched a processor in Surabaya commission a twin screw line where the extruder pushed material faster than the downstream dryer could handle moisture removal. The TVP came out gummy, clumped on the cooling belt, and had to be re-run. The extruder itself was never the problem — the mismatch between stations was. A properly configured plant based meat processing line sizes the multi-layer dryer belt length, airflow, and residence time to the exact moisture load the extruder delivers at its target throughput [NEED_CITE: moisture removal rates in multi-layer drying of extruded protein].
Barrel Sections and Screw Geometry That Shape Protein Fibre Formation
The twin screw extruder on this plant based meat processing line uses configurable screw lengths — 1050 mm or 1520 mm — which directly control residence time inside the barrel. Longer screw sections give defatted soya flour more time under heat and shear, allowing the protein molecules to align into the layered, meat-like fibre structure that buyers expect from TVP. The screw configuration is not generic; it is specified to the raw material behaviour and the target chunk or nugget format before production begins.
Die Plate Selection Across Nugget, Chunk, and Mince Formats
The interchangeable mould system lets a single extruder platform produce soya nuggets, soya chunks, and TSP in different cross-sections and densities. Each die plate changes the expansion ratio and surface texture of the exiting protein matrix. This matters because a fast food supplier wants a chunk that holds together during frying, while a frozen food manufacturer needs a mince-grade output that blends into patty formulations. Switching formats means swapping the die and adjusting the cutter speed — not replacing the extruder.
Reading the Power and Capacity Figures Correctly
Installed power ranges from 84 kW on the MT65 to 210 kW on the MT85, but actual power consumption sits lower — 59 kW to 140 kW across the range. The gap exists because heating elements, main drive, and feeder motors do not all draw peak current simultaneously during steady-state operation. Output capacity figures (100–150 kg/h for the MT65, scaling up to 250–300 kg/h for the MT85) depend entirely on raw material moisture content, die configuration, and the specific TVP format being produced. Always confirm capacity against your own defatted soya flour specification and target product shape [NEED_CITE: throughput variance in TVP extrusion based on raw material moisture and die geometry].
What Happens When Stations Are Sourced Separately
Purchasing an extruder from one vendor and a dryer from another often means the dryer’s belt width, airflow volume, and thermal capacity were never calculated against the extruder’s actual output rate. The result is a line that idles at half speed because the dryer cannot keep up, or worse, protein pieces that exit with internal moisture pockets that promote spoilage during storage. Matching throughput across every station — mixer batch size, screw conveyor feed rate, extruder output, dryer residence time, and cooling belt speed — prevents these imbalances before the line ships [NEED_CITE: throughput matching in integrated extrusion line design].
Why This Equipment Range Fits Integrated TVP Projects
Every station on this line is available from a single equipment catalogue, so the mixer capacity, extruder throughput, and dryer belt length are calculated together rather than assembled from independent quotations. The screw configuration and die design are specified to your raw material — whether defatted soya flour or low temperature soya flakes — and the target product format. An in-house testing workshop runs trial production on your actual material before the line leaves the factory. The multi-layer dryer offers fuel, gas, or electric heating, selected based on your facility’s available utilities. Electrical schematics, voltage, and frequency are confirmed to your market before production starts, so the control panel speaks the right language and the motors spin the right direction on day one.
Documentation & Verification
- Line layout drawing showing station-by-station throughput matching for your target TVP output rate
- Screw and die configuration record specifying geometry to your defatted soya flour or soya flakes
- Trial run report produced on your raw material in the in-house testing workshop before shipment
- Electrical schematic with confirmed voltage, frequency, and control language for your facility
- Factory test record documenting actual run conditions and output quality before dispatch
- CE declaration of conformity and ISO certificate included in the shipping documentation package
Installation, Commissioning & Support
- Foundation and floor space planning based on the line’s overall dimensions, up to 45000×1500×3500 mm for the MT85 configuration
- Dedicated electrical circuit sizing matched to installed power draw, up to 210 kW for the largest model in the range
- Factory-assembled stations delivered for sequential positioning, with air conveyor and dryer sections aligned on-site
- First-run commissioning including screw speed, barrel temperature profile, and die pressure calibration for your TVP format
- Operator training covering die changeover, dryer temperature adjustment, and mixer batch timing for consistent output
- Wear parts list covering screws, dies, and cutting blades with recommended replacement intervals
What to Include in Your Inquiry
Specify the raw material you plan to process — defatted soya flour, low temperature soya flakes, or a blend — along with the protein content and moisture level from your supplier’s certificate of analysis. State your target product format (nuggets, chunks, or mince-grade TVP) and the hourly output rate your downstream packaging or blending operation requires. Confirm the voltage, frequency, and preferred control language at your facility, and whether your site supports fuel, gas, or electric heating for the dryer section.
Frequently Asked Questions
Q: How is output capacity verified on my specific raw material and product format?
A: The in-house testing workshop runs your actual defatted soya flour or soya flakes through the twin screw extruder with the die plate matched to your target format. A trial run report documents throughput, product texture, and moisture content at discharge. This report ships with the line so you know the confirmed capacity before installation begins.
Q: How are dryer capacity and extruder throughput matched to prevent line bottlenecks?
A: The multi-layer dryer belt length, airflow volume, and thermal input are calculated against the extruder’s moisture output at your confirmed production rate. The round-trip drying path and adjustable temperature zones ensure that protein pieces reach the target moisture level before entering the cooling machine, preventing downstream clumping or spoilage.
Q: What die and screw configurations are available for different TVP and soya chunk formats?
A: Interchangeable moulds cover soya nuggets, soya chunks, and TSP in various cross-sections. The screw configuration — including element arrangement and total length of 1050 mm or 1520 mm — is specified to your raw material and desired fibre density. Configuration records are documented before production and included in your delivery package.
Q: Which energy sources does the multi-layer dryer support and how is the choice made?
A: The dryer accepts fuel, gas, or electric heating. The selection depends on your facility’s available utilities, local energy costs, and the thermal demand calculated from your production rate. This choice is confirmed during the line configuration stage so the correct heating system is installed before the dryer ships.
Q: What voltage, frequency, and control language options are confirmed before shipment?
A: Electrical schematics are reviewed and confirmed against your site’s power supply before production begins. Motor ratings, heating element specifications, and control panel language are set to match your local standards, preventing commissioning delays caused by incorrect voltage or unreadable interface labels [NEED_CITE: voltage and frequency standards by export market].