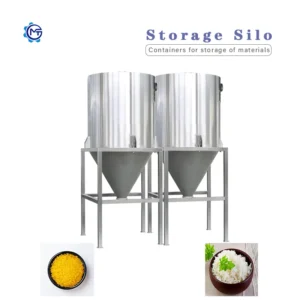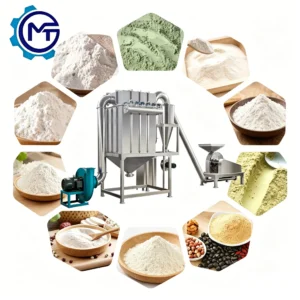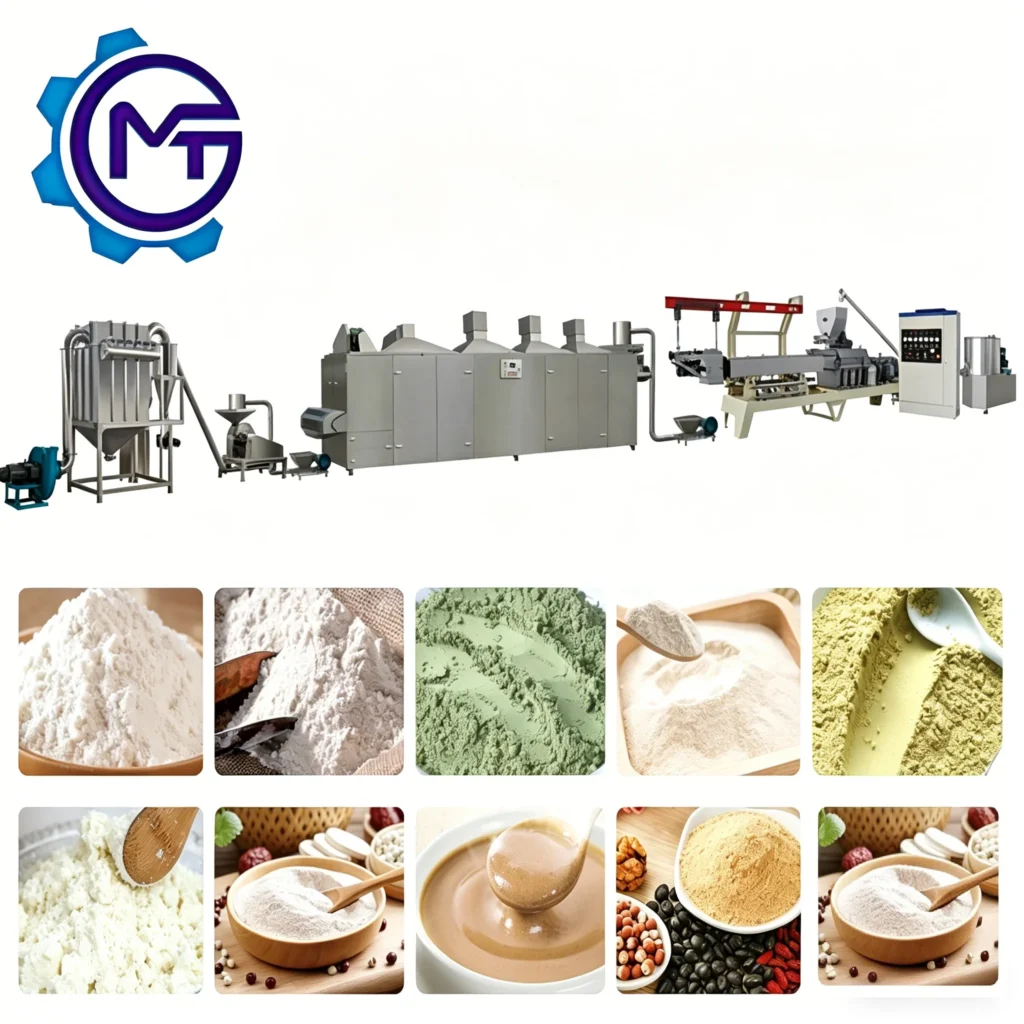
Balanced Throughput Across Stations — every mixer, extruder, dryer and packing unit in this nutritional powder processing line is sized to your actual grain formulation, preventing the bottleneck that happens when vendors size to generic capacity charts.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Nutritional Powder Processing Line |
| Output Capacity | 200-500 kg/h (basis not stated in source — confirm raw material / moisture content) |
| Construction Material | Food-Grade 304 Stainless Steel |
| Control System | PLC with Touch Control Panel & Digital System |
| Heat Source Options | Electric / Gas / Steam |
| Raw Materials Processed | Rice, Corn, Beans, Various Grains |
| Warranty | 1 Year |
| After-Sales Support | Overseas Engineer Service |
| Key Line Stations | Baking Ovens, Mixers, Extruders, Dryers |
| Language Options | (basis to be confirmed) |
| Voltage & Frequency | (basis to be confirmed) |
| Screw Type | (basis to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| Infant cereal and baby food production | Rice, corn, oat and blended grain formulations |
| Fortified food powder for nutrition programmes | Grain blends with added vitamin and mineral premixes |
| Contract manufacturing across multiple recipes | Switching between rice, corn, beans, and multi-grain mixes on one line |
| Porridge and weaning food manufacturing | Fine-milled cereal powders requiring controlled gelatinisation |
Why Your Raw Material Report Matters More Than the Brochure Capacity
A nutritional powder processing line full equipment range is only as reliable as the material data used to size it.
I spent years doing aftermarket commissioning on grain-based extrusion lines across Latin America, and the most expensive delays never came from mechanical faults. They came from recipe mismatches. In Peru, a baby cereal line stalled on day one because the customer’s bean flour had a protein content far higher than the test sample we ran back at the factory. The die blocked within minutes, the screw profile was wrong for that viscosity, and we waited two weeks for replacement parts to arrive from China [NEED_CITE: impact of raw material variability on extrusion screw configuration]. When I moved into specifying lines for buyers, the first document I requested was always the actual lab analysis of their grain supply — not the generic recipe they found online. That single step eliminates the most common cause of commissioning failure on cereal and nutrition powder lines.
Mapping Every Station in the Nutritional Powder Processing Line Full Equipment Range
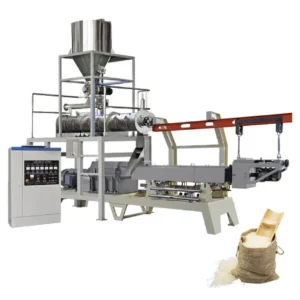
Buyers evaluating a cereal powder line need to see the complete machine catalogue — not just the extruder. This line covers batching and mixing upstream, extrusion as the core transformation step, drying to reach target moisture, and packing downstream. Each station is selected so that the throughput of one does not starve or flood the next. The PLC touch control panel ties the sequence together, giving operators a single digital interface rather than separate controls scattered across the floor.
How Heat Source Selection Changes the Dryer Specification
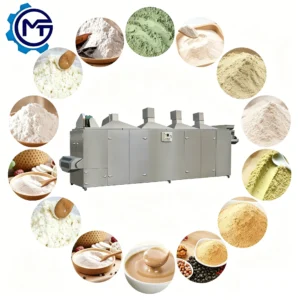
The drying stage is where many powder lines lose their rhythm. This line offers electric, gas, or steam heating, and the choice depends entirely on what your factory already has available. A steam-heated dryer integrates with an existing boiler plant and keeps running cost predictable in regions where natural gas is volatile. An electric dryer suits smaller facilities or markets where industrial gas infrastructure is unreliable [NEED_CITE: industrial dryer heat source selection criteria for food processing]. The food-grade 304 stainless steel construction across contact surfaces means the dryer interior can be washed down between recipe changes without corrosion risk, which matters when a contract manufacturer switches from a corn-based baby cereal to a bean-based formula on the same shift.
Reading the Specifications That Actually Affect Your Powder Quality
The screw type — single or twin — determines how aggressively the grain matrix is sheared and cooked. Twin-screw setups handle higher-moisture doughs and protein-rich bean blends with less risk of surge, while single-screw extruders are simpler to maintain on straightforward rice or corn recipes. The PLC control system governs barrel temperature zones and screw speed, which together set the degree of starch gelatinisation. Under-cooked starch means the powder will not dissolve properly in water when the end consumer prepares it; over-cooked starch destroys heat-sensitive vitamin premixes added to fortified products. The 304 stainless steel contact material is not just a hygiene checkbox — it prevents iron contamination that can discolour light-coloured rice cereal and trigger metal detector rejects at the packing station [NEED_CITE: food contact material standards for infant food processing equipment]. Capacity figures of 200-500 kg/h must be confirmed against your specific grain blend and target moisture, since a high-protein bean formulation will extrude at a lower mass throughput than a pure corn grit recipe under identical screw speed.
What Happens When Stations Are Sized to Catalogue Numbers Instead of Your Recipe
When an extruder is selected for its nominal output but the dryer is picked from a different vendor’s brochure, the dryer often becomes the constraint. Powder exits the extruder at high moisture and must be reduced to a shelf-stable level within a defined residence time. If the dryer is undersized, powder piles up on the belt, dries unevenly, and clumps before it reaches the packing station [NEED_CITE: moisture migration defects in extruded cereal powder drying]. The reverse problem — an oversized dryer — wastes energy and can over-dry the outer layer while the core remains too moist, leading to caking in the bag weeks after packing.
Why Buyers Specify Their Next Line Here
Every station from mixer to packer is sourced from one supplier, so throughput calculations are cross-checked rather than assumed from individual machine brochures. Screw configuration and die design are specified to your actual grain report, not copied from a standard build. Before shipment, your raw material runs in the in-house testing workshop, generating a trial report that confirms output and powder texture. The PLC control language, voltage and frequency are confirmed before production begins, so the line powers up correctly the day your overseas engineer arrives. Spare screws, dies and dryer belts are documented and shipped with the first container so your first replacement cycle never waits on a backlog.
Documentation & Verification
- Line layout and capacity calculation matched to your grain blend and target moisture
- Machine specification sheet for each station with confirmed voltage and frequency
- Trial run report produced on your supplied raw material before shipment
- Screw and die configuration record documenting the profile used for your recipe
- Food-grade 304 stainless steel material certificates for all product contact surfaces
- Operation and maintenance manual with PLC screen translations in your language
Installation, Commissioning & Support
- Foundation and floor space plan confirming footprint for mixer, extruder and dryer sequence
- Dedicated electrical circuit sizing based on confirmed total kW draw and voltage
- Modular shipping configuration allowing container-level assembly on your workshop floor
- First-run parameter log capturing barrel temperature, screw speed and dryer residence time
- Operator training on PLC touch interface covering recipe storage and fault diagnostics
- Wear parts kit including initial spare screws, dies and dryer belt sections shipped with line
What to Include in Your Inquiry
To size this nutritional powder processing line correctly, share your grain formulation with protein and moisture percentages, your target daily output in kilograms, and the voltage and frequency at your facility. If you run multiple recipes, list each one so the screw profile and die selection can accommodate the full range. Let us know whether you prefer electric, gas or steam heating for the dryer, and whether your packing hall has existing upstream conveyors the line must connect to.
Frequently Asked Questions
Q: How is the 200–500 kg/h capacity confirmed for my specific grain blend?
A: We request your raw material lab report showing protein, fat and moisture content, then run a trial on that exact blend in our testing workshop. The resulting trial report documents actual throughput and powder quality, so the capacity figure you receive is tied to your recipe, not a generic catalogue value.
Q: Which stations are included and how is throughput balanced between them?
A: The line covers mixing, extrusion, drying and packing support equipment. Each station is sized using a shared capacity calculation so the extruder output matches dryer belt loading and packing speed, avoiding the common problem where one station starves or floods the next.
Q: Can the line handle rice, corn and bean formulations on the same equipment?
A: Yes, but the screw configuration and die selection must be specified to cover your full recipe range. High-protein bean blends behave differently from pure rice or corn during extrusion, so the profile is designed for your most demanding formulation and tested across all recipes before shipment.
Q: What electrical and control details are confirmed before the line is built?
A: Voltage, frequency, PLC control language and heat source type for the dryer are all confirmed during the specification stage. This prevents the common delay where a line arrives on site and the control panel displays a language your operators cannot read or the motor voltage does not match your supply.
Q: What trial runs happen before the line ships?
A: We run your actual raw material through the extruder and dryer in our testing workshop and document throughput, moisture content and powder texture in a trial report. This means product development starts before you receive the machines, not after installation.