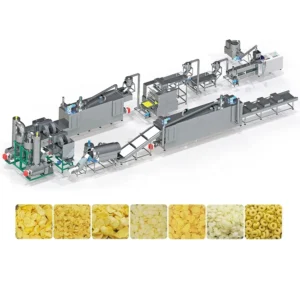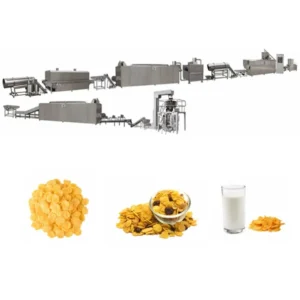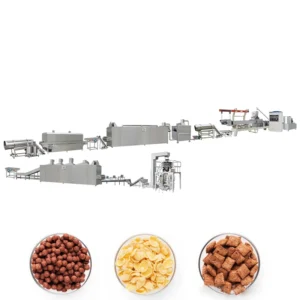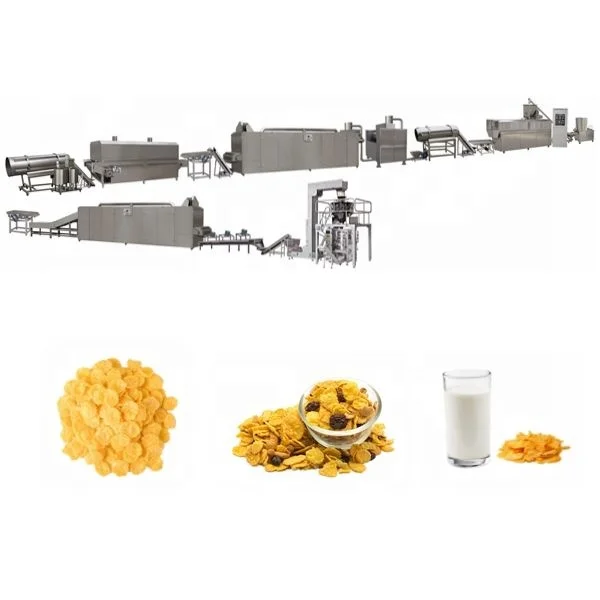
Integrated Line Stations — throughput between the extruder, press, and dryer is calculated together so no single station bottlenecks the corn flakes output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Model | MT65 / MT70 / MT85 |
| Installed Power | MT65 70 kW / MT70 100 kW / MT85 200 kW |
| Real Power Consumption | MT65 40 kW / MT70 70 kW / MT85 150 kW |
| Output Capacity | MT65 100–150 kg/h (basis to be confirmed) / MT70 200–240 kg/h (basis to be confirmed) / MT85 300–400 kg/h (basis to be confirmed) |
| Overall Dimensions (L×W×H) | MT65 20000×1200×2200 mm / MT70 25000×1500×2200 mm / MT85 30000×3500×4300 mm |
| Screw Type | Twin-screw, co-rotating, sectional modules |
| Screw Material | 38CrMoAL alloy, nitriding process |
| Motor | SIEMENS (China) |
| Inverter | Delta |
| Control System | Control box (PLC / MCC available on request) |
| Feeding System | Food-grade stainless steel twin-screw feeder with variable-speed converter |
| Gearbox | Automatic lubrication function |
| Cutting System | Knife fixed in die head seat, rotary cutting by V-belt drive |
| Corn Flakes Press Machine Power | 16.12 kW |
| Corn Flakes Press Machine Roller | 510×310×1050 mm |
| High-Temperature Oven Size | 4.5×1.4×1.8 m |
| High-Temperature Oven Heating | Gas, both-side baking system |
| Sugar Spraying System Power | 28.75 kW |
| Sugar Spraying System Roller | Ø600×2700 mm |
| Dryer Type | Multilayer (3 / 5 / 7 layer options), electric or steam |
| Dryer Temperature Range | 0–200 °C |
| Line Stations | Mixer, screw conveyor, extruder, press machine, high-temperature oven, sugar spraying system, cooling conveyor, sifter, packing machine |
| Warranty | 1 year |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Crispy corn flakes for breakfast cereal retail | Maize and corn grits |
| Multigrain breakfast flakes | Rice, wheat, oat, and rye blends |
| Sugar-coated and honey-coated cereal flakes | Grain flakes with syrup or sugar spray |
| Fortified breakfast cereal production | Grain base with added nutritional premix |
| Private-label cereal contract manufacturing | Various grain inputs matched to buyer specification |
What "Output Capacity" Means When the Raw Material Changes
A rated capacity figure is only meaningful when tied to the exact grain variety, moisture level, and starch content you will actually feed into the hopper.
Over the years I have watched corn flakes lines stall not because the extruder was undersized, but because the maize arriving at the factory had a different starch profile than the sample used during quotation. The gelatinisation window shifts, the dough viscosity changes inside the barrel, and the press rollers receive a sheet that tears instead of flattening cleanly. This is why every breakfast cereal corn flakes machine complete equipment range we quote starts with a raw-material confirmation step rather than a catalog number [NEED_CITE: grain starch variability across harvest regions].
How Each Station Fits the Corn Flakes Process
A corn flakes line is a sequence of thermal and mechanical stages. The mixer hydrates the grits uniformly, the twin-screw extruder gelatinises the starch under controlled shear, and the press machine flattens the cooked pellets into thin sheets. Downstream, the high-temperature oven toasts both sides simultaneously, and the multilayer dryer brings residual moisture down to a shelf-stable level. Specifying any one of these stations in isolation leaves gaps that surface only during continuous production.
Matching Dryer and Coating Capacity to Extruder Output
The most common mismatch I see in breakfast cereal corn flakes machine complete equipment range inquiries is a dryer sized for the extruder’s nominal output while the sugar spraying system runs at a different throughput. When coating takes longer than drying, flakes queue up on the cooling conveyor, absorb ambient humidity, and lose crispness before packing. The sugar spraying system here uses an Ø600×2700 mm roller and 28.75 kW of heating capacity, and its cycle time is factored against the extruder’s real throughput so the line holds a steady rhythm [NEED_CITE: thermal balance in cereal drying and coating stages].
Reading the Screw and Barrel Specifications
The twin-screw, co-rotating design with sectional modules allows the screw profile to be rearranged as the grain type or target flake texture changes. The 38CrMoAL nitrided alloy resists abrasion from coarse maize grits over extended runs. The automatic lubrication gearbox reduces unplanned stops during long production campaigns. SIEMENS motors paired with Delta inverters give operators fine control over screw speed, which directly affects residence time and the degree of starch gelatinisation inside the barrel — a critical variable when switching between corn, wheat, and oat formulations.
The Hidden Cost of Skipping Pre-Shipment Trials
When a line ships without a trial run on the buyer’s actual grain, the first week of commissioning becomes an expensive experiment. Die openings may need resizing, press roller gaps require recalibration, and oven temperature profiles have to be rewritten from scratch. Each adjustment means hours of off-spec product that cannot be sold. Running the buyer’s raw material through the extruder and press before dispatch catches these mismatches while changes are still inexpensive [NEED_CITE: cost of post-installation rework in food extrusion projects].
Why Source the Full Range Here
Every station from the mixer to the packing machine is spec’d under one supplier, so throughput figures are calculated against the same production target rather than assembled from separate vendor catalogs. The corn flakes press machine, high-temperature oven, and sugar spraying system are dimensioned to match the extruder model chosen, eliminating the bottleneck risk that arises when stations are procured independently. Screw configuration and die design are matched to the buyer’s grain and target flake density. An in-house testing workshop allows trial runs on customer-supplied raw material before the line leaves the factory. Pre-sales engineering through on-site commissioning and ongoing wear-part supply keeps the project continuous from first inquiry to steady-state production.
Documentation & Verification
- Line layout and capacity calculation covering every station from mixer to packing machine
- Machine specification sheet with screw and die configuration record for your grain type
- Electrical schematic with voltage and frequency confirmed for your target market
- Trial run report on your actual maize or multigrain raw material before shipment
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Operation and maintenance manual with wear parts list for press rollers and screws
Installation, Commissioning & Support
- Foundation plan accounts for the MT85’s 30-meter line length and 4300 mm headroom requirement
- Dedicated electrical circuit sized to the model’s real power draw, up to 150 kW for the MT85
- Stations ship in modular sections for container loading and on-site reassembly
- First-run parameter setting covers extruder screw speed, press roller gap, and oven temperature profile
- Operator training on control box interface, inverter adjustment, and daily lubrication checks
- Wear parts list with lead times for screws, dies, and press rollers from first replacement onward
What We Need to Spec Your Line
To prepare an accurate breakfast cereal corn flakes machine complete equipment range proposal, share the grain variety you will process, its typical moisture content, and the flake thickness your market expects. Include your target hourly output, workshop dimensions, and the local voltage and frequency standard so the electrical package matches your facility. If you have existing upstream milling or downstream packing equipment, note the interface points so the new stations integrate without modification.
Frequently Asked Questions
Q: How is output capacity verified for each extruder model?
A: Capacity depends on grain starch content, moisture level, and target flake density. We confirm these variables during pre-sales consultation and run a trial on your raw material in our testing workshop. The resulting trial report documents actual throughput, giving you a verified figure rather than a generic catalog value.
Q: Which dryer configuration matches the extruder throughput for corn flakes?
A: The multilayer dryer is available in three, five, or seven layers with electric or steam heating. Layer count and belt speed are selected so the dryer’s residence time aligns with the extruder and press output, preventing flakes from queuing and absorbing moisture before packing.
Q: How are voltage and control language confirmed before shipment?
A: During specification confirmation we record your facility’s voltage, frequency, and preferred control language. The electrical schematic and control box configuration are then built to match. This step prevents commissioning delays caused by mismatched power supplies or untranslated operator interfaces.
Q: How are screw and die configurations matched to different grains?
A: The co-rotating twin-screw extruder uses sectional modules that can be rearranged. For coarse maize grits we select a screw profile that extends residence time for full gelatinisation. For softer grains like oat, a gentler profile prevents over-shearing. Die openings are sized to produce pellets that press into the target flake thickness.
Q: What spare wear parts should be on hand for the first year?
A: Screws, dies, and press rollers experience the highest abrasion during corn flakes production. We supply a wear parts list with recommended first-replacement intervals based on your grain type and daily run hours, so spares are available before the originals reach end of service.