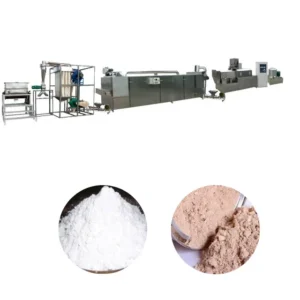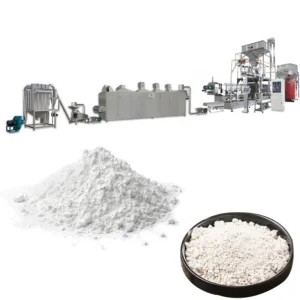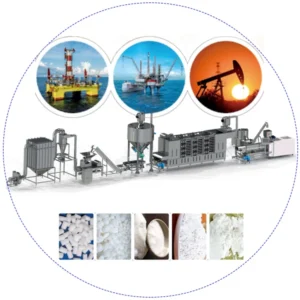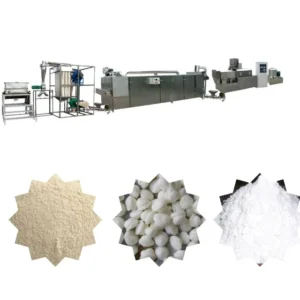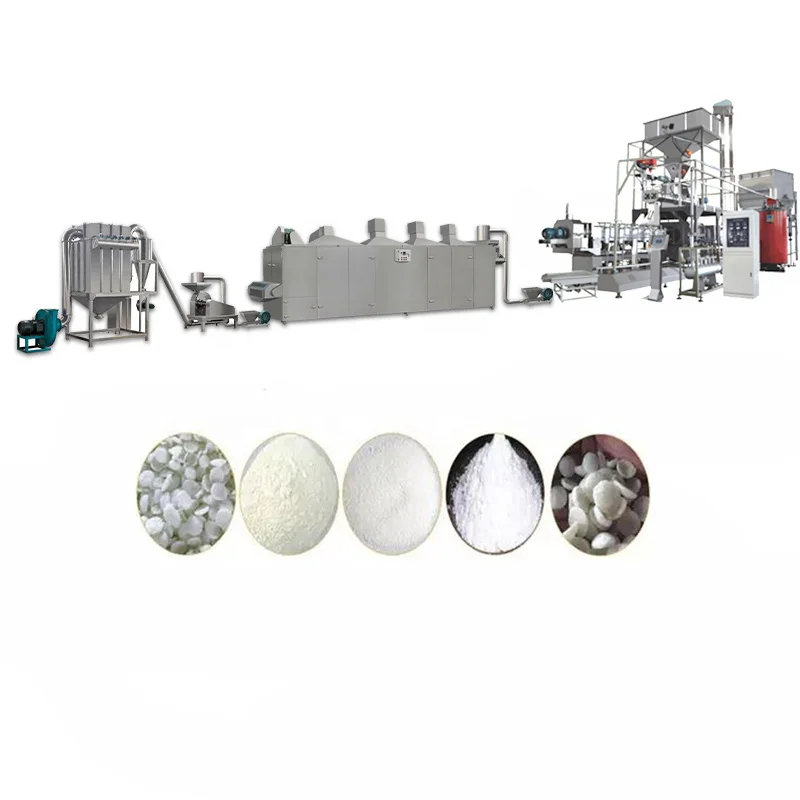
Complete turnkey configuration under one supplier — Every station in a modified starch production line, from batching and mixing through extrusion, drying, grinding, and packing, is throughput-matched and sourced from a single point of responsibility.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Modified Starch Production Line |
| Extruder Type | Twin Screw |
| Available Extruder Models | MT85, MT100, MT110, MT135 |
| Installed Power | MT85: 90 kW; MT100: 180 kW; MT110: 200 kW; MT135: 240 kW |
| Real Power Consumption | MT85: 63 kW; MT100: 120 kW; MT110: 150 kW; MT135: 165 kW |
| Output Capacity | MT85: 100–200 kg/h; MT100: 500–600 kg/h; MT110: 500–600 kg/h; MT135: 1000–1500 kg/h (basis: corn starch / tapioca starch / potato starch — exact raw material and moisture condition not stated in source, confirm with supplier) |
| Control System | Frequency speed controlling system |
| Heating Source Options (Dryer) | Electric, steam, or gas |
| Grinding Fineness | < 10 mm |
| Grinder Construction | Stainless steel 304 food-contact parts, bottom butterfly valve discharge |
| Extruder Lubrication | Automatic lubricating and cooling system |
| Processing Flow | Materials preparation → Blending → Mixing → Extruding → Drying → Grinding → Packing |
| Construction Materials | Food-grade stainless steel on contact parts |
| Warranty | 1 year |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Modified starch for textile sizing | Corn starch or tapioca starch treated for viscosity control |
| Pre-gelatinized starch for instant food blends | Potato starch or corn starch processed for cold-water solubility |
| Modified starch for oil drilling fluids | High-viscosity starch substrates requiring thermal and shear modification |
| Modified starch for paper coating | Corn starch modified for surface adhesion and film formation |
| Pre-gelatinized starch for construction materials | Tapioca or corn starch for dry-mix mortar and wallboard additives |
When the Extruder Outruns Everything Downstream
Matching throughput across every station prevents the most expensive bottleneck in a modified starch production line — the one nobody quotes.
I once watched a starch processor in Southeast Asia bring a newly installed line online, only to find the extruder pushing material faster than the dryer could remove moisture. Wet, sticky clumps accumulated at the dryer infeed, and operators had to manually throttle the extruder speed to keep up. The line ran at a fraction of its rated capacity for weeks until a larger dryer was shipped in. The extruder was never the problem. The gap between stations was [NEED_CITE: line throughput matching across extrusion and drying stages].
On this modified starch production line full equipment range, every station — mixer, extruder, dryer, grinder — is sized so that the throughput ceiling of the slowest station never strangles the rest.
The Full Equipment Catalogue at a Glance
This modified starch production line full equipment range covers every station a processor needs, from raw material blending through final grinding and packing. The mixer feeds a twin-screw extruder where starch undergoes controlled thermal and mechanical treatment. Downstream, the dryer or roaster removes residual moisture before the grinder reduces the product to the target particle fineness.
How Heating Source Selection Affects Your Dryer Station
The drying stage determines how quickly the line can move material from extrusion to grinding. Choosing between electric, steam, or gas heating depends on what your facility already has available. A plant running a boiler for other processes can route steam into the dryer at lower operating cost, while a standalone facility may find gas or electric more practical. Specifying the heating source before production avoids costly retrofitting after the line is commissioned [NEED_CITE: industrial drying energy source selection criteria].
Why Screw Configuration Matters More Than Motor Size
Twin-screw extrusion relies on the interplay between screw element geometry, barrel temperature, and raw material moisture to achieve the right degree of starch gelatinization and modification. A screw combination optimized for corn starch may not handle tapioca starch well — tapioca develops higher viscosity under shear, which can overload the motor or produce inconsistent gelatinization if the screw profile is not adjusted. The automatic lubricating and cooling system on the extruder helps maintain stable barrel temperatures across long production runs, but it cannot compensate for a mismatched screw configuration.
The grinder downstream uses stainless steel 304 contact parts with a bottom butterfly valve discharge, producing particle fineness below 10 mm. This fineness level is important for applications like instant food blends or construction additives where lump-free dispersion in cold water is expected. The frequency speed controlling system on the extruder allows operators to fine-tune screw speed in response to material behavior, which supports batch-to-batch consistency [NEED_CITE: twin-screw extrusion parameters for starch modification].
The Hidden Cost of Unmatched Stations
When a buyer assembles a line from separate vendors, each supplier quotes their own machine at its best-case output. The mixer may be rated for a certain batch size, the extruder for a continuous throughput, and the dryer for a given evaporation rate — but those numbers rarely align perfectly. The result is a line that technically runs but never reaches the throughput any single station was sold on. Operators spend their shifts adjusting feed rates and clearing blockages instead of monitoring product quality [NEED_CITE: production line bottleneck analysis in food processing].
Why Buyers Source the Full Range Here
The extruder, dryer, grinder, and every supporting station come from one supplier, so throughput calculations are done across the entire line rather than per machine. Screw configuration and die design are specified to the buyer’s actual starch source and target modification level, not copied from a generic build. Before shipment, raw material trials run in the in-house testing workshop to verify output and product quality. Electrical schematics confirm voltage and frequency to the buyer’s local grid before the control cabinets are wired. Wear parts lists cover screws, dies, and grinder components with replacement intervals mapped out.
Documentation & Verification
- Line layout showing throughput calculation for each station on your starch type
- Machine specification sheet per station: extruder, dryer heating source, grinder discharge
- Screw and die configuration record matched to your raw material
- Electrical schematic with voltage and frequency locked to your site grid
- Factory trial run report on your starch sample before dispatch
Installation, Commissioning & Support
- Foundation and floor plan based on the selected extruder model footprint and dryer length
- Dedicated power circuit sized to the real consumption figure, not the installed peak
- On-site assembly with station-by-station alignment checks before line startup
- First-run parameter setting covering screw speed, barrel zones, and dryer temperature
- Operator training on frequency speed controls and automatic lubrication monitoring
- Wear parts kit with screws, dies, and grinder screen included for the first replacement cycle
What to Include in Your Inquiry
Provide the specific starch source you intend to process — corn, tapioca, potato, or another substrate — along with the target modification type and your required daily output. Share your facility’s available heating infrastructure (boiler, gas line, or electric capacity) and the local voltage and frequency so the dryer and control system can be configured correctly. If you have existing upstream or downstream equipment that must integrate, include those specifications as well.
Frequently Asked Questions
Q: What stations are included in the full modified starch processing line?
A: The line covers material preparation, blending, mixing, twin-screw extrusion, drying or roasting, grinding, and packing. Each station is sized so that throughput aligns across the entire sequence, preventing any single machine from becoming a bottleneck. Supporting conveyors and cooling equipment are included as needed.
Q: How is capacity matched between the extruder, dryer, and grinder?
A: Throughput is calculated based on the buyer’s raw material and target moisture content at each stage. The dryer evaporation rate and grinder feed rate are selected to handle the extruder’s actual output on that specific starch, so no station forces another to slow down.
Q: Which heating options are available for the drying station?
A: The dryer can be configured for electric, steam, or gas heating. The choice depends on the buyer’s existing utility infrastructure and local energy costs. Steam is common in facilities with a central boiler, while gas or electric suits standalone installations.
Q: What materials are used on food-contact parts across the line?
A: All food-contact surfaces use food-grade stainless steel. The grinder contact parts are specifically stainless steel 304, and the extruder barrel and screw elements are selected for food-grade compliance. This supports hygiene standards required in starch processing for food and industrial applications.
Q: How do I select the right extruder model for my target output?
A: Model selection depends on your required hourly throughput and the specific starch you are processing. Different starches behave differently under shear and heat, so the same model may deliver different actual outputs on corn versus tapioca starch. A trial run on your material confirms the right model and screw configuration.