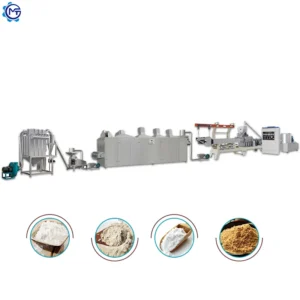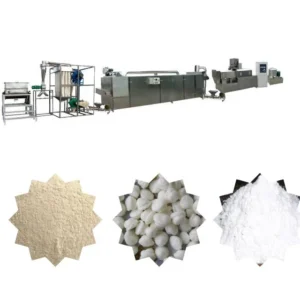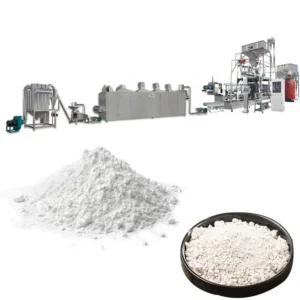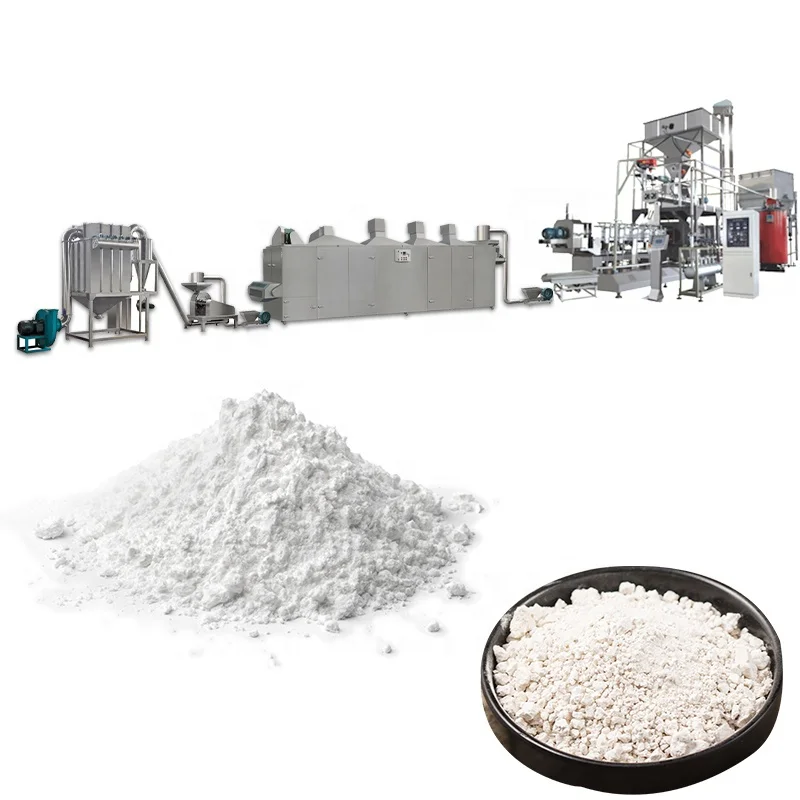
Integrated Extruder-to-Grinder Throughput — Each station in the MT70/MT85/MT75 modified starch processing line is matched by mass flow rate rather than assembled from isolated vendors, preventing the dryer or grinder from becoming an unseen bottleneck once the twin-screw reaches full barrel fill.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Modified Starch Extrusion Production Line |
| Available Models | MT70 / MT85 / MT75 |
| Extruder Type | Twin-screw, 38CrMoAl alloy screws |
| Installed Power | 160 kW (MT70) / 190 kW (MT85) / 210 kW (MT75) |
| Power Consumption | 120 kW (MT70) / 140 kW (MT85) / 150 kW (MT75) |
| Output Capacity | 150–200 kg/h (MT70) / 300–400 kg/h (MT85) / 300–500 kg/h (MT75) (basis not stated in source — confirm raw material type, moisture content and starch modification degree before specification) |
| Barrel Heating | 7 zones, 14 kW total (MT70) |
| Barrel Cooling | Integrated water/air cooling circuit |
| Mixer Batch Capacity | 20–30 kg / 70–80 kg / 170–180 kg options available |
| Mixer Contact Material | 201 SS or 304 SS options |
| Dryer Configuration | 5-layer baking oven, gas or diesel heated |
| Dryer Dimensions | 5000 × 1200 × 2300 mm |
| Grinder Type | Pulse grinder with cyclone discharge and dust collector |
| Voltage | 380 V / 50 Hz, three-phase (destination market voltage to be confirmed) |
| Line Dimensions (L×W×H) | 41000 × 1500 × 2200 mm (MT70) / 43000 × 1500 × 3200 mm (MT85) / 45000 × 1500 × 3500 mm (MT75) |
| Certification | CE (certified since 2014) |
Application Suitability
| Application | Material or Output |
|---|---|
| Pre-gelatinized cassava starch for food-grade binding and thickening | Native cassava starch, adjusted moisture feed |
| Pre-gelatinized corn starch for instant food and nutritional powders | Corn starch with target gelatinisation degree |
| Denatured starch for oil-drilling fluid-loss additives | Modified corn or potato starch, heat-stable formulation |
| Industrial modified starch for textile sizing and paper coating | Chemically treated starch feed requiring controlled expansion and particle size |
What a Modified Starch Processing Line Manufacturer Often Leaves Out of the Quotation
The capacity figure on the proposal only holds true when the raw material matches the test conditions — and starch sources rarely do.
I spent a week on-site in Southeast Asia re-tuning a pre-gelatinized cassava starch line because the customer’s local tuber supply carried a lower amylose fraction than our standard trial material. Gelatinisation onset shifted, expansion collapsed, and the powder that came off the grinder looked nothing like the sample. A modified starch processing line manufacturer quoting a single throughput number without naming the feed moisture, amylose ratio, and modification chemistry is handing you a best-case scenario, not a guaranteed output [NEED_CITE: variability of native starch amylose content across crop regions]. The extruder barrel profile, screw pitch sequence, and die land length all need to be re-derived from the buyer’s actual material before the line ever leaves the factory floor.
Gelatinisation Control Through Barrel Zone Profiling
Starch granule disruption requires holding the melt above the gelatinisation onset temperature long enough for hydrogen bonds to break, yet below the degradation threshold where dextrinisation discolours the product. The seven heating zones on the MT series, paired with barrel cooling circuits, allow the operator to set a rising temperature ramp — typically starting just below onset in the feed section and peaking in the metering zone — so that residence time and thermal input are decoupled. This independent control is what separates a modified starch processing line manufacturer offering real process flexibility from one simply supplying a fixed-temperature barrel.
Matching Dryer Capacity to Extruder Evaporation Load
Pre-gelatinized starch exits the die at a moisture content significantly higher than the target powder specification. The five-layer baking oven must evaporate that water without case-hardening the pellet surface, which would trap internal moisture and cause clumping in the grinder. Gas or diesel heating gives the dryer enough thermal mass to sustain evaporation across all five layers, while inverter-driven belt speed lets the operator extend or shorten residence time as the extruder output shifts between MT70 and MT85 volume ranges [NEED_CITE: heat transfer requirements for multi-layer starch drying].
Screw Geometry and Starch Shear Sensitivity
The 38CrMoAl nitrided screws resist the abrasive wear that starch-filled melts impose, but geometry matters as much as metallurgy. A compression ratio suited to corn starch may over-shear potato starch, rupturing granules prematurely and producing a gummy extrudate that blocks the die. Screw configuration must be selected against the buyer’s specific starch source and the target degree of modification — whether physical pre-gelatinisation or chemical denaturation for drilling fluids. This is the point where generic screw builds copied from a catalogue fail.
Reading the Specification Sheet Beyond Installed Power
Installed power tells you what the transformer must supply; actual consumption tells you what the product really costs to run per kilogram. On the MT85, installed power sits at 190 kW while running consumption is 140 kW — the gap covers heater ramp-up, start-up purge, and intermittent cooling pump draw. Barrel heating accounts for 14 kW across seven zones on the MT70, meaning individual zone control is essential rather than cosmetic; locking all zones to one set-point wastes energy and degrades product colour. Screw diameter and length determine the L/D ratio and therefore mean residence time — a short barrel forces higher screw speed to maintain output, increasing shear heat and narrowing the gelatinisation window. Mixer batch capacity must be matched to extruder feed rate: a 20 kg batch feeding an MT85 running at 300 kg/h means the mixer empties roughly every four minutes, which is impractical without a buffer hopper. These cross-references between spec rows reveal whether the line was designed as a system or assembled from standalone catalogue items.
When Stations Are Sized Independently
A twin-screw extruder producing at its upper range will overwhelm a dryer that was quoted on a lower nominal figure, forcing the operator to slow the extruder and forfeit the capacity they paid for. The grinder then sees irregular feed — surges followed by gaps — producing inconsistent particle size and overloading the cyclone dust collector. These bottlenecks are invisible on the proposal sheet because each station’s capacity is listed in isolation [NEED_CITE: throughput mismatch consequences in multi-station processing lines]. The buyer only discovers the problem during commissioning, when the line’s real ceiling turns out to be set by the weakest station, not the extruder nameplate.
Why Sourcing the Full Line from One Supplier Matters
Complete station matching — mixer batch cycle, extruder throughput, dryer evaporation rate, and grinder classification speed — is calculated against a single mass balance rather than left to individual vendor assumptions. Screw configuration and die geometry are specified to the buyer’s starch source and modification target, not copied from a generic build. An in-house testing workshop runs the customer’s actual raw material before the line ships, so gelatinisation degree and powder particle size are confirmed in advance, not discovered on-site. Voltage, frequency, and control language are locked in at the engineering stage, avoiding the commissioning delays that arise when a panel arrives wired for a grid the destination plant does not have. Pre-sales consultation through installation, operator training, and wear-part supply keeps responsibility under one contract rather than split across four equipment vendors and a local integrator.
Documentation & Verification
- Line layout drawing showing station spacing and utility connection points for MT70/85/75 footprint
- Screw and die configuration record matched to buyer’s specific starch source and modification chemistry
- Trial run report on customer raw material confirming gelatinisation degree and output before shipment
- Electrical schematic with confirmed voltage, frequency, and control language for destination plant
- CE declaration of conformity covering the complete extrusion and drying assembly
- Wear parts list with part numbers and lead times for screws, dies, and barrel heating elements
Installation, Commissioning & Support
- Foundation plan reflecting 41–45 m line length and 1.8-tonne dryer dead load for level slab preparation
- Dedicated power feed sized to 210 kW maximum installed draw with isolation for barrel heater circuits
- Mixer and grinder shipped as separate skids requiring on-site mechanical coupling to extruder discharge
- Barrel zone temperature ramp and dryer belt speed set during first production run on buyer’s starch
- Operator training covering screw pull procedure, die change, and pulse grinder screen replacement
- Spare screw element and die segment inventory recommended for first twelve months of operation
Preparing Your Line Specification Inquiry
To configure a modified starch processing line that matches your plant, share the starch source (cassava, corn, or potato), any pre-treatment or chemical modification already applied, and the target gelatinisation degree or powder mesh size. Specify your destination voltage, frequency, and preferred control language so the electrical panel is built correctly before shipping. Include your available floor length and ceiling height to confirm which model — MT70, MT85, or MT75 — fits the building envelope. If you can send a sample of your raw material, a trial run in the testing workshop will establish realistic output and product quality before the quotation is finalised.
Frequently Asked Questions
Q: How is output capacity verified before the line ships?
A: The customer’s actual starch material is run through the twin-screw extruder in the in-house testing workshop. The trial run report records achievable gelatinisation degree, moisture reduction across the dryer, and grinder particle size at a documented feed rate, forming the basis for the quoted capacity rather than a generic catalogue figure.
Q: How are screw and barrel zone settings chosen for different starch sources?
A: Cassava, corn, and potato starches each have distinct gelatinisation onset temperatures and shear sensitivities. The screw compression ratio, element pitch sequence, and seven-zone barrel temperature profile are configured against the buyer’s specific material data sheet and the target modification type — physical pre-gelatinisation or chemical denaturation.
Q: What electrical and control options are available for export markets?
A: Voltage, frequency, and control panel language are confirmed during the engineering stage to match the destination plant’s grid. The standard 380 V / 50 Hz three-phase supply can be adapted, and MCC or PLC control options are available depending on the level of automation the buyer requires.
Q: How do you prevent dryer or grinder bottlenecks at full extruder output?
A: Each station’s capacity is calculated from a single mass balance based on the buyer’s raw material moisture and target powder specification. The five-layer dryer evaporation rate and pulse grinder throughput are matched to the selected extruder model’s verified output, so no individual unit limits line speed.
Q: Can a trial run be performed on our raw material before shipment?
A: Yes. The in-house machine testing workshop runs the buyer’s starch sample through the complete extruder-dryer-grinder sequence. The resulting trial run report documents screw configuration, barrel temperature profile, product gelatinisation degree, and output rate, giving the buyer verified performance data before the line is crated for dispatch.