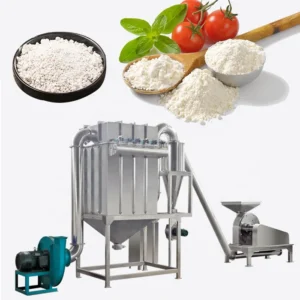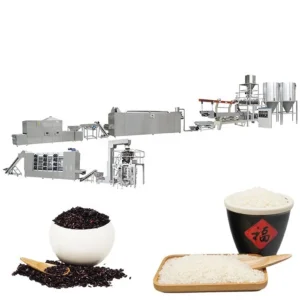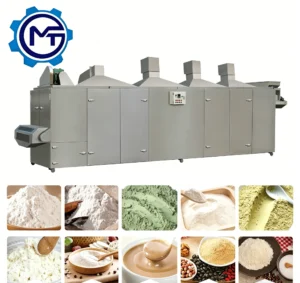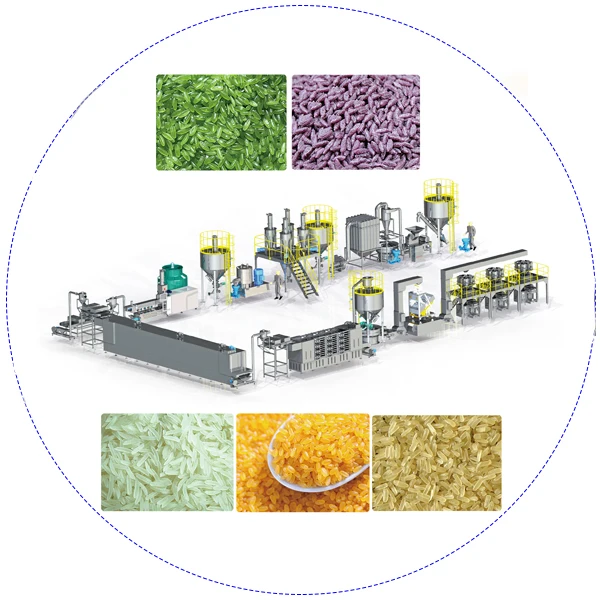
Throughput-Matched Line Design — every MT extruder model is paired with upstream and downstream stations sized to its real output, preventing bottlenecks in fortified rice kernel production.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 / MT75 / MT95 |
| Product Type | Fortified Rice Kernel Extrusion Production Line |
| Extruder Type | Twin Screw |
| MT65 Installed Power | 85 kW |
| MT65 Power Consumption | 60 kW |
| MT65 Output Capacity | 80–100 kg/hr (basis not stated in source — confirm raw material / moisture content) |
| MT65 Overall Dimensions | 28 × 1.2 × 2.2 m |
| MT70 Installed Power | 120 kW |
| MT70 Power Consumption | 85 kW |
| MT70 Output Capacity | 100–120 kg/hr (basis not stated in source — confirm raw material / moisture content) |
| MT70 Overall Dimensions | 30 × 1.5 × 2.2 m |
| MT85 Installed Power | 235 kW |
| MT85 Power Consumption | 165 kW |
| MT85 Output Capacity | 200–300 kg/hr (basis not stated in source — confirm raw material / moisture content) |
| MT85 Overall Dimensions | 34 × 3.5 × 4.3 m |
| MT75 Installed Power | 180 kW |
| MT75 Power Consumption | 135 kW |
| MT75 Output Capacity | 300–500 kg/hr (basis not stated in source — confirm raw material / moisture content) |
| MT75 Overall Dimensions | 32 × 3.5 × 4.3 m |
| MT95 Installed Power | 260 kW |
| MT95 Power Consumption | 195 kW |
| MT95 Output Capacity | 800–1000 kg/hr (basis not stated in source — confirm raw material / moisture content) |
| MT95 Overall Dimensions | 36 × 3.5 × 4.3 m |
| Voltage | 220V / 380V (frequency to be confirmed for target market) |
| Control System | Frequency speed controlling, high automation |
| Feeding System | Single or double screw feeding, selected by material characteristics |
| Lubrication | Automatic lubricating and cooling system |
| Drying Oven Heating Source | Electric or gas |
| Drying Oven | Circulation drying with frequency motor mesh belt speed control |
| Assembly State | Complete production line (mixing, extruding, vibrating, drying, cooling, roasting, cooling, packing) |
| Contact Material | Stainless steel food-contact components |
| Standards | CE, ISO |
| Warranty | 1 Year |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice kernel (FRK) for public nutrition programs | Broken rice or rice bran blended with vitamins, iron, zinc, and folic acid |
| Artificial nutrition rice | Corn, millet, wheat, oats, or buckwheat as base with micro-nutrient fortification |
| Value-added extruded rice products | Starch-based blends with added minerals for food and beverage factories |
| Instant nutrition porridge base | Multi-grain formulations with protein and vitamin enrichment |
Why "Nominal Capacity" Can Mislead a Fortified Rice Line Buyer
A capacity figure without a raw material basis is a guess, not a guarantee.
When a buyer sources a full equipment range fortified rice extrusion line, the quoted throughput often comes from a benchmark run on pure rice flour at a fixed moisture level. In real production, fortified rice kernels contain broken rice, rice bran, bean flour, and micro-nutrient premixes that change gelatinisation temperature and melt viscosity inside the barrel. [NEED_CITE: starch gelatinisation behaviour in multi-ingredient extrusion] I once watched a line stall because the buyer’s actual blend included soy flour and trace mineral powder — the die blocked within minutes, and the screw combination had to be rebuilt on-site over several days. That is why every MT model’s capacity must be verified against your specific formulation before the order is finalised.
Five Models Covering Small Pilot to Full Industrial Output
The MT series offers five twin-screw extruder models — MT65, MT70, MT85, MT75, and MT95 — spanning from small-batch production to high-volume industrial runs. Each model occupies a distinct capacity band, so buyers can match extruder selection to their target output without oversizing or underfeeding downstream stations. The twin screw extruder for fortified rice kernel configuration provides consistent shear and residence time across the barrel, which matters when micro-nutrients must be evenly dispersed throughout the kernel matrix.
How Downstream Stations Prevent Line Bottlenecks
A common failure in extruded rice lines is a dryer or cooling conveyor that cannot keep pace with the extruder. The circulation drying oven on this line uses a frequency-controlled mesh belt, allowing belt speed to be adjusted to the actual moisture load leaving the die. Gas or electric heating options let the buyer match local utility costs. When the dryer is correctly sized to the extruder’s real throughput, kernels reach the cooling and roasting stages at the right moisture level, maintaining the shape and density that the market expects. [NEED_CITE: moisture management in extruded rice kernel drying]
What the Barrel, Screw, and Die Actually Do to Your Blend
In twin-screw extrusion for fortified rice, the screw configuration determines how thoroughly the vitamin-mineral premix disperses into the starch matrix. A longer effective L/D ratio gives the blend more residence time, which improves gelatinisation uniformity but also increases energy input per kilogram. The die design controls kernel shape — whether round, oval, or rice-grain profile — and directly affects cooking behaviour when the end consumer prepares the product. Single or double screw feeding is selected based on whether the raw material is free-flowing granular or a cohesive premix, preventing surge or starvation at the feed throat. The automatic lubricating and cooling system keeps barrel temperature stable during long production runs, reducing thermal drift that could alter kernel density mid-shift.
The Cost of Skipping Raw Material Trials
When a line ships without a trial run on the buyer’s actual formulation, the first production day becomes an expensive experiment. Screw combinations may need repeated adjustment, die inserts might require replacement to hit the correct kernel shape, and the dryer settings could be entirely wrong for the real moisture load. [NEED_CITE: extrusion line commissioning challenges without pre-shipment trials] These issues compound when the buyer is producing for a government nutrition tender with strict kernel specifications on density, cooking time, and nutrient retention.
Why Buyers Source the Full Equipment Range Fortified Rice Extrusion Line Here
Every station in the line — mixing, extruding, vibrating, drying, cooling, roasting, and packing — is sourced and throughput-balanced from one supplier, eliminating the finger-pointing that happens when separate vendors supply mismatched equipment. Screw configuration and die design are specified to the buyer’s raw material and target kernel shape rather than copied from a generic build. An in-house testing workshop allows trial runs on your actual formulation before shipment. Electrical schematics and voltage confirmation are completed before production begins, so the control panel matches your facility’s supply. Food-grade stainless steel is used throughout all contact surfaces, meeting hygiene requirements for nutrition-grade production.
Documentation & Verification
- Line layout drawing showing every station from batching to packing with throughput annotations
- Screw and die configuration record matched to your specific raw material blend
- Trial run report on your fortified rice formulation completed before dispatch
- Electrical schematic with voltage and frequency confirmed for your facility
- Operation and maintenance manual covering all five extruder models in the series
Installation, Commissioning & Support
- Foundation requirements based on the selected model’s dimensions and 6000 kg net weight class
- Dedicated power circuit sized to the chosen model’s installed power rating up to 260 kW
- On-site assembly of drying oven and cooling conveyors to match extruder throughput
- First-run parameter setting including barrel temperature profile and mesh belt speed calibration
- Operator training on screw configuration changes for different fortified rice formulations
- Wear parts list covering screws, dies, and barrel liners with recommended replacement intervals
Before You Send an Inquiry
To configure the right line, share your base raw material blend and the specific vitamins or minerals you plan to add, along with your target daily output. Confirm your facility’s voltage, frequency, and available floor space so the layout can be designed before quotation. If your formulation is proprietary, we can sign a non-disclosure agreement before running a trial on your actual material in the testing workshop.
Frequently Asked Questions
Q: How is output capacity verified for each extruder model?
A: Each model’s capacity rating must be confirmed against the buyer’s specific raw material formulation and moisture content. A trial run in the testing workshop using your actual fortified rice blend — including any bean flour, starch, or micro-nutrient premix — provides a verified throughput figure before the order is placed.
Q: How are the dryer and cooling stations sized to the extruder?
A: The circulation drying oven and cooling conveyor are matched to the selected extruder model’s real throughput. Belt speed and heating capacity are calculated so kernels reach the correct moisture level without backlog or idle time between stations.
Q: What electrical specifications are confirmed before production starts?
A: Voltage, frequency, and control panel language are confirmed against the buyer’s facility supply. Electrical schematics are reviewed and approved before the machine enters production, preventing commissioning delays caused by mismatched power configurations.
Q: Which supporting stations are included in the complete line?
A: The line includes mixing and batching, extrusion, vibrating conveyance, circulation drying, cooling, roasting, secondary cooling, and packing stations. Each station is throughput-balanced to the selected extruder model so no single point restricts the line’s real output.
Q: Can I run a trial on my own raw material before the line ships?
A: Yes. The in-house testing workshop accepts the buyer’s actual raw material blend for a trial run. The resulting report covers extruder behaviour, screw configuration, die performance, and product quality, giving you verified data before shipment.