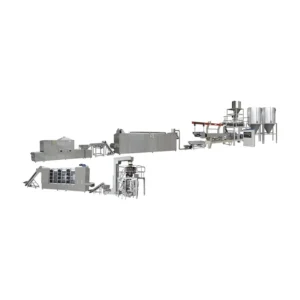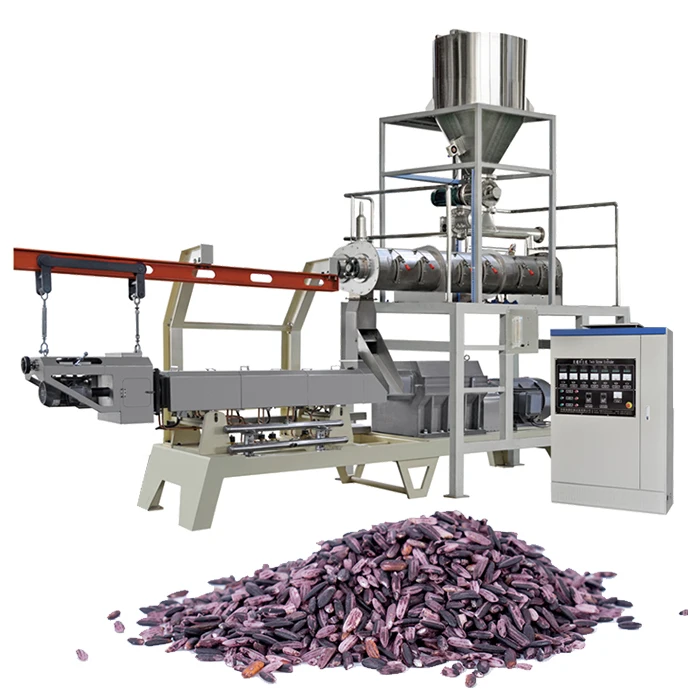
Complete Turnkey Integration — throughput matching across every station from batching through packing, verified on customer raw material before dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fortified Rice Kernel Extrusion Line |
| Model | MT65 / MT70 / MT85 / MT75 / MT95 |
| Rated Power | MT65: 85 kW; MT70: 120 kW; MT85: 235 kW; MT75: 180 kW; MT95: 260 kW |
| Power Consumption | MT65: 60 kW; MT70: 85 kW; MT85: 165 kW; MT75: 135 kW; MT95: 195 kW |
| Output Capacity | MT65: 80–100 kg/h (basis not stated in source — confirm raw material formulation / moisture); MT70: 100–120 kg/h (basis not stated in source); MT85: 200–300 kg/h (basis not stated in source); MT75: 300–500 kg/h (basis not stated in source); MT95: 800–1000 kg/h (basis not stated in source) |
| Overall Dimensions (L×W×H) | MT65: 28 × 1.2 × 2.2 m; MT70: 30 × 1.5 × 2.2 m; MT85: 34 × 3.5 × 4.3 m; MT75: 32 × 3.5 × 4.3 m; MT95: 36 × 3.5 × 4.3 m |
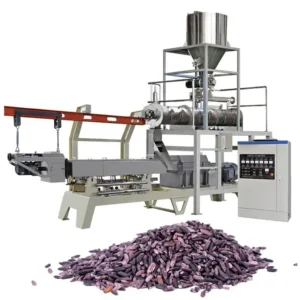
| Screw Type | Twin-screw |
| Feeding System | Single or double screw feeding system selectable |
| Control System | Frequency speed controlling (PLC / MCC architecture to be confirmed) |
| Screw Material | Wear-resistant alloy |
| Lubrication & Cooling | Automatic lubricating system and automatic cooling system |
| Dryer Type | Multi-layer mesh belt dryer with frequency motor speed control |
| Dryer Heating Source | Electric or gas |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice kernel production | Broken rice, rice flour blended with vitamin and mineral premix |
| Artificial rice for food security programs | Corn, millet, wheat, oats formulated into rice-shaped kernels |
| High-value grain by-product conversion | Buckwheat, bean, starch processed into extruded nutritional kernels |
| Fortified breakfast and infant nutrition ingredients | Cereal and starch blends with supplementary micronutrients |
When the Dryer Cannot Keep Up with the Extruder
An extruder that outpaces its downstream dryer creates a bottleneck that forces the whole fortified rice extruder full equipment range to idle while operators clear the backlog.
We see this mismatch on nearly every line audit. A buyer selects an extruder based on rated output, then pairs it with a dryer sized for a different material or moisture load. The result is kernels that exit the dryer still holding excess moisture, leading to spoilage or cracking during storage. The dryer becomes the constraint, and the extruder never reaches its actual throughput. Sizing each station to the material’s real drying curve — not just the extruder’s nameplate capacity — is the only way to avoid this. [NEED_CITE: moisture equilibrium targets for extruded cereal kernels]
Matching Every Station to the Material Profile
A fortified rice extruder full equipment range must handle raw materials that vary widely in starch content, fiber ratio, and moisture absorption. Broken rice behaves differently from corn or buckwheat when it enters the barrel. The twin-screw configuration with selectable single or double screw feeding allows the operator to match feed uniformity to the specific blend, preventing surging or starvation at the die plate.
Die Design and Kernel Geometry
The final kernel shape and density depend on die aperture geometry and the cut-off mechanism speed. If the die is specified for a standard rice shape but the formulation includes a high proportion of bean or oat flour, the extrudate may swell beyond the intended profile. Die design must be matched to the buyer’s exact formulation before production begins, not adjusted empirically after installation. [NEED_CITE: die land length and extrudate swell in starch-based extrusion]
Reading the Specs Beyond Nameplate Numbers
The five models in this range span rated power from 85 kW on the MT65 to 260 kW on the MT95. Power consumption figures are correspondingly lower — 60 kW to 195 kW — which reflects the difference between installed motor capacity and actual energy draw under load. The multi-layer mesh belt dryer with frequency motor speed control allows the operator to adjust dwell time without changing belt length, which is critical when switching between a high-moisture corn blend and a low-moisture broken rice formulation. Automatic lubricating and cooling systems reduce unplanned stops during long production runs, and the wear-resistant alloy screw material extends the interval between screw and barrel replacements. The overall line length ranges from 28 meters to 36 meters depending on model, which affects workshop layout planning and utility routing.
The Hidden Cost of Skipping the Trial Run
Lines shipped without a trial run on the buyer’s actual raw material almost always require extended on-site commissioning. The screw combination that works on the manufacturer’s test material may not gelatinise starch correctly when the buyer adds a 30%杂粮 premix or alters the moisture ratio. Remote troubleshooting then stretches into days of video calls adjusting barrel temperature zones and feed rates. This delay costs the buyer production time and may push delivery commitments to their own customers. [NEED_CITE: typical commissioning duration when trial runs are omitted]
Why Source the Full Range Here
Every station in the fortified rice extruder full equipment range is specified under one supplier, so throughput calculations are consistent from the mixer to the packing station. Screw configuration and die design are documented against the buyer’s raw material formulation rather than pulled from a generic build library. The in-house testing workshop runs the buyer’s actual material before shipment, generating a trial report that becomes the baseline for commissioning. Electrical schematics and voltage confirmation are completed before production starts, preventing delays at the destination site. Wear parts lists and spare screw sets are included with the first order so the first replacement cycle does not halt production.
Documentation & Verification
- Line layout drawing showing each station footprint and throughput match
- Screw and die configuration record tied to your raw material formulation
- Trial run report on your material from the in-house testing workshop
- Electrical schematic with voltage and frequency confirmed for your market
- Factory test record documenting output and kernel geometry before dispatch
- Operation and maintenance manual with wear parts replacement intervals
Installation, Commissioning & Support
- Workshop floor must accommodate line lengths up to 36 meters with utility drops at each station
- Dedicated circuit required matching the model’s rated power from 85 kW to 260 kW
- Line arrives in modular sections for staged assembly and belt alignment
- First run includes screw combination verification against trial run baseline
- Operator training covers dryer frequency adjustment and moisture monitoring
- Spare screw and die sets ship with initial order to cover first replacement cycle
What We Need to Specify Your Line
To size each station correctly, share your raw material formulation including the ratio of broken rice or alternative grains to any vitamin and mineral premix. Provide your target daily output and the moisture content you expect at the dryer exit. Confirm the voltage and frequency at your facility, the preferred control language for the operator interface, and whether your dryer heating source will be electric or gas. If you can send a sample of your raw material, we will run a trial in our testing workshop and include the results with the proposal.
Frequently Asked Questions
Q: What stations are included in the full line and how is throughput matched?
A: The line includes mixing, twin-screw extruding, vibrating, low-temperature drying, cooling, high-temperature roasting, a second cooling stage, and packing. Each station is sized so that its maximum throughput matches the extruder’s actual output on your specific material, preventing bottlenecks at any single point.
Q: Which raw materials are compatible with this extrusion line?
A: The line processes broken rice, rice, corn, millet, wheat, oats, buckwheat, bean, and starch as main ingredients, with vitamins and minerals as supplementary ingredients. The screw combination and die design are adjusted to match the starch and fiber profile of your specific blend.
Q: What dryer heating source options are available?
A: The multi-layer mesh belt dryer can be configured for electric or gas heating. The choice depends on local energy costs and available utility infrastructure at your facility. Frequency motor speed control on the dryer belt allows dwell time adjustment regardless of heating source.
Q: How are voltage and control language confirmed before shipment?
A: Electrical schematics are reviewed with the buyer during the specification stage. The destination market voltage, frequency, and preferred operator interface language are documented and confirmed before production begins, so the control cabinet arrives ready for connection.
Q: What spare wear parts ship with the first order?
A: The initial shipment includes a documented wear parts list and a set of replacement screws and dies so the first scheduled maintenance cycle does not require an emergency order. Additional spares can be quoted based on your projected annual running hours.