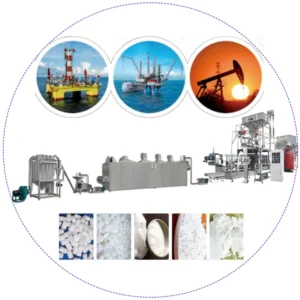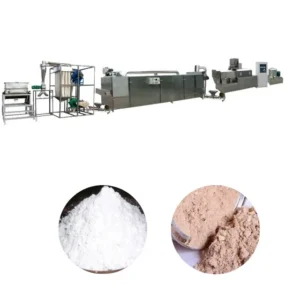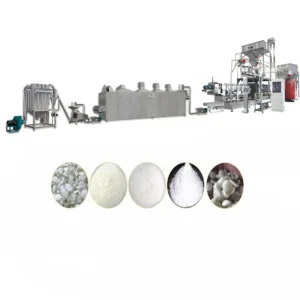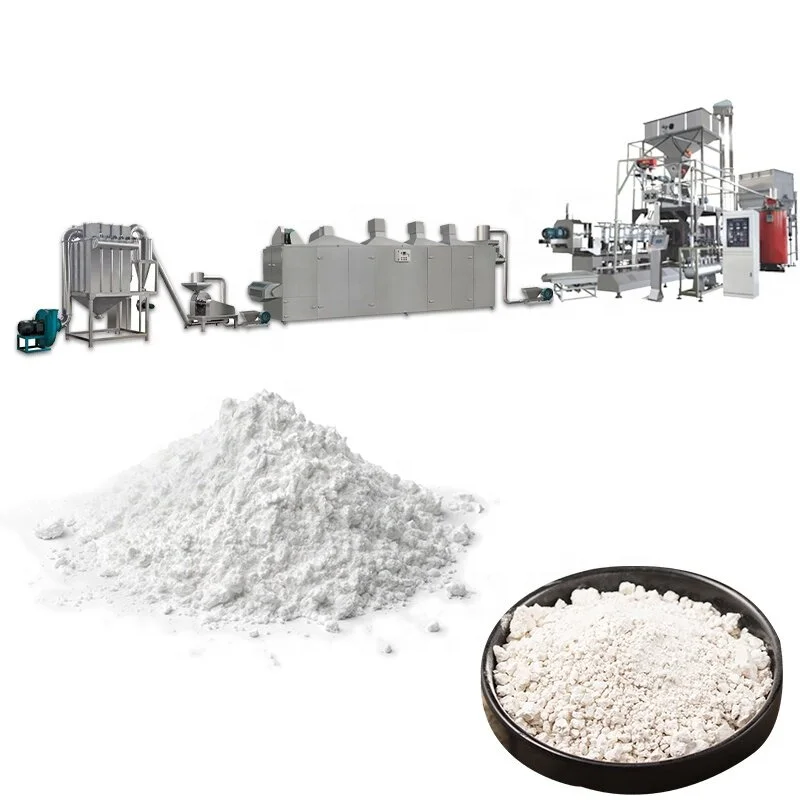
Thermodynamic balance across every station — The twin screw extrusion profile, dryer residence time and grinder throughput are sized together so one section never starve or flood another when processing starch with varying gelatinisation points.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruder Modified Starch Production Line |
| Raw Materials | wheat flour, corn starch, potato starch, cassava starch |
| Output Capacity | 80–500 kg/h (basis not stated in source — confirm raw material type, moisture content and target modification degree) |
| Screw Type | Twin screw |
| Frame Material | stainless steel 201 |
| Contact Parts Material | food grade stainless steel 304 |
| Mixer Motor | 4.0 kW |
| Mixer Batch Output | 3.0–4.0 kg per batch |
| Screw Conveyor Motor | 1.1 kW |
| Screw Conveyor Throughput | 0–150 kg/h |
| Total Installed Power (electric heating) | approximately 100 kW |
| Total Installed Power (gas/diesel heating) | approximately 50–60 kW |
| Voltage Options | 380 V / 50 Hz (three phase), 220 V / 50 Hz (single phase); custom voltage available per destination country |
| Energy Source Options | electricity, gas, diesel, steam |
| Control System | inverter-driven motors (Delixi or Delta inverter); main motors Siemens (China) or equivalent top-tier Chinese brand |
| Line Stations | Mixer → Screw Conveyor → Twin Screw Extruder → Shift Conveyor → Air Conveyor → Dryer → Air Conveyor → Conditioning → Conveyor → Grinder |
| Assembly State | complete production line with supporting equipment |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Modified starch for food processing | corn starch, cassava starch, wheat flour, potato starch with controlled gelatinisation |
| Pregelatinised starch for instant foods | corn and wheat starch requiring full expansion and rapid cold-water thickening |
| Industrial starch for paper making | corn and potato starch modified for surface sizing and coating adhesion |
| Pre-gel starch for drilling and textiles | cassava and corn starch processed to specified viscosity and solubility profiles |
Why the Moisture Reading Should Come Before the Capacity Quote
Starch behaves differently at every percentage point of moisture, and a line sized without that number will underperform on your actual feedstock.
I have watched buyers sign off on a modified starch processing line equipment catalogue based on a throughput number that was generated with a completely different moisture level than the one their silos deliver. The extruder barrel temperature profile, the screw pitch, and the dryer retention time all assume a starting water activity. When the real material arrives drier or wetter, gelatinisation shifts, expansion collapses, and the grinder chokes on half-cooked pellets [NEED_CITE: starch gelatinisation temperature variance by moisture content]. The capacity figure is not wrong — it just belongs to a different raw material.
How the Station Sequence Matches Starch Behaviour
The line follows the thermal journey starch actually takes. The mixer conditions the powder with water to a target moisture, and the screw conveyor feeds the twin screw extruder at a controlled rate. Inside the barrel, shear and heat convert native granules into a molten, gelatinised mass. The die cuts pressure, causing expansion that locks in the modified structure. From there, the shift and air conveyors move the hot, fragile extrudate into the dryer without crushing it, which matters because damaged pellets produce uneven flour in the grinder.
Where Bottlenecks Hide in Starch Lines
Starch expands aggressively compared to snack doughs, so the air conveyor cross-section and dryer belt width must handle a volume that can be several times the raw feed rate. If the dryer is specified by weight alone without accounting for bulk density after expansion, moisture leaves the product unevenly and the grinder produces a mix of over-dried fines and under-dried lumps [NEED_CITE: bulk density shift during starch extrusion]. Capacity-matching every station against the expanded volume, not the raw flour weight, keeps the modified starch processing line equipment catalogue honest.
Reading the Specs Against Your Raw Material
The twin screw configuration lets operators adjust screw element spacing to change shear intensity — higher shear for cassava starch that needs strong molecular breakdown, gentler profiles for wheat flour where gluten development must be limited. The 4.0 kW mixer motor handles the 3.0–4.0 kg batch size typical for starch conditioning, keeping residence time short enough to prevent premature hydration. With total installed power around 100 kW on electric heating and 50–60 kW on gas or diesel, the energy source choice affects more than the utility bill; steam heating delivers a softer temperature ramp that some pregelatinised starch specs demand. Inverter-driven motors across the line allow fine speed tuning so the screw conveyor throughput of 0–150 kg/h can be dialled to match the extruder’s actual consumption rate rather than a theoretical maximum.
What Happens When Stations Are Mismatched
A dryer that is too short forces operators to slow the entire line, and the extruder then runs below its thermal design point, producing under-gelatinised product that fails viscosity tests downstream. Conversely, an oversized grinder pulling material faster than the conditioner can stabilise moisture creates static-charge dust clouds and screen blinding [NEED_CITE: dust explosion risk in starch grinding operations]. These problems do not show up on a single-machine quote because each vendor only guarantees their own section.
Why Sourcing the Full Range Matters Here
Every station in this modified starch processing line equipment catalogue is sized against the others before the layout is frozen, so the air conveyor diameter, the dryer belt length, and the grinder screen area all trace back to the same expanded-volume calculation. Food grade stainless steel 304 contact parts prevent iron-catalysed discolouration that can ruin white starch batches. The inverter and motor combination — Siemens-class main drives with Delta or Delixi inverters — gives operators the speed resolution to hold a steady feed rate despite the flow variations that fine starch powders cause. Electrical schematics are confirmed against destination voltage before production starts, avoiding the commissioning delays that happen when a 380 V machine arrives at a 415 V site. Trial runs on the buyer’s actual starch are done in the testing workshop before the line is crated, so screw configuration, barrel temperatures and dryer settings ship as a recorded baseline rather than a blank starting point.
Documentation & Verification
- Line layout showing throughput calculation between each station matched to your starch type
- Screw and die configuration record tied to your raw material and target modification degree
- Electrical schematic with voltage and frequency confirmed for your destination country
- Factory test record from trial run on your actual starch batch before dispatch
- CE declaration of conformity covering the complete assembled line
Installation, Commissioning & Support
- Foundation plan sized to the total line footprint and approximately 100 kW electrical heating load
- Dedicated circuit specification for the 380 V three-phase supply and inverter-driven motor starts
- Modular station delivery allowing phased assembly in workshops with limited overhead clearance
- First-run parameter setting on your starch with recorded barrel temperature and screw speed baseline
- Operator training covering screw element changes for switching between corn, cassava and wheat starch
- Wear parts list for screws, dies and grinder screens with reorder intervals noted
What to Include in Your First Enquiry
Share the exact starch type you plan to run, the moisture content as it arrives at the mixer, and the modification spec your end customer requires — viscosity, solubility or pregelatinisation degree. Confirm the local voltage, frequency and whether steam, gas or electric heating is available on site. If you already have upstream storage or downstream packing equipment, send the interface dimensions so the air conveyor and final conveyor heights can be matched before fabrication.
Frequently Asked Questions
Q: How is the output capacity of a modified starch processing line verified before delivery?
A: Capacity is confirmed through a trial run using the buyer’s actual starch in the testing workshop. The run records real throughput at the target modification degree, moisture level and barrel temperature profile. The resulting test report ships with the line so operators start from a proven baseline rather than generic settings.
Q: Which energy source configuration should I choose for a starch extrusion line?
A: The choice depends on plant utilities and product requirements. Electric heating gives precise barrel zone control, while gas or diesel reduces installed power from approximately 100 kW to 50–60 kW. Steam heating suits pregelatinised starch where a gentler temperature ramp is needed. The line is configurable to any of these before fabrication.
Q: How are stations sized to avoid bottlenecks in a modified starch processing line equipment catalogue?
A: Each station — mixer, extruder, dryer, grinder — is calculated against the expanded volume of the specific starch, not just the raw flour weight. Air conveyor diameter, dryer belt length and grinder screen area are all matched to the same throughput basis, so no single section limits the rest.
Q: What voltage and frequency options are available for different export markets?
A: Standard options include 380 V / 50 Hz three-phase and 220 V / 50 Hz single-phase. Custom voltage and frequency configurations are available to match destination country standards. The electrical schematic and motor nameplates are confirmed against the buyer’s local supply before production begins [NEED_CITE: voltage and frequency standards by export market].
Q: What material grades are used for product-contact versus structural components?
A: All zones that touch starch — mixer bowl, screw conveyor trough, extruder barrel, die, dryer belt and grinder chamber — use food grade stainless steel 304 to prevent discolouration and contamination. Structural frames and non-contact supports use stainless steel 201, keeping the line durable without inflating cost on parts that never see the product.