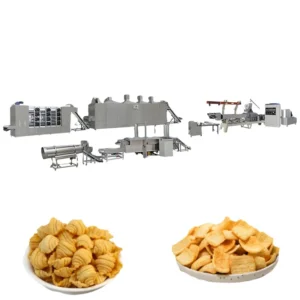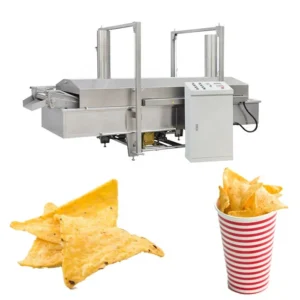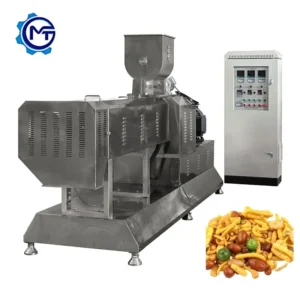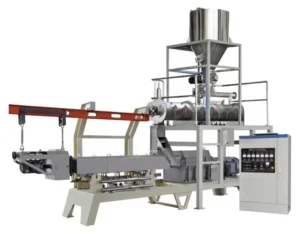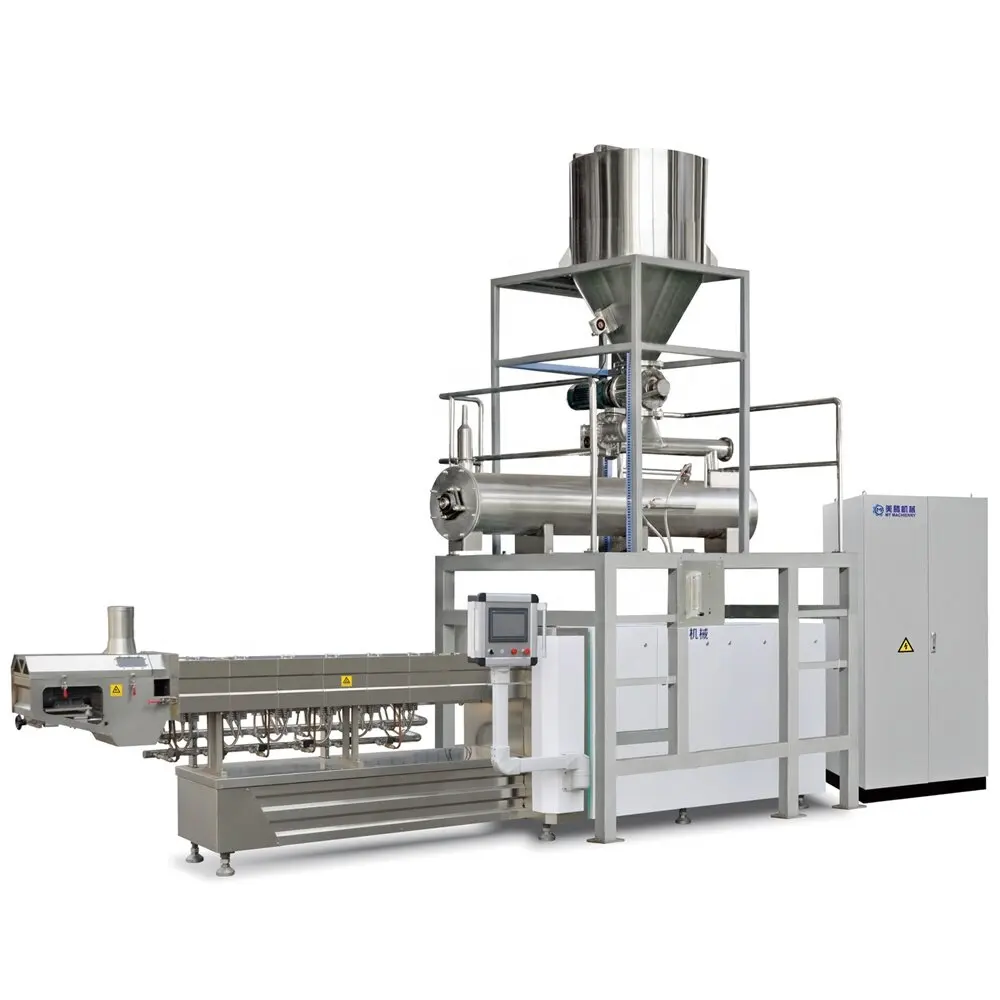
Complete Line Throughput Matching — every station from feeder to fryer is sized against your actual flour blend so no single machine bottlenecks the extrusion output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fried Pasta Snacks & Kurkure Extrusion Line |
| Output Capacity | 150–200 kg/h (basis not stated in source — confirm raw material, moisture content and product format) |
| Construction Material | Food-grade stainless steel |
| Screw Extrusion Structure | Professional screw extrusion for uniform shaping (screw type, diameter, L:D ratio not specified in source) |
| Control System | Automatic integrated feeding, extruding, molding and conveying (PLC / MCC not specified in source) |
| Voltage & Frequency | To be confirmed before order |
| Die Configuration | Configured to product shape (details not specified in source) |
| Line Stations | Automatic feeding → extruding → molding → conveying (downstream drying, frying, flavouring, cooling, packing not specified in source) |
| Standards | CE, ISO (per company profile) |
Application Suitability
| Application | Material or Output |
|---|---|
| Nimko production | Corn-based or mixed grain flour blends, extruded and fried to a crispy bite |
| Kurkure production | Corn grits and spice-compatible dough, extruded into irregular curled shapes |
| Fried pasta snacks | Durum wheat semolina or blended flour, extruded into pasta-style forms before frying |
| Extruded crispy snack foods | Various grain and pulse flours shaped for continuous frying and seasoning |
Why "150 kg/h" Means Nothing Without Your Raw Material
A capacity figure divorced from your actual flour blend and moisture target is just a number on a brochure.
I spent years on the assembly floor before moving into export sales, and one lesson stays sharp: a line that runs perfectly on standard corn flour can lose half its expansion rate when the buyer switches to a chickpea-rice blend. I once watched a Middle Eastern customer receive a fried pasta snacks making machine manufacturer unit, load their proprietary mix, and discover the output texture was completely wrong. The screw combination had to be rebuilt on-site [NEED_CITE: impact of raw material composition on extrusion expansion rate]. When you source a fried pasta snacks and Kurkure line, the throughput claim must be tied to your specific recipe, moisture level, and target product density — not a generic test run.
How Extrusion Shapes the Final Bite
The screw configuration inside the barrel determines shear force, residence time, and starch gelatinisation — three variables that directly control whether your Kurkure curls hold their structure through the fryer. A fried pasta snacks making machine manufacturer must match screw pitch and flight depth to your dough viscosity. If the flour blend carries higher protein or fibre, the barrel temperature profile needs adjustment to prevent surface burning before the core cooks through.
Barrel Temperature Zones and Product Consistency
Multiple heating zones along the barrel let the operator stage gelatinisation so the dough reaches the die at the correct viscosity. Without that staging, you get inconsistent expansion — some pieces puff correctly while others stay dense and hard. For Kurkure, where the irregular curled shape depends on controlled moisture flash-off at the die face, zone-by-zone temperature management is the difference between a market-ready product and a batch that sinks to the bottom of the fryer [NEED_CITE: barrel temperature profiling in snack extrusion processes].
Reading the Specs That Actually Matter
The output capacity of 150–200 kg/h is listed without a raw material basis, which means it is a nominal reference, not a guaranteed production rate. Confirm what flour blend, moisture percentage, and product shape that figure was measured on before comparing it against your daily target. The food-grade stainless steel construction covers contact surfaces, which matters for hygiene audits and corrosion resistance in humid fry rooms. The automatic integrated sequence from feeding through molding and conveying reduces manual transfer points where product can break or cool unevenly. Die configuration must be specified to your target shape — Kurkure curls, pasta tubes, or flat chips each demand a different die geometry and cut-off mechanism.
The Hidden Cost of Unmatched Downstream Stations
An extruder that produces at a steady rate is useless if the dryer or fryer cannot keep up. I have seen snack producers lose entire shifts because the fryer basket capacity was sized for a smaller extruder, creating a backlog of raw product that dried out before it ever reached the oil [NEED_CITE: throughput bottleneck between extrusion and frying stations]. When the flavouring drum runs slower than the cooler feed belt, seasoned product piles up and breaks. Every station in a fried pasta snacks line must be throughput-matched to the extruder output on your specific recipe, not assembled from whatever models happen to be in stock.
Why Source This Line Here
Screw and die configuration is specified to your flour blend and target product shape before production begins, not copied from a generic build. The in-house testing workshop runs your actual raw material through the line before shipment, so expansion rate, texture, and fry behaviour are verified before the machines leave Jinan. Every station — feeder, extruder, molder, conveyor — is selected and matched under one supplier so throughput calculations hold across the full sequence. Electrical schematics and voltage confirmation are completed before the control panel is wired, avoiding commissioning delays when the line arrives at your plant. Documentation includes a trial run report on your raw material, not a standard factory test on generic corn flour.
Documentation & Verification
- Line layout and capacity calculation matched to your flour blend and target output rate
- Screw and die configuration record written for your specific product shape and moisture target
- Electrical schematic with voltage and frequency locked to your plant supply before wiring
- Trial run report on your actual raw material conducted in the testing workshop before dispatch
- CE declaration of conformity and ISO certificate included with shipment documentation
- Wear parts list with reorder codes for screws, dies, and seals
Installation, Commissioning & Support
- Foundation and floor space plan sized to the full line footprint including fryer and cooler
- Power supply requirements with dedicated circuit specifications confirmed before shipment
- Machines shipped in modular sections for container loading and on-site reassembly
- First-run commissioning with screw speed, barrel temperature, and fryer settings calibrated to your recipe
- Operator training covering die changes, screw cleaning, and moisture adjustment procedures
- Spare wear parts including screws and dies supplied with initial shipment for first replacement cycle
What to Include in Your Inquiry
To size the fried pasta snacks making machine manufacturer line correctly, share your actual flour blend composition, target moisture range at the die, and the specific snack shape you intend to produce. Provide your plant voltage and frequency, the available floor space with ceiling height, and whether you need downstream frying, flavouring, and packing stations included. If you have existing upstream mixers or downstream conveyors, send their throughput rates so the new line integrates without bottlenecks.
Frequently Asked Questions
Q: How is the 150–200 kg/h capacity verified, and on which raw material and moisture level?
A: The listed capacity is a nominal range. We verify actual throughput by running your specific flour blend and moisture target through our testing workshop before shipment. The trial run report documents the measured output rate, expansion ratio, and product texture so you know exactly what the line delivers on your recipe before it leaves our factory.
Q: Which line stations are included — does the quotation cover dryer, fryer, flavouring drum and cooler?
A: The base line covers automatic feeding, extruding, molding, and conveying. Downstream stations such as drying, frying, flavouring, cooling, and packing are configured based on your production requirements. We calculate throughput at each station against your extruder output so no single machine creates a bottleneck.
Q: How do I confirm voltage, frequency and control language for my country before production starts?
A: We request your plant electrical specifications during the inquiry stage and confirm voltage, frequency, and control panel language before the electrical schematic is finalised. This ensures the control system matches your local supply and your operators can read all interface prompts in their working language upon arrival.
Q: Can I send my raw material for a trial run before the machine ships?
A: Yes. Our in-house testing workshop runs your actual flour blend through the configured line before dispatch. We document expansion behaviour, product shape integrity, and fry response in a trial run report. If adjustments to screw configuration or die design are needed, we make them before the machines are packed for shipment.
Q: What spare wear parts such as screws and dies are supplied, and how do I order replacements?
A: An initial set of spare screws, dies, and seals is included with the shipment based on expected wear intervals. A wear parts list with reorder codes is provided in the documentation package. You can order replacements directly from us using those codes whenever your first replacement cycle is due.