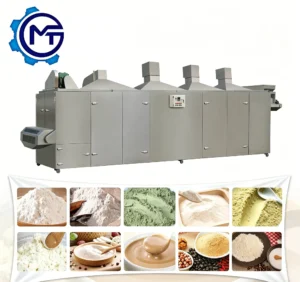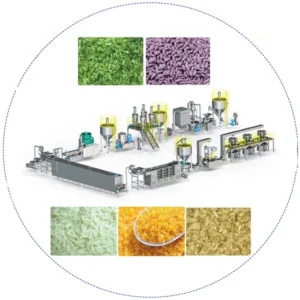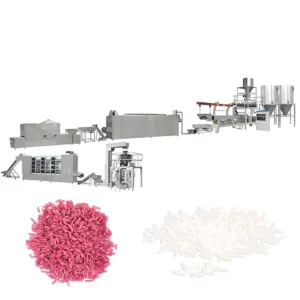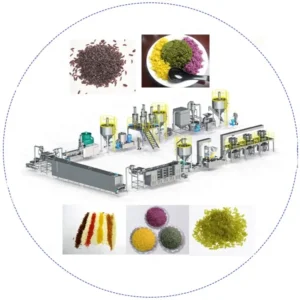
Throughput matched at every station — a full artificial rice production line engineered so the extruder, dryer, roaster and packing stations run at the same output target rather than being assembled from mismatched vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 / MT75 / MT95 |
| Product Type | Twin Screw Extruder Artificial Rice Production Line |
| Installed Power | 85 kW (MT65) / 120 kW (MT70) / 180 kW (MT75) / 235 kW (MT85) / 260 kW (MT95) |
| Power Consumption | 60 kW (MT65) / 85 kW (MT70) / 135 kW (MT75) / 165 kW (MT85) / 195 kW (MT95) |
| Capacity | 80–100 kg/h (MT65) / 100–120 kg/h (MT70) / 300–500 kg/h (MT75) / 200–300 kg/h (MT85) / 800–1000 kg/h (MT95) (basis to be confirmed — depends on raw material type, moisture content and pellet size) |
| Screw Type | Twin-screw |
| Speed Control | Frequency speed controlling |
| Lubrication | Automatic lubricating and cooling system |
| Drying Oven Heating Source | Electric or gas |
| Drying Oven Feature | Circulation drying with frequency motor mesh belt speed control |
| Overall Dimensions (L×W×H) | 28×1.2×2.2 m (MT65) / 30×1.5×2.2 m (MT70) / 32×3.5×4.3 m (MT75) / 34×3.5×4.3 m (MT85) / 36×3.5×4.3 m (MT95) |
| Contact Material | 304 Stainless Steel |
| Production Procedure | Mixing → Extruding → Vibrating → Low temperature drying → Cooling → High temperature roasting → Cooling → Packing |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice kernel production | Broken rice and rice bran blended with vitamins and minerals |
| Artificial rice for nutrition programmes | Corn, millet and starch reconstituted into rice-shaped kernels |
| Multi-grain reconstituted rice | Wheat, oats and buckwheat with added micro-nutrients |
| Protein-enriched rice analogues | Bean flour and starch blends with supplementary nutrients |
What a Capacity Figure Leaves Out When Stations Are Mismatched
A line is only as fast as its slowest station, and the bottleneck is rarely the extruder.
Buyers often focus on extruder throughput and overlook the dryer or roaster downstream. When those stations are sized to a different capacity, the extruder either starves or piles up material on the conveyor. On an artificial rice production line full equipment range, the drying oven must handle the same hourly kilogram load that exits the die, and the roaster must keep pace without scorching kernels that sit too long on the belt. I have watched lines sit half-idle because a circulation dryer could not evaporate moisture fast enough, turning a rated output into a practical ceiling well below the nameplate. [NEED_CITE: matching throughput across extrusion line stations]
How the Twin-Screw Barrel Profile Shapes the Kernel
Twin-screw extrusion forces the starch matrix through high shear and controlled temperature zones, gelatinising the grain flour while the die cuts each kernel to shape. Frequency speed control on the main drive lets the operator adjust residence time inside the barrel, which directly affects how completely the starch gelatinises. Incomplete gelatinisation produces kernels that fracture during roasting; excessive residence time degrades heat-sensitive vitamins added to fortified formulations. The MT series artificial rice production line full equipment range uses an automatic lubricating and cooling system to keep barrel temperatures within the window that preserves both kernel structure and nutrient integrity.
Why Low-Temperature Drying Precedes High-Temperature Roasting
After extrusion, the rice kernels carry significant surface and internal moisture. A two-stage thermal process — low-temperature circulation drying followed by high-temperature roasting — removes that moisture gradually so the kernel shrinks uniformly rather than cracking. The mesh belt speed on the drying oven is governed by a frequency motor, allowing fine adjustment of dwell time to match the moisture load exiting the extruder. This staged approach is what lets the kernels survive roasting without splitting along the seam line. [NEED_CITE: staged drying and roasting in reconstituted rice production]
Reading the Power and Capacity Table Correctly
Installed power on the MT85 reaches 235 kW while actual consumption sits at 165 kW — the gap reflects start-up surge and reserve for harder material blends. Capacity figures across the five models span from 80 to 1000 kg/h, but those numbers shift with raw material density, moisture content and the die opening selected for the target kernel size. A line processing corn-based formulations at higher moisture will move fewer kilograms per hour than one running dry rice flour through the same die. Always confirm the capacity basis against your specific formulation before sizing downstream dryers and packing stations to the extruder’s nameplate rating. The overall footprint also grows with model size, from 28 m for the MT65 to 36 m for the MT95, which affects utility routing and workshop layout.
The Hidden Cost of Skipping a Factory Trial
When a line ships without a trial run on the buyer’s actual formulation, commissioning becomes product development. Screw speed, barrel temperature and die selection that work on standard test material may produce cracked kernels or inconsistent density on a high-fat or high-protein blend. On-site rework then stretches across days while the dryer and roaster settings are recalibrated to match the new extrusion output. I once saw a nutrition programme supplier lose an entire week because the screw configuration had been set for generic starch, and the customer’s bean-fortified recipe demanded a completely different shear profile. [NEED_CITE: factory trial runs before extrusion line shipment]
Why Sourcing the Full Line from One Manufacturer Matters
Every station on this artificial rice production line full equipment range is configured under a single line layout and capacity calculation, so the mixer batch size, extruder output, dryer belt length and roaster dwell are all derived from the same throughput target. Screw and die configurations are specified against the buyer’s raw material, not copied from a generic build. An in-house testing workshop runs trial production on the customer’s actual formulation before the line ships, catching mismatches that would otherwise surface during on-site commissioning. Electrical schematics and voltage are confirmed for the destination market before production begins. Food-grade 304 stainless steel contact parts run through every station from mixer to packing, meeting the hygiene requirements of fortified food production.
Documentation & Verification
- Line layout and capacity calculation showing throughput at each station for your formulation
- Screw and die configuration record matched to your raw material test results
- Electrical schematic with voltage and frequency confirmed for your local grid
- Factory trial run report produced on your actual material before dispatch
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
Installation, Commissioning & Support
- Foundation and utility planning based on the MT model’s overall dimensions and installed power rating
- Dedicated electrical circuit sized to the confirmed voltage and frequency for your site
- Frequency-controlled drives on extruder and dryer calibrated during on-site commissioning
- Operator training covering screw speed adjustment, mesh belt speed and roaster temperature settings
- Wear parts list covering screws, dies and mesh belt sections with recommended stock quantities
- Scheduled maintenance intervals for the automatic lubricating and cooling system documented in the manual
What to Share When Requesting a Line Proposal
To size an artificial rice production line full equipment range correctly, provide the raw material formulation including any vitamin or mineral premix percentages, the target kernel dimensions, and the hourly output you need to sustain. Confirm your workshop length and ceiling height so the overall footprint can be mapped before fabrication. Specify the local voltage, frequency and preferred control language so the electrical package matches your site from day one.
Frequently Asked Questions
Q: How is capacity verified across each station of the line?
A: Each station — mixer, extruder, dryer, roaster and packing — is sized from a single throughput calculation based on your raw material and target kernel size. A trial run in the testing workshop confirms actual output before the line ships, so the capacity figure reflects your formulation rather than a generic test material.
Q: What supporting equipment is included and how is throughput matched?
A: The line covers mixing, extruding, vibrating, low-temperature drying, cooling, high-temperature roasting, second-stage cooling and packing. Belt speed on the dryer and roaster is frequency-controlled, and each station’s dwell time is calculated from the extruder’s verified kilogram-per-hour output on your material.
Q: What voltage and control options are available for different markets?
A: Voltage, frequency and control panel language are confirmed during the proposal stage to match the destination site’s electrical supply. Electrical schematics are issued for approval before production begins, preventing commissioning delays caused by mismatched power specifications.
Q: How is screw configuration selected for different raw materials?
A: Screw element arrangement and die design are chosen after reviewing the buyer’s formulation and running a trial in the testing workshop. A high-protein bean blend requires a different shear profile than a pure rice flour recipe, and the configuration record documents the setup used during the successful trial.
Q: What footprint and utility planning is needed before installation?
A: Overall line length ranges from 28 m to 36 m depending on model, with width and height varying by configuration. A detailed layout drawing is provided during the proposal stage so foundation work, utility drops and ventilation can be prepared before the equipment arrives on site.