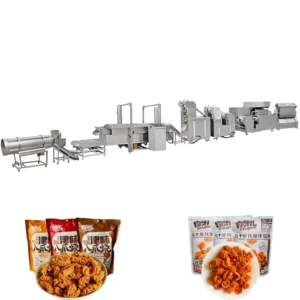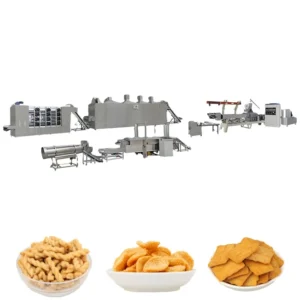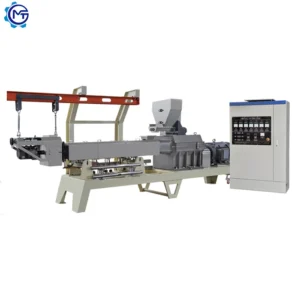
Integrated Line Matching — Throughput calculations verified across upstream extruders and downstream coating stations to eliminate frying bottlenecks before the order is placed.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Continuous Frying Machine |
| Applicable Industries | Food & Beverage Factory, Food & Beverage Shops |
| Place of Origin | Shandong Province, China |
| Power Source | Electric / Gas (dual option) |
| Voltage | 380V/50HZ |
| Total Power | 2.6 kW (control/drive) |
| Heating Tube Power | 60 kW |
| Oil Capacity | 320 L |
| Weight | 2000 KG |
| Overall Dimensions (L×W×H) | 6700 × 2200 × 1200 mm |
| Output Capacity | 100–1000 kg/h (basis not stated in source — confirm product type, moisture, frying time) |
| Control System | PLC |
| Material | Food-grade 304 Stainless Steel |
| Heating Method | Electricity Heating / Gas Heating |
| Mesh Belt | Upper and lower double-layer |
| Speed Regulation | Frequency conversion stepless speed regulation |
| Oil Filtration | Automatic oil circulation filtration system |
| Slag Discharge | Bottom-mounted slag discharge system |
| Lifting System | Automatic lifting for upper hood and mesh belt |
| Assembly State | Complete unit |
| Warranty | 1 Year |
| Core Components | PLC |
Application Suitability
| Application | Material or Output |
|---|---|
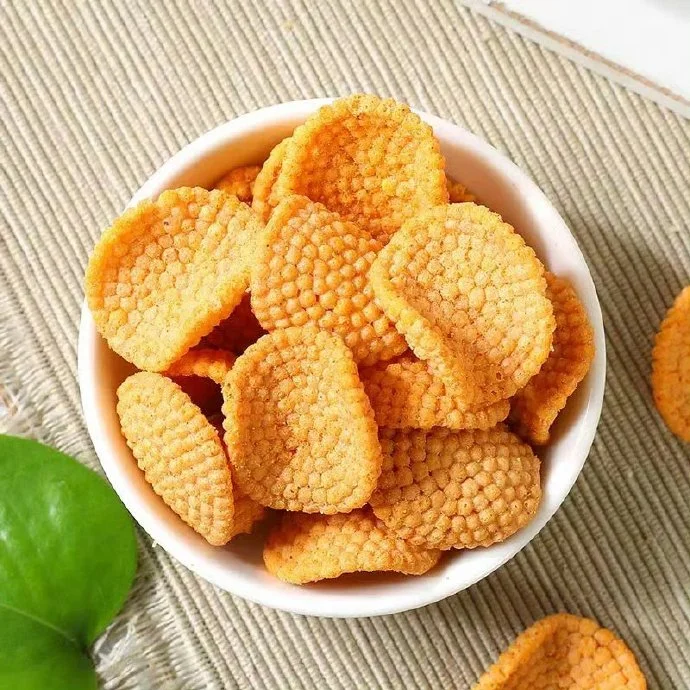
| Fried puffed snack processing | Bugles, corn chips, maize curls from extruded pellets or direct expansion dough |
| Continuous deep frying in snack lines | Integrated station between extrusion/drying and flavouring/coating stages |
| Restaurant and food factory frying | Batch or continuous operation for savoury snack formats requiring uniform oil immersion |
Why Unmatched Frying Capacity Kills Snack Line Output
A Continuous Frying Machine manufacturer must size the fryer against the actual extruder discharge rate, not a catalogue headline.
Matching fryer belt speed and oil volume to upstream extruder output prevents the most common snack line failure: a bottleneck at the frying station that starves downstream coating drums.
When the fryer runs slower than the extruder, product backs up on the conveyor, cools unevenly, and absorbs excess moisture before it ever hits the oil. The result is a texture shift the market rejects. I have seen operators throttle back an extruder to keep pace with an undersized fryer, effectively running the most expensive machine in the line at a fraction of its capability [NEED_CITE: snack line throughput balancing principles]. The Snack Frying Line for sale should always be specified on confirmed wet-product throughput, not dry-weight estimates.
Double-Layer Mesh Belt for Uniform Oil Immersion
The upper and lower mesh belt configuration holds lightweight puffed pieces — bugles, corn chips, maize curls — completely submerged throughout the frying zone. Without the top belt, buoyant snacks float to the oil surface, frying only on the underside while the top remains undercooked. This Continuous Frying Machine uses frequency conversion stepless speed regulation to adjust dwell time without stopping the line, keeping product geometry intact through the oil bath.
Oil Circulation Filtration and Slag Management
The automatic oil circulation filtration system continuously removes particulate fines that accumulate during continuous frying of extruded snacks. Left in the bath, these fines carbonise, raising the acid value and darkening subsequent batches. The bottom-mounted slag discharge system collects settled debris separately, so filtration media handle only suspended particles. This two-stage approach extends edible oil service life and maintains consistent heat transfer across the heating tube array [NEED_CITE: edible oil degradation in continuous industrial frying operations].
Reading the Power and Capacity Sheet Correctly
The 60 kW heating tube rating and 2.6 kW control/drive figure serve different functions: the heating tubes bring 320 L of oil to frying temperature and recover heat between product loads, while the 2.6 kW drives the mesh belt, oil pump, and lifting mechanism. Buyers comparing machines on total connected load should note that gas-heated variants shift thermal input to the burner, changing the electrical requirement entirely. The 6700 × 2200 × 1200 mm footprint includes the oil tank, filtration loop, and lifting clearance — verify that your snack line layout accommodates the full envelope, not just the tank dimensions. Output capacity of 100–1000 kg/h depends on product density, initial moisture, and target fry time; the Continuous Frying Machine manufacturer must confirm a realistic rate against your specific extrudate.
The Cost of Specifying a Fryer in Isolation
Ordering a fryer without confirming the upstream extruder discharge rate and downstream de-oiling or flavouring capacity creates a cascade of problems. Oversaturated product reaches the coating drum and clumps the seasoning powder into an unworkable paste. Undersized oil filtration allows acid value to climb, triggering off-flavours that no amount of seasoning masks. I once worked on a line where the fryer ran fine alone, but the extruder pushed product faster than the belt could carry it through the oil — the pile-up at the infeed meant half-fried pieces jammed the transfer conveyor [NEED_CITE: extrusion-to-frying line integration failure modes].
Why Procure This Station From MT
MT supplies the fryer as one station in a complete Snack Frying Line for sale, meaning throughput calculations run from batching through extrusion, frying, coating, and packing under a single supplier. The screw configuration and die design on the upstream extruder are specified alongside fryer belt speed and oil volume, so the hand-off between stations is calculated, not assumed. The in-house testing workshop runs your actual raw material through the frying station before shipment, generating a trial run report that confirms oil absorption and product colour against your market specification. PLC control language and voltage are locked in during the electrical schematic confirmation stage, not discovered at commissioning. Food-grade 304 stainless steel contact surfaces and the automatic lifting system for the hood and mesh belt support the hygiene protocols your HACCP plan requires.
Documentation & Verification
- Line layout and capacity calculation matching fryer throughput to your extruder discharge rate
- Electrical schematic with voltage and frequency confirmed for your local grid standard
- Trial run report on your raw material documenting oil temperature profile and product colour
- Factory test record covering PLC function, belt speed range, and heating tube integrity
- Operation and maintenance manual with cleaning intervals for mesh belt and filtration system
Installation, Commissioning & Support
- Foundation must support 2000 KG static load plus dynamic vibration from oil circulation pump
- Dedicated 380V/50Hz circuit required; gas-heated variant needs certified burner gas supply line
- Arrives as complete unit; lifting system used for hood elevation during installation alignment
- PLC parameter set loaded with frying temperature, belt speed, and oil filtration cycle times
- Operator training covers mesh belt tension adjustment and slag discharge valve operation
- Wear parts list includes replacement mesh belt sections, heating tubes, and filtration media
Preparing Your Frying Station Inquiry
To size the Continuous Frying Machine correctly, share your extruded product format — bugles, corn chips, or another shape — along with wet-product discharge rate from the upstream extruder. Confirm your local voltage and frequency, and whether electric or gas heating suits your facility’s utility infrastructure. If you are integrating into an existing line from another extruder brand, provide the discharge conveyor height and product transfer method so the fryer infeed can be matched.
Frequently Asked Questions
Q: How is fryer capacity matched to upstream extruders and downstream coating stations?
A: Throughput calculations start with your extruder’s confirmed wet-product discharge rate. The mesh belt speed and oil volume are then set so the fryer neither starves nor floods the downstream de-oiling and flavouring drums, keeping the entire Snack Frying Line for sale balanced at every station.
Q: What voltage and frequency options are available for export markets?
A: The standard configuration is 380V/50Hz, but the Continuous Frying Machine manufacturer confirms your local grid requirements during the electrical schematic stage. Heating tube ratings and drive motor specifications are adjusted accordingly before production begins.
Q: Can this fryer integrate into an existing snack line from another extruder brand?
A: Yes. The infeed conveyor height and transfer method must match your current extruder discharge. We request those dimensions during the line layout stage to ensure product transfers cleanly onto the double-layer mesh belt without manual intervention.
Q: How does the oil circulation filtration system extend oil service life?
A: The system continuously pumps oil through filtration media to remove suspended fines, while the bottom-mounted slag discharge collects heavier settled debris. This two-stage separation keeps the acid value lower for longer, reducing oil replacement frequency during continuous frying shifts.
Q: What spare wear parts ship with the machine, and how are replacements sourced?
A: The wear parts list includes mesh belt sections, heating tubes, and filtration media. Replacement components are identified in the operation manual with part numbers, and the PLC logs operating hours to signal when scheduled replacements are due.