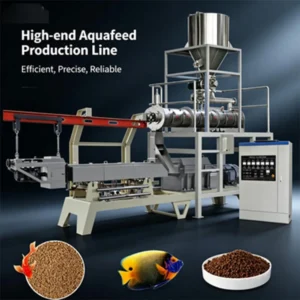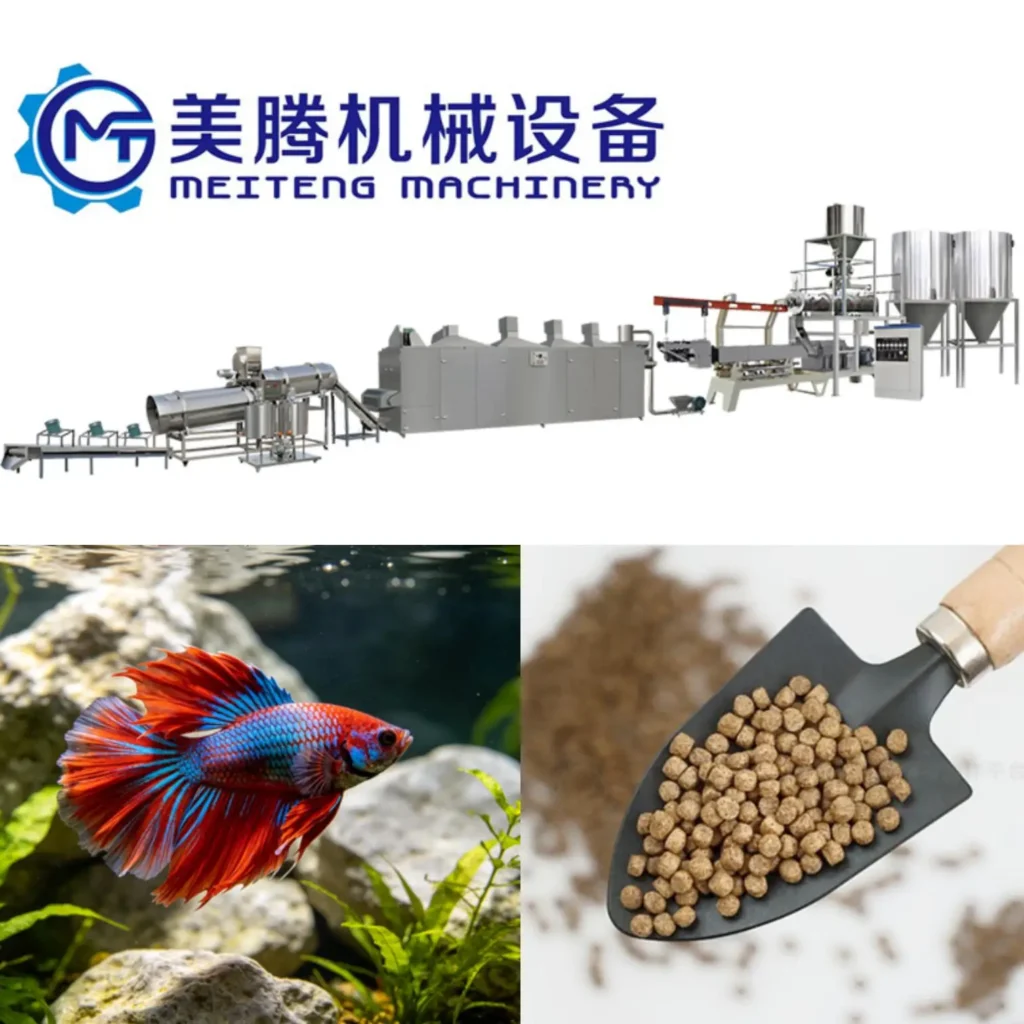
Equipment Catalogue Integrity — every station in this twin-screw line is specified to match throughput across mixing, extrusion, drying and coating, so no single machine bottlenecks the next.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin-Screw Fish Feed Extrusion Production Line |
| Extruder Type | Twin-screw |
| Output Capacity | 1.0–1.2 t/h (basis not stated in source — confirm raw material formulation, moisture content, pellet diameter) |
| Construction Material | 304 stainless steel (contact parts) |
| Control System | PLC and MCC control (configurable) |
| Target Species | Trout, salmon, catfish, tilapia, shrimp |
| Pellet Type | Floating and sinking feed |
| Line Stations | Batching, extrusion, drying, coating, cooling, packing (verify against quotation) |
| Screw Configuration | Matched to raw material and target pellet density |
| Die Design | Specified to target pellet size and shape |
| Voltage & Frequency | To be confirmed with buyer’s market |
| Control Language | To be confirmed |
| Standards | CE, ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Floating aquaculture feed | Corn, wheat, soybean meal, fish meal blends for trout and salmon |
| Sinking aquaculture feed | High-protein formulations for catfish and shrimp |
| Multi-species production runs | Die and screw changes between tilapia, catfish, and salmon formulations |
| High-protein kibble | Meat meal, soy protein concentrate, and starch binders for predatory fish |
Why Matching Dryer Capacity to Extruder Output Matters on a Fish Feed Processing Line for Sale
An extruder running at full rate means nothing if the dryer cannot pull moisture down to shelf-stable levels before pellets reach the coating drum.
I once saw a 1.0 t/h twin-screw line in a tilapia plant where the extruder pushed pellets faster than the dryer could handle. Moisture readings at the cooler inlet stayed above safe storage limits, and the packing team was bagging feed that later caked inside woven bags. The mill blamed the extruder, but the real fault was an undersized dryer ordered as an afterthought. When evaluating any fish feed processing line for sale, the buyer must confirm that every station — from batching through drying to coating — carries a matched capacity rating based on the actual formulation, not just a headline number [NEED_CITE: dryer residence time versus pellet diameter and initial moisture].
Every Station Visible in One Equipment Catalogue
The value of surveying a full equipment range before specifying a line is that you can see where throughput gaps appear. A twin-screw extruder rated at 1.0–1.2 t/h on a given formulation must be followed by a dryer with sufficient belt area and airflow to reduce pellet moisture within the target window. If the coating drum is too small, fat and palatant application becomes uneven, and the final product fails sensory tests at the farm. This page lays out each station — batching system, extruder, dryer, flavouring drum, cooler, packing — so the buyer can read across the catalogue and confirm that no single unit creates a choke point.
How Screw and Die Selection Shapes Pellet Density
Floating feed for trout and sinking feed for catfish start from the same twin-screw extruder platform but diverge at the screw configuration and die geometry. A longer barrel with higher shear promotes starch gelatinisation and traps more air cells in the pellet, giving the buoyancy that salmon and trout farmers expect. Sinking pellets need lower expansion, which means a different screw profile, reduced barrel temperature, and a die with smaller orifices that compress the dough rather than let it expand. The extruder itself does not change; the internal configuration does, and the specification record should document which screw elements and die plates ship with the line so that future changeovers are repeatable [NEED_CITE: twin-screw extrusion parameters for floating versus sinking aquaculture pellets].
Reading the Specs That Actually Affect Pellet Quality
Screw configuration determines residence time and shear energy inside the barrel. A combination of kneading blocks and reverse elements can be swapped to control how long high-protein or high-starch blends stay in the cooking zone, which directly influences gelatinisation degree and pellet durability.
Die orifice diameter governs pellet size before drying shrinkage. A 3 mm die will not produce a finished 3 mm pellet; moisture loss during drying contracts the diameter, and the relationship varies with formulation fat content and dryer temperature profile.
304 stainless steel contact parts resist the chloride load in fish meal and premix blends, preventing corrosion pitting that would otherwise contaminate feed and shorten barrel life in humid coastal mill environments.
PLC and MCC control allows the operator to save recipes for each species, locking in screw speed, barrel zone temperatures, and feeder ratios so that a catfish run on Monday and a tilapia run on Wednesday start from identical parameter sets, reducing off-spec product at changeover.
The Hidden Cost of Skipping the Trial Run
When an extruder ships without a trial on the buyer’s actual raw material, the first commissioning day becomes a product development exercise. I worked on a project where the supplier configured the screw profile around a standard fish meal formulation, but the buyer’s local soy-heavy blend had different viscosity and oil absorption. Pellets exited the die too soft, collapsed in the dryer, and the mill lost several shifts of production before the correct screw elements arrived by air freight. That downtime could have been avoided with a pre-shipment trial in the supplier’s testing workshop [NEED_CITE: importance of raw material trial runs in extrusion equipment procurement].
Why This Equipment Range Stands Up to Scrutiny
The complete line is specified under one supplier, meaning throughput calculations between the extruder, dryer, and coater are coordinated rather than left to the buyer to reconcile from separate vendors. Screw and die configurations are documented against the buyer’s raw material, not copied from a generic build. An in-house testing workshop allows the buyer’s formulation to run before the machine is crated, producing a trial report that becomes the baseline for commissioning. Every food-contact surface uses 304 stainless steel, which matters when fish meal chlorides accelerate wear on cheaper alloys. PLC and MCC panels are wired and labelled in the control language the buyer confirms before production starts, so the first operator training session happens on a familiar interface.
Documentation & Verification
- Screw and die configuration record matched to your target pellet density and species
- Line layout showing every station and its throughput rating relative to extruder output
- Trial run report on your raw material formulation before the line ships
- Electrical schematic with voltage and frequency locked to your site supply
- CE declaration of conformity covering the complete extrusion assembly
Installation, Commissioning & Support
- Foundation loading plan based on extruder and dryer weight distribution for this line
- Power distribution schedule confirming PLC panel voltage and dedicated dryer circuit amperage
- Assembly sequence for twin-screw barrel sections and die plate alignment on site
- First-run parameter setting against the pre-shipment trial report baseline
- Operator training on recipe selection and screw changeover procedures
- Wear parts list covering screws, dies, and barrel liners with reorder intervals
What to Share Before Requesting a Quotation
To size each station correctly, send the formulation you will actually run — including protein, starch, and fat percentages along with moisture at the mixer outlet. Specify the target pellet diameter range and whether you need floating, sinking, or both. Confirm the voltage and frequency at your mill so the MCC and PLC panels are built for your grid, and state the control language your operators need on the HMI screens.
Frequently Asked Questions
Q: What is the difference between twin-screw and single-screw extruders for fish feed?
A: Twin-screw extruders handle a wider range of formulations, especially high-fat or high-moisture blends, because the intermeshing screws provide positive conveying and self-cleaning action. Single-screw designs work well on simpler starch-rich recipes but struggle with the protein variability common in aquaculture feed.
Q: How do I choose the right dryer capacity to match the extruder output?
A: Dryer capacity depends on pellet diameter, initial moisture leaving the die, and target final moisture. Request a heat and mass balance calculation from the supplier based on your formulation, rather than matching only the extruder’s hourly tonnage rating.
Q: Which stations do I need for floating versus sinking feed production?
A: Both lines share batching, extrusion, drying, coating, and cooling stations. Floating feed typically requires a higher expansion die and possibly a post-extrusion conditioning step, while sinking feed needs a densification die and lower dryer temperatures to preserve pellet integrity.
Q: Can individual machines be purchased separately to upgrade an existing line?
A: Yes. Each station in the catalogue — extruder, dryer, coating drum, cooler — can be specified and quoted on its own. Provide the throughput and interface dimensions of your current equipment so the replacement unit is matched correctly.