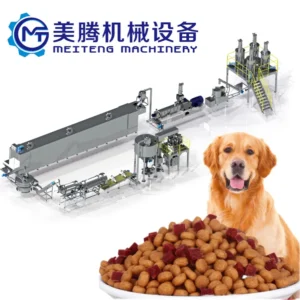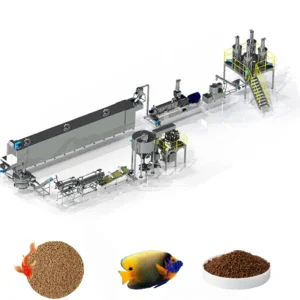
Matched Throughput Across Stations — every unit from the mixer to the cooler is sized against the same output target, eliminating the bottleneck that forms when an extruder outruns its dryer.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Aquatic Feed Extrusion Production Line |
| Extruder Type | Twin-screw |
| Output Capacity | 500 kg/h (basis not stated in source — confirm raw material formulation / moisture content / pellet diameter) |
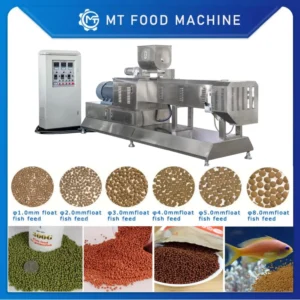
| Pellet Size Range | 0.5 mm – 12 mm (adjustable) |
| Main Structure Material | Stainless steel |
| Control System | Simple control panel |
| Line Stations | Feeding, mixing, extruding, pelletizing, drying, cooling |
| Automation Level | Fully automatic continuous operation |
Application Suitability
| Application | Material or Output |
|---|---|
| Floating fish feed for grow-out stages | Fish meal, soybean meal, corn flour blends formed into 3 mm – 12 mm pellets |
| Fry and fingerling feed production | High-protein formulations processed into 0.5 mm – 2 mm micro-pellets |
| Continuous aquatic feed factory operation | Integrated drying and cooling for stable pellet moisture before bagging |
| Species-specific feed runs | Catfish, tilapia, and shrimp formulations with varying starch and lipid content |
What a "500 kg/h Fish Feed Making Machine for Sale" Actually Means on Your Floor
Capacity is only real when the dryer and cooler can keep pace with the extruder at that same rate.
I have watched lines stall within the first month because the pellet output exceeded what the downstream dryer could handle. Moisture stays trapped inside the pellet, mold shows up in the warehouse, and the whole aquatic feed extrusion line backs up to the die face. When capacity is quoted without a matched drying and cooling calculation, the number is just a motor rating, not a production reality [NEED_CITE: matching extruder output to dryer evaporation rate in feed milling].
How Each Station Links to the Next
The feeding and mixing stage sets the moisture and protein ratio that the twin-screw extruder will work with. If the mixer batches faster than the extruder can accept, material sits and segregates; if slower, the screws run starved and pellet density drifts. This fish feed making machine for sale keeps those intervals aligned so the extruder barrel stays consistently loaded.
Why Stainless Steel Matters in a Feed Mill
Aquatic feed formulations are high in fish meal and marine oils, and the humidity inside a drying chamber accelerates corrosion on untreated surfaces. Stainless steel contact parts and structural frames resist that environment. Over successive production runs, this keeps pellet surfaces free from flaking scale and reduces the cleaning time between formulation changeovers [NEED_CITE: corrosion behavior of carbon steel versus stainless steel in high-humidity feed processing].
Reading the Specs That Actually Shape the Pellet
The twin-screw configuration gives this line a self-wiping action that handles sticky, high-protein aquatic formulations without material building up on the flight edges. Pellet size adjustment from 0.5 mm to 12 mm is achieved through die changes, meaning one extruder covers fry feed through grow-out feed without a second machine. The simple control panel centralizes parameter adjustments for barrel temperature zones and screw speed, keeping batch-to-batch consistency within a practical range for small and medium mills. Because voltage and frequency are not pre-set in the spec sheet, confirming your site’s electrical standard before production avoids motor rewinding delays at commissioning.
The Hidden Cost of an Undersized Dryer
When the dryer capacity is quoted independently from the extruder, pellets leave the chamber above safe storage moisture. In humid climates that gap narrows further, and a line that performs acceptably in winter can spoil product through summer. Re-drying batches doubles your energy cost and cuts effective throughput in half, which is a loss no spec sheet warns you about in advance [NEED_CITE: safe moisture thresholds for stored aquatic feed pellets in tropical climates].
Why Source the Full Line from One Equipment Supplier
The entire aquatic feed extrusion line is configured under one layout calculation, so the mixer batch cycle, extruder throughput, dryer residence time, and cooler airflow are all set to the same target. Screw and die configurations are specified against your actual raw material rather than copied from a generic template. An in-house testing workshop runs your formulation before shipment, producing a trial report that confirms pellet float rate and density. Documentation covers line layout, electrical schematics, and wear parts lists so your maintenance team is not guessing at first replacement. Pre-sales consultation extends through on-site installation and operator training, which reduces the gap between delivery and stable production.
Documentation & Verification
- Line layout drawing showing station spacing and throughput match for your target pellet size
- Screw and die configuration record tied to your specific fish meal and starch formulation
- Trial run report from in-house testing workshop on your raw material before dispatch
- Electrical schematic with confirmed voltage, frequency, and control panel language
- Wear parts list with part numbers for screws, dies, and dryer screen panels
- Operation and maintenance manual covering daily inspection and lubrication intervals
Installation, Commissioning & Support
- Foundation plan based on the line footprint and extruder vibration load
- Dedicated power circuit sized to the total connected kW of all stations
- Modular station delivery allowing phased placement if workshop access is limited
- First-run parameter setting for barrel zones, screw speed, and dryer temperature
- Operator training covering die changes across the 0.5 mm – 12 mm pellet range
- Spare screw and die elements stocked for first replacement cycle
What to Prepare Before Requesting a Quotation
To get a line configuration that reflects your actual production conditions, share your raw material formulation including protein and starch percentages, the pellet diameter range you need, and your target daily output. Confirm your site voltage, frequency, and preferred control language. If you already have upstream milling or downstream packing equipment, provide their capacity so the aquatic feed extrusion line can be matched at both ends.
Frequently Asked Questions
Q: How is the 500 kg/h capacity verified for my formulation?
A: That figure is referenced without a stated raw material basis, so it needs confirmation against your specific formulation, moisture content, and pellet diameter. We run your actual material in the testing workshop and document the measured output in a trial report before finalizing the line specification.
Q: What electrical standards will the line be built to?
A: Voltage, frequency, and control panel language are not preset in the base specification. We confirm your site’s electrical standard during the quotation stage and reflect it in the electrical schematic before production begins, so motors and controls arrive ready for connection.
Q: How are screw and die configurations chosen for floating pellets?
A: Screw pitch, flight depth, and die land length are selected based on your formulation’s starch-to-protein ratio and the target pellet density. Floating pellets require higher expansion at the die face, which is achieved through specific barrel temperature profiles and die geometry matched to your material.
Q: Is the dryer capacity matched to extruder output?
A: Yes. The dryer and cooler in this line are sized to handle the extruder’s output at the quoted throughput target, so pellets reach safe storage moisture in a single pass. The line layout calculation documents the evaporation rate and residence time for your specific pellet diameter.