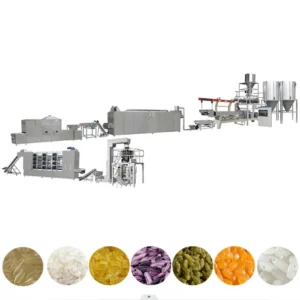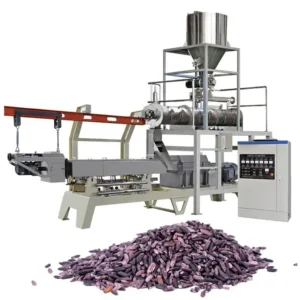
Complete Equipment Matching — every station from batching to packing is specified under one roof, so throughput is balanced across the mixer, extruder, dryer, roaster, and packer rather than assembled from mismatched vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Nutritional Fortified Artificial Rice Production Line |
| Models Available | MT65, MT70, MT85, MT75, MT95 |
| Screw Type | Twin-screw (single-screw feeding option available based on material) |
| Installed Power (MT65) | 85 kW |
| Installed Power (MT70) | 120 kW |
| Installed Power (MT85) | 235 kW |
| Installed Power (MT75) | 180 kW |
| Installed Power (MT95) | 260 kW |
| Power Consumption (MT65) | 60 kW |
| Power Consumption (MT70) | 85 kW |
| Power Consumption (MT85) | 165 kW |
| Power Consumption (MT75) | 135 kW |
| Power Consumption (MT95) | 195 kW |
| Output Capacity (MT65) | 80–100 kg/h (basis not stated in source — confirm raw material blend and moisture) |
| Output Capacity (MT70) | 100–120 kg/h (basis not stated in source — confirm raw material blend and moisture) |
| Output Capacity (MT85) | 200–300 kg/h (basis not stated in source — confirm raw material blend and moisture) |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material blend and moisture) |
| Output Capacity (MT95) | 800–1000 kg/h (basis not stated in source — confirm raw material blend and moisture) |
| Overall Dimensions (MT65) | 28 × 1.2 × 2.2 m |
| Overall Dimensions (MT70) | 30 × 1.5 × 2.2 m |
| Overall Dimensions (MT85) | 34 × 3.5 × 4.3 m |
| Overall Dimensions (MT75) | 32 × 3.5 × 4.3 m |
| Overall Dimensions (MT95) | 36 × 3.5 × 4.3 m |
| Control System | Frequency speed control with automated operation |
| Lubrication | Automatic lubrication and cooling system |
| Heating Source (Dryer) | Electric or gas |
| Production Procedure | Mixing → Extruding → Vibrating → Low-temperature drying → Cooling → High-temperature roasting → Cooling → Packing |
| Key Features | CE certified, twin-screw extrusion, automated PLC and MCC control available, in-house trial run before shipment |
Application Suitability
| Application | Material or Output |
|---|---|
| Nutritional fortified rice kernel production | Broken rice, rice bran, corn, millet, wheat, oats, buckwheat, bean, starch with added vitamins and minerals |
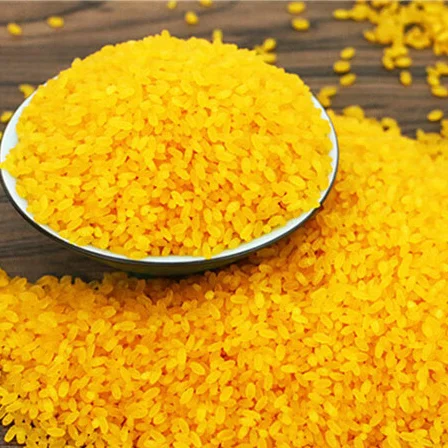
| Artificial rice reconstitution | Broken rice and rice bran blended and extruded into whole-grain-shaped kernels |
| Micro-nutrient fortified grain products | Cereal and legume blends supplemented with iron, zinc, vitamin A, and folic acid |
| High-nutrition extruded food processing | Multi-grain formulations requiring controlled gelatinisation and density |
What Happens When the Dryer Cannot Keep Up with the Extruder
A bottlenecked line runs at the speed of its slowest station, not the extruder nameplate.
I once saw a nutritional rice line where the extruder was rated for a solid mid-range output but the mesh-belt dryer was sized one tier too small. The operator had to throttle the extruder feed rate to prevent wet, half-dried kernels from piling up at the dryer discharge. Over a full shift that meant the entire nutritional rice production line full equipment range ran well below the expected throughput, and the owner blamed the extruder when the real problem was a mismatch downstream. Matching every station to the same target capacity is the foundation of a line that actually delivers. [NEED_CITE: throughput balancing principles in continuous food processing lines]
Station-by-Station Capacity Alignment
When surveying the nutritional rice production line full equipment range, buyers need to verify that each station can handle the output the extruder pushes through. The mixing and batching system must meter raw material at a rate consistent with the extruder barrel volume and screw speed. The vibrating conveyor after extrusion separates and spreads kernels before they enter the dryer, preventing clumping that would otherwise create uneven moisture profiles. Each of the five extruder models — MT65 through MT95 — is paired with drying and roasting equipment sized to the same throughput tier, so no single section limits the rest.
Drying and Roasting Sequence Explained
The low-temperature drying stage removes surface moisture gradually, which stabilises kernel shape before the high-temperature roasting pass. The mesh belt speed is controlled by a frequency motor, allowing operators to adjust residence time depending on the moisture content of the incoming extrudate. Electric or gas heating sources are both available, and the choice often depends on local energy costs and workshop utility infrastructure. After roasting, a second cooling station brings kernel temperature down before packing to prevent condensation inside sealed bags. [NEED_CITE: food-grade drying temperature profiles for extruded cereal products]
How Screw Configuration Affects Gelatinisation and Kernel Density
Twin-screw extrusion is the core of this line because the intermeshing screw elements provide the shear and residence time needed to fully gelatinise starches from broken rice, corn, and millet blends. The screw configuration and die design are selected based on the buyer’s raw material formula — a high-fibre bran-heavy blend requires a different element arrangement than a pure starch mix. The automatic lubrication and cooling system keeps barrel temperature within a controlled band, which matters because starch gelatinisation temperature windows are narrow. Frequency speed control on the main motor lets operators fine-tune screw RPM without stopping the line, maintaining consistent kernel density across long production runs.
When the Extruder Torque Is Not Enough for the Actual Formula
A few years back a customer sourced a line configured at the lowest price point, and the extruder screw torque could not handle the high-viscosity multi-grain formula they actually ran. Within three months the barrel was clogging, production stopped, and they waited for replacement parts. Every project now starts with a material trial run in our testing workshop before the line ships. The screw elements and die openings are reconfigured to the buyer’s specific blend, which adds time up front but prevents the kind of on-site failures that cost far more. [NEED_CITE: twin-screw torque requirements for high-viscosity cereal formulations]
Why Sourcing the Full Range from One Supplier Matters
A single source for the nutritional rice production line full equipment range means throughput calculations are done once across the entire chain, not negotiated separately with each vendor. The line layout and capacity document shows how many kilograms per hour each station is rated for, so mismatches are caught before metal is cut. Screw and die configuration records are tied to the buyer’s raw material, not copied from a generic build. Electrical schematics are confirmed against the destination country’s voltage and frequency before production begins, avoiding commissioning delays. The in-house testing workshop allows trial runs on the buyer’s actual formula so product development starts before installation, not after.
Documentation & Verification
- Line layout drawing with throughput matched across mixer, extruder, dryer, roaster, and packer
- Machine specification sheet for each model including screw configuration record
- Electrical schematic with voltage and frequency confirmed for destination market
- Trial run report on customer raw material from in-house testing workshop
- Factory test record covering continuous run before dispatch
- CE declaration of conformity covering the complete line assembly
Installation, Commissioning & Support
- Foundation and floor space planning based on overall line dimensions up to 36 m long for the MT95 configuration
- Dedicated electrical circuits sized to installed power requirements ranging from 85 kW to 260 kW depending on model
- Assembly from modular sections with station-by-station alignment verification during commissioning
- Screw and die configuration adjustment on site based on initial production run with buyer’s formula
- Operator training covering frequency speed control, automatic lubrication system monitoring, and dryer belt tensioning
- Wear parts list provided at shipment including spare screw elements, die plates, and mesh belt sections
Preparing Your Inquiry
To move forward with a line configuration, share your raw material formula including moisture content, the grain or legume types in the blend, and the vitamin or mineral additives you plan to incorporate. Let us know your target hourly output and the voltage, frequency, and control language your workshop requires. If you have existing upstream milling or downstream packing equipment, tell us the interface specifications so we can match the connection points. We will then prepare a station-by-station layout and schedule a trial run on your material before final quotation.
Frequently Asked Questions
Q: How is capacity verified on my actual raw material blend, and what does the rated output assume?
A: The output figures listed for each model are based on standard reference conditions that may not match every formulation. Before shipment, we run your specific raw material blend in the in-house testing workshop and record actual throughput, kernel density, and moisture levels. The trial run report confirms whether the selected model meets your target or if a larger extruder is needed.
Q: Which supporting stations are matched to each extruder model to avoid line bottlenecks?
A: Each extruder model from MT65 through MT95 is paired with a dryer, roaster, and cooler sized to handle the same throughput tier. The capacity calculation document shows rated output at every station, not just the extruder, so you can verify no downstream bottleneck exists before committing to the line specification.
Q: What voltage, frequency, and control language options are available for different target markets?
A: Electrical schematics are prepared after confirming the destination market’s utility standards. Frequency speed control panels and automated operation interfaces can be configured for local voltage and language requirements. This confirmation step happens before production to prevent commissioning delays on site.
Q: Can individual stations be purchased separately, or is the line only offered as a complete package?
A: Individual stations such as the drying oven or roasting unit can be supplied separately for integration into existing lines. However, throughput matching across stations is most reliable when the full range is specified together, allowing capacity calculations to account for every transition point from mixer through packer.
Q: What spare wear parts are included with the initial shipment, and how are replacements sourced?
A: The initial shipment includes a wear parts list covering screw elements, die plates, and dryer mesh belt sections sized for the specific line configuration. Replacement parts are manufactured to the same screw configuration and die design records held on file, ensuring compatibility when the first changeover is due.