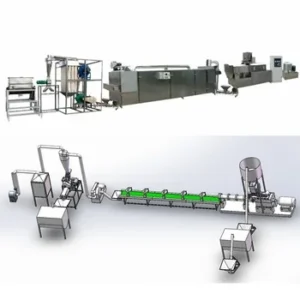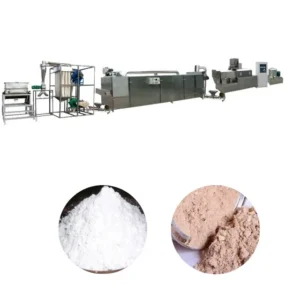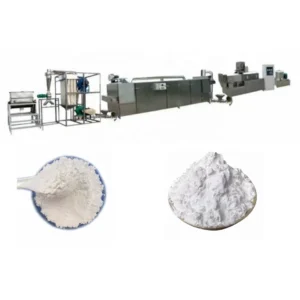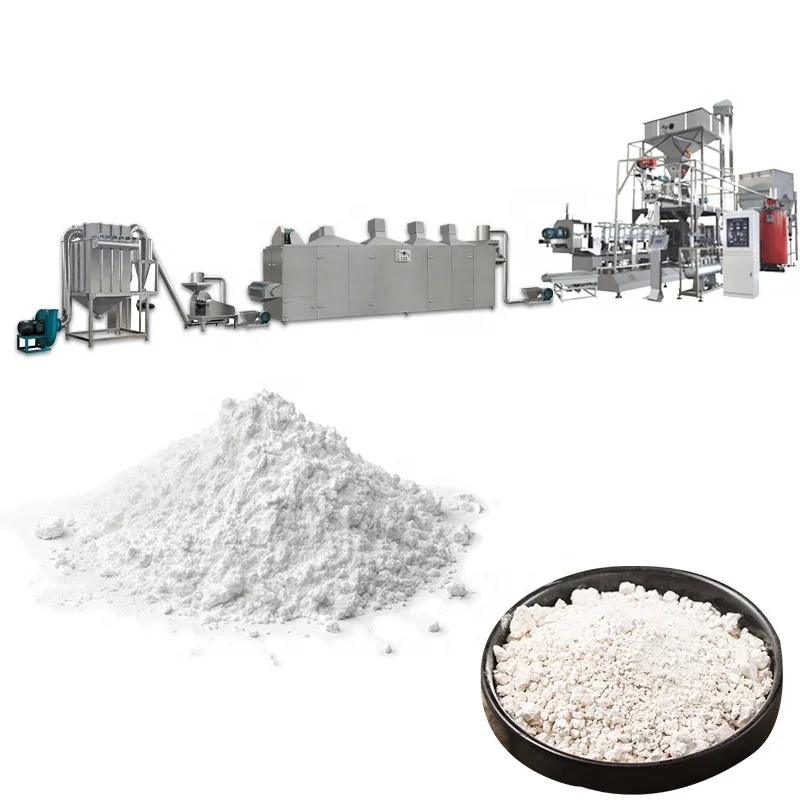
Matched Throughput Across Every Station — each mixer, extruder, dryer and grinder is sized to the same output target so the modified starch processing line full equipment range runs without bottlenecks.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Modified Starch Processing Line (Twin-Screw Extrusion) |
| Screw Type | Twin-screw |
| Installed Power | 180 kW |
| Power Consumption | 135 kW |
| Output Capacity | 200–250 kg/h (basis not stated in source — confirm raw material / moisture) |
| Overall Dimensions (L×W×H) | 32000×3500×4300 mm |
| Voltage & Frequency | 380 V, 50 Hz, Three Phase (full-line voltage per destination to confirm) |
| Control System | Frequency conversion speed regulation on feeding, driving and rotary cutting |
| Mixer Capacity Options | 20–30 kg/time, 70–80 kg/time, 170–180 kg/time |
| Mixer Power Options | 4 kW / 7.5 kW / 15 kW |
| Mixer Stainless Steel Grade | 201 S.S. or 304 S.S. |
| Dryer Type | Multi-layer mesh belt, double pitch roller chain transmission, round-trip drying |
| Pulse Grinder Drive Motor | 15 kW |
| Grinder Mesh | 100–120 |
| Line Stations | Mixer → Twin-screw extruder → Dryer → Pulse grinder → Packaging machine |
Application Suitability
| Application | Material or Output |
|---|---|
| Pregelatinised starch for food ingredients | Corn starch, maize starch |
| Modified starch for industrial adhesives | Cassava starch, tapioca starch |
| Oil-drilling fluid-loss-agent starch | Potato starch, corn starch blends |
| Denatured starch for textile sizing | Tapioca starch, cassava starch |
| Pre-cooked starch for instant food mixes | Potato starch, maize starch |
Why "Rated Output" Means Nothing Without the Raw Material Context
Capacity figures only hold when the screw profile and barrel temperatures match your exact starch feedstock and moisture content.
I have seen processors order a line based on a headline throughput number, only to discover their cassava-to-tapioca ratio demands a completely different screw element sequence. The extruder runs, but the gelatinisation degree stays below what the market requires, and the batch is reworked or scrapped. When buyers evaluate a modified starch processing line full equipment range, the conversation must start with the raw material certificate of analysis, not the brochure [NEED_CITE: starch gelatinisation temperature ranges by botanical source].
Frequency-Conversion Feeding and Driving for Batch Consistency
The MT75 uses frequency-conversion speed regulation on the feeding system, main drive and rotary cutting unit. This arrangement lets operators fine-tune the feed rate independently of screw speed, which matters when switching between corn starch and cassava starch because the two materials respond differently to shear input. Maintaining a stable residence time inside the barrel keeps the gelatinisation window consistent from the first kilogram to the last.
Multi-Layer Dryer Geometry and Moisture Uniformity
The dryer section uses a multi-layer mesh belt with a double pitch roller chain and a round-trip airflow path. Starch pellets enter at one end, travel back and forth across successive layers, and exit at a moisture level low enough for safe grinding. The round-trip design keeps the overall footprint compact while providing the dwell time that pregelatinised starch needs to release internal moisture without surface case-hardening [NEED_CITE: drying curve requirements for pregelatinised starch pellets].
Reading the Power and Dimension Data
Installed power of 180 kW and operating consumption of 135 kW indicate a load factor typical of twin-screw extrusion where the main motor rarely runs at full nameplate rating during steady-state starch processing. The 32-metre line length reflects the sequence of mixing, extrusion, multi-layer drying and grinding; buyers should verify ceiling height against the 4.3-metre dryer and conveyor elevations. Frequency conversion on three separate subsystems means the electrical cabinet houses multiple variable-frequency drives, so the destination-site transformer must handle the aggregate starting current without voltage dip.
The Cost of Mismatched Stations Downstream
An extruder that delivers stable output means little if the dryer cannot remove moisture fast enough, or if the grinder sieve jams on semi-dry pellets. Bottlenecks like these force operators to throttle the extruder feed, turning a nominal capacity figure into an optimistic ceiling. Reworking off-spec starch also consumes additional electricity and labour while delaying shipments [NEED_CITE: hidden cost of downstream bottlenecks in continuous food processing lines].
Why Sourcing the Full Equipment Range From One Supplier Matters
Every station in this modified starch processing line full equipment range is configured under a single engineering responsibility, so conveyor heights, utility tie-in points and control signals align before the machines leave the factory. Screw and die configurations are selected after trial runs on the buyer’s actual starch sample rather than copied from a generic build. The in-house testing workshop allows raw-material validation before shipment, reducing on-site commissioning surprises. Documentation — from electrical schematics to wear-parts lists — references one set of station identifiers instead of a patchwork of vendor codes.
Documentation & Verification
- Line layout drawing showing station sequence and utility connection points for the MT75 footprint
- Screw and die configuration record matched to your starch feedstock
- Electrical schematic confirming voltage, frequency and VFD ratings
- Factory test record documenting run parameters on your raw material sample
- CE declaration of conformity and ISO certificate in electronic format
Installation, Commissioning & Support
- Foundation must accommodate 32 m line length and 4.3 m maximum equipment height
- Three-phase 380 V 50 Hz supply with dedicated circuit for 180 kW extruder main drive
- Frequency-conversion drives require parameter setting during first power-on
- Trial-run results transferred to on-site commissioning parameter sheet
- Operator training covers sieve mesh changes on the 15 kW pulse grinder
- Wear parts list specifies screw elements, die plates and mesh screens for stocking
Preparing Your Inquiry
Share your starch type, typical moisture percentage and the gelatinisation or modification degree your product specification demands. Include the destination-site voltage and frequency, available workshop length and ceiling height, and whether you need the line to integrate with an existing upstream batching system or downstream packing hall.
Frequently Asked Questions
Q: How is each station’s capacity matched so the line runs at its rated output without bottlenecks?
A: Mixer batch size, extruder throughput, dryer belt speed and grinder feed rate are all calculated against the same hourly target. Conveyor widths and motor ratings are then selected to carry that flow without accumulation or starvation at any transfer point.
Q: What raw material types does each extruder model handle, and how does screw configuration change?
A: Corn, cassava, potato, maize and tapioca starch each have distinct gelatinisation temperatures and shear sensitivity. Screw element sequences and die geometries are adjusted after a trial run on the buyer’s sample to reach the required modification degree.
Q: Can individual machines be ordered separately to retrofit an existing starch line?
A: Yes. The dryer, pulse grinder or packaging machine can be supplied as standalone units. Interface dimensions, belt widths and control signals are matched to the existing upstream equipment during the engineering review.
Q: What voltage and control-panel language options are available?
A: The standard configuration is 380 V 50 Hz three-phase, but motor ratings and transformer taps can be adapted to destination requirements. Control-panel labels and HMI text are confirmed with the buyer before the cabinet is wired.
Q: Which supporting stations are included versus optional?
A: The standard sequence covers mixer, extruder, dryer, grinder and packaging machine. Upstream raw-material silos, dust-extraction ductwork and downstream pallet conveyors are quoted separately based on site layout and local regulations.