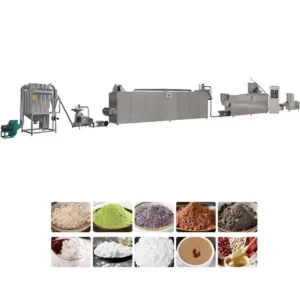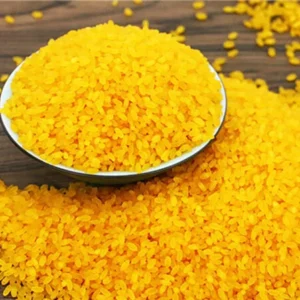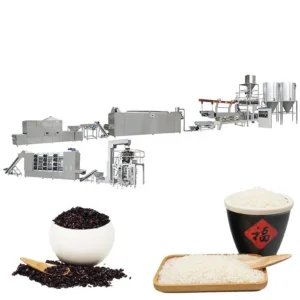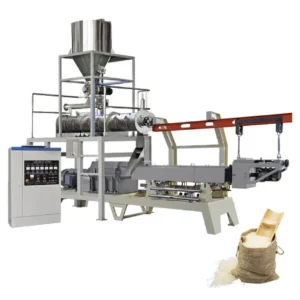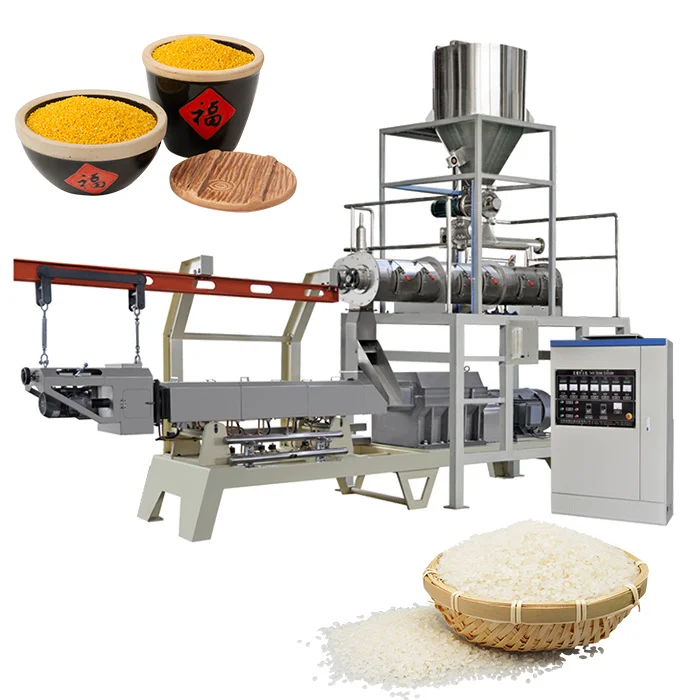
Integrated Throughput Matching — Every station from mixer to fryer is sized so the extruder never waits on upstream or downstream units, verified during factory trial runs on your grain formulation.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Artificial Rice Production Line |
| Output Capacity | 70–300 kg/h (basis to be confirmed against raw material type, moisture, and grain formulation) |
| Voltage & Frequency | 380V / 50Hz (configurable to site standard) |
| Construction Material | Food-grade stainless steel on all product-contact surfaces |
| Line Stations | Mixer, extrusion system, fryer, and downstream auxiliaries |
| Control System | Automatic control with PLC or MCC option |
| Color | Silver |
| Assembly State | Complete line integration, pre-assembled for site connection |
| Raw Material Compatibility | Rice flour and grain-based materials |
| Customization Scope | Minor adjustments, drawing-based adaptation, or full redesign |
| Packaging | Standard wooden case |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice production | Rice flour blended with micronutrient premix |
| Reconstituted rice manufacturing | Broken rice flour and grain-based binders |
| Multi-grain artificial rice | Blends of rice, corn, sorghum, or millet flour |
| Nutrition programme rice | Formulations with controlled iron, zinc, or vitamin content |
| Value-added grain processing | Custom starch-to-protein ratios for specialty rice shapes |
Why the Voltage Question Must Come Before Anything Else
Locking electrical standards at the inquiry stage prevents a month-long commissioning delay that no amount of on-site rewiring can shorten.
I once watched a Southeast Asian facility lose three full weeks because the extruder motors were rated for 50Hz while the local grid ran at 60Hz. Every variable frequency drive tripped into protection mode repeatedly, and the artificial rice production line full equipment range sat idle while replacement components shipped overseas. The buyer had focused entirely on throughput and price, leaving voltage as a footnote on the purchase order [NEED_CITE: voltage and frequency standards by export market]. That single oversight pushed the entire commissioning schedule back by a month and cost more in lost production than any price negotiation could recover.
Matching Every Station to the Extruder’s True Output
A common mistake in sourcing an artificial rice production line full equipment range is evaluating the extruder in isolation. The extruder may be rated for a certain output, but if the fryer belt speed or the mixer batch cycle cannot keep pace, the line runs in a stop-start pattern that degrades product consistency. Each station in this line is sized so the mixer delivers batches at intervals the extruder can absorb continuously, and the fryer residence time aligns with the extrusion rate to produce uniform color and texture across every grain.
Food-Grade Contact Surfaces Across the Entire Flow Path
Stainless steel construction on all product-contact surfaces means that from the mixer bowl through the extrusion barrel and into the fryer, no carbon steel component touches the rice dough or finished grain. This matters not only for food safety audits but also for cleaning efficiency between formulation changes [NEED_CITE: food contact material regulations for grain processing equipment]. When a plant switches from a plain rice flour recipe to a micronutrient-fortified blend, rapid washdown without corrosion risk keeps changeover windows short and prevents cross-contamination between batches.
How Extrusion Parameters Shape the Final Grain
The extrusion step determines whether the reconstituted rice holds its shape during cooking or disintegrates in the pot. Barrel temperature profile, screw speed, and die geometry together control the degree of starch gelatinisation inside each grain. Too little gelatinisation and the rice falls apart when boiled; too much and it becomes gummy. The die aperture and cutter speed define grain length and diameter, allowing producers to match the visual profile consumers expect in their regional market. Automatic control maintains these parameters within tight bands once the optimal window is established on the buyer’s specific formulation, reducing operator-dependent variation between shifts.
What a Mismatched Line Costs After Startup
When throughput is not balanced across stations, the consequences appear weeks after installation. The extruder idles while waiting for the next mixer batch, or finished rice piles up ahead of an undersized fryer, cooling unevenly and developing surface cracks. Wear accelerates on screws and dies that cycle through repeated start-stop sequences rather than running at steady load [NEED_CITE: twin-screw wear patterns under intermittent operation]. Spare parts consumption rises, and the maintenance schedule collapses because components fail before their planned replacement interval.
What Distinguishes This Supplier’s Approach
Every station is sourced and configured under one responsibility, so throughput matching is not left to the buyer to reconcile across separate vendors. Screw configuration and die geometry are specified against the buyer’s actual rice flour blend, not copied from a generic build. The in-house testing workshop runs the buyer’s raw material before shipment, producing a trial run report that confirms output, grain shape, and cooking integrity. Electrical schematics and voltage confirmation are locked before production begins, not discovered at commissioning. Ongoing support covers operator training, wear parts supply, and maintenance scheduling once the artificial rice production line full equipment range is running on site.
Documentation & Verification
- Line layout drawing showing station spacing and utility connection points
- Machine specification sheet listing throughput at each station for bottleneck review
- Screw and die configuration record matched to your rice flour formulation
- Trial run report on your raw material confirming grain shape and cooking stability
- Electrical schematic with voltage, frequency, and control language confirmed pre-production
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation and floor space plan aligned to the line’s station footprint and utility drops
- Dedicated electrical circuit sizing for the 380V extruder motor and fryer heating elements
- Station-by-station assembly sequence with alignment checks between extruder die and fryer infeed
- First-run parameter setting on your grain formulation, including barrel zones and screw speed
- Operator training covering recipe changeover, die cleaning, and fryer temperature adjustment
- Wear parts list with screw, die, and fryer belt part numbers confirmed available at first replacement
Preparing Your Inquiry
To move from a general specification to a line configuration that fits your facility, share your target rice formulation including flour type and any fortification premix, your required daily output in kilograms, and the voltage and frequency standard at your plant. If you have an existing factory floor plan, include dimensions so the layout can be adapted around structural columns and utility routes. Specify the control interface language your operators need and whether you want a trial run on your raw material before the line ships.
Frequently Asked Questions
Q: How is the output capacity of 70–300 kg/h verified, and what raw material formulation is it based on?
A: The capacity range depends on your specific rice flour blend, moisture content, and grain formulation. A trial run using your actual raw material in the testing workshop confirms the achievable throughput before the line ships, so the figure on your quotation reflects your product rather than a generic benchmark.
Q: Which line stations are included, and how is throughput matched between them?
A: The line covers mixing, extrusion, frying, and downstream auxiliaries. Each station is sized so the mixer batch cycle, extruder output rate, and fryer belt speed align without bottlenecking, preventing the idle time or product pile-up that occurs when stations are sourced from separate vendors.
Q: What voltage and frequency options are available, and can the control interface be set to our local language?
A: The standard configuration is 380V / 50Hz, but voltage and frequency are confirmed against your facility’s electrical standard before production begins. The control interface language is specified at the same stage, ensuring operators can read alarms and setpoints in their working language from day one.
Q: Can the line layout be adapted to our existing factory floor plan?
A: Customization ranges from minor station repositioning to a full drawing-based redesign. Providing your floor plan with column positions, utility drop locations, and ceiling height allows the layout to be configured around your building constraints rather than requiring structural modification.
Q: What does the wooden case packaging include, and are all auxiliary components shipped together?
A: The standard wooden case covers the main line stations and their auxiliary components. Spare wear parts, fasteners, and connection fittings are packed within the same shipment, so nothing is left behind that would delay assembly when the containers arrive at your facility.