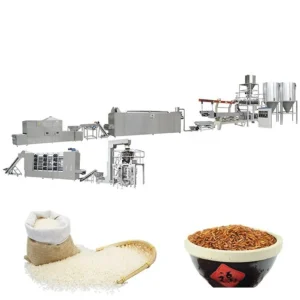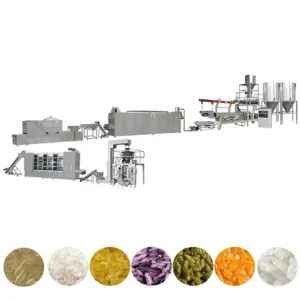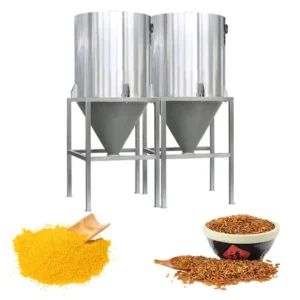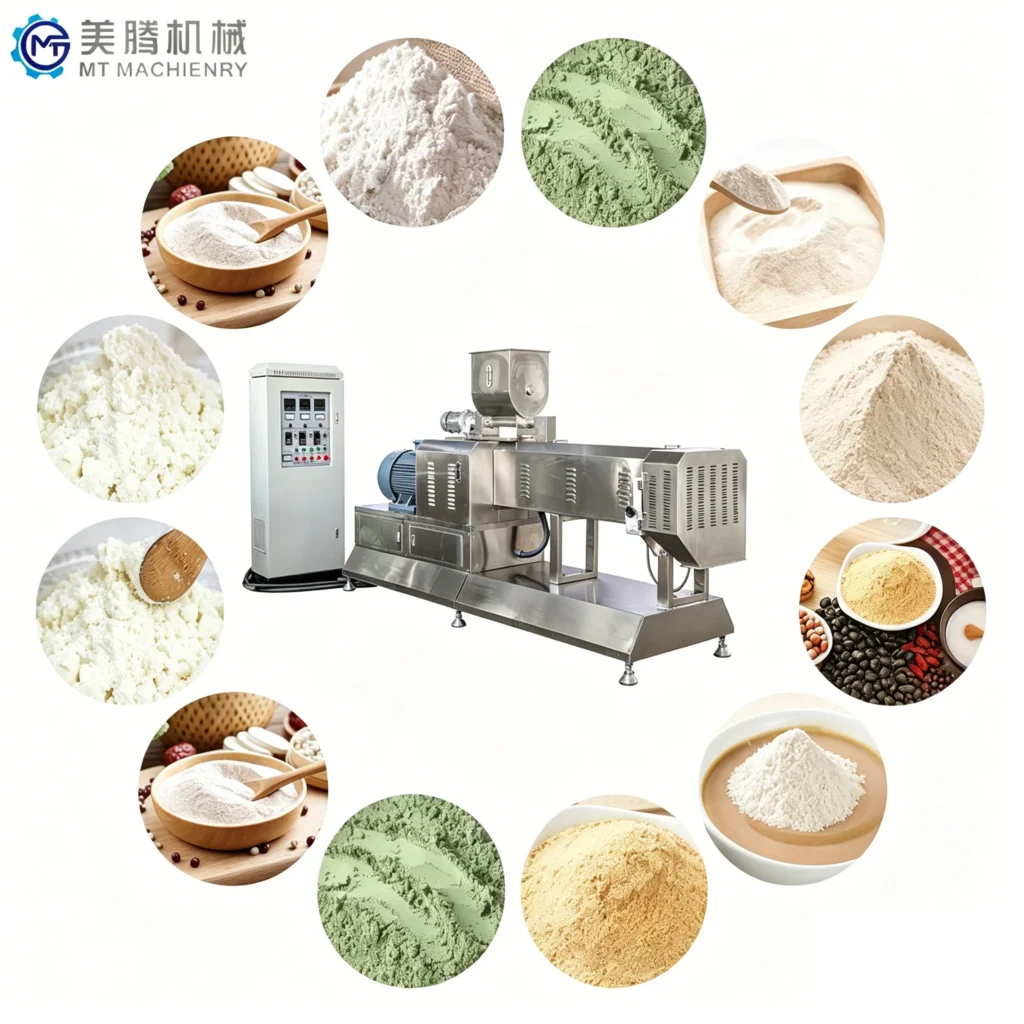
Throughput-Matched Stations — Every mixer, extruder, dryer, and grinder in this line is sized against the same formulation data, so no single station chokes the output you were promised.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruder Baby Rice Flour and Nutritional Powder Processing Line |
| Model Options | MT65 / MT70 / MT75 / MT85 |
| Screw Type | Twin screw |
| Extruder Barrel Material | Food-grade stainless steel |
| Installed Power (MT65) | 84 kW |
| Installed Power (MT70) | 160 kW |
| Installed Power (MT75) | 190 kW |
| Installed Power (MT85) | 210 kW |
| Power Consumption (MT65) | 59 kW |
| Power Consumption (MT70) | 120 kW |
| Power Consumption (MT75) | 140 kW |
| Power Consumption (MT85) | 150 kW |
| Output Capacity (MT65) | 120–150 kg/h (basis not stated in source — confirm raw material type, moisture content, and target powder mesh size) |
| Output Capacity (MT70) | 150–200 kg/h (basis not stated in source — confirm raw material type, moisture content, and target powder mesh size) |
| Output Capacity (MT75) | 200–250 kg/h (basis not stated in source — confirm raw material type, moisture content, and target powder mesh size) |
| Output Capacity (MT85) | 300–400 kg/h (basis not stated in source — confirm raw material type, moisture content, and target powder mesh size) |
| Voltage & Frequency | 380 V, 50 Hz, Three Phase (other voltage configurations available on request) |
| Control System | PLC and MCC control |
| Mixer Material | 304 stainless steel |
| Mixer Power Options | 4 kW / 7.5 kW / 15 kW |
| Mixer Batch Capacity | 20–30 kg / 70–80 kg / 170–180 kg per batch |
| Mixer Dimensions | 1000×900×1300 mm / 1300×1200×1500 mm / 1500×1400×1600 mm |
| Pulse Crusher Capacity | ~200 kg/h (basis not stated in source — confirm raw material and target fineness) |
| Pulse Crusher Power | 11 kW |
| Pulse Crusher Dimensions | 3000 × 900 × 2200 mm |
| Drying Oven Fuel Options | Electricity / Gas / Fuel (customer selectable) |
| Drying Oven Drive | Double pitch roller chain drive, round-trip drying |
| Line Stations | Mixing → Screw Conveying → Extruding → Air Conveying → Drying → Air Conveying → Pulse Grinding |
| Assembly State | Complete line, modular station configuration |
| Standards | CE, ISO |
| Warranty | One year free warranty |
Application Suitability
| Application | Material or Output |
|---|---|
| Baby rice flour production | Rice, brown rice, and grain blends processed into infant-grade powder |
| Infant nutritional powder | Cereal bases fortified with vitamins, trace elements, and protein |
| Fortified and artificial rice | Rice flour and starch blends extruded into reconstituted grain kernels |
| Modified starch processing | Pregelatinised starch from corn, cassava, or potato feedstock |
| Breakfast cereal and instant porridge powder | Whole grain and multi-grain formulations for hot cereal applications |
| Functional food powder | Therapeutic and dietary supplement bases requiring starch gelatinisation |
What "Rated Capacity" Hides When You Buy a Nutritional Powder Line
The number on the nameplate is not the number your raw material will produce.
I watched a buyer in Southeast Asia accept a twin screw extruder nutritional powder processing line rated at a certain hourly output, only to find that his local brown rice — higher in bran oil and fibre than the supplier’s test grain — dropped actual throughput and wrecked the gelatinisation window. The extruder ran, but the powder failed every lab test for expansion rate and starch conversion. A capacity figure without raw material, moisture content, and target mesh size attached to it is just a starting point for negotiation [NEED_CITE: how raw material composition affects extrusion throughput and gelatinisation].
This is the reason every model on this page — MT65 through MT85 — lists output ranges alongside a note to confirm the basis. Before a line ships, the testing workshop needs to run your actual formulation, lock the screw configuration, and document what comes out the die. That report is the only capacity number that matters.
Every Station in the Catalogue and How They Connect
The twin screw extruder nutritional powder processing line on this site covers the full station sequence: batching mixer, screw conveyor, twin screw extruder, air conveyor, drying oven, second air conveyor, and pulse grinder. Each station is specified independently — mixer batch capacity, extruder installed power, dryer fuel option, grinder motor rating — so you can see where material enters, how it moves, and what form it takes at each handoff point.
This matters because nutritional powder is not a single-step product. Starch must be preconditioned in the mixer, gelatinised under heat and shear inside the extruder barrel, stabilised at target moisture in the dryer, and then reduced to a specific particle size in the pulse grinder. If any station is undersized relative to the one before it, material queues, moisture shifts, and the powder specification drifts outside the range your market requires.
Sizing the Extruder Tier to Your Production Target
Four models — MT65, MT70, MT75, MT85 — span from small-batch nutritional powder runs to continuous production at higher volumes. Installed power steps from 84 kW to 210 kW, and physical footprint extends from 20 metres to 25 metres in line length [NEED_CITE: extruder motor power and barrel length relationship to residence time]. Choosing between them is not simply picking the largest number you can afford; it is matching screw diameter and barrel length to the residence time your formulation needs for full starch gelatinisation.
A baby rice flour making machine at the MT65 tier may be the right call for a facility that runs multiple short formulations per day — fortified blends, trial batches, or therapeutic powders that change weekly. The MT85, with its longer barrel and higher power draw, suits dedicated single-formulation lines where the grinder and dryer are also specified at the upper end of their ranges.
Reading the Specs That Actually Affect Powder Quality
The twin screw design is central to nutritional powder because it provides the mixing shear needed to fully gelatinise starch at relatively low moisture — something a single screw struggles with on high-fibre or high-protein formulations. Barrel material being food-grade stainless steel is not a marketing point; it prevents iron contamination that shows up as dark specks in light-coloured baby rice flour and triggers rejection on metal-detector checks downstream.
PLC and MCC control means temperature zones along the barrel, screw speed, and feeder rate are managed through one interface rather than individual dials. For nutritional powder where a five-degree shift in barrel temperature can move starch conversion outside the specification, this level of control is what keeps batch-to-batch consistency within the limits your lab requires. The drying oven’s selectable fuel source — electricity, gas, or liquid fuel — lets you match local energy costs and availability without redesigning the thermal profile [NEED_CITE: industrial drying oven fuel selection for food processing facilities].
The Hidden Cost of Mismatched Stations
A buyer once paired a high-output extruder with a dryer sized for a lower tier, reasoning that drying could be extended by slowing the line. What actually happened was that material sat too long in the dryer, over-dried on the surface while retaining internal moisture, and the pulse grinder then produced a powder that clumped in packaging. The extruder was never the bottleneck — the mismatch was [NEED_CITE: consequences of throughput imbalance in multi-station food processing lines].
When stations are sourced from different vendors, each one quotes against its own optimum. The dryer vendor does not know the extruder’s actual discharge moisture. The grinder vendor does not know the dryer’s exit temperature. The result is a line that runs but never hits the specification you showed your customer.
Why Procure This Line from One Equipment Range
The complete machine catalogue here means every station — from the 304 stainless steel mixer through the pulse grinder — is specified under one roof, so throughput calculations reference the same formulation data across all units. Screw configuration and die design are documented against your raw material rather than copied from a generic build, which is what protects your gelatinisation rate and powder density.
The testing workshop runs your actual grain or starch blend before the line ships, generating a trial run report that locks parameters for screw speed, barrel temperature profile, and dryer settings. Documentation covers line layout, electrical schematics with confirmed voltage and frequency, and a wear parts list so your first screw or die replacement does not arrive as a surprise [NEED_CITE: documentation standards for food extrusion machinery export].
Documentation & Verification
- Line layout and capacity calculation matched across mixer, extruder, dryer, and grinder
- Screw and die configuration record specific to your grain type and target mesh size
- Electrical schematic with voltage, frequency, and PLC language confirmed before production
- Trial run report on your raw material from the in-house testing workshop before shipment
- Wear parts list covering screws, dies, and grinder screens with replacement intervals
Installation, Commissioning & Support
- Foundation must accommodate the full line length, up to 25 metres for the MT85 configuration
- Dedicated three-phase circuit required at 380 V 50 Hz or confirmed alternative voltage
- Modular station assembly arrives in sections for sequential installation along the line axis
- PLC and MCC system commissioned on-site with barrel temperature zones calibrated to your formulation
- Operator training covers screw speed adjustment, dryer temperature profile, and pulse grinder screen changes
- First-year warranty with ongoing maintenance support and spare wear parts supply
What to Prepare Before Requesting a Quote
To size a twin screw extruder nutritional powder processing line correctly, share your raw material type and its typical moisture content, the target powder mesh size your market requires, and your planned daily production hours. Confirm your facility voltage and frequency, the control language your operators need, and whether any upstream or downstream equipment already exists on your floor. If you can send a sample of your grain or starch blend, the testing workshop will run it and return a trial report before any production commitment.
Frequently Asked Questions
Q: How is the output capacity for each extruder model verified?
A: Rated output depends on raw material type, incoming moisture content, and the target powder mesh size. Capacity figures listed for MT65 through MT85 are ranges that must be validated against your specific formulation. The testing workshop runs your actual material before shipment and documents the confirmed throughput in a trial run report.
Q: What supporting stations are included, and how is throughput balanced?
A: The full line covers mixer, screw conveyor, twin screw extruder, air conveyor, drying oven, second air conveyor, and pulse grinder. Each station is sized so its rated handling capacity matches the extruder output on your formulation, preventing bottlenecks at the dryer or grinder stage.
Q: What voltage and control options can be configured before production?
A: Standard configuration is 380 V, 50 Hz, three-phase, with other voltages available on request. The PLC and MCC control system supports multiple interface languages. Electrical schematics are confirmed with the buyer before production begins to match the destination facility supply.
Q: Can individual stations be ordered to match existing equipment?
A: Yes. Each mixer, dryer, and grinder is specified independently with its own power rating and capacity range. If you already have an extruder or upstream system, the remaining stations can be sized to match its actual discharge rate and moisture level.
Q: What documentation accompanies the line at delivery?
A: Buyers receive a line layout, machine specification sheet, screw and die configuration record, electrical schematic, trial run report on the buyer’s raw material, operation and maintenance manual, wear parts list, and packing photographs for customs clearance support.