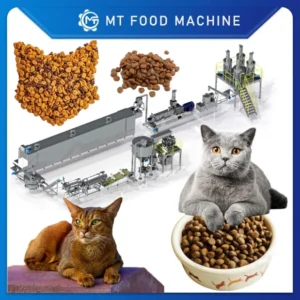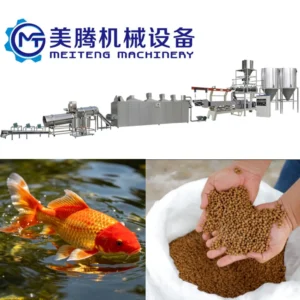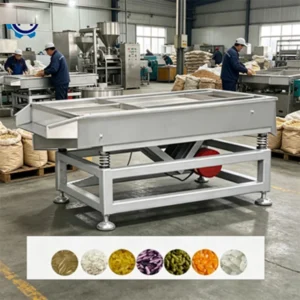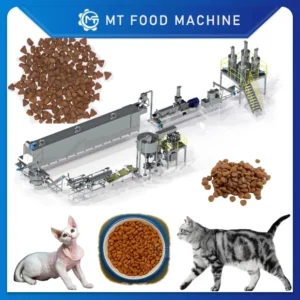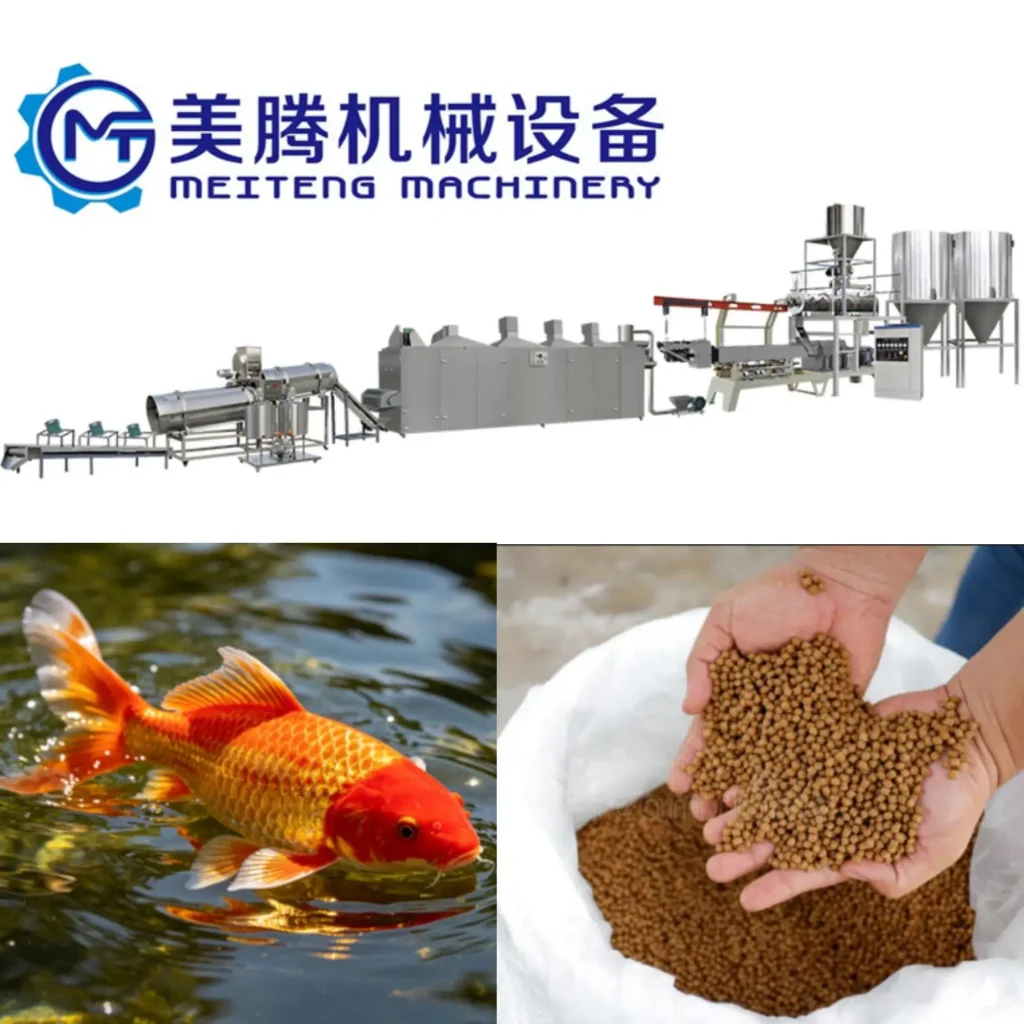
Integrated Line Engineering — throughput-matched stations from batching to packing ensure the dryer and coater never starve while the extruder runs at full screw speed.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fish Feed Processing Line |
| Extruder Type | Twin-screw extruder |
| Output Capacity | Up to 1.5 t/h (basis not stated in source — confirm raw material formulation, moisture content, and pellet size) |
| Construction Material | 304 stainless steel (food-grade contact parts) |
| Control System | PLC and MCC control |
| Application Species | Trout, salmon, catfish, and other fish species |
| Line Stations | Batching, mixing, extrusion, drying, coating, cooling, packing |
| Assembly State | Complete production line |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Floating aquaculture feed for trout and salmon | High-starch formulations requiring controlled expansion and low bulk density |
| Sinking feed for catfish and bottom-feeding species | Dense formulations with higher protein and fat content, minimal expansion at the die |
| Multi-species feed plants switching production runs | Variable raw material blends including fish meal, soy, corn, and vitamin premixes |
| Medium-to-high capacity aquaculture operations | Continuous production with matched drying and coating throughput |
Why "Rated Capacity" Means Nothing Without the Raw Material Context
A fish feed processing line manufacturer quoting 1.5 t/h on a standard corn-starch test blend tells you nothing about what happens when your actual formulation hits the barrel.
I have watched lines get crated and shipped after a successful factory trial on generic corn flour, only for the buyer to run their own high-protein, high-fat salmon feed on day one and find the pellets sinking when they should float. The screw configuration that expands a 60% starch mix beautifully will collapse entirely under a formulation loaded with fish meal and oils. The extruder is not the bottleneck — the mismatch between the screw profile and the buyer’s real recipe is. [NEED_CITE: starch gelatinisation thresholds in high-protein extrusion formulations]
Every fish feed processing line manufacturer should be asking for your raw material sample before they finalise the screw and die specification. If they are not, the capacity number on the quotation is a guess.
Barrel Zones and Temperature Control Across the Screw Length
The twin-screw extruder in this line uses multiple independently heated barrel zones. This matters because starch gelatinisation and protein denaturation happen at different temperatures, and the feed formulation determines which reaction dominates. A trout feed high in wheat flour needs a different thermal profile through the barrel than a catfish feed loaded with meat and bone meal. The PLC control maintains each zone within a tight band, preventing the surging that causes pellet density to drift mid-run.
Die Geometry and the Floating Versus Sinking Decision
The die plate at the end of the extruder barrel is where expansion is either encouraged or suppressed. For floating feed targeting trout or salmon in cage culture, the die orifice and land length are selected to allow maximum steam expansion as the pellet exits. For sinking feed, the same extruder barrel can produce dense pellets simply by changing the die specification and adjusting the moisture profile upstream. This flexibility is what allows one fish feed processing line to serve multiple species without a second extruder. [NEED_CITE: die land length effects on extrudate density in aquatic feed production]
Reading the Specs That Actually Determine Line Performance
The twin-screw configuration is specified here because single-screw extruders struggle with the high-fat, high-protein formulations common in salmonid feeds — the material slips on the barrel wall instead of being conveyed forward by the intermeshing screws. The 304 stainless steel contact surfaces are not optional in feed production; corrosion from salt-laden fish meal destroys carbon steel barrels within months. The PLC and MCC control system matters beyond simple automation: it logs barrel temperature, screw speed, and feeder rates for every production run, giving you traceability when a batch does not meet pellet durability index specifications. The capacity figure of up to 1.5 t/h requires confirmation against your specific raw material blend, pellet diameter, and target moisture at the dryer outlet — these three variables together determine whether the line holds that throughput or falls short.
The Bottleneck You Do Not See Until Commissioning Day
An extruder rated for a given throughput is useless if the downstream dryer cannot remove moisture fast enough to keep up. I have seen lines where the extruder runs for twenty minutes, then the operator has to stop and wait for the dryer to catch up because the belt length and air temperature were never calculated against the actual pellet moisture coming out of the die. The same problem appears at the coating drum — if it cannot tumble and spray fat onto the pellets at the extruder’s output rate, you get uneven coating and rancid spots within days of bagging. [NEED_CITE: dryer capacity matching in extruded feed line design]
What This Supplier Does Differently at the Engineering Stage
Every station on this line — batching, mixing, extrusion, drying, coating, cooling, packing — is specified under one supplier so that throughput is calculated end-to-end before fabrication starts. The screw configuration and die design are matched to the buyer’s raw material formulation, not copied from a generic build. An in-house testing workshop runs the buyer’s actual raw material before the line ships, catching density and expansion problems at the factory instead of on the buyer’s floor. The 304 stainless steel construction on all food-contact surfaces is standard, not an upgrade. Electrical schematics are confirmed against the buyer’s local voltage and frequency before the control panels are wired.
Documentation & Verification
- Line layout and capacity calculation showing throughput match across batching, extrusion, drying, and packing stations
- Screw and die configuration record specified to your raw material formulation and target pellet density
- Factory trial run report on your actual fish meal and starch blend conducted before crating
- Electrical schematic with voltage, frequency, and control language confirmed to your local standard
- CE declaration of conformity and ISO certificate for customs and regulatory submission
- Wear parts list with screw element and die specifications for reorder
Installation, Commissioning & Support
- Foundation load and floor space plan matched to the full line footprint from batching silos to packing station
- Dedicated power circuit specification for the twin-screw extruder main drive and dryer heating elements
- Assembled and factory-tested before dispatch, with modular frames for container loading and on-site reassembly
- First-run commissioning on your raw material with barrel temperature and screw speed profiling
- Operator training covering PLC navigation, screw element replacement, and die changeover procedure
- Wear parts inventory recommendation covering screw elements, die plates, and dryer belt sections
What We Need to Move from Inquiry to Line Proposal
Send us your raw material formulation — the actual fish meal, starch, fat, and premix percentages you plan to run — along with your target pellet diameter and whether you need floating, sinking, or both. Confirm your local voltage and frequency, and whether you need the HMI in a language other than English. If you have an existing dryer or packing system you want to integrate, share the make and throughput rating so we can match the new extruder output to your current downstream equipment.
Frequently Asked Questions
Q: How is the output capacity verified, and what raw material formulation is it based on?
A: The stated capacity requires confirmation against your specific formulation, pellet size, and target moisture. We run your actual raw material in our testing workshop before shipment, documenting the achieved throughput, pellet density, and expansion ratio in a trial report you receive with the line documentation.
Q: Which screw configuration and die design is selected for floating versus sinking feed?
A: Floating feed requires a screw profile that maximises shear and steam expansion at the die, with a short land length to allow rapid pressure release. Sinking feed uses a higher-compression screw and a longer die land to suppress expansion. Both configurations are available for this line and are selected based on your trial run results.
Q: How are dryer and coating station capacities matched to the extruder?
A: The dryer belt length, air temperature, and residence time are calculated from the extruder output rate and the moisture differential between die exit and target bagging moisture. The coating drum volume and spray rate are sized to handle the same throughput without accumulation or uneven fat distribution.
Q: What voltage, frequency, and control language options are confirmed before shipment?
A: We confirm your local grid voltage and frequency before the electrical panels are wired, and the PLC and MCC are programmed accordingly. The HMI language is set to your preference. This is documented in the electrical schematic provided before production begins.
Q: Are spare wear parts available, and what is the recommended replacement schedule?
A: Screw elements, die plates, and dryer belt sections are listed in the wear parts document shipped with the line. Replacement intervals depend on your formulation abrasiveness — high-fibre or mineral-heavy feeds accelerate screw wear. We recommend an initial spare set on first order to avoid production stops while replacements are in transit.