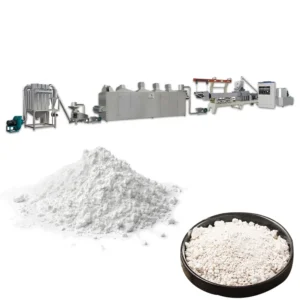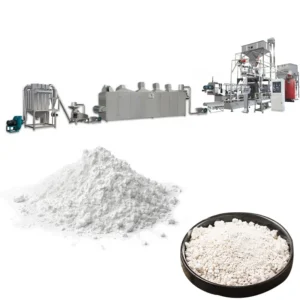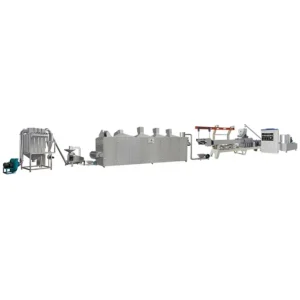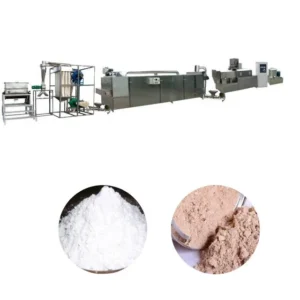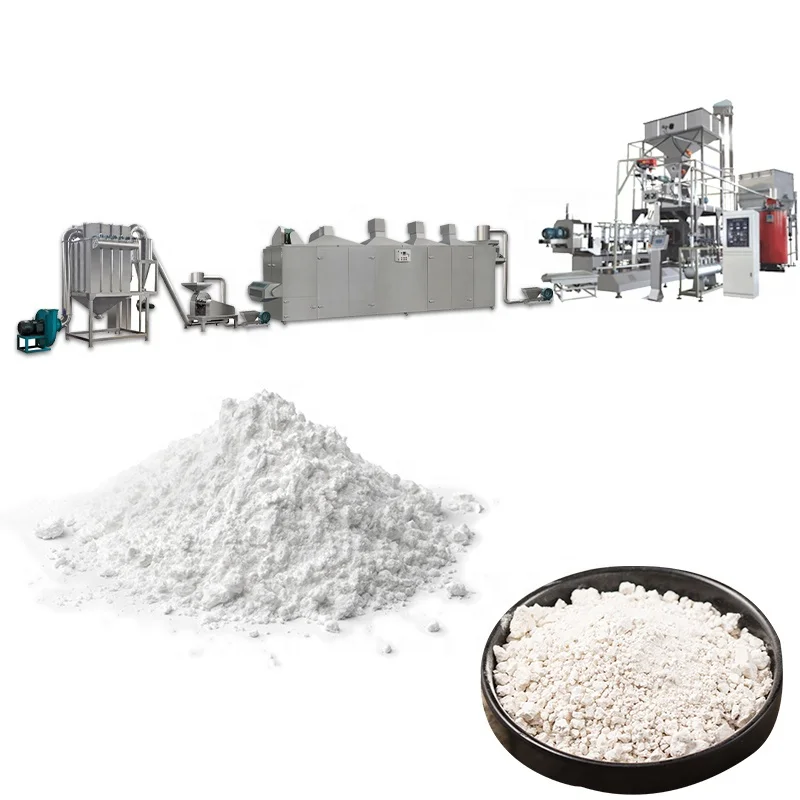
Full-range equipment catalogue — Every station from batching through extrusion to grinding is specified to the buyer’s raw material, ensuring matched throughput rather than a collection of mismatched standalone machines.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extrusion Modified Starch Processing Line |
| Screw Type | Twin-screw extruder |
| Raw Materials | Wheat flour, corn starch, potato starch |
| Output Capacity | 80–500 kg/h (basis not stated in source — confirm raw material type, moisture content, and modification degree) |
| Process Flow | Mixer → Screw Conveyor → Twin Screw Extruder → Air Conveyor → Dryer → Air Conveyor → Conditioning → Conveyor → Grinder |
| Energy Options | Electricity, gas, diesel, or steam |
| Rated Power | approx. 100 kW (electric heating) / 50–60 kW (gas or diesel heating) |
| Frame Material | Stainless steel 201 |
| Contact Material | Food-grade stainless steel 304 |
| Motor Brand | Siemens (China) or equivalent top Chinese brand |
| Inverter | Delixi or Delta |
| Mixer Main Motor | 4.0 kW |
| Mixer Dimensions | 1.2 × 0.9 × 1.4 m |
| Screw Conveyor Main Motor | 1.1 kW |
| Screw Conveyor Dimensions | 2.5 × 0.6 × 2.3 m |
| Screw Conveyor Output | 0–150 kg/h |
| Die Configuration | Adjustable dies for different product shapes |
| Voltage & Frequency | Three phase 380V/50Hz, Single phase 220V/50Hz (customizable to local voltage) |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Food-grade modified starch for sauces, bakery, and confectionery | Wheat flour, corn starch, potato starch |
| Industrial starch adhesives for paper and packaging | Corn starch |
| Pre-gelatinised starch for nutritional and infant formula | Wheat flour, corn starch |
| Modified starch for textile sizing and drilling fluids | Potato starch, corn starch |
What the Nominal Capacity Figure Leaves Out About Your Modified Starch Line
A capacity number without a raw material specification is just a starting guess, not a production guarantee.
When buyers compare modified starch processing line equipment for sale, the first question is often output per hour. But a line quoted on a generic starch may not hold that throughput on your actual feedstock. Corn starch behaves differently from potato starch inside a twin-screw barrel — the gelatinisation temperature, moisture uptake, and melt viscosity all shift. A screw configuration that works for one material can choke or surge on another, dropping effective output and producing inconsistent modification [NEED_CITE: starch gelatinisation behaviour under twin-screw shear]. The only way to validate capacity is a trial run on the buyer’s own raw material before the line ships.
Matching Every Station on the Starch Line
A modified starch processing line is only as productive as its slowest station. The mixer must deliver a batch size that keeps the twin-screw extruder fed continuously; the dryer must have enough residence time to bring moisture down to target without bottlenecking the extruder output; the grinder must clear the dried product at the same rate it arrives. When these stations are sourced from separate vendors, the interfaces are where capacity disappears — a hopper too small, a conveyor too slow, a dryer belt that cannot keep up. Cataloguing the full range of supporting equipment means every station is specified together, with throughput calculated end-to-end.
The Role of Screw and Die Design in Starch Modification
The twin-screw extruder is where the actual modification happens. Shear, temperature, and residence time inside the barrel determine the degree of gelatinisation and the final starch properties — viscosity, gel strength, water-binding capacity. Screw elements are arranged in zones that control mixing intensity and forward conveyance, while the die shapes the extrudate before drying. Different starch targets — high-viscosity food starch versus a lower-molecular-weight paper adhesive — require different screw profiles and die geometries [NEED_CITE: twin screw element configuration for starch modification]. Recording the screw and die specification against each buyer’s raw material ensures the configuration is reproducible in future production runs.
Reading the Specs: What the Numbers Mean for Starch Output
The rated power split between electric heating and gas or diesel heating reflects two fundamentally different energy strategies. Electric barrel heaters offer precise zone control, which matters when a few degrees’ difference shifts the gelatinisation outcome. Gas or diesel heating reduces peak power demand, which is relevant where electrical supply is limited. The stainless steel 304 contact surfaces are a non-negotiable requirement for food-grade starch applications, preventing contamination and meeting sanitary standards. The screw conveyor’s enclosed design at 0–150 kg/h capacity prevents starch dust from escaping into the workshop, which is both a safety and a product-loss consideration. Finally, the inverter choice between Delixi and Delta determines motor speed control precision, which directly affects feed consistency into the extruder barrel.
When Stations Are Mismatched
A line assembled from independent purchases often hits a wall at the dryer. The extruder runs at target output, but the dryer cannot remove moisture fast enough, so the conveyor backs up and the extruder must be throttled down. Operators then adjust screw speed to compensate, which changes shear and residence time, shifting the modification degree away from specification [NEED_CITE: throughput bottleneck between extruder and dryer in starch lines]. The result is product that does not meet the buyer’s viscosity or gel-strength target, and a production rate far below the quoted number. This is the most common failure mode on starch lines where no single supplier matched the stations.
Why Source the Full Range from One Catalogue
Complete line coverage means the mixer batch cycle, extruder throughput, dryer belt speed, and grinder capacity are all calculated together before production begins. Screw configuration and die design are specified against the buyer’s exact raw material and target starch properties, not copied from a generic build. An in-house testing workshop allows trial runs on the buyer’s starch before shipment, validating product specification and throughput. The electrical schematic and voltage are confirmed against the destination country standard before the control panel is wired. CE certification covers the full line as an integrated system, not individual machines in isolation [NEED_CITE: CE machinery directive requirements for integrated production lines].
Documentation & Verification
- Line layout and capacity calculation matched across mixer, extruder, dryer, and grinder
- Screw and die configuration record tied to your starch raw material
- Electrical schematic with voltage and frequency confirmed to local standard
- Factory trial run report on your raw material before dispatch
- CE declaration of conformity covering the complete line
Installation, Commissioning & Support
- Foundation and floor space plan reflecting the full line footprint from mixer to grinder
- Dedicated three-phase circuit sized to the 100 kW electric heating peak load
- Modular station delivery with assembly sequence planned for workshop access
- First-run parameter logging for screw speed, barrel temperature, and dryer residence time
- Operator training covering screw element changeover and die adjustment
- Wear parts list for screws, dies, and conveyor seals with replacement intervals
What to Prepare Before Requesting a Quotation
To configure a modified starch processing line that holds capacity on your actual feedstock, we need the specific starch type — corn, wheat, or potato — along with the target modification and end-use application. Share your local voltage, frequency, and preferred energy source for the dryer. If the line will integrate with existing upstream or downstream equipment, provide the interface heights and conveyor speeds so throughput matching can be verified before production.
Frequently Asked Questions
Q: How is the output capacity of 80–500 kg/h verified on my raw material?
A: The capacity range is a general indicator that depends on the specific starch type, incoming moisture, and degree of modification targeted. Verification happens through a trial run on your raw material in the testing workshop before shipment, where actual throughput and product specification are recorded and reported.
Q: Can the voltage, frequency, and control panel language match our local standard?
A: Yes. The standard configuration is three-phase 380V/50Hz, but voltage and frequency are customizable. The control panel language is confirmed during the specification stage, before the electrical cabinet is wired, so operators can read alarms and parameters in their working language from day one.
Q: How are screw configuration and die design selected for different starch targets?
A: Screw elements are arranged to deliver the shear and residence time your modification requires — high-viscosity food starch and low-molecular-weight adhesive starch use different profiles. Die geometry controls extrudate shape and expansion before drying. Both are recorded against your raw material for repeatability.
Q: What supporting equipment is included and how is throughput matched?
A: The line includes mixer, screw conveyor, twin-screw extruder, air conveyors, dryer, conditioning station, conveyor, and grinder. Each station’s capacity is calculated so the mixer batch size, extruder output, dryer residence time, and grinder clearance rate all align without bottlenecks.
Q: Is a trial run on our raw material possible before shipment?
A: Yes. The in-house testing workshop runs your starch through the configured line, producing a test report that covers actual throughput, product viscosity or gel strength, moisture content after drying, and particle size after grinding — all validated before the equipment leaves the factory.